An aluminium stage plate for medical devices is mostly datum: dowel holes, a tapped pattern and a flatness callout leave very little room for rounding or distortion. A buyer in Amsterdam, Netherlands can send a representative plate to SurfacePolish, a cross-border supplier of finishing machines, media and compounds, for a free sample trial. This brief is written for a buyer in Amsterdam working on medical devices; it describes equipment, media and a scoped sample review, not a local polishing service.
Who defines and verifies the cleanliness, residue and any regulatory requirement, and by what method and limit?
Which surfaces on this aluminium part carry a cosmetic grade, which are functional seating or sealing faces, and which are indifferent?
What are the alloy and temper, and has machining, casting, welding or heat treatment already changed the surface hardness and porosity?
Thin aluminium walls are the most common source of trouble in a vibratory or barrel route. Below roughly two millimetres of wall, part-on-part contact and media impact bend a rib, peen a flange or drive small media into a pocket where it wedges and stays. Blind holes, cross-drillings, undercuts, fine threads and knurled bands all trap media, and a lodged piece of ceramic later shows up as a rattle, a scored bore or a rejected assembly. Count the features that cannot be inspected easily from outside, then decide whether they need masking, a plug, a fixture that shields them or a different route entirely. A thin-wall housing that survives one cycle may not survive a hundred, so ask for wall thickness and unsupported span rather than assuming them.
A round bowl vibrator suits small to medium aluminium components that tumble freely and pass a media gate: instrument handles, ferrules, cover plates, brackets. It gives good part-to-part uniformity because the whole load circulates through the same energy field, and it is easy to automate with compound flow and a discharge gate. The limit is size and shape. A long extruded frame, a tall manifold or a part with a protruding boss will not circulate well in a bowl and will shadow itself, leaving the sheltered side unfinished. Tub vibrators handle long and large parts because the working channel is linear and the part can be oriented; the trade-off is slower uniform coverage and a greater tendency for parts to settle in one attitude. Match machine to part envelope first, then to finish.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Rotary barrel finishing machine | Gentle, low-energy deburring of small precise aluminium parts in high volume, including thin and light components | Longer cycles for the same result; flat or light parts may slide rather than tumble, and an overloaded barrel stops working the load |
| Dry polishing machine and dryer | Post-wet drying and dry polishing of aluminium parts before anodising, laser marking, bonding or packaging | Does not remove a burr or refine a surface on its own; residual media dust and incomplete drying still cause marking and coating defects |
| Grinding finishing machine | Higher material removal on aluminium parts that need a heavy burr or a pronounced chamfer removed before a gentler finishing step | Aggressive on soft aluminium, difficult to control on cosmetic faces and functional edges, and not a finishing step on its own |
| Disc finishing machine | Fast burr removal and edge radiusing on robust aluminium parts where a short cycle and high material removal matter most | High part-on-part contact and impingement risk; smears soft 6061, is hard to localise, and adds fixturing labour to every cycle |
Aluminium reacts to both strong acid and strong alkali, so compound chemistry deserves more care here than on steel. A mildly alkaline or near-neutral cleaning and burnishing compound with a suitable inhibitor is the usual starting point for aluminium, because a strongly alkaline product etches the surface, darkens it and attacks exposed edges, while a strongly acidic one can pit it and leave smut. The compound also carries debris and controls foam, lubricity and rinsing, so concentration and flow rate matter as much as family. Water quality is part of the chemistry: hard water leaves mineral spotting and deposits, chloride content in the supply raises a corrosion concern on aluminium, and a recirculated system concentrates fines and dissolved metal over time. Set a working range for concentration, pH and flow, then monitor and correct it during the shift.

| Media | Best fit | Watch out for |
|---|---|---|
| Ceramic media, spheres and low-density ceramic, fine size class | Bright surface development and light edge work on small aluminium components with mixed cosmetic and internal features | Fine media lodges in blind holes, cross-drillings and thin-wall pockets and is harder to screen out of the load |
| Plastic-bonded media, ball and ellipsoid shapes | Surface refinement and blending on cosmetic aluminium faces where edges, seal lands and dowel bores must stay close to drawing | Removes very little edge material, so a burr at a bore exit or a thread crest may survive the cycle and need a separate step |
| Dry media, walnut shell, fine grade | Dry polishing, light surface cleaning and preparation before anodising or laser marking on aluminium parts | Shell dust must be extracted and the part cleaned, or the residue interferes with marking, bonding or a later coating step |
| Dry media, corn cob with a polishing compound charge | Final dry polish and drying assistance on small aluminium parts where a wet rinse and dry would leave spotting | Compound loading saturates with use and the media cakes; the charge needs regular replacement, and soft aluminium can still smear |
Media cannot tell a cosmetic edge from a sealing edge, so a cycle that breaks a burr nicely on the outside of a housing can round a seal land, a dowel bore or a press-fit shoulder until it no longer functions. The drift is gradual and cumulative: each pass removes a little more material, and a batch that was within tolerance at the start of a media charge may be outside it by the end. Watch for a seal face that has lost its flat land, a bore edge closed to a radius, or a chamfer grown past the drawing. Detect it with an optical comparator or radius gauge on a cross-section, or by measuring the feature with a CMM before and after. Protection comes from shielding the functional edge, rounder and lighter media, and a first-article check.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Finish bloom or speckle, or poor laser mark contrast, revealed after anodising or marking | Embedded media, a silicate or residue film, a directional texture that marks unevenly, or an oxide layer from a slow dry | Evaluate the appearance on a coated or marked sample rather than bare metal, and compare marking contrast on parts from different positions in the load |
| Damaged thread or media wedged in a thread root | Threads left exposed to the media field, sharp media entering the crest, insufficient plugging or masking of ports before the cycle | Run a go and no-go gauge through every sampled thread and inspect the root with a borescope or a thread impression |
| Dimensional drift on a critical bore, dowel hole or press-fit diameter | Aggressive media attacking a feature the cycle should not touch, cumulative removal over repeated runs, no masking of close-tolerance geometry | Measure the feature with a CMM or bore gauge at first article and at the end of the media charge, and chart the trend against drawing limits |
| Black smut or scattered dark specks on the finished surface | Iron transferred from steel media, a shared barrel, worn machine parts or a shared media store; galvanic reaction on the soft aluminium surface | Examine under magnification and with a light acidified wipe, and audit media storage, barrel liners and screening equipment for steel contact |
Amsterdam's industrial base is organised around the Port of Amsterdam and the North Sea Canal rather than around large manufacturing campuses. In 2024 the port handled 62.2 million tonnes of cargo; coal fell to 6.6 million tonnes while dry bulk grew, with agribulk reaching 7.1 million tonnes (+12%), and oil products held at 29.1 million tonnes. CBS counted 4,170 industrial establishments (SBI C) in the municipality on 1 January 2026 out of 216,360 business establishments in total. The port's 2040 vision positions it as a destination port for clean shipping, circular industry and renewable energy.
The nearest part of that base to this brief is machinery: CBS recorded 4,170 industrial establishments (SBI C Industrie) and 160 energy-supply establishments in Amsterdam on 1 January 2026.
Agri-food, edible-oil and energy bulk handling in the port depends on stainless and carbon steel pumps, valves, pipework, tanks and conveyors, where burr removal, weld dressing and passivation of wetted surfaces affect both corrosion resistance and cleanability. Terminal and ship-repair work is typically low-volume and part-specific, so the practical question is usually media and process selection for mixed stainless and carbon steel parts rather than high throughput.
Before selecting equipment, a buyer here should settle whether the parts are hygienic stainless (cleanability, passivation, no media embedded in the surface) or structural carbon steel (edge radius, burr height, Ra), because that decision drives media and compound chemistry far more than machine size does.
Freight context: Port of Amsterdam (North Sea Canal), IJmuiden sea lock (Zeesluis IJmuiden). The harbour is a combined sea and inland-barge port; Port of Amsterdam reported 99 sea cruise calls and 1,880 river cruise calls in 2024. Machinery imported from outside the EU is declared to Dutch Customs at the point of entry and needs an EORI number, while goods arriving from another EU member state are not declared to customs at all.
The Dutch standards body is NEN (Nederlands Normalisatie-instituut), which publishes and maintains the NEN and NEN-EN-ISO standards; the content of a standard is set by a NEN standards committee made up of the organisations concerned, not by NEN itself. For surface finishing NEN publishes NEN-EN-ISO 2080, which defines the terms for the general types of surface-finishing processes with emphasis on practical use in metal finishing, under the standards committee for metallic coatings and corrosion of metals and alloys. Machinery safety, EMC, low-voltage, ATEX, RoHS and ecodesign requirements reach Dutch buyers through the CE directives and regulations referenced by KVK, with the Machinery Regulation applying from 20 January 2027.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Appearance is the requirement most likely to be argued about, because it is easy to state and hard to define. Agree a physical reference: a first-article part or a set of graded coupons, viewed under a stated light source, at a stated distance and angle, by a named inspector. Record whether the accepted finish is bright, satin, directional or non-directional, and whether machining marks may remain visible. If the part will be anodised later, the finish that looks correct as bare aluminium may look different after anodising, because the coating is partly transparent and the underlying texture remains; evaluate the appearance on an anodised sample rather than bare metal. Keep reference parts labelled, protected and stored, because a visual standard that lives only in memory changes with every batch.
A sample trial is most useful when it isolates one change. If media family, size, compound and cycle time all change together, a difference in the result cannot be attributed to anything and the trial cannot be repeated. Ask for a small matrix: the same parts run with two media families at the same cycle, or the same media at two cycle times, with every other condition held constant and a record of the settings used for each cell. Photograph or measure each result on the same features under the same lighting, and keep an untreated reference beside them. Reproducibility deserves attention too: one good part proves little, so ask whether the result repeated on the other pieces in the charge. A trial yields observations on the parts tested, not a guaranteed production result.
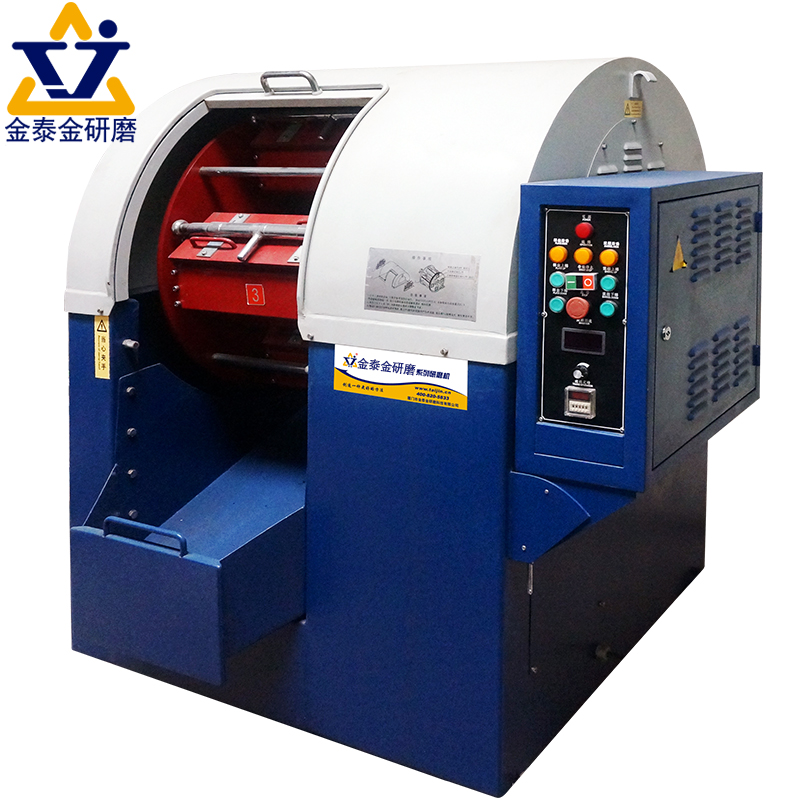

A bowl vibrator circulates a load through a media field at moderate energy, with good uniformity on small parts that tumble freely and easy discharge. A centrifugal barrel presses media and parts together at high force in a much shorter cycle, producing a fine finish and controlled edge quickly, but bending thin walls, distorting light sections and rounding edges faster. Bowl routes suit mixed small parts and gentle work; centrifugal routes suit a narrow part family that fits the barrel and accepts the energy. Parts made in Netherlands should be trialled in the specific geometry before a machine size is fixed, because barrel dimensions limit part length and load size.
Keep the aluminium loop physically separate. Steel media, steel barrels, worn machine parts and shared screening equipment all transfer iron to a soft aluminium surface, and the result shows as black smut, dark specks or a galvanic couple that becomes visible under a coating or after anodising. Dedicated media, a dedicated barrel or bowl liner, separate screens and separate storage are the practical controls, along with a check of the finished surface under directional light. For a plant in Netherlands running both steel and aluminium work, the segregation rule needs to cover media storage and top-up stocks, not only the machine, because a shared media bin reintroduces the contamination.
Laser marking interacts with surface texture, so contrast depends on whether the surface is directional, random satin or bright. A strong directional finish from a tub or a linishing step can produce a marking that reads differently when the part is turned, while a uniform random texture marks more consistently. Residue and embedded media also interfere, because the marking energy meets a contaminated surface. For a marked cover plate in Netherlands, the practical sequence is to fix the finish first, then qualify the marking programme on finished parts, and to check the mark under the lighting the end user will use rather than a bench lamp.
Use Amsterdam, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A local buyer would reference the CE marking regime for machinery — with the Machinery Regulation replacing the Machinery Directive and compliance required by 20 January 2027 — and the Dutch/EN-ISO surface-finishing vocabulary published by NEN, notably NEN-EN-ISO 2080 for metal-finishing terms. Food-contact and wetted-surface work is normally specified through the customer's own hygiene and material requirements rather than through a single national finishing standard.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Amsterdam.
The buyer must remove machining burrs from the hole pattern without moving the dowel hole edges or disturbing the plate's flatness.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0603; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0603 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
