High-volume small aluminium components for medical devices live or die on part-to-part consistency, and a batch of several thousand ferrules in Bengaluru, India will show any weakness in media size class, screening or load control. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on the buyer's parts. This brief is written for a buyer in Bengaluru working on medical devices; it describes equipment, media and a scoped sample review, not a local polishing service.
What downstream operation follows finishing, such as anodising, laser marking, bonding or assembly, and what does it require of the surface?
What are the alloy and temper, and has machining, casting, welding or heat treatment already changed the surface hardness and porosity?
Which surfaces on this aluminium part carry a cosmetic grade, which are functional seating or sealing faces, and which are indifferent?
Controlled edge rounding is where a finishing route earns or loses its place. Every machined aluminium edge carries a burr and a stress concentration, and a deburring cycle removes both, but it also moves the edge position. On a mating face, a seal groove, a bearing seat or a dowel hole that movement is a functional change, not a cosmetic one. Establish the allowed edge radius or chamfer per feature, then measure the finished edge against it rather than judging by eye, using an optical comparator or a radius gauge on a sectioned or replica sample. A part with generous cosmetic edges and one tight sealing edge usually needs a shielded fixture or selective hand finishing after the machine cycle. Deciding this after the first batch has run is how an assembly ends up with a leak path.
Aluminium reacts to both strong acid and strong alkali, so compound chemistry deserves more care here than on steel. A mildly alkaline or near-neutral cleaning and burnishing compound with a suitable inhibitor is the usual starting point for aluminium, because a strongly alkaline product etches the surface, darkens it and attacks exposed edges, while a strongly acidic one can pit it and leave smut. The compound also carries debris and controls foam, lubricity and rinsing, so concentration and flow rate matter as much as family. Water quality is part of the chemistry: hard water leaves mineral spotting and deposits, chloride content in the supply raises a corrosion concern on aluminium, and a recirculated system concentrates fines and dissolved metal over time. Set a working range for concentration, pH and flow, then monitor and correct it during the shift.

| Media | Best fit | Watch out for |
|---|---|---|
| Alumina-based ceramic media, low-density, cylindrical and pin shapes | Internal bores, slots and cross-holes on small aluminium components that a rounded tumbling body cannot reach | Pin and cylinder shapes can wedge in a bore or a slot; confirm retrieval and inspection before running a production batch |
| Steel media, balls or pins, for bright polishing | Bright reflective finish on hard, robust steel work where a high lustre is the primary requirement | Deposits iron on aluminium, causing black smut, staining and a galvanic couple; keep it out of any loop shared with aluminium parts |
| Plastic-bonded media, light to medium abrasive grade, cone and triangle shapes | General deburring and satin finishing on 6061 and 7075 where galling risk rules out dense ceramic | Wears quickly and loses edge definition; cut rate drops as the charge ages and the cosmetic result drifts unless media is screened and topped up |
| Dry media, walnut shell, fine grade | Dry polishing, light surface cleaning and preparation before anodising or laser marking on aluminium parts | Shell dust must be extracted and the part cleaned, or the residue interferes with marking, bonding or a later coating step |
Magnetic finishing works on small aluminium parts with fine internal features, using a magnetic field to drive small pins or abrasive media through holes, slots and recesses that a tumbling load cannot reach. It is useful on small fittings, valve spools, connector components and parts with internal cross-holes, and it can be gentle enough for thin sections if field strength and cycle are controlled. Its limits are size and throughput: the working envelope is small and the process suits a narrow part family rather than a mixed batch, and fine media or pins lodge in blind features just as tumbling media do, so retrieval and inspection matter. Dry polishing machines and dryers handle the post-wet step, removing water from blind holes before anodising or laser marking, where a trapped droplet becomes a stain or a marking defect.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Grinding finishing machine | Higher material removal on aluminium parts that need a heavy burr or a pronounced chamfer removed before a gentler finishing step | Aggressive on soft aluminium, difficult to control on cosmetic faces and functional edges, and not a finishing step on its own |
| Dry polishing machine and dryer | Post-wet drying and dry polishing of aluminium parts before anodising, laser marking, bonding or packaging | Does not remove a burr or refine a surface on its own; residual media dust and incomplete drying still cause marking and coating defects |
| Tub vibrator | Long and large aluminium parts such as extruded frames and housings that can be oriented in a linear working channel | Slower uniform coverage, a tendency for parts to settle in one attitude, and greater floor space and media volume than a bowl |
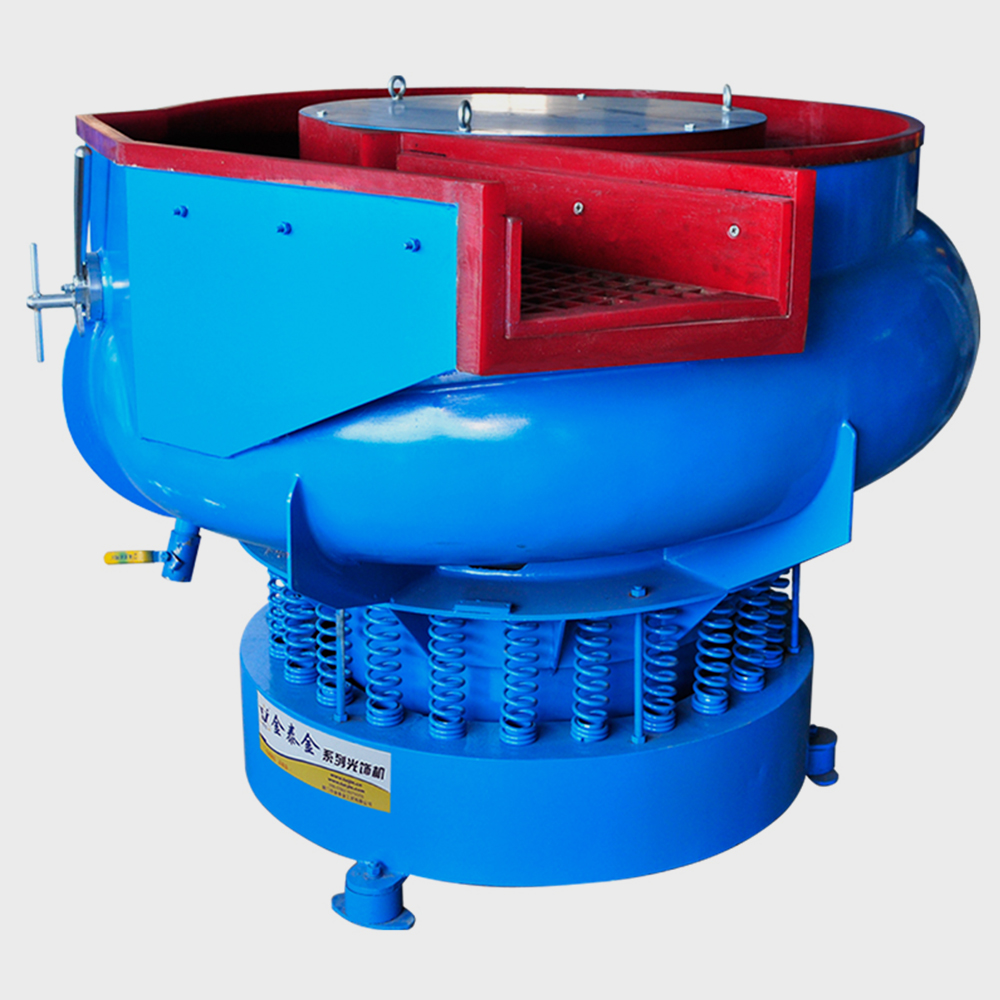
| Vibratory bowl finishing machine | Small to medium aluminium components that tumble freely: ferrules, handles, brackets and cover plates needing uniform deburring or satin finishing | Long, tall or heavily recessed parts shadow themselves and finish unevenly; part envelope must fit free circulation in the bowl |
Aluminium can leave a finishing cycle looking worse in colour than it went in. Over-alkaline compound etches and darkens the surface; hard water leaves mineral spotting that dries into rings; iron transferred from steel media or worn machine parts appears as black smut or scattered dark specks; and a slow or hot dry lets an oxide film form unevenly across a face. Castings with porosity are especially prone, because they hold liquid and release it later as a bloom. Check the part dry, under the lighting the customer will use, and compare against a retained reference part rather than memory. Control compound pH and concentration, rinse with controlled water quality, dry promptly and completely, and keep steel out of the aluminium loop. A stain found after anodising or packaging has already cost the value of the part.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Finish bloom or speckle, or poor laser mark contrast, revealed after anodising or marking | Embedded media, a silicate or residue film, a directional texture that marks unevenly, or an oxide layer from a slow dry | Evaluate the appearance on a coated or marked sample rather than bare metal, and compare marking contrast on parts from different positions in the load |
| Sealing land or dowel bore edge rounded past the drawing limit | Long or energetic cycle on an unprotected functional edge, sharp-edged media, cumulative material removal across repeated passes | Measure the edge with an optical comparator or radius gauge on a cross-section, or compare a CMM scan of the feature before and after finishing |
| Uneven finish with bright and dull bands on the same face | Part settling in one attitude, self-shadowing on a long or recessed part, wrong load ratio, media too large to flow around the geometry | Compare several parts taken from different positions in the load under directional light rather than sampling only the discharge gate |
| Galled, smeared or picked surface with transferred aluminium | Media too heavy or too dense for the alloy, insufficient compound lubricity, hot or overloaded charge, aluminium parts rubbing against each other | Inspect under low-angle directional light for smears and cold welds, then wipe with a white lint-free cloth to reveal transferred metal |
Bengaluru anchors Karnataka's industrial base. Invest Karnataka, the state's investment-promotion agency, describes Karnataka as the second highest producer of heavy electrical machinery in India and as home to DRDO, ISRO, HAL and BEML, and states that the state is developing a Hi-Tech Aerospace and Defence Park of about 1,000 acres at Devanahalli, Bangalore, with forging, precision machining, surface treatment and aero assemblies listed among the capabilities of its aerospace and defence parks. Karnataka accounts for 8.5% of India's total automobile output and hosts leading global vehicle and component companies, and the state records 85+ chip designing houses, 55% of the country's IoT startups and a dedicated electronics manufacturing cluster at Adinarayana Hosahalli in Bengaluru Rural. On the life-sciences side the state supplies over 10% of India's pharma revenues and 60% of its biotech revenues, with the Bangalore Helix biotechnology park and the Bangalore bio cluster in the city.
For this brief the relevant part of that base is medical: Over 10% of India's pharma revenues and 60% of India's biotech revenues come from Karnataka, which hosts the Bangalore Helix biotechnology park and the Bangalore bio cluster.
The part mix here — forged and machined aerospace structures, precision auto components and electronics tooling — makes burr removal, edge condition and surface finish production concerns rather than cosmetic ones, because they affect fit, fatigue behaviour and assembly. Karnataka's aerospace park brief lists surface treatment among the capabilities the state is set up to host, and the region's machine-tool, foundry and precision-machining suppliers work to drawing callouts on edge radii and Ra/Rz. Buyers typically have to settle whether the requirement is edge control on a machined feature or a specified finish on a functional face, since those two aims select different machine types and media.
A Bengaluru buyer should first settle which requirement governs acceptance — edge or radius control on a machined or forged feature, or an Ra/Rz value on a functional surface — because that determines the process type and media, and whether a customer-specific surface specification requires trial parts before a process is frozen.
Freight context: Kempegowda International Airport, Bengaluru (KIA), Inland Container Depot, Whitefield (CONCOR), Bengaluru Urban, Chennai, JNPT and Krishnapatnam ports (300-400 km). Invest Karnataka's logistics page records KIA as holding a 42% share of south India's air cargo market and lists 3 inland container depots (Whitefield/CONCOR among them) and 5 container freight stations with rail connectivity to ports; the same page puts the Chennai, JNPT and Krishnapatnam ports 300-400 km away. Air-freighted machines and sample parts clear at Bengaluru airport, while sea freight normally moves by rail from those ports to an inland container depot.
India's foreign-trade, customs and standards machinery works in English: the Foreign Trade Policy, DGFT's IEC and scheme material, the BIS standards catalogue and Invest India's investor guide are all published in English, and the mandatory import documents are the internationally conventional bill of lading, commercial invoice cum packing list and bill of entry (c1, c3, c6, c10). Payment in the import channel is bank-intermediated; the Foreign Trade Policy treats the irrevocable commercial letter of credit as the instrument that fixes an importer's commitment when import policy changes (c4), so a supplier should expect LC or advance terms rather than open-account credit on a first order. Indian industry associations are explicit about import substitution: the Bombay Chamber of Commerce and Industry states that one of its major focuses today is how to expand manufacturing setups and substitute imported products (c13), so a cross-border equipment seller should expect questions about local support, spares, training and total cost of ownership rather than price alone, and should hold the IEC, GST registration, bill of entry documentation and any BIS obligation as part of the commercial discussion.
An Importer-Exporter Code (IEC) issued by DGFT is a key business identification number which is mandatory for exports or imports, and since the introduction of GST the IEC number is the same as the PAN of the firm (c6). The post-incorporation clearance list published by Invest India includes the IEC, a Customs- Special Valuation Branch reference and the grant of a Bureau of Indian Standards (BIS) licence, and it names the Central Board of Excise and Customs among the agencies in the framework (c10). The Foreign Trade Policy fixes the mandatory import documents as a bill of lading / airway bill / lorry receipt / railway receipt, a commercial invoice cum packing list and a bill of entry, with additional documents or NOCs possible for goods subject to product-specific compliance (c3); it also states that domestic laws, rules, orders, technical specifications and environmental, safety and health norms applicable to domestically produced goods apply mutatis mutandis to imports unless specifically exempted (c2), which is the basis on which a BIS quality-control order can bite on imported machinery. A landed-cost plan therefore needs the correct ITC(HS) classification and the basic customs duty and IGST that follow from it, plus the IEC, the bill of entry documentation and any BIS licence or registration obligation, and a related-party import can additionally be pulled into special customs valuation.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Appearance is the requirement most likely to be argued about, because it is easy to state and hard to define. Agree a physical reference: a first-article part or a set of graded coupons, viewed under a stated light source, at a stated distance and angle, by a named inspector. Record whether the accepted finish is bright, satin, directional or non-directional, and whether machining marks may remain visible. If the part will be anodised later, the finish that looks correct as bare aluminium may look different after anodising, because the coating is partly transparent and the underlying texture remains; evaluate the appearance on an anodised sample rather than bare metal. Keep reference parts labelled, protected and stored, because a visual standard that lives only in memory changes with every batch.
Send parts that represent the real production condition, not a polished bench sample. A useful set includes the worst case: the thinnest wall, the tightest sealing edge, the deepest tool mark, the casting with visible porosity, the smallest hole and the feature most likely to trap media. Include two or three pieces of each condition so one can be sectioned or inspected internally, and include an untreated part as the comparison reference. Label every part with its alloy and temper, its part number, the surfaces that are cosmetic, the surfaces that are functional, and the edge radius or chamfer allowed at each critical feature. State the current process and the defect that prompted the enquiry, plus the downstream operation such as anodising, laser marking or assembly.

It does. Anodising is partly transparent over the underlying texture, so machining marks, media direction and any residual film remain visible, and embedded media or a silicate deposit can show as a bloom or speckle. Aluminium also needs a clean, freshly finished surface, because a slow dry or a contaminated rinse leaves an oxide or residue layer that shows through the coating. A buyer planning a cosmetic anodised finish should evaluate appearance on an anodised sample rather than on bare metal, and should specify the rinse, dry and handling expectations to the finishing supplier. Acceptance of the coating itself remains with the buyer and the anodiser.
No. SurfacePolish is a cross-border supplier of finishing machines, media and compounds and runs a free sample trial on parts the buyer sends. A trial reports observations on the parts tested under the settings used; it does not qualify, approve or validate a process, and it does not create biocompatibility, cleanability, sterility or regulatory documentation. Any requirement of that kind must be defined by the buyer and verified by the buyer's own engineering and quality functions, usually with the help of specialist testing providers. For a device programme in India, treat the finishing route as one input into the buyer's own verification plan rather than as evidence for it.
Start with media that are softer or lighter than the workpiece is likely to tolerate: plastic-bonded media in a light or medium abrasive grade, or a low-density ceramic. Dense ceramic and steel media that cut steel efficiently will embed, smear or gall aluminium and can implant iron that later shows as staining. Media weight, compound lubricity and load ratio matter as much as family, because a heavy, hot, under-lubricated charge will gall parts even with the right media. A buyer in India should treat media selection as a two-stage question: what removes the burr, and what produces the final cosmetic surface without transfer.
Use Bengaluru, India as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
The national reference for material and product conformity is the Bureau of Indian Standards (BIS), whose certification scheme BIS describes as basically voluntary in nature, with compliance made compulsory for a number of products by the Central Government. Aerospace, defence and automotive customers add their own qualification and drawing specifications, and surface callouts are written to the ISO 4287/ISO 21920 family as general industry practice.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Bengaluru.
The buyer needs part-to-part consistency across a large batch and is worried about small parts escaping a screen or lodging in each other.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0923; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0923 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
