A buyer in Hamamatsu, Japan finishing a 6061-T6 instrument housing for medical devices has to hold two requirements at once: a satin face the customer will see, and an O-ring groove edge that must stay within a stated radius. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on the parts the buyer sends. This brief is written for a buyer in Hamamatsu working on medical devices; it describes equipment, media and a scoped sample review, not a local polishing service.
What edge radius or chamfer is allowed at each mating, sealing and press-fit feature, and how will it be measured?
Which surfaces on this aluminium part carry a cosmetic grade, which are functional seating or sealing faces, and which are indifferent?
What are the alloy and temper, and has machining, casting, welding or heat treatment already changed the surface hardness and porosity?
Controlled edge rounding is where a finishing route earns or loses its place. Every machined aluminium edge carries a burr and a stress concentration, and a deburring cycle removes both, but it also moves the edge position. On a mating face, a seal groove, a bearing seat or a dowel hole that movement is a functional change, not a cosmetic one. Establish the allowed edge radius or chamfer per feature, then measure the finished edge against it rather than judging by eye, using an optical comparator or a radius gauge on a sectioned or replica sample. A part with generous cosmetic edges and one tight sealing edge usually needs a shielded fixture or selective hand finishing after the machine cycle. Deciding this after the first batch has run is how an assembly ends up with a leak path.
Disc finishing machines generate high energy at the disc face and remove material and round edges quickly, which is attractive when a batch of aluminium parts needs a burr gone in a short cycle. That same energy is what makes them risky on soft wrought aluminium and on thin castings. Part-on-part contact is high, so parts impinge, peen each other and develop a hammered or uneven surface, and 6061 will smear rather than cut if the compound is wrong or the load too heavy. Fixturing helps: a carrier that holds each part in a fixed attitude reduces random contact but adds load and unload labour to every cycle. Disc routes are also unforgiving on edge control because removal is neither uniform nor easy to localise. Use them where a robust part needs a fast radius.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Tub vibrator | Long and large aluminium parts such as extruded frames and housings that can be oriented in a linear working channel | Slower uniform coverage, a tendency for parts to settle in one attitude, and greater floor space and media volume than a bowl |
| Rotary barrel finishing machine | Gentle, low-energy deburring of small precise aluminium parts in high volume, including thin and light components | Longer cycles for the same result; flat or light parts may slide rather than tumble, and an overloaded barrel stops working the load |
| Grinding finishing machine | Higher material removal on aluminium parts that need a heavy burr or a pronounced chamfer removed before a gentler finishing step | Aggressive on soft aluminium, difficult to control on cosmetic faces and functional edges, and not a finishing step on its own |
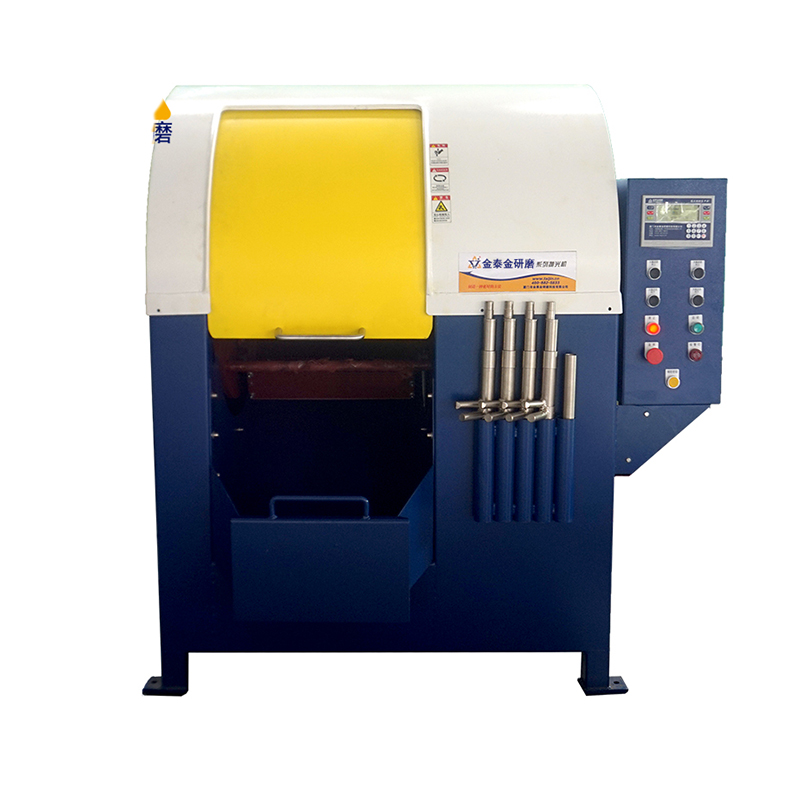
| Centrifugal barrel finishing machine | Short, controlled cycles producing a fine satin finish and a defined edge on small to medium aluminium device parts | High energy bends thin walls and distorts light sections; barrel geometry limits part length and pieces per run |
Aluminium reacts to both strong acid and strong alkali, so compound chemistry deserves more care here than on steel. A mildly alkaline or near-neutral cleaning and burnishing compound with a suitable inhibitor is the usual starting point for aluminium, because a strongly alkaline product etches the surface, darkens it and attacks exposed edges, while a strongly acidic one can pit it and leave smut. The compound also carries debris and controls foam, lubricity and rinsing, so concentration and flow rate matter as much as family. Water quality is part of the chemistry: hard water leaves mineral spotting and deposits, chloride content in the supply raises a corrosion concern on aluminium, and a recirculated system concentrates fines and dissolved metal over time. Set a working range for concentration, pH and flow, then monitor and correct it during the shift.

| Media | Best fit | Watch out for |
|---|---|---|
| Plastic-bonded media, ball and ellipsoid shapes | Surface refinement and blending on cosmetic aluminium faces where edges, seal lands and dowel bores must stay close to drawing | Removes very little edge material, so a burr at a bore exit or a thread crest may survive the cycle and need a separate step |
| Plastic-bonded media, light to medium abrasive grade, cone and triangle shapes | General deburring and satin finishing on 6061 and 7075 where galling risk rules out dense ceramic | Wears quickly and loses edge definition; cut rate drops as the charge ages and the cosmetic result drifts unless media is screened and topped up |
| Alumina-based ceramic media, low-density, cylindrical and pin shapes | Internal bores, slots and cross-holes on small aluminium components that a rounded tumbling body cannot reach | Pin and cylinder shapes can wedge in a bore or a slot; confirm retrieval and inspection before running a production batch |
| Steel media, balls or pins, for bright polishing | Bright reflective finish on hard, robust steel work where a high lustre is the primary requirement | Deposits iron on aluminium, causing black smut, staining and a galvanic couple; keep it out of any loop shared with aluminium parts |
Media cannot tell a cosmetic edge from a sealing edge, so a cycle that breaks a burr nicely on the outside of a housing can round a seal land, a dowel bore or a press-fit shoulder until it no longer functions. The drift is gradual and cumulative: each pass removes a little more material, and a batch that was within tolerance at the start of a media charge may be outside it by the end. Watch for a seal face that has lost its flat land, a bore edge closed to a radius, or a chamfer grown past the drawing. Detect it with an optical comparator or radius gauge on a cross-section, or by measuring the feature with a CMM before and after. Protection comes from shielding the functional edge, rounder and lighter media, and a first-article check.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Black smut or scattered dark specks on the finished surface | Iron transferred from steel media, a shared barrel, worn machine parts or a shared media store; galvanic reaction on the soft aluminium surface | Examine under magnification and with a light acidified wipe, and audit media storage, barrel liners and screening equipment for steel contact |
| Uneven finish with bright and dull bands on the same face | Part settling in one attitude, self-shadowing on a long or recessed part, wrong load ratio, media too large to flow around the geometry | Compare several parts taken from different positions in the load under directional light rather than sampling only the discharge gate |
| Galled, smeared or picked surface with transferred aluminium | Media too heavy or too dense for the alloy, insufficient compound lubricity, hot or overloaded charge, aluminium parts rubbing against each other | Inspect under low-angle directional light for smears and cold welds, then wipe with a white lint-free cloth to reveal transferred metal |
| Dimensional drift on a critical bore, dowel hole or press-fit diameter | Aggressive media attacking a feature the cycle should not touch, cumulative removal over repeated runs, no masking of close-tolerance geometry | Measure the feature with a CMM or bore gauge at first article and at the end of the media charge, and chart the trend against drawing limits |
Hamamatsu City's own English-language industry profile describes a manufacturing city positioned between Tokyo and Osaka whose post-war base - textiles, musical instruments and motorcycles - developed into transport equipment, precision machinery, optics and electronics. It names Suzuki and Honda as rooted in the city, Yamaha and Kawai as instrument makers, and Hamamatsu Photonics as the anchor of an optoelectronics field that extends into medical devices and precision measurement instruments, and it states that transportation equipment is a key pillar while musical instruments are a signature strength. The city publishes industrial statistics by industry category and has adopted a second Hamamatsu industrial innovation plan, designating seven growth sectors supported through industry, academia, government and finance collaboration.
For this brief the relevant part of that base is medical: The city profile states that, anchored by Hamamatsu Photonics, the city drives research and development in optoelectronics applications such as medical devices and precision measurement instruments.
Optics and photonics hardware, precision measuring instruments and instrument-grade cosmetic parts put a premium on scratch-free surfaces, controlled edge break and cleanliness before coating or assembly. Musical instrument manufacturing adds cosmetic metal finishing, while automotive and aerospace work adds burr-sensitive machined features and sealing faces where edge condition affects function and inspection.
A Hamamatsu buyer's first question is whether the part is instrument-grade (where cosmetic surface quality and scratch-free edge condition dominate) or a functional precision part (where burr removal, edge break and roughness on a mating or sealing face dominate); that distinction decides the process and the media and compound combination to be trialled on samples.
Freight context: Tokyo-Osaka national corridor (city position as described by Hamamatsu City). The city's official profile states that Hamamatsu is strategically located between Tokyo and Osaka, so freight for machine deliveries and sample parts moves along that corridor; the city has no international seaport of its own, and no Hamamatsu port-authority or cargo-terminal page could be verified in this research, so seaport routing for this city remains unconfirmed.
The national standards body is the Japanese Industrial Standards Committee (JISC), which states that JIS covers industrial and mineral products, data, services and management systems under the Industrial Standardization Act. Its technical divisions include mechanical engineering, ferrous materials and metallurgy, nonferrous materials and metallurgy, ceramics, medical equipment and safety appliances, and aircraft and aviation, which are the divisions a finishing or deburring requirement is normally read against. Product certification runs through the JIS Mark Certification Scheme, operated by accredited certification bodies compliant with ISO/IEC 17065; as of March 2019 there were 24 JIS-accredited bodies, three of them outside Japan, with about 8,700 certifications issued, and the scheme explicitly covers foreign manufacturers, processors and exporters.
Documentation and technical communication are Japanese-language in practice: JISC states that the documents submitted for JIS certification-body accreditation must be written in Japanese, and drawings, inspection sheets and purchase specifications from Japanese buyers are normally issued in Japanese. Import declarations are filed in triplicate and importers commonly use licensed customs brokers, so the commercial invoice, packing list and origin documents must be complete and consistent with the declared commodity code. As general industry practice in Japan, industrial buyers qualify a supplier on documentation, quality-management evidence and a defined inspection standard before volume orders, and expect a named Japanese-speaking contact for technical and commercial follow-up.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Residue requirements on a device component come from the buyer's own specification, not from a finishing route, and they should be stated as a measurable limit before parts are accepted. Practical checks include visual inspection of internal features under magnification or with a borescope, a wipe test with a defined solvent and a white substrate, a gravimetric non-volatile residue determination on a rinse sample, and a rinse-water conductivity or particulate count where the assembly is sensitive. Blind holes, threads and press fits are the features that retain residue, so sample them specifically rather than only a flat exterior face. If a validated cleaning process, biocompatibility data or a sterility claim is needed, that work belongs to the buyer's own quality system.
A sample trial is most useful when it isolates one change. If media family, size, compound and cycle time all change together, a difference in the result cannot be attributed to anything and the trial cannot be repeated. Ask for a small matrix: the same parts run with two media families at the same cycle, or the same media at two cycle times, with every other condition held constant and a record of the settings used for each cell. Photograph or measure each result on the same features under the same lighting, and keep an untreated reference beside them. Reproducibility deserves attention too: one good part proves little, so ask whether the result repeated on the other pieces in the charge. A trial yields observations on the parts tested, not a guaranteed production result.

It will if the edge is exposed to the media for long enough. Media cannot distinguish a cosmetic edge from a seal land, a dowel bore or a press-fit shoulder, and rounding accumulates gradually, so a batch inside tolerance at the start of a media charge can be outside it later. Protection comes from shielding or masking the functional edge, using rounder and lighter media, shortening the cycle, and checking the feature with an optical comparator, radius gauge or CMM rather than by eye. A buyer in Japan should state the allowed edge radius per feature on the drawing, because a blanket edge-break note will be read literally.
It does. Anodising is partly transparent over the underlying texture, so machining marks, media direction and any residual film remain visible, and embedded media or a silicate deposit can show as a bloom or speckle. Aluminium also needs a clean, freshly finished surface, because a slow dry or a contaminated rinse leaves an oxide or residue layer that shows through the coating. A buyer planning a cosmetic anodised finish should evaluate appearance on an anodised sample rather than on bare metal, and should specify the rinse, dry and handling expectations to the finishing supplier. Acceptance of the coating itself remains with the buyer and the anodiser.
Laser marking interacts with surface texture, so contrast depends on whether the surface is directional, random satin or bright. A strong directional finish from a tub or a linishing step can produce a marking that reads differently when the part is turned, while a uniform random texture marks more consistently. Residue and embedded media also interfere, because the marking energy meets a contaminated surface. For a marked cover plate in Japan, the practical sequence is to fix the finish first, then qualify the marking programme on finished parts, and to check the mark under the lighting the end user will use rather than a bench lamp.
Use Hamamatsu, Japan as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Japanese buyers work to JIS (Japanese Industrial Standards), enacted and revised under the Industrial Standardization Act after the law was renamed from the Industrial Standardization Act (工業標準化法) to the Industrial Standardization Act (産業標準化法) in 2019; JIS content is administered through the Japanese Industrial Standards Committee (JISC). Drawings normally reference JIS or customer specifications for surface finish, and ISO 9001 management-system certification is commonly requested as general industry practice.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Hamamatsu.
The buyer needs a uniform satin cosmetic face without rounding the O-ring groove edge or driving media into the threaded bosses.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0893; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0893 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
