Long thin-wall aluminium frames for medical devices will not circulate freely in a round bowl, so one face usually comes out duller than the rest. A buyer in Toulouse, France weighing a tub vibrator against a fixtured route can send parts to SurfacePolish, a cross-border supplier of finishing machines, media and compounds, for a free sample trial. This brief is written for a buyer in Toulouse working on medical devices; it describes equipment, media and a scoped sample review, not a local polishing service.
What is the minimum wall thickness and unsupported span, and which internal features could trap media?
What downstream operation follows finishing, such as anodising, laser marking, bonding or assembly, and what does it require of the surface?
What are the alloy and temper, and has machining, casting, welding or heat treatment already changed the surface hardness and porosity?
Controlled edge rounding is where a finishing route earns or loses its place. Every machined aluminium edge carries a burr and a stress concentration, and a deburring cycle removes both, but it also moves the edge position. On a mating face, a seal groove, a bearing seat or a dowel hole that movement is a functional change, not a cosmetic one. Establish the allowed edge radius or chamfer per feature, then measure the finished edge against it rather than judging by eye, using an optical comparator or a radius gauge on a sectioned or replica sample. A part with generous cosmetic edges and one tight sealing edge usually needs a shielded fixture or selective hand finishing after the machine cycle. Deciding this after the first batch has run is how an assembly ends up with a leak path.
Magnetic finishing works on small aluminium parts with fine internal features, using a magnetic field to drive small pins or abrasive media through holes, slots and recesses that a tumbling load cannot reach. It is useful on small fittings, valve spools, connector components and parts with internal cross-holes, and it can be gentle enough for thin sections if field strength and cycle are controlled. Its limits are size and throughput: the working envelope is small and the process suits a narrow part family rather than a mixed batch, and fine media or pins lodge in blind features just as tumbling media do, so retrieval and inspection matter. Dry polishing machines and dryers handle the post-wet step, removing water from blind holes before anodising or laser marking, where a trapped droplet becomes a stain or a marking defect.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Magnetic finishing machine | Small aluminium parts with fine internal features such as cross-holes, slots and recesses that tumbling media cannot reach | Small working envelope and low throughput; pins and fine media can lodge in blind features, and mixed part families are awkward |
| Grinding finishing machine | Higher material removal on aluminium parts that need a heavy burr or a pronounced chamfer removed before a gentler finishing step | Aggressive on soft aluminium, difficult to control on cosmetic faces and functional edges, and not a finishing step on its own |
| Disc finishing machine | Fast burr removal and edge radiusing on robust aluminium parts where a short cycle and high material removal matter most | High part-on-part contact and impingement risk; smears soft 6061, is hard to localise, and adds fixturing labour to every cycle |
| Tub vibrator | Long and large aluminium parts such as extruded frames and housings that can be oriented in a linear working channel | Slower uniform coverage, a tendency for parts to settle in one attitude, and greater floor space and media volume than a bowl |
After a wet cycle an aluminium part carries compound residue, suspended fines, media dust and water. Some of it sits in a blind hole, under a flange or in a thread and is not removed by a plain rinse. A dried residue film or a silicate deposit can interfere with later operations: it can show as a bloom under anodising, uneven laser marking, a poor bond or a stained appearance after assembly. Define what the downstream operation needs and state it, because the buyer owns that requirement; the realistic levers are rinse stages, water quality, a controlled dry, and verification by the buyer on the parts they receive. Nothing about equipment supply or a sample trial establishes biocompatibility, sterility or a validated cleaning process, and residue limits for a device must be set and verified by the buyer against their own specification.

| Media | Best fit | Watch out for |
|---|---|---|
| Plastic-bonded media, ball and ellipsoid shapes | Surface refinement and blending on cosmetic aluminium faces where edges, seal lands and dowel bores must stay close to drawing | Removes very little edge material, so a burr at a bore exit or a thread crest may survive the cycle and need a separate step |
| Ceramic media, angle-cut triangles, medium size class | Heavy-cut deburring on cast or robust aluminium parts where the machined surface will be finished again or is not appearance graded | Rounds functional edges quickly and can chip or peen thin walls; not suitable where a sealing land or press fit is exposed |
| Dry media, walnut shell, fine grade | Dry polishing, light surface cleaning and preparation before anodising or laser marking on aluminium parts | Shell dust must be extracted and the part cleaned, or the residue interferes with marking, bonding or a later coating step |
| Plastic-bonded media, light to medium abrasive grade, cone and triangle shapes | General deburring and satin finishing on 6061 and 7075 where galling risk rules out dense ceramic | Wears quickly and loses edge definition; cut rate drops as the charge ages and the cosmetic result drifts unless media is screened and topped up |
Small media, abrasive grit and magnetic pins can lodge in a blind hole, a cross-drilling, a thread root, an undercut or a thin-wall pocket and stay there through rinsing. A lodged fragment is a functional defect, not a cosmetic one: it can score a mating bore during assembly, come loose inside a device, or sit under a coating. Thin walls make it worse because the pocket deforms slightly under load and grips the fragment. Detect it with a borescope on internal features, by weighing parts against a known-clean reference, by controlled tapping over a white surface, or by an ultrasonic clean followed by inspection of the bath residue. Design the route around it: plug or shield the features that trap media, change the size class, or choose a route whose loading geometry differs. A visual pass is not proof that a cavity is clean.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Water spotting, rings or mineral staining after drying | Hard rinse water, slow or incomplete dry, droplets trapped in blind holes or under a flange, no final deionised rinse | Inspect the dried part in raking light against a reference, and check rinse-water hardness and conductivity records for the shift |
| Finish bloom or speckle, or poor laser mark contrast, revealed after anodising or marking | Embedded media, a silicate or residue film, a directional texture that marks unevenly, or an oxide layer from a slow dry | Evaluate the appearance on a coated or marked sample rather than bare metal, and compare marking contrast on parts from different positions in the load |
| Dimensional drift on a critical bore, dowel hole or press-fit diameter | Aggressive media attacking a feature the cycle should not touch, cumulative removal over repeated runs, no masking of close-tolerance geometry | Measure the feature with a CMM or bore gauge at first article and at the end of the media charge, and chart the trend against drawing limits |
| Uneven finish with bright and dull bands on the same face | Part settling in one attitude, self-shadowing on a long or recessed part, wrong load ratio, media too large to flow around the geometry | Compare several parts taken from different positions in the load under directional light rather than sampling only the discharge gate |
Toulouse is the centre of the European aerospace industry: Aerospace Valley describes itself as the leading European aerospace competitiveness cluster, serving three sectors across the Occitanie/Pyrenees-Mediterranee and Nouvelle-Aquitaine regions, and it runs its aeronautics, space and drones programmes and its annual InnoDay innovation event in Toulouse. INSEE counted 19 612 establishments in the commune at the end of 2024 with a 4,1 % industry share, the highest of the large French cities sampled here, and 358 827 jobs at the place of work in 2023. Around the aircraft and space primes sits a deep supplier base of machining, sheet-metal, composites, surface-treatment and assembly shops, plus electronics and equipment manufacturing; the city's second historical industrial pillar is agri-food and agricultural equipment for the surrounding Midi-Pyrenees farming economy.
For this brief the relevant part of that base is medical: Toulouse-Blagnac airport presents more than 70 destinations in direct flight, the route used for urgent tooling, media and sample parts.
Aerospace parts made in and around Toulouse are surface-critical: deburring and edge radiusing on machined brackets, engine and landing-gear components, burr-free fluid lines, and controlled surface texture on sealing and bearing faces. Fatigue life and fatigue scatter are directly sensitive to edge condition and residual surface damage, so the burr and edge specification is usually an engineering requirement rather than a shop-floor preference. Because the primes audit the tier, the finishing operation normally has to be qualified and documented per part number, which puts the process window and media control under scrutiny.
A Toulouse buyer should settle how the edge and surface requirement is expressed - a drawing callout, a fatigue-driven internal rule, or a visual workmanship standard - because only a numerically defined requirement can be validated on sample parts and then held in series production.
Freight context: Toulouse-Blagnac Airport, Grand Port Maritime de Bordeaux / Bassens for sea freight, Toulouse rail-road combined terminals. Toulouse has no seaport; the official airport site presents Toulouse-Blagnac with more than 70 destinations in direct flight, which is the normal route for urgent tooling, media and sample parts, while machines and heavy equipment come in by road or rail from Atlantic or Mediterranean ports. Aerospace suppliers here routinely send sample parts by express air and schedule machine deliveries around production shutdowns.
France applies the EU common commercial policy, so industrial machinery arriving from China enters under the Union Customs Code and the Common Customs Tariff rather than under any bilateral French regime; the EU has no free-trade agreement with China, so no preferential duty rate applies and normal third-country duties are due on the customs value. Importers classify the machine in the tariff nomenclature and lodge a customs declaration; French Customs publishes the common and national tariff through its RITA online service and states that three notions are fundamental: the tariff classification of the product, its origin or destination, and the value of the goods.
The working language of French industrial procurement is French: tenders, drawings, inspection plans and technical dossiers are normally issued and answered in French, and quotations that omit French documentation slow down qualification. Buyers qualify a machine against a written specification and expect traceable material certificates, machine safety documentation and, where applicable, a CE declaration of conformity and a risk assessment; acceptance is often staged (documentary review, factory acceptance test, then commissioning). Payment and documentation norms are conventional EU practice: euro invoicing, SEPA or SWIFT bank transfer, Incoterms agreed in writing, and customs paperwork (commercial invoice, packing list, transport document, proof of origin where a preference is claimed) prepared for the declarant or customs representative. Because customs and tax authorisations are handled jointly through SOPRANO, non-EU sellers are normally advised to sell to an established French/EU importing entity rather than to act as importer of record themselves.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Treat the first finished part of every batch as a first article and hold it until it has been checked against the agreed criteria. Record the part number, alloy and temper, the machine and route, the media charge identity and its accumulated hours, the compound and concentration, the cycle time, the load ratio and the drying step. Retain a reference part from the accepted first article, and when a later batch differs, compare the two physically before adjusting anything. Segregate batches by alloy and part number, and keep the aluminium loop separate from steel work so iron cannot transfer onto a soft surface. This discipline, not the machine settings, is what makes a finish reproducible. Who performs the checks and who signs the release is a buyer decision, but the record of what was run is worth keeping.
Scaling from a bench or pilot run to a producing line changes several things at once, and each has to be planned. The machine must be sized for the part envelope and the throughput the buyer needs, which sets load volume, media quantity and compound dosing. A compound delivery system with a dosing pump, a flow meter and a recirculation or once-through decision is what makes the chemistry repeatable rather than hand-mixed. Media handling needs a screen or separator, a stock of graded media for top-up, and a rule for replacing worn media. Parts need a defined load pattern, and any fixture or mask needs a duplicate so it does not become the bottleneck. Rinse and drying stages must match the downstream requirement. The layout, services and acceptance criteria remain the buyer's engineering decisions.
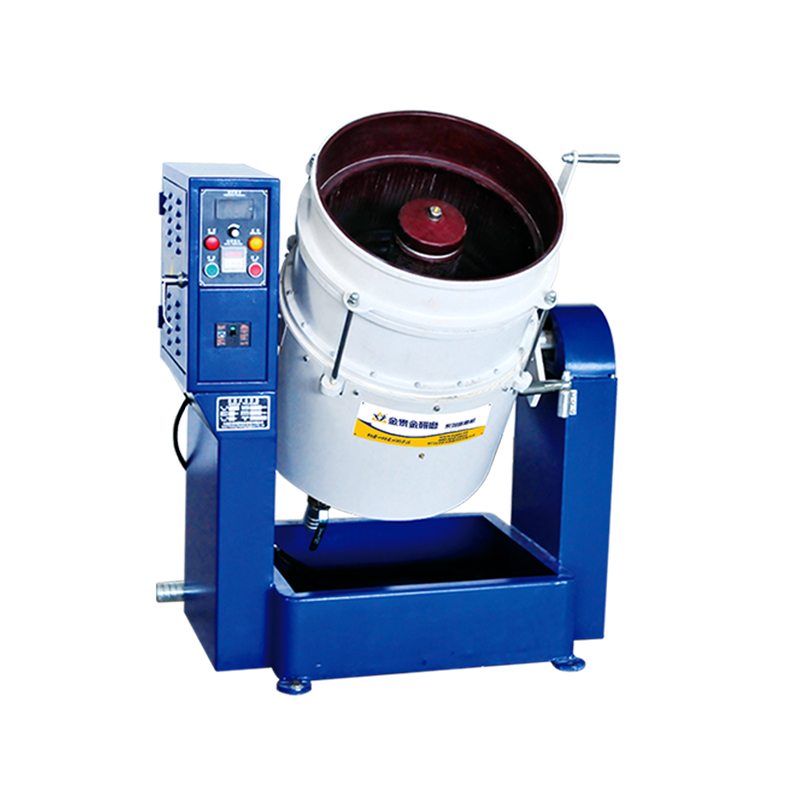

A bowl vibrator circulates a load through a media field at moderate energy, with good uniformity on small parts that tumble freely and easy discharge. A centrifugal barrel presses media and parts together at high force in a much shorter cycle, producing a fine finish and controlled edge quickly, but bending thin walls, distorting light sections and rounding edges faster. Bowl routes suit mixed small parts and gentle work; centrifugal routes suit a narrow part family that fits the barrel and accepts the energy. Parts made in France should be trialled in the specific geometry before a machine size is fixed, because barrel dimensions limit part length and load size.
No. A trial shows what happened on the parts tested, with the media, compound and cycle used at that time. It does not guarantee a roughness value, appearance grade, edge radius, dimensional result, cycle time, capacity or cost in production, and it cannot cover the drift that comes from media wear, compound carry-over, water changes or a different machine. What it can do is indicate whether a mechanical route is plausible, which media and compound direction deserves a closer look, and which features need protection. A buyer in France should plan a first-article routine and retain a reference part before releasing a production batch.
It will if the edge is exposed to the media for long enough. Media cannot distinguish a cosmetic edge from a seal land, a dowel bore or a press-fit shoulder, and rounding accumulates gradually, so a batch inside tolerance at the start of a media charge can be outside it later. Protection comes from shielding or masking the functional edge, using rounder and lighter media, shortening the cycle, and checking the feature with an optical comparator, radius gauge or CMM rather than by eye. A buyer in France should state the allowed edge radius per feature on the drawing, because a blanket edge-break note will be read literally.
Use Toulouse, France as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Toulouse aerospace buyer qualifies finishing suppliers against EN 9100 and the specific prime requirements that sit under it, and specifies surface texture with ISO/NF EN surface-texture standards plus programme cleanliness and edge-condition requirements (NADCAP-style special-process approval is commonly the gate for surface treatment and finishing). Where the supplier also serves the automotive or general machinery chain, IATF 16949 or ISO 9001 applies.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Toulouse.
The buyer cannot keep the long frame from shadowing in a bowl route and needs to know whether a tub or a fixture is the realistic answer.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0523; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0523 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
