A automotive parts buyer in Canberra, Australia has a hardened stainless exhaust valve that must be deburred at the seat margin without rounding the seat edge or disturbing a nitrided stem. SurfacePolish supplies finishing machines and consumables across borders and runs a free sample trial in Xiamen, returning the tested parts with observations and a proposed media, compound and cycle direction for the buyer's own engineering review. This brief is written for a buyer in Canberra working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which surfaces on this part carry a visible appearance grade, which are hidden, and which edges have a functional requirement rather than a cosmetic one?
At what batch size, load fill ratio and media wear state does a trial observation still describe what series production will produce?
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
Stainless automotive parts usually carry two requirements that pull against each other: an appearance grade on surfaces the customer sees, and an edge or function requirement on features that must keep working. Map the part into exterior visible surfaces, hidden surfaces, and edges with a functional role such as sealing, bearing, fatigue resistance or assembly clearance. An edge that only needs a burr broken can take an energetic cycle; a bore edge that sets a seal or a press fit cannot. Ask which faces are graded after assembly, because a bright panel that meets a specification by itself may look mismatched against the mating panel next to it. A marked-up drawing that states, per surface, whether it is graded, functional or indifferent is the cheapest document in the whole finishing project.
Geometry, not preference, sets media shape and size. Angle-cut triangles and similar forms reach slots, corners and recesses and cut faster on burrs; cylinders and balls blend broad surfaces more evenly and are kinder to edges; small media reaches tighter features but carries more edge impact per contact and is harder to separate. The usable window for any feature lies between media that is too small and packs or lodges and media that is too large to enter at all. For cross-drillings, gear teeth and narrow slots, work from the smallest opening on the drawing and pick a size class that flows through it without wedging. For stainless appearance parts, check the surface texture the shape leaves behind, because some forms produce overlapping impacts that read as a texture rather than as a polish.

| Media | Best fit | Watch out for |
|---|---|---|
| Steel media, including balls and shaped steel forms | Brightening and burnishing of austenitic stainless appearance parts where the highest available gloss is the objective. | Deforms and generates metallic fines, adds weight to the load, and can transfer iron if used in a line shared with carbon steel work. |
| Ceramic cylinders, balls and other rounded shapes | General surface refinement and blending on broad stainless faces where a more even texture and gentler edge action are wanted. | Does not reach sharp internal corners, and long enough running on thin sections can still round edges beyond a tight callout. |
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
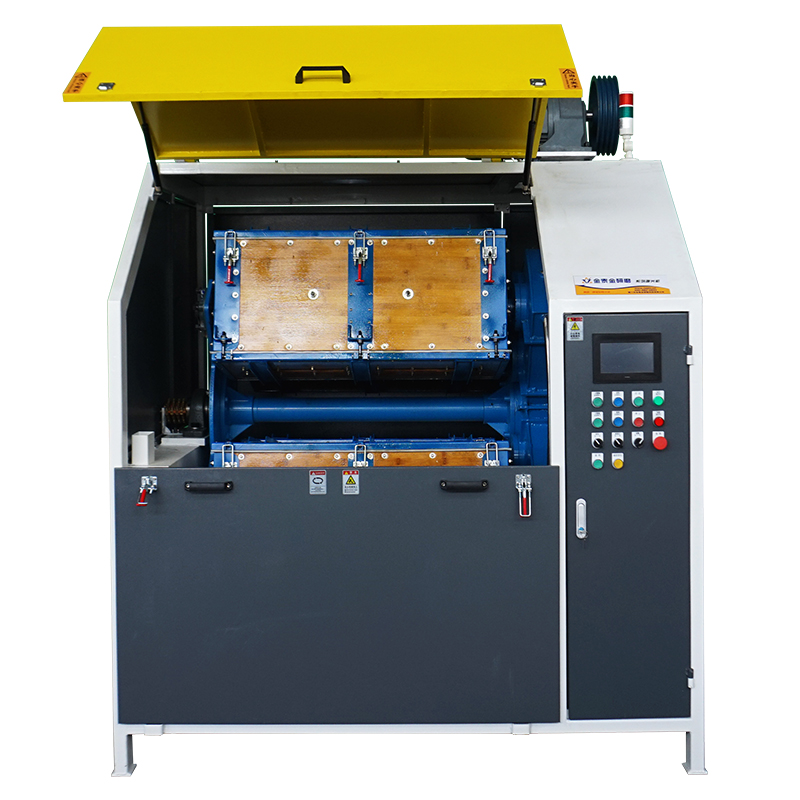
Disc finishing machines run a shallow, fast-moving charge that deburrs heavier machined stainless parts quickly: valve bodies, fittings, machined brackets and parts whose edges can lose material. The energy is an advantage for cycle time and a liability for thin walls and delicate features, so tooling and compartments often decide whether the route is acceptable at all. Centrifugal barrel finishing uses a planetary barrel motion that produces very high energy in short cycles, useful for aggressive edge radiusing on small, hard parts. The same energy rounds edges quickly, can exceed a tight radius callout within a short run, has part size and shape limits, and needs a larger load to justify the cycle. Treat both routes as candidates for heavy deburring and blending, and verify edge results on the actual part rather than assuming a shorter cycle means a safer one.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Dry polishing machine with heated dryer | Post-wet drying, residue control and light dry finishing of stainless parts that must leave the line dry and free of moisture in blind features. | Dry media does not cut stainless, and moisture trapped in a blind hole, hem or tight joint can cause staining if drying is not effective. |
| Magnetic finishing machine | Small precise stainless parts with internal features, slots and blind holes that must be deburred without media lodging in the passages. | Works within a small part envelope, and the route has to be tested per grade because it depends on the part's magnetic response. |
| Centrifugal barrel finishing machine | Very high energy deburring and edge radiusing of small, hard stainless parts in short cycles. | Rounds edges quickly and can exceed a tight radius within a short run; part size and shape are restricted and a substantial load is needed to justify the cycle. |
| Tub vibrator | Long stainless parts such as trim sections, exhaust profiles and shafts that cannot be loaded into a bowl without being cut down. | Media velocity varies along the length, so finish evenness must be verified at both ends, and the machine occupies more floor space and compound volume. |
Cross-drillings, tapped holes, folded hems and closed volumes are lodging sites, and a lodged medium is worse than a visible defect because it can travel to the customer, escape during cleaning, or damage a mating surface in service. Detection needs a defined routine rather than a shake and a look: weigh the part where that is sensitive enough, inspect internal passages with a borescope at agreed angles, confirm each passage with a pin or plug gage, and record the media count into and out of the batch. Weighing alone catches only gross lodges, since a retained chip may be a fraction of a gram. Where a feature cannot be inspected reliably after processing, the better answer is to plug or mask it before the cycle rather than to add inspection afterwards. Any media found downstream is a signal to redesign the separation step, not to add more inspection.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Heat tint, oxide or weld discolouration remaining after a light cycle | Incoming oxide from welding or laser cutting deeper than the finishing stage is designed to remove, or a finishing sequence that only brightens the surrounding surface. | Record the incoming oxide condition with photographs at agreed locations, then compare the same locations after processing and confirm whether removal of the oxide was inside the agreed scope. |
| Media lodged in cross-drillings, tapped holes, hems or closed volumes | Media size class small enough to enter a passage but not guaranteed to exit, or a separation step that relies on gravity alone. | Weigh the part where sensitivity allows, inspect passages with a borescope at agreed angles, pass pin or plug gages through each passage, and reconcile media counted into and out of the batch. |
| Edge rounding beyond the specified radius on a functional edge | Cycle energy, time or media size class chosen for appearance rather than for the tightest edge callout on the drawing. | Measure edge radius at marked locations with an optical comparator or a cast impression before and after, and record the result against a written allowable band rather than judging it visually. |
| Hazing or waviness on a part specified as mirror or bright | An intermediate refining stage skipped or cut short, media too coarse for the final texture, or a media charge that has worn out of its working size range. | View under defined lighting against a physical master at the acceptable and marginal limits, measure roughness across the lay with a fixed instrument setup, and screen the media charge for size and condition. |
Canberra's industrial base is unusual for Australia: it is built around the Australian Government as the country's largest single buyer of goods and services, plus national research institutions rather than heavy manufacturing. The ACT Government's business and investment site describes a 'future-focused knowledge economy' with defence, space, cyber and quantum, agri-technology and renewable energy as its named key sectors. Local manufacturing does exist and is concentrated in high-value, low-volume work: Skykraft designs and manufactures mini-satellites in Canberra, the Canberra Deep Space Communication Complex is managed for NASA by CSIRO, and the Advanced Instrumentation and Technology Centre at Mount Stromlo provides space test and verification facilities. The Australian National University, the University of Canberra, CSIRO and Geoscience Australia maintain major laboratories and instrument-building capability in the city, and Geoscience Australia operates a purpose-built Canberra headquarters. Canberra Airport's precincts at Brindabella Business Park, Majura Park and Fairbairn, adjoining the RAAF base, concentrate aviation, defence and light industrial tenancies.
The nearest part of that base to this brief is semiconductor: Canberra concentrates national instrument-building and precision fabrication capability through ANU, the University of Canberra, CSIRO and Geoscience Australia, and the ACT Government promotes the ACT as a testing ground and incubator for new technologies; no ACT-specific semiconductor fabrication plant could be verified, so this is recorded as precision instrument and sensor fabrication capability rather than wafer fabrication.
Canberra's manufacturing is precision, low-volume work — satellite structures, space instrument payloads, scientific apparatus and defence electronics — where burr removal, edge break and surface cleanliness affect optical alignment, vacuum compatibility and electrical contact rather than cosmetic appearance. For parts machined from aluminium, stainless and titanium in small batches, the choice between vibratory, barrel and disc finishing methods is driven by part geometry and allowable edge radius, and deburring must not alter critical dimensions or introduce media carry-over into clean assemblies. Buyers in this city typically need a documented, repeatable process for a small number of high-value parts rather than high-throughput finishing.
Before selecting finishing equipment or media, an ACT buyer working on space, defence or scientific hardware should settle whether the required surface condition is specified as a measurable edge radius or surface roughness value, or only as a visual 'deburred' requirement, and whether the process must avoid media embedding and cross-contamination because the part goes into an optical, vacuum or clean assembly.
Freight context: Canberra Airport (terminal, Brindabella Business Park, Majura Park, Fairbairn precinct, adjoining Fairbairn RAAF base), South Jerrabomberra Regional Job Precinct (NSW, 20-minute drive from Queanbeyan, serving the ACT workforce), Port of Eden (NSW south coast deep-water port, regional gateway). Canberra Airport is the city's international gateway and its business precincts handle the light-industrial and aviation tenancies; the airport's own site describes it as having 'thriving business precincts and daily international flights'. Canberra is an inland city with no seaport, so sea freight for machines or sample parts arrives through Port Botany, Port Kembla or the Port of Eden and moves by road, while the South Jerrabomberra Regional Job Precinct gives businesses in the corridor direct access to the ACT workforce and to Commonwealth agencies.
Australia and China are parties to the China-Australia Free Trade Agreement (ChAFTA), signed on 17 June 2015 and in force since 20 December 2015; the Australian Border Force maintains a dedicated ChAFTA page and working tariff schedule, and FTAs give importers a route to preferential rates of duty where the rules of origin are met. China was Australia's largest source of imports in 2025 at $130.2b, up 12.5% on 2024, and 56% (69,567) of Australian business importers traded at least once with China in 2020-21. A Chinese supplier of finishing machines, media or compounds is therefore shipping into Australia's single largest import stream, and preferential duty depends on origin documentation rather than on a blanket zero-tariff guarantee for every product line.
The Australian Border Force (ABF) is the customs authority and clears imported goods through customs; all goods arriving in Australia must be declared unless an exception applies, goods valued at up to A$1,000 can be imported without a formal import declaration, and entry is made through the Integrated Cargo System (Form B650 for sea or air cargo). Generally all goods imported into Australia are liable for duties and taxes unless an exemption or concession applies, and most imports are subject to 10% GST, so classification, customs valuation and any preferential tariff claim drive the landed cost; a licensed customs broker is the normal route for a first-time importer. Electrical equipment can fall under the Electrical Equipment Safety System, under which the first Australian supplier registers as a Responsible Supplier, holds an ABN, makes a Responsible Supplier Declaration and marks the equipment with the Regulatory Compliance Mark (RCM) in accordance with AS/NZS 4417.1 and AS/NZS 4417.2. Imported goods may also require a trade description naming the country of manufacture, and machinery that is not in-scope electrical equipment still has to meet state work health and safety duties covering plant.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Appearance grading on stainless is best served by physical masters: one part at the acceptable limit and one at the marginal limit, viewed under the same lighting, at the same distance and at the same angle as production inspection. Lighting is the dominant variable in appearance judgment, so a master viewed beside a window in the morning will not agree with parts viewed under a machine light at night. Record the viewing conditions with the master, keep the master protected and dated, and photograph it as a supplement rather than as a replacement. For satin and brushed finishes, the master should also fix the direction and uniformity of the texture, since a part can meet a roughness figure and still look wrong beside a mating panel. Keep a small library of masters for the finishes this process actually produces, because a single nominal sample cannot cover a batch.
A trial answers questions only if the parts represent the real range of variation. Send the difficult members of the family rather than an ideal sample: the thinnest wall, the tightest internal feature, the part with the worst incoming burr, the most visible face, and at least two parts that represent normal production condition. Include one part that was rejected for a finishing-related reason, so the trial addresses a defect that actually occurs. With the parts, send the drawing revision, the material grade and condition, the operations that created the current surface, the specified finish requirement, and any feature that must not be touched. A trial run on a single pristine sample tends to produce a pleasant result that says nothing about the batch the buyer will actually process.

Hydrogen uptake is a documented concern for high-strength martensitic stainless steels when acid chemistry and mechanical work are combined, and it is not visible on the surface. The practical route is to state the material and hardness in the enquiry, ask which compound families are proposed and at what concentration, and confirm with your own engineering function whether any post-finishing treatment is required and within what window. SurfacePolish can describe the compound family and the process conditions used on a trial, but fitness for a given strength level, and any treatment specification that follows, must be defined and verified by the buyer.
Steel media generally produces the brightest result on austenitic stainless, but brightness depends on the whole progression rather than one medium. A common sequence is a hard ceramic stage that removes burrs and machine marks, a finer stage that refines the texture, then a low-amplitude stage that brightens. Media that is too soft for the work-hardened surface burnishes and dulls instead of cutting. The shape and size class also matter, because small media reaches tight features but leaves a different texture from larger forms. Treat any proposed progression as a comparison to test on real parts with your own measurement setup.
Start from the drawing. Size the media class against the smallest opening so it flows rather than wedges, and where a passage cannot be inspected reliably, plug or mask it before the cycle instead of adding inspection afterwards. Build a retrieval routine with media counts into and out of the batch, borescope checks at agreed angles, and pin or plug gages on each passage. Weigh parts where the tolerance for retained chips is tight. For a Australia buyer planning a trial, send the part with the tightest passage so the media class is selected against real geometry. SurfacePolish reports what the trial found; your own cleanliness inspection remains the acceptance decision.
Use Canberra, Australia as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Canberra buyers are typically Commonwealth agencies or their suppliers, so work is frequently procured against Australian Standards and, for defence and space work, against the relevant Defence specifications and mission-assurance requirements rather than a purely commercial finish specification. Standards Australia is the national standards body, and AS/NZS 4417.1 and AS/NZS 4417.2 govern use of the Regulatory Compliance Mark for electrical equipment — relevant if a finishing machine is electrically powered.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Canberra.
The buyer needs the stem and seat margins deburred and blended without rounding the seat edge or disturbing the nitrided layer.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0752; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0752 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
