A automotive parts buyer in Kobe, Japan has a hardened stainless exhaust valve that must be deburred at the seat margin without rounding the seat edge or disturbing a nitrided stem. SurfacePolish supplies finishing machines and consumables across borders and runs a free sample trial in Xiamen, returning the tested parts with observations and a proposed media, compound and cycle direction for the buyer's own engineering review. This brief is written for a buyer in Kobe working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which dimensions, seal faces and thread forms carry functional geometry, and what limit on stock removal per cycle can those features tolerate?
Which internal features must be deburred without lodging media, and what retrieval and verification step proves the passage and thread form are clean?
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
What arrives at finishing often predicts the route better than the drawing does. Burrs sit at cross-drilling intersections, sheared edges and machined contours, heat tint comes from welding and laser cutting, and stamping flash, grinding marks, existing polished bands and handling scratches all behave differently under the same medium and compound. Baseline the incoming surface with roughness readings and consistent-lighting photographs at agreed locations, plus a written note on where the largest burrs sit. Cleanliness before processing also matters, because cutting fluid, marking ink, adhesive residue and shop dust load the medium and confound comparison. Batch size and mix enter here too: a load of thirty small brackets behaves differently from four large housings, and mixing families of different weight in one chamber risks damage to the lighter parts and cross-contamination between grades.
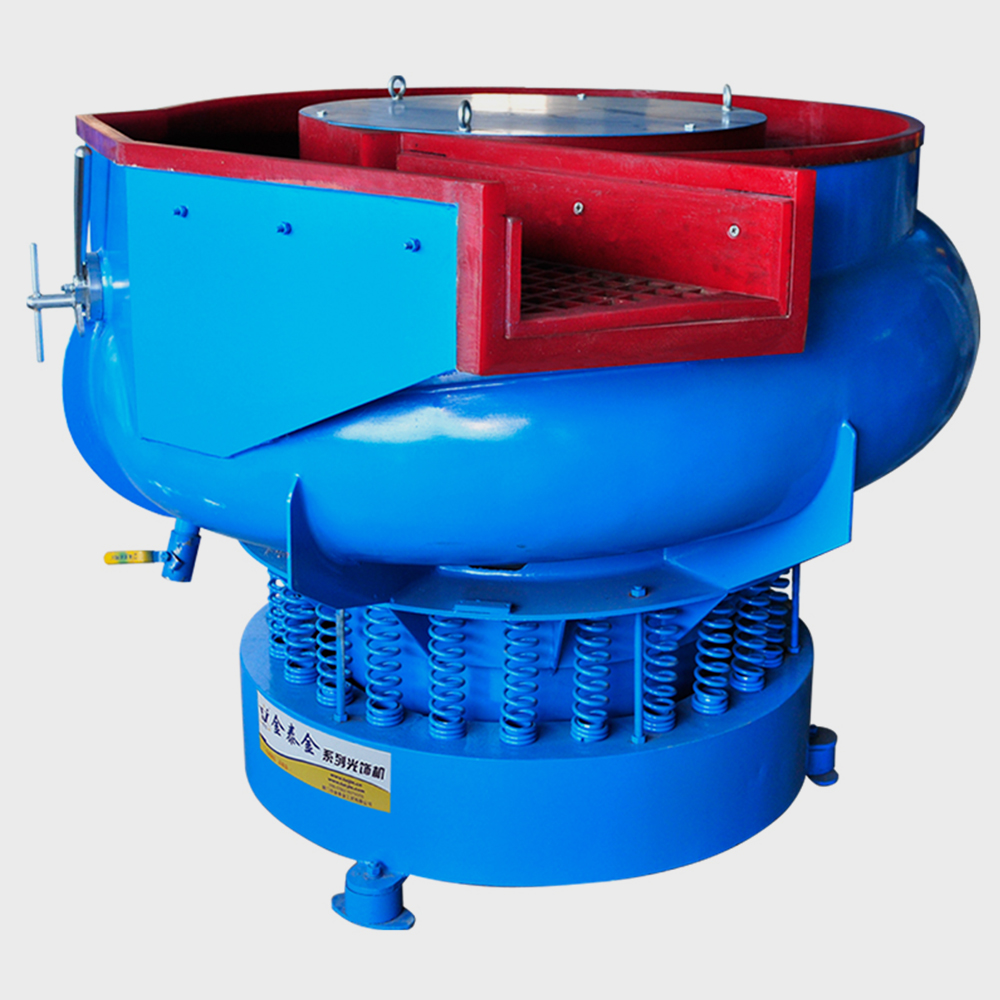
A vibratory bowl handles a broad middle band of stainless automotive parts: brackets, housings, flange blanks, handles, trim sections and small fittings. The load stays visible, amplitude, frequency and media blend can be adjusted, and the same machine serves both deburring and surface refinement when the media progression is planned. Limits are real, though. Part size and shape are capped by chamber geometry, and long or slender parts bridge and stall unless a tub or a fixture is used. Thin and threaded parts need compartments or fixtures to limit part-on-part contact. Watch fill ratio and the ratio of media to parts, because an over-filled or under-filled chamber changes both edge results and finish consistency, and keep the fill ratio stable from trial to production rather than filling to whatever the shift finds convenient.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Continuous or indexed wet line with staged media charges | Multi-stage stainless finishing where deburring, refining and brightening are separated to control edge loss and texture progression. | Needs clear segregation between stages to prevent carry-over of coarse media or iron contamination, and adds handling and floor space. |
| Disc finishing machine | Fast deburring and blending of heavier machined stainless parts whose edges can accept a higher removal rate. | The higher energy can damage thin walls and delicate features, so tooling or compartments are often needed to protect them. |
| Tub vibrator | Long stainless parts such as trim sections, exhaust profiles and shafts that cannot be loaded into a bowl without being cut down. | Media velocity varies along the length, so finish evenness must be verified at both ends, and the machine occupies more floor space and compound volume. |
| Magnetic finishing machine | Small precise stainless parts with internal features, slots and blind holes that must be deburred without media lodging in the passages. | Works within a small part envelope, and the route has to be tested per grade because it depends on the part's magnetic response. |
Media is a consumable that changes during use, and stainless finishing is sensitive to that drift. Ceramic media loses size and edge sharpness, its cutting rate falls, and the charge accumulates broken pieces and fines; steel media deforms and generates metallic fines; plastic media can load with metal particles; compound residue and swarf build up in the mass. The practical consequence is that a cycle tuned on fresh media behaves differently after days of running, which is why results can drift without any setting having been touched. Track wear by screening a sample of the charge at intervals, logging media make-up quantities and cycle hours, and replacing on measured condition rather than on a fixed calendar. Keeping the charge inside a known working window, and re-verifying the finish after any full charge replacement, is what makes a production result repeatable.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media, walnut shell and corn cob | Post-wet drying, light residue and scale removal, and dry polishing of surfaces that must not be re-wetted. | Does not cut stainless, generates dust, and leaves organic residue on parts if the medium is not kept clean and dry. |
| Porcelain and fine high-density ceramic media | Pre-polish refining stages on austenitic stainless appearance parts before a brightening stage, where a finer texture is the objective. | Limited cutting power on hard or work-hardened surfaces, and wear changes the charge gradually, so finish can drift between batches. |
| Steel media, including balls and shaped steel forms | Brightening and burnishing of austenitic stainless appearance parts where the highest available gloss is the objective. | Deforms and generates metallic fines, adds weight to the load, and can transfer iron if used in a line shared with carbon steel work. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
Two failure modes produce a damaged edge and are often confused. Impingement, sometimes called a gouge or a nick, is local damage from part-on-part contact or media striking a feature at excessive energy, and it typically appears on thin stamped covers, large flat panels and unsupported webs. Its signature is randomness: the defect site moves from part to part and does not follow the geometry of the edge. Over-rounding is systematic, follows the edge itself, and repeats at the same location on every part in the load. Both are found with raking-light photographs, magnification on the suspect feature and comparison across several parts from the same batch. The remedy differs too, because impingement is addressed by load fill ratio, amplitude, compartments or fixtures, while over-rounding is addressed by cycle intensity, media size class and media hardness.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Media lodged in cross-drillings, tapped holes, hems or closed volumes | Media size class small enough to enter a passage but not guaranteed to exit, or a separation step that relies on gravity alone. | Weigh the part where sensitivity allows, inspect passages with a borescope at agreed angles, pass pin or plug gages through each passage, and reconcile media counted into and out of the batch. |
| Rust blooms or speckling on austenitic or duplex parts after finishing | Free iron transferred from carbon steel, ferritic stainless or worn steel machine parts sharing the same media, chamber, racks or bench area. | Run a ferroxyl-type test for free iron at agreed locations, compare against an untouched part from the same batch, and repeat the check after a defined exposure period to catch delayed blooms. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
| Thread crests rounded and thread gages failing after finishing | Mechanical action removing material from crests during an energetic or extended cycle, sometimes with media large enough to strike the thread form directly. | Gage every threaded feature before and after the cycle with the drawing's gages, inspect crest form with an optical comparator, and keep the shortest cycle that still achieves the required appearance. |
Kobe's manufacturing is concentrated in food, transport equipment and general machinery. The city's 2020 Census of Manufacture report counts 1,394 establishments with four or more employees, 67,951 workers and 3,421.1 billion yen of manufactured goods shipments, with value added up 3.3 per cent. It states that food manufacturing and metal products together account for about a quarter of all establishments, and that food, transport equipment and general machinery together account for just over half of employment, with Hyogo ward especially strong in transport equipment and Nishi ward in production machinery and metal products. The city also publishes an economic census and industrial statistics series, and the port has been the city's trade gateway since it opened to foreign trade in 1868.
For this brief the relevant part of that base is automotive: Kobe's 2020 Census of Manufacture report lists transport equipment manufacturing among the three industries that together account for just over half of manufacturing employment, and records Hyogo ward as having a high share of transport equipment.
Kobe's three largest manufacturing employers by industry are food, transport equipment and general machinery, so the surface requirement splits between hygienic, cleanable finishes for food equipment and dimensional, burr-controlled finishes for transport and general machinery parts. General machinery and metal products are concentrated in Nishi ward, where small firms supplying machined components need a finish specification that travels with the drawing rather than a verbal agreement.
A Kobe buyer should separate the two cases before choosing a process: transport and general machinery parts where edge and burr limits govern, and food-equipment parts where cleanability and surface condition govern, because the same media and compound choice will not serve both.
Freight context: Port of Kobe (神戸港), open to foreign trade since 1868, Kobe Airport (神戸空港), opened in 2006. Kobe City records that after the 1995 Hanshin-Awaji earthquake the port's facilities were restored within two years, and that the 2006 opening of Kobe Airport established a combined sea, air and land transport system. Customs clearance in the Kobe area is handled by Kobe Regional Customs, one of Japan Customs' regional offices.
The national standards body is the Japanese Industrial Standards Committee (JISC), which states that JIS covers industrial and mineral products, data, services and management systems under the Industrial Standardization Act. Its technical divisions include mechanical engineering, ferrous materials and metallurgy, nonferrous materials and metallurgy, ceramics, medical equipment and safety appliances, and aircraft and aviation, which are the divisions a finishing or deburring requirement is normally read against. Product certification runs through the JIS Mark Certification Scheme, operated by accredited certification bodies compliant with ISO/IEC 17065; as of March 2019 there were 24 JIS-accredited bodies, three of them outside Japan, with about 8,700 certifications issued, and the scheme explicitly covers foreign manufacturers, processors and exporters.
Documentation and technical communication are Japanese-language in practice: JISC states that the documents submitted for JIS certification-body accreditation must be written in Japanese, and drawings, inspection sheets and purchase specifications from Japanese buyers are normally issued in Japanese. Import declarations are filed in triplicate and importers commonly use licensed customs brokers, so the commercial invoice, packing list and origin documents must be complete and consistent with the declared commodity code. As general industry practice in Japan, industrial buyers qualify a supplier on documentation, quality-management evidence and a defined inspection standard before volume orders, and expect a named Japanese-speaking contact for technical and commercial follow-up.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Acceptance for a stainless automotive part should be settled before a machine or medium is proposed, because the acceptance rule determines which route is even capable. If the finish callout is a word like bright, inspection is whoever looks last; if it is a roughness range at a named location plus a physical visual master viewed under stated lighting, inspection becomes repeatable and the argument moves to the part. Set the sampling plan, the inspection method and the instrument or gage for each characteristic, and decide separately which features get a functional check as opposed to a cosmetic one. Write the rule into the purchase documentation along with the material grade, the marked measurement locations and the acceptance limits for edge condition. A supplier can then report observations against a defined rule instead of being asked to judge its own work.
A trial answers questions only if the parts represent the real range of variation. Send the difficult members of the family rather than an ideal sample: the thinnest wall, the tightest internal feature, the part with the worst incoming burr, the most visible face, and at least two parts that represent normal production condition. Include one part that was rejected for a finishing-related reason, so the trial addresses a defect that actually occurs. With the parts, send the drawing revision, the material grade and condition, the operations that created the current surface, the specified finish requirement, and any feature that must not be touched. A trial run on a single pristine sample tends to produce a pleasant result that says nothing about the batch the buyer will actually process.

They are different processes with different effects, and SurfacePolish does not supply or perform electropolishing. Mechanical finishing works by media contact, so it blends, deburrs and brightens the surfaces the media can reach, and it rounds edges as it works. Electrochemical treatment removes material ionically and reaches into recesses that media cannot. Where an electropolished surface is specified for corrosion or cleanliness reasons, treat electrochemical processing as a comparison point and ask whether the specified requirement can be met by another route, then verify that on your own parts and against your own acceptance rule.
Use a test that detects iron rather than one that detects appearance. A ferroxyl-type reagent applied at agreed locations, left for the specified time, and read against its own reference is the usual method, and it detects free iron before a rust bloom becomes visible. Test the same locations on every sample, keep an untouched control part from the same batch for comparison, and record the result with the date and the part identification. Because a bloom may appear only after days of exposure, agree a defined evaluation window and storage condition. SurfacePolish reports what a trial observed; test method and acceptance level remain the buyer's decision.
Uneven finish comes from position in the load, dead zones in the media mass, shielding by neighbouring parts and part-on-part contact, so evenness is a loading and handling question as much as a machine question. Mark reference locations on the part, photograph under fixed raking light, and measure the same feature at both ends and in the middle rather than at one convenient spot. If the variation is positional, rotating parts between cycles, changing the load pattern, or shortening cycles with repositioning usually helps more than adding time. Tubs suit long parts but need evenness verified along the length.
Use Kobe, Japan as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Kobe buyers reference JIS, maintained by the Japanese Industrial Standards Committee, whose mechanical engineering and ferrous materials divisions cover the city's machinery and transport-equipment output, with the JIS Mark scheme available for third-party product certification. For food-equipment work the additional reference is the customer's hygiene and cleanability requirement, which is specified on the drawing rather than by a general finishing standard.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Kobe.
The buyer needs the stem and seat margins deburred and blended without rounding the seat edge or disturbing the nitrided layer.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0852; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0852 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
