A automotive parts buyer in Maastricht, Netherlands has a thin formed sensor bracket whose laser-cut edges carry dross that must come off without distorting the bend or damaging a threaded insert. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and its free sample trial processes parts sent to Xiamen and returns them with observations and a proposed media, compound and cycle direction for the buyer to verify. This brief is written for a buyer in Maastricht working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which internal features must be deburred without lodging media, and what retrieval and verification step proves the passage and thread form are clean?
Which dimensions, seal faces and thread forms carry functional geometry, and what limit on stock removal per cycle can those features tolerate?
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
Stainless automotive parts usually carry two requirements that pull against each other: an appearance grade on surfaces the customer sees, and an edge or function requirement on features that must keep working. Map the part into exterior visible surfaces, hidden surfaces, and edges with a functional role such as sealing, bearing, fatigue resistance or assembly clearance. An edge that only needs a burr broken can take an energetic cycle; a bore edge that sets a seal or a press fit cannot. Ask which faces are graded after assembly, because a bright panel that meets a specification by itself may look mismatched against the mating panel next to it. A marked-up drawing that states, per surface, whether it is graded, functional or indifferent is the cheapest document in the whole finishing project.
Geometry, not preference, sets media shape and size. Angle-cut triangles and similar forms reach slots, corners and recesses and cut faster on burrs; cylinders and balls blend broad surfaces more evenly and are kinder to edges; small media reaches tighter features but carries more edge impact per contact and is harder to separate. The usable window for any feature lies between media that is too small and packs or lodges and media that is too large to enter at all. For cross-drillings, gear teeth and narrow slots, work from the smallest opening on the drawing and pick a size class that flows through it without wedging. For stainless appearance parts, check the surface texture the shape leaves behind, because some forms produce overlapping impacts that read as a texture rather than as a polish.

| Media | Best fit | Watch out for |
|---|---|---|
| Steel media, including balls and shaped steel forms | Brightening and burnishing of austenitic stainless appearance parts where the highest available gloss is the objective. | Deforms and generates metallic fines, adds weight to the load, and can transfer iron if used in a line shared with carbon steel work. |
| Porcelain and fine high-density ceramic media | Pre-polish refining stages on austenitic stainless appearance parts before a brightening stage, where a finer texture is the objective. | Limited cutting power on hard or work-hardened surfaces, and wear changes the charge gradually, so finish can drift between batches. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
Disc finishing machines run a shallow, fast-moving charge that deburrs heavier machined stainless parts quickly: valve bodies, fittings, machined brackets and parts whose edges can lose material. The energy is an advantage for cycle time and a liability for thin walls and delicate features, so tooling and compartments often decide whether the route is acceptable at all. Centrifugal barrel finishing uses a planetary barrel motion that produces very high energy in short cycles, useful for aggressive edge radiusing on small, hard parts. The same energy rounds edges quickly, can exceed a tight radius callout within a short run, has part size and shape limits, and needs a larger load to justify the cycle. Treat both routes as candidates for heavy deburring and blending, and verify edge results on the actual part rather than assuming a shorter cycle means a safer one.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Tub vibrator | Long stainless parts such as trim sections, exhaust profiles and shafts that cannot be loaded into a bowl without being cut down. | Media velocity varies along the length, so finish evenness must be verified at both ends, and the machine occupies more floor space and compound volume. |
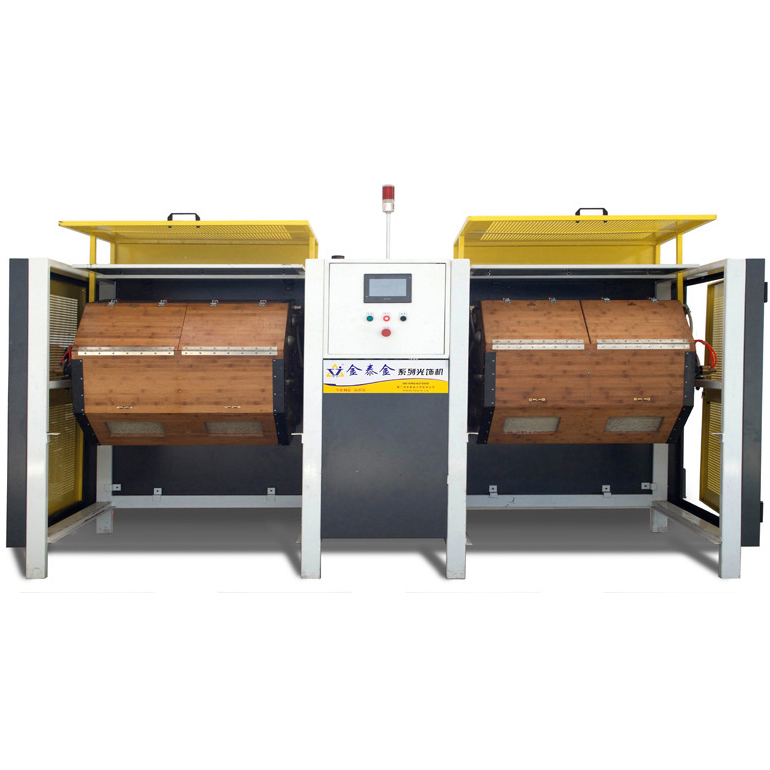
| Barrel finishing machine, rotary barrel tumbler | Gentle deburring and finishing of delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins. | Cycles run longer than in higher-energy machines, and coverage can be uneven on large or complex parts. |
| Vibratory finishing machine, bowl type | General deburring and surface refinement of medium-sized stainless automotive parts such as brackets, small housings and flange blanks in a visible batch load. | Part size and shape are capped by chamber geometry, and thin or threaded parts may need compartments or fixtures to control part-on-part contact. |
| Disc finishing machine | Fast deburring and blending of heavier machined stainless parts whose edges can accept a higher removal rate. | The higher energy can damage thin walls and delicate features, so tooling or compartments are often needed to protect them. |
Two failure modes produce a damaged edge and are often confused. Impingement, sometimes called a gouge or a nick, is local damage from part-on-part contact or media striking a feature at excessive energy, and it typically appears on thin stamped covers, large flat panels and unsupported webs. Its signature is randomness: the defect site moves from part to part and does not follow the geometry of the edge. Over-rounding is systematic, follows the edge itself, and repeats at the same location on every part in the load. Both are found with raking-light photographs, magnification on the suspect feature and comparison across several parts from the same batch. The remedy differs too, because impingement is addressed by load fill ratio, amplitude, compartments or fixtures, while over-rounding is addressed by cycle intensity, media size class and media hardness.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Discolouration or mottling that appears only after drying | Mineral or compound residue carried in the final rinse, hard or chloride-bearing water, or slow drying that leaves a film on the brightened surface. | Compare wet and dry appearance under fixed lighting on the same parts, wipe a sample with a white lint-free cloth and solvent, and check the site water supply for hardness and chloride content. |
| Heat tint, oxide or weld discolouration remaining after a light cycle | Incoming oxide from welding or laser cutting deeper than the finishing stage is designed to remove, or a finishing sequence that only brightens the surrounding surface. | Record the incoming oxide condition with photographs at agreed locations, then compare the same locations after processing and confirm whether removal of the oxide was inside the agreed scope. |
| Rust blooms or speckling on austenitic or duplex parts after finishing | Free iron transferred from carbon steel, ferritic stainless or worn steel machine parts sharing the same media, chamber, racks or bench area. | Run a ferroxyl-type test for free iron at agreed locations, compare against an untouched part from the same batch, and repeat the check after a defined exposure period to catch delayed blooms. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
Maastricht's economy combines a life-sciences campus with an established production base in the city and its surrounding region. The Brightlands Maastricht Health Campus is part of the Brightlands open-innovation community in Limburg, which reports over 32,000 innovative entrepreneurs, researchers and students working on sustainability, health and digitisation, and the campus concentrates researchers, entrepreneurs and students on healthcare, medicine and life sciences with imaging and analytical facilities used by medical start-ups. Alongside that, the Maastricht Maakt industry platform represents 16 production companies in the city, with employers including Tata Steel, Sappi, the Regout Group, SteelSolutions, Mosa, FENZI AGT and SunChemical, and says its operators, technicians and logistics staff work in sectors such as chemistry, food and production. Sappi's Maastricht mill employs nearly 500 people and produces around 260,000 tons of coated woodfree paper and paperboard a year. Maastricht Aachen Airport is part of the national aviation infrastructure and, after Schiphol, the only Dutch airport with a cargo function; the province of Limburg is a shareholder and funds the airport.
The nearest part of that base to this brief is medical: The campus describes first-class imaging facilities and analytical technology as the basis of medical innovation at the site, and positions itself as a location for medical start-ups.
Maastricht and the surrounding Limburg region combine medical-technology work, steel and metal processing, paper production and glass and food manufacturing. Medical-technology and life-sciences activity on the Brightlands Maastricht Health Campus involves stainless and titanium instruments, implants, device housings and precision components, where deburring, edge rounding, passivation and residue-free cleaning are quality requirements, while the city's steel, metal and equipment producers need burr and edge control on machined and cut parts before assembly, coating or further processing. Limburg's wider Brightlands network also includes the Chemelot chemical campus, which adds stainless process and laboratory equipment with comparable cleanliness and corrosion expectations.
A buyer here should settle the documentation and cleanliness standard first, because medical and life-sciences supply chains normally require validated, repeatable processes with defined residue limits, whereas general metal parts usually need no more than a specified burr height and Ra.
Freight context: Maastricht Aachen Airport (cargo function). Maastricht Aachen Airport is the only Dutch airport other than Schiphol with a cargo function and is part of the national aviation infrastructure, which gives the region an air-freight option for urgent parts or samples; the province of Limburg is a shareholder and has funded infrastructure and route development. Machinery arriving by sea is declared to Dutch Customs at its EU point of entry, and the importer needs an EORI number.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
Goods entering the Netherlands from outside the EU must be declared to Dutch Customs (Douane, part of the Belastingdienst); the importer needs an EORI number, import duty is calculated on the customs value (goods value plus transport and insurance to the EU external border), and import VAT is paid at the border unless an article 23 permit or a fiscal representative is used. CE marking is mandatory for most machinery placed on the EEA market: the Machinery Regulation replaced the Machinery Directive and manufacturers must comply with the new requirements by 20 January 2027. The importer must verify that the conformity assessment was carried out correctly, that CE marking is applied properly, that the technical file is present and complete, and that the user manual is supplied in the correct language; the manufacturer's EC Declaration of Conformity must be kept. Dutch companies imported over EUR 140 billion of machinery and appliances in 2024, 24% of total Dutch goods imports.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Appearance grading on stainless is best served by physical masters: one part at the acceptable limit and one at the marginal limit, viewed under the same lighting, at the same distance and at the same angle as production inspection. Lighting is the dominant variable in appearance judgment, so a master viewed beside a window in the morning will not agree with parts viewed under a machine light at night. Record the viewing conditions with the master, keep the master protected and dated, and photograph it as a supplement rather than as a replacement. For satin and brushed finishes, the master should also fix the direction and uniformity of the texture, since a part can meet a roughness figure and still look wrong beside a mating panel. Keep a small library of masters for the finishes this process actually produces, because a single nominal sample cannot cover a batch.
A trial is more useful as a structured comparison than as a single demonstration. Decide in advance what is being compared, such as two media shapes in the same size class, two compound families on one media charge, or two cycle lengths at one energy setting, and hold everything else constant. Keep a control part that receives no finishing at all, so that post-process differences can be attributed to the process rather than to handling. Name the features that must not change and the level of change that would be unacceptable, so that a result can be judged on the spot. Write down the questions the trial must answer before parts are shipped, and rank them, because the ranking is what tells the supplier which comparison matters most when cycle time is limited.

Cost is governed by cycle time and the number of parts that fit in a load, by media consumption and replacement rate, and by labour for loading, unloading, separation, inspection and masking. Parts with several protected features cost more before the machine starts, because plugging and fixturing consume labour. A cycle that needs several stages for deburring, refining and brightening multiplies handling. Drying time and cleanliness verification add further steps, and mixing stainless with carbon steel in shared equipment forces either segregation or extra contamination checks. Ask for cost as a function of volume and batch size rather than as a single figure.
Steel media generally produces the brightest result on austenitic stainless, but brightness depends on the whole progression rather than one medium. A common sequence is a hard ceramic stage that removes burrs and machine marks, a finer stage that refines the texture, then a low-amplitude stage that brightens. Media that is too soft for the work-hardened surface burnishes and dulls instead of cutting. The shape and size class also matter, because small media reaches tight features but leaves a different texture from larger forms. Treat any proposed progression as a comparison to test on real parts with your own measurement setup.
Uneven finish comes from position in the load, dead zones in the media mass, shielding by neighbouring parts and part-on-part contact, so evenness is a loading and handling question as much as a machine question. Mark reference locations on the part, photograph under fixed raking light, and measure the same feature at both ends and in the middle rather than at one convenient spot. If the variation is positional, rotating parts between cycles, changing the load pattern, or shortening cycles with repositioning usually helps more than adding time. Tubs suit long parts but need evenness verified along the length.
Use Maastricht, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers here would reference the CE machinery regime (Machinery Regulation from 20 January 2027) and the Dutch/EN-ISO surface-finishing standards published by NEN, such as NEN-EN-ISO 2080. For medical and life-sciences customers the binding requirements are normally the customer's own cleanliness and validation specification, with ISO 13485 as the customary quality-system reference for medical devices.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Maastricht.
The buyer needs the laser-cut dross and edge burrs removed without distorting the formed bend, rounding the slots beyond limit, or altering the thread insert.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0692; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0692 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
