In Mississauga, Canada, an automotive parts buyer needs a small stainless trim cap brought to a uniform bright finish without waviness, rust speckling or loss of a locating tab. SurfacePolish is a cross-border supplier of finishing machines, media and compounds and runs a free sample trial: parts sent to the Xiamen factory are processed and returned with observations and a proposed media, compound and cycle direction for the buyer to verify. This brief is written for a buyer in Mississauga working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which dimensions, seal faces and thread forms carry functional geometry, and what limit on stock removal per cycle can those features tolerate?
Which surfaces on this part carry a visible appearance grade, which are hidden, and which edges have a functional requirement rather than a cosmetic one?
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
What arrives at finishing often predicts the route better than the drawing does. Burrs sit at cross-drilling intersections, sheared edges and machined contours, heat tint comes from welding and laser cutting, and stamping flash, grinding marks, existing polished bands and handling scratches all behave differently under the same medium and compound. Baseline the incoming surface with roughness readings and consistent-lighting photographs at agreed locations, plus a written note on where the largest burrs sit. Cleanliness before processing also matters, because cutting fluid, marking ink, adhesive residue and shop dust load the medium and confound comparison. Batch size and mix enter here too: a load of thirty small brackets behaves differently from four large housings, and mixing families of different weight in one chamber risks damage to the lighter parts and cross-contamination between grades.
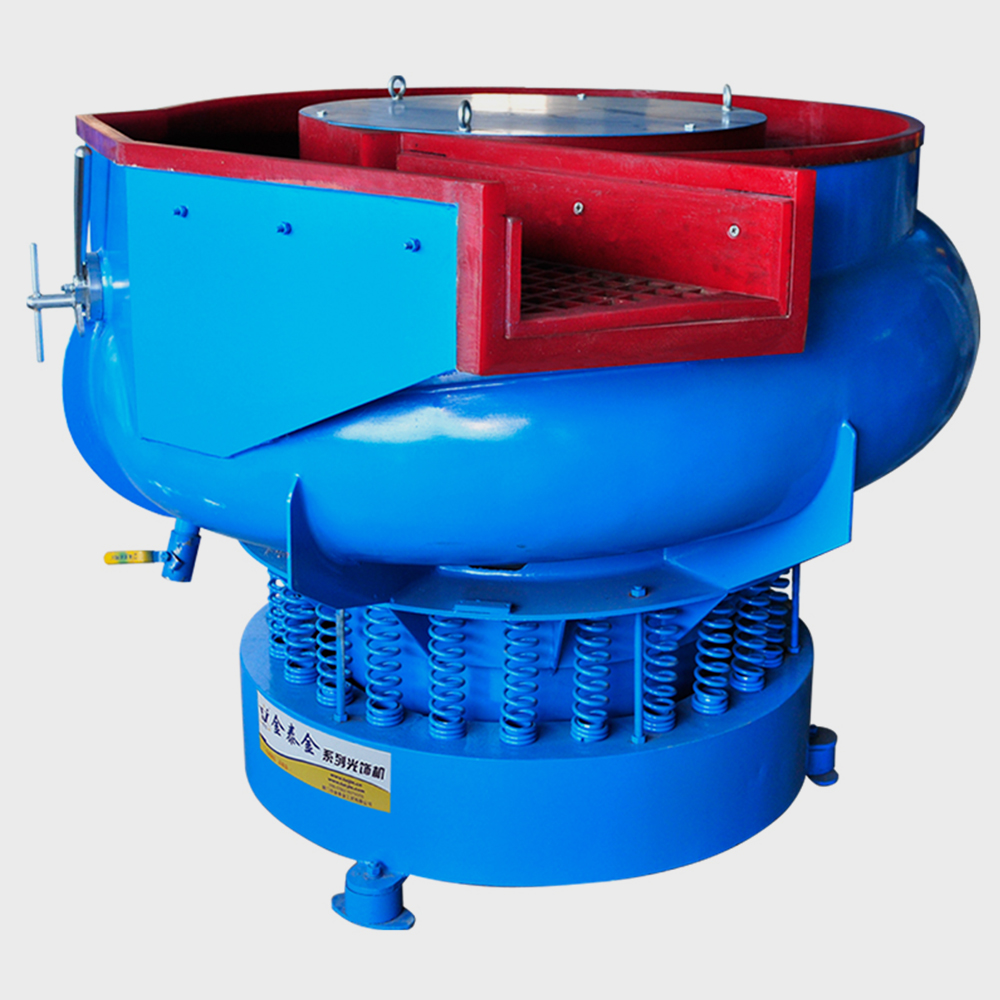
In stainless finishing the first machine question is not how bright the part must become but how much material the most sensitive edge can lose. Mechanical action removes stock far faster at edges, corners and thin sections than on a flat face, so the route follows the tightest edge requirement on the drawing. Where a hole edge or a stamped cover sits in a narrow allowable band, a gentler route such as barrel or rotary, or a vibratory bowl run at moderate energy with an edge-specific compound, is the defensible starting point. Where heavier deburring is needed and edges can tolerate more removal, a disc or centrifugal barrel route uses energy more productively. Record the decision as allowable stock removal per cycle at the tightest feature, because that framing is what lets a supplier recommendation and a buyer limit be compared honestly.
| Machine route | Where it fits | What it will not do |
|---|---|---|
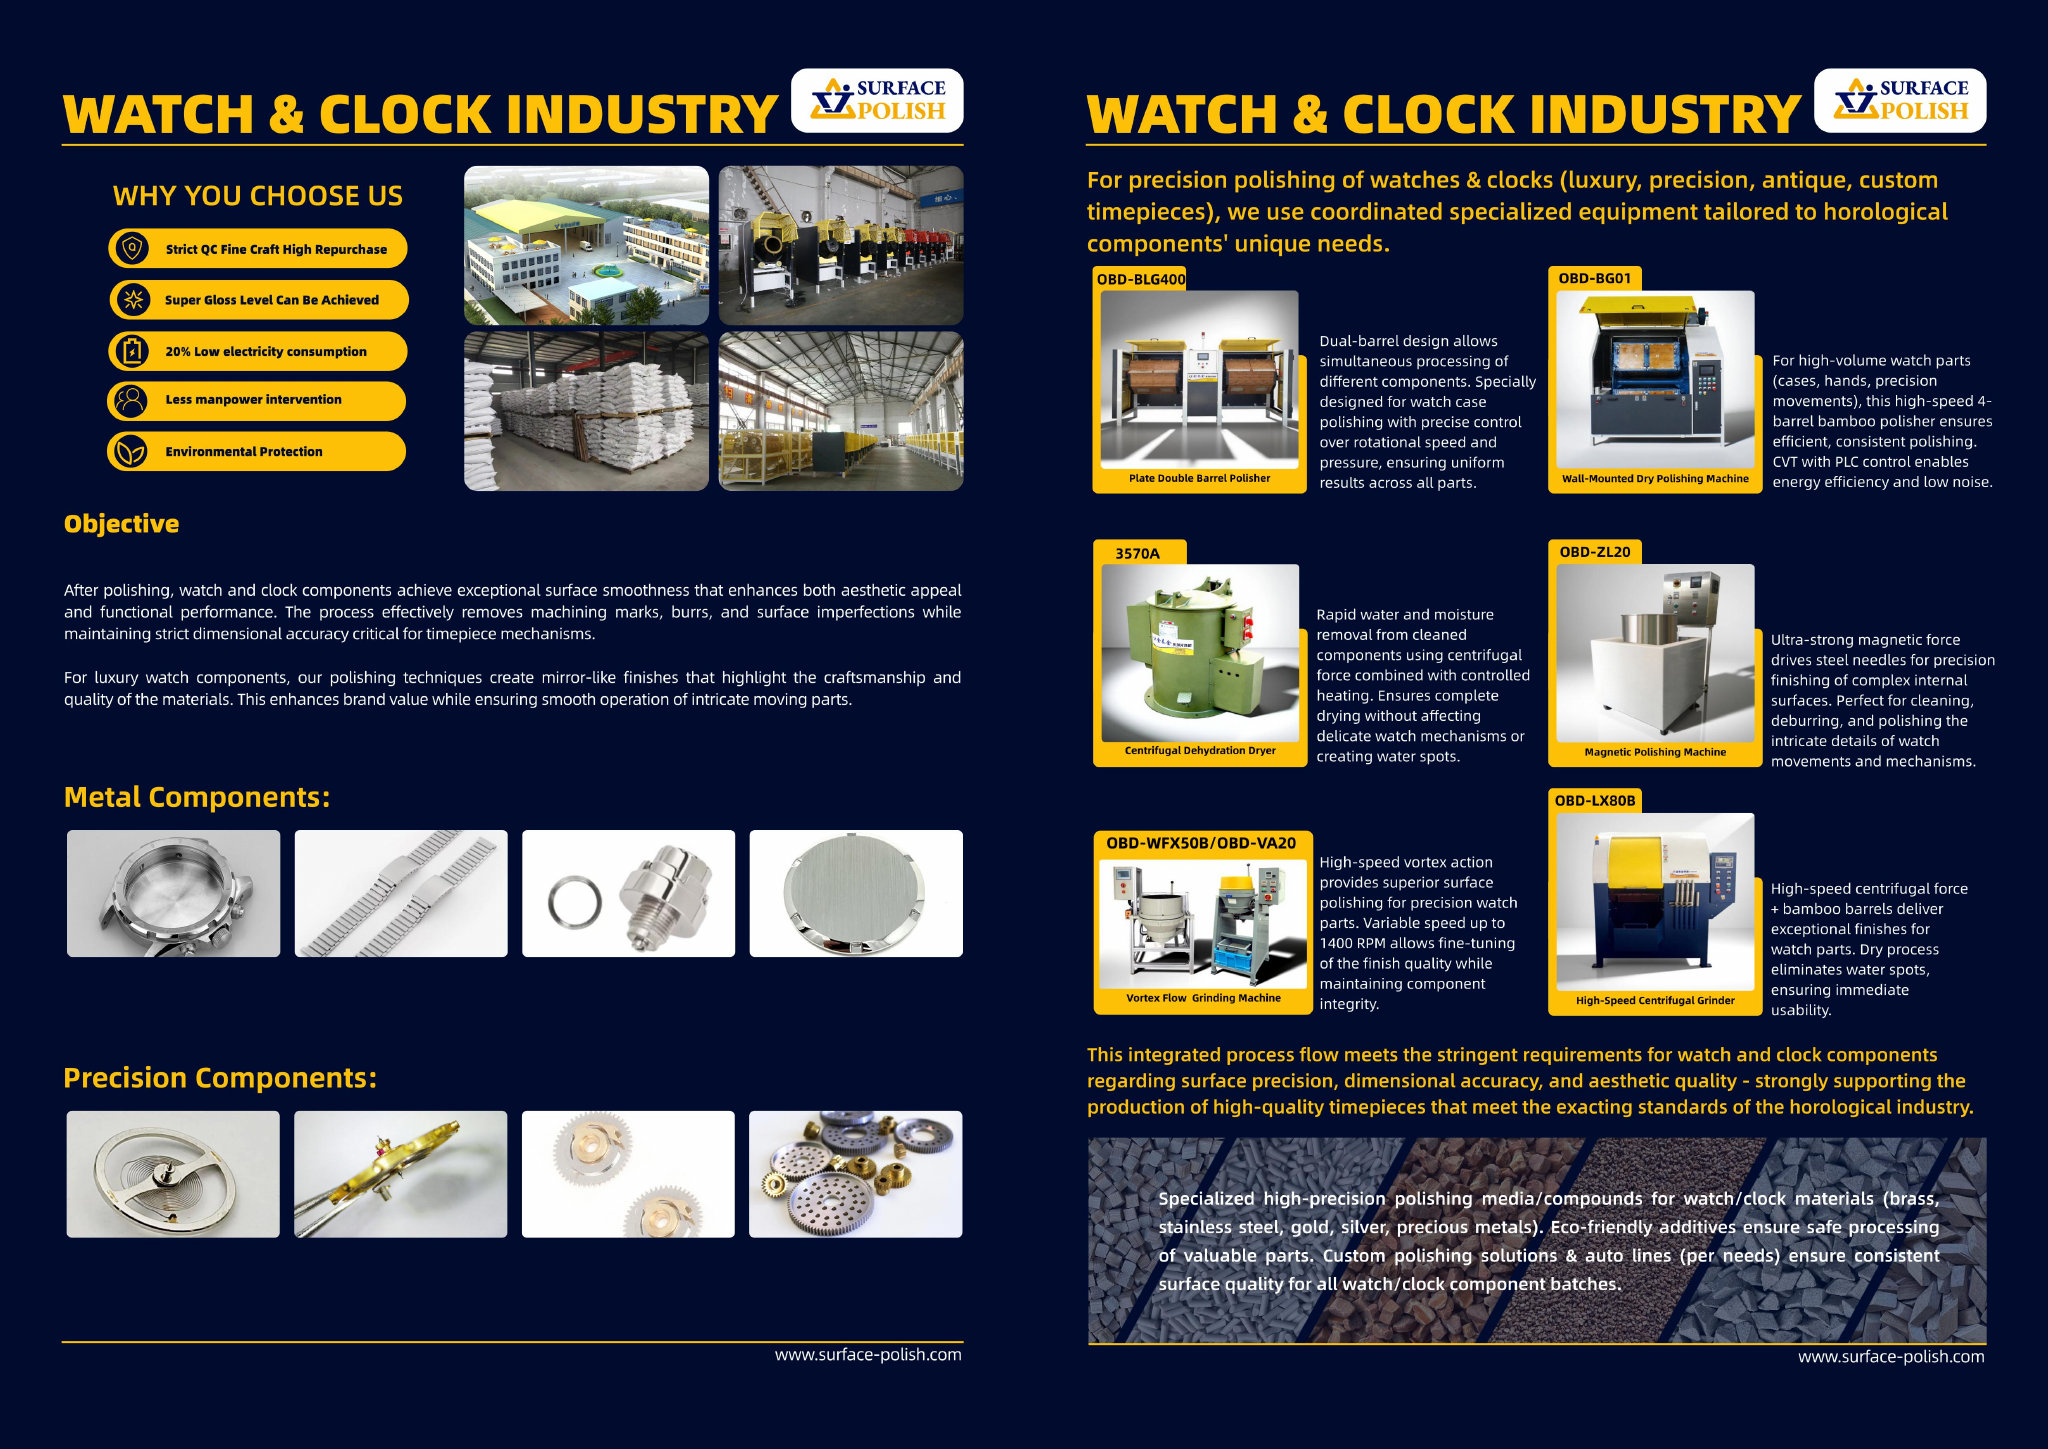
| Magnetic finishing machine | Small precise stainless parts with internal features, slots and blind holes that must be deburred without media lodging in the passages. | Works within a small part envelope, and the route has to be tested per grade because it depends on the part's magnetic response. |
| Barrel finishing machine, rotary barrel tumbler | Gentle deburring and finishing of delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins. | Cycles run longer than in higher-energy machines, and coverage can be uneven on large or complex parts. |
| Dry polishing machine with heated dryer | Post-wet drying, residue control and light dry finishing of stainless parts that must leave the line dry and free of moisture in blind features. | Dry media does not cut stainless, and moisture trapped in a blind hole, hem or tight joint can cause staining if drying is not effective. |
| Disc finishing machine | Fast deburring and blending of heavier machined stainless parts whose edges can accept a higher removal rate. | The higher energy can damage thin walls and delicate features, so tooling or compartments are often needed to protect them. |
A medium can only cut what is softer than itself, and stainless work hardens at the surface during mechanical action, so a medium that is too soft burnishes and dulls instead of brightening. Alumina-based ceramic is the general-purpose choice for deburring, blending and satin finishes on stainless; steel media produces the brightest results on austenitic parts; plastic media suits softer or more delicate components and is usually the wrong tool for stainless cutting; dry media such as walnut shell or corn cob removes residue and moisture but does not generate a true stainless finish. The usual progression for an appearance part is a hard ceramic stage that removes the burr and machine marks, a finer stage that refines the texture, then a low-amplitude brightening stage. Whichever progression is proposed, treat it as a comparison to test on the real part rather than as a fixed recipe.

| Media | Best fit | Watch out for |
|---|---|---|
| Magnetic stainless pins and fine needles for magnetic finishing | Deburring and brightening of intricate small stainless features, slots, gear teeth and blind holes where media cannot be allowed to lodge. | Suits small part envelopes only, and the route needs testing on magnetic grades before it is assumed to apply to a given part. |
| Alumina-based ceramic triangles and angle-cut forms | Heavy deburring, edge blending and machine-mark removal on stainless brackets, flanges and housings where corners and recesses must be reached. | Wears down in size and sharpness, so cutting rate falls without any setting change; broken pieces and fines can lodge in small features and must be screened out. |
| Ceramic cylinders, balls and other rounded shapes | General surface refinement and blending on broad stainless faces where a more even texture and gentler edge action are wanted. | Does not reach sharp internal corners, and long enough running on thin sections can still round edges beyond a tight callout. |
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
Stainless parts that emerge with speckled rust, a brown bloom or a grey smut have usually picked up foreign metal, and the source is often the shop rather than the alloy. Free iron can arrive from carbon steel parts run in the same machine or media, from worn steel components in the chamber, from steel racks and containers, from a wire brush used elsewhere, or from airborne grinding dust settling on a wet part. A ferroxyl-type test at agreed locations detects free iron, and a comparison against an untouched control part from the same batch makes the result interpretable. Because the visible bloom may take days to appear, agree an evaluation window and keep sample parts in defined conditions before judging. Prevention is segregation: dedicated media and machines for stainless, non-metallic or stainless handling, covered storage, and a check on incoming media for metallic debris.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Edge rounding beyond the specified radius on a functional edge | Cycle energy, time or media size class chosen for appearance rather than for the tightest edge callout on the drawing. | Measure edge radius at marked locations with an optical comparator or a cast impression before and after, and record the result against a written allowable band rather than judging it visually. |
| Discolouration or mottling that appears only after drying | Mineral or compound residue carried in the final rinse, hard or chloride-bearing water, or slow drying that leaves a film on the brightened surface. | Compare wet and dry appearance under fixed lighting on the same parts, wipe a sample with a white lint-free cloth and solvent, and check the site water supply for hardness and chloride content. |
| Thread crests rounded and thread gages failing after finishing | Mechanical action removing material from crests during an energetic or extended cycle, sometimes with media large enough to strike the thread form directly. | Gage every threaded feature before and after the cycle with the drawing's gages, inspect crest form with an optical comparator, and keep the shortest cycle that still achieves the required appearance. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
Mississauga is one of the largest manufacturing and distribution municipalities in the Greater Toronto Area, and its economic development agency positions the city specifically around industrial supply chains: Invest Mississauga's leading-industries page invites businesses to "Join a growing community of globally connected businesses and robust supply chains in Mississauga", and it maintains a public economic development data centre for the city. The city's manufacturing base sits inside the Toronto region's food and beverage cluster, which the City of Toronto measures at more than 64,000 workers across the region with more than half of those jobs located inside the city of Toronto itself, leaving a substantial remainder in the surrounding 905 municipalities including Mississauga and Brampton. Mississauga also sits inside the automotive and advanced-manufacturing belt of southern Ontario, whose supply chains the federal government is actively supporting: FedDev Ontario announced a combined repayable investment of over CAD 12.5 million for Hamilton-area businesses alone as they "respond to tariff-related pressures, strengthen domestic supply chains, and position themselves for long-term growth".
For this brief the relevant part of that base is automotive: Federal regional development funding for the southern Ontario manufacturing belt is framed around helping area businesses respond to tariff-related pressures and strengthen domestic supply chains, with over CAD 12.5 million announced for nine Hamilton-area manufacturers including steel, welding and automation firms.
Mississauga's manufacturing mix of food and beverage processing, metal fabrication and automotive-tier parts creates three distinct finishing problems in one city: stainless process and packaging equipment where weld dressing and cleanable surfaces are required, sheet-metal and fabricated enclosures where a uniform finish on visible surfaces is part of the delivered product, and machined or stamped metal components where burrs interfere with assembly, sealing or coating adhesion. Because much of this work is high-mix and short-run, the practical constraint is changeover time and the cost of dedicating a finishing step to a small batch, which is what drives interest in flexible batch machines rather than large dedicated lines.
A Mississauga buyer should settle the batch-size and changeover question before choosing equipment, because a high-mix fabricator or food-equipment builder will lose more money to media changeover and cleaning between jobs than to slow cycle times within a job. The second question is whether the finishing step is there to protect a downstream process — coating adhesion, sealing, or a customer's burr limit on an automotive drawing — in which case the acceptance criterion and the inspection method need to be agreed in writing before the machine is specified.
Freight context: Toronto Pearson International Airport (immediately adjacent to Mississauga), CN and CPKC intermodal terminals in the Greater Toronto Area, Port of Toronto (inland marine gateway), Greater Toronto Area 400-series highway freight network. Mississauga's principal logistics advantage is its position directly beside Toronto Pearson International Airport, which makes air freight of sample parts, media and urgent spares practical, combined with dense rail intermodal and highway freight capacity across the GTA. Machines arriving from Asia would normally land at a coastal container port and be railed or trucked into the GTA, with the Port of Toronto providing an inland marine option for bulk and project cargo.
The customs authority is the Canada Border Services Agency (CBSA), and importers of commercial goods must work through the CBSA Assessment and Revenue Management (CARM) system, which is where registration, the duties-and-taxes calculator, advance rulings and national customs rulings, and the commercial accounting declaration (CAD) are handled. Documentation expectations are explicit: "You must provide proof of country of origin when you import goods into Canada and, in some cases, your goods must also be clearly marked", the invoice or sales receipt must carry "a complete description of the goods", "the selling price" and "any conditions and terms of the sale", and the value for duty must be declared in Canadian currency only. Duties and taxes are layered rather than single: customs duty on the tariff item, the Goods and Services Tax calculated on the duty-paid value, and potentially excise duty, excise tax, surtax or safeguard measures. Importers must also clear non-tariff gates: goods must be admissible, some goods need permits, certificates or inspections from other federal departments that the CBSA applies on their behalf, controlled goods under the Defence Production Act require consultation with the CBSA and Global Affairs Canada before import, and "Goods manufactured or produced wholly or in part by forced or prison labour are prohibited from entering Canada", with due diligence resting on the importer. For electrical machinery, the practical conformity route in Canada is certification of the product to Canadian electrical safety standards by an accredited certification body rather than a self-declared CE-style mark; buyers should confirm the specific certification body and mark required before shipment. For a first shipment of a finishing machine or a media/compound sample lot, the fastest way to remove classification and valuation uncertainty is to use the CARM portal to request an advance ruling for tariff classification and origin.
Canada's national standards system is coordinated by the Standards Council of Canada (SCC), which accredits standards-development organizations, certification bodies and testing laboratories; the SCC and CSA Group websites could not be retrieved for citation during this research, so this entry rests on the accessible Government of Canada and CCOHS material below. The Canadian Centre for Occupational Health and Safety describes standards as documents that "establish specifications and procedures to ensure the reliability of the products, methods, and services people use every day on the job", and Innovation, Science and Economic Development Canada (ISED) maintains the federal entry point for "[t]he different types of standards and certifying bodies that can be used by your business". In practice a Canadian buyer of finishing equipment references (a) the Canadian electrical safety certification of the machine and its control panel, (b) provincial occupational health and safety regulation for machine guarding, lockout and dust/ventilation control, which in Canada is enforced by the provinces rather than by a single federal inspectorate, and (c) the buyer's own customer-specific surface finish, edge-condition and cleanliness specifications, which are contractual rather than national standards. Finishing-process standards in the ISO 25.080 machine-tool and ISO 8500-series surface-preparation families are the usual technical reference points, but product-level standards sold by CSA Group were not retrievable for verification here.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Acceptance for a stainless automotive part should be settled before a machine or medium is proposed, because the acceptance rule determines which route is even capable. If the finish callout is a word like bright, inspection is whoever looks last; if it is a roughness range at a named location plus a physical visual master viewed under stated lighting, inspection becomes repeatable and the argument moves to the part. Set the sampling plan, the inspection method and the instrument or gage for each characteristic, and decide separately which features get a functional check as opposed to a cosmetic one. Write the rule into the purchase documentation along with the material grade, the marked measurement locations and the acceptance limits for edge condition. A supplier can then report observations against a defined rule instead of being asked to judge its own work.
A trial answers questions only if the parts represent the real range of variation. Send the difficult members of the family rather than an ideal sample: the thinnest wall, the tightest internal feature, the part with the worst incoming burr, the most visible face, and at least two parts that represent normal production condition. Include one part that was rejected for a finishing-related reason, so the trial addresses a defect that actually occurs. With the parts, send the drawing revision, the material grade and condition, the operations that created the current surface, the specified finish requirement, and any feature that must not be touched. A trial run on a single pristine sample tends to produce a pleasant result that says nothing about the batch the buyer will actually process.

Control direction, texture depth and coverage, not only a roughness number. Mechanical finishing tends to create directionality, so agree with the customer whether the grain runs in one direction across the whole part order and how visible variation may be. Keep a physical master for the satin finish and view parts under the same lighting, distance and angle as the master, because lighting changes appearance judgements more than small process changes do. Fix media shape, size class and cycle settings in a work instruction, and re-verify the finish whenever the media charge is replaced or a new supplier batch of compound is introduced.
Speckled rust usually means free iron contamination rather than a material fault. Common sources are carbon steel parts run in the same machine or media, worn steel components in the chamber, steel racks and baskets, grinding dust settling on wet parts, and tools used elsewhere in the shop. A ferroxyl-type test at agreed locations confirms free iron, and a comparison against an untouched part from the same batch makes the result usable. Prevention is segregation: dedicated media and handling for stainless, covered storage, and a check on incoming media for metallic debris.
A trial produces observations on the parts tested under the settings used, and nothing more. It cannot guarantee a surface value, appearance grade, cycle time, capacity or cost in production, and it does not certify or qualify a process for any regulated application. What it can do is narrow the field: compare two media, two compound families or two cycle lengths under controlled conditions, expose edge and lodging risks, and give your engineering team measured before-and-after data to work from. Read the trial record, check that the settings are described fully enough to repeat, and keep the acceptance decision and any qualification work inside your own quality system.
Use Mississauga, Canada as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Mississauga buyer references Canadian electrical safety certification of the equipment, Ontario occupational health and safety requirements for guarding and lockout, and — for food and beverage customers — the food-safety expectations that apply to product-contact surfaces and cleaning procedures. Automotive-tier customers add their own drawing-level specifications for burr limits, edge condition and surface roughness.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Mississauga.
The buyer needs the cap brought to a uniform bright finish without waviness, cross-contamination speckling or loss of the locating tab geometry.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0152; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0152 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
