A buyer in Phoenix, United States working on automotive parts has an exhaust flange that needs a brighter visible face while its sealing bead stays flat and free of iron contamination. SurfacePolish supplies finishing machines and consumables across borders and runs a free sample trial: the parts travel to Xiamen and come back with observations plus a proposed media, compound and cycle direction for the buyer's own engineering review. This brief is written for a buyer in Phoenix working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
At what batch size, load fill ratio and media wear state does a trial observation still describe what series production will produce?
Which internal features must be deburred without lodging media, and what retrieval and verification step proves the passage and thread form are clean?
Which surfaces on this part carry a visible appearance grade, which are hidden, and which edges have a functional requirement rather than a cosmetic one?
Stainless is a family, not one material, and the finishing window changes with it. Ferritic grades used for exhaust and trim are magnetic and generally softer, so they cut quickly and can smear; martensitic grades used for wear parts are hard and magnetic, and some high-strength conditions carry a hydrogen concern when acid chemistry is involved; austenitic grades are tough, work harden under mechanical action and are usually non-magnetic, which changes retrieval options; duplex and super-duplex grades combine high strength with chloride sensitivity, so surface contamination matters more. Cold work matters twice, because a pressing or a machined skin alters surface hardness and can shift magnetic response, and because a bright finish on a work-hardened skin may not survive a later forming operation. Record grade, delivery condition, hardness range and prior cold work, then match machine energy and media hardness to the family rather than reusing a recipe that worked elsewhere.
A medium can only cut what is softer than itself, and stainless work hardens at the surface during mechanical action, so a medium that is too soft burnishes and dulls instead of brightening. Alumina-based ceramic is the general-purpose choice for deburring, blending and satin finishes on stainless; steel media produces the brightest results on austenitic parts; plastic media suits softer or more delicate components and is usually the wrong tool for stainless cutting; dry media such as walnut shell or corn cob removes residue and moisture but does not generate a true stainless finish. The usual progression for an appearance part is a hard ceramic stage that removes the burr and machine marks, a finer stage that refines the texture, then a low-amplitude brightening stage. Whichever progression is proposed, treat it as a comparison to test on the real part rather than as a fixed recipe.

| Media | Best fit | Watch out for |
|---|---|---|
| Magnetic stainless pins and fine needles for magnetic finishing | Deburring and brightening of intricate small stainless features, slots, gear teeth and blind holes where media cannot be allowed to lodge. | Suits small part envelopes only, and the route needs testing on magnetic grades before it is assumed to apply to a given part. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
| Steel media, including balls and shaped steel forms | Brightening and burnishing of austenitic stainless appearance parts where the highest available gloss is the objective. | Deforms and generates metallic fines, adds weight to the load, and can transfer iron if used in a line shared with carbon steel work. |
| Dry media, walnut shell and corn cob | Post-wet drying, light residue and scale removal, and dry polishing of surfaces that must not be re-wetted. | Does not cut stainless, generates dust, and leaves organic residue on parts if the medium is not kept clean and dry. |
In stainless finishing the first machine question is not how bright the part must become but how much material the most sensitive edge can lose. Mechanical action removes stock far faster at edges, corners and thin sections than on a flat face, so the route follows the tightest edge requirement on the drawing. Where a hole edge or a stamped cover sits in a narrow allowable band, a gentler route such as barrel or rotary, or a vibratory bowl run at moderate energy with an edge-specific compound, is the defensible starting point. Where heavier deburring is needed and edges can tolerate more removal, a disc or centrifugal barrel route uses energy more productively. Record the decision as allowable stock removal per cycle at the tightest feature, because that framing is what lets a supplier recommendation and a buyer limit be compared honestly.
| Machine route | Where it fits | What it will not do |
|---|---|---|
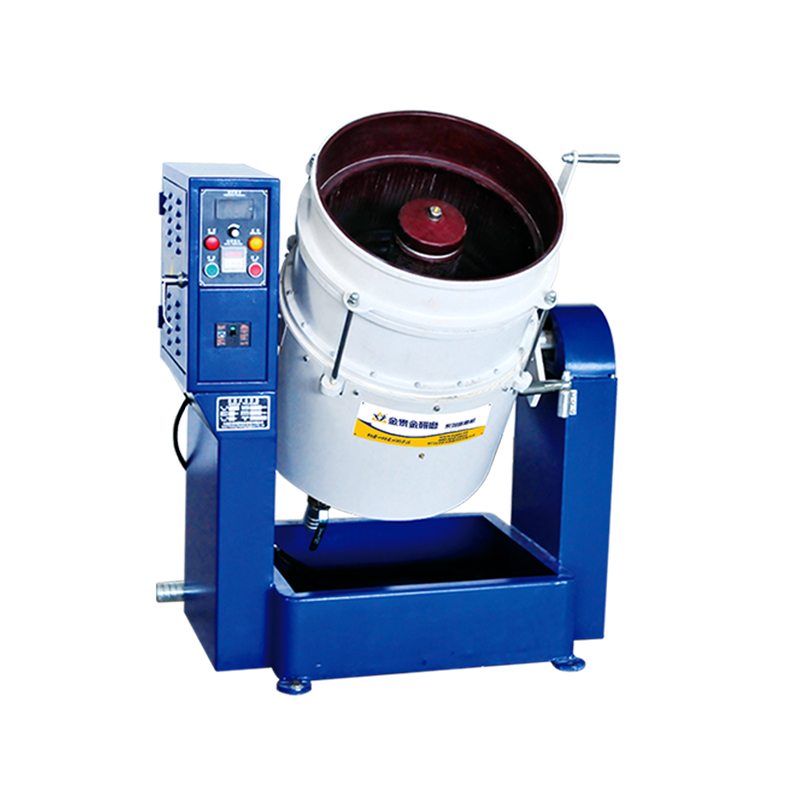
| Vibratory finishing machine, bowl type | General deburring and surface refinement of medium-sized stainless automotive parts such as brackets, small housings and flange blanks in a visible batch load. | Part size and shape are capped by chamber geometry, and thin or threaded parts may need compartments or fixtures to control part-on-part contact. |
| Tub vibrator | Long stainless parts such as trim sections, exhaust profiles and shafts that cannot be loaded into a bowl without being cut down. | Media velocity varies along the length, so finish evenness must be verified at both ends, and the machine occupies more floor space and compound volume. |
| Continuous or indexed wet line with staged media charges | Multi-stage stainless finishing where deburring, refining and brightening are separated to control edge loss and texture progression. | Needs clear segregation between stages to prevent carry-over of coarse media or iron contamination, and adds handling and floor space. |
| Disc finishing machine | Fast deburring and blending of heavier machined stainless parts whose edges can accept a higher removal rate. | The higher energy can damage thin walls and delicate features, so tooling or compartments are often needed to protect them. |
Two failure modes produce a damaged edge and are often confused. Impingement, sometimes called a gouge or a nick, is local damage from part-on-part contact or media striking a feature at excessive energy, and it typically appears on thin stamped covers, large flat panels and unsupported webs. Its signature is randomness: the defect site moves from part to part and does not follow the geometry of the edge. Over-rounding is systematic, follows the edge itself, and repeats at the same location on every part in the load. Both are found with raking-light photographs, magnification on the suspect feature and comparison across several parts from the same batch. The remedy differs too, because impingement is addressed by load fill ratio, amplitude, compartments or fixtures, while over-rounding is addressed by cycle intensity, media size class and media hardness.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Rust blooms or speckling on austenitic or duplex parts after finishing | Free iron transferred from carbon steel, ferritic stainless or worn steel machine parts sharing the same media, chamber, racks or bench area. | Run a ferroxyl-type test for free iron at agreed locations, compare against an untouched part from the same batch, and repeat the check after a defined exposure period to catch delayed blooms. |
| Impingement marks, nicks or gouges on thin stainless panels and webs | Part-on-part contact in an under-filled chamber, excessive amplitude, or free parts striking each other where no compartment or fixture controls them. | Inspect the suspect feature under magnification and raking light before and after processing, and compare its location across several parts from the same load to confirm the defect is random rather than systematic. |
| Thread crests rounded and thread gages failing after finishing | Mechanical action removing material from crests during an energetic or extended cycle, sometimes with media large enough to strike the thread form directly. | Gage every threaded feature before and after the cycle with the drawing's gages, inspect crest form with an optical comparator, and keep the shortest cycle that still achieves the required appearance. |
| Heat tint, oxide or weld discolouration remaining after a light cycle | Incoming oxide from welding or laser cutting deeper than the finishing stage is designed to remove, or a finishing sequence that only brightens the surrounding surface. | Record the incoming oxide condition with photographs at agreed locations, then compare the same locations after processing and confirm whether removal of the oxide was inside the agreed scope. |
Metro Phoenix combines semiconductor packaging and device manufacturing, aerospace and defence production, electric-vehicle assembly and large-scale nuclear generation. Amkor Technology lists its corporate headquarters and business operations in Tempe, Arizona and promotes a new US advanced packaging and test facility for the domestic semiconductor supply chain. Boeing states that it builds and tests AH-64 Apache helicopters at its Mesa, Arizona site for the US Army and global customers, and Lucid Motors states it selected a 500-acre property in Casa Grande, Arizona, between Phoenix and Tucson, for its first purpose-built electric-vehicle factory. The US Energy Information Administration locates the Palo Verde nuclear station in Maricopa County, and CBP lists Phoenix, Arizona (2605) and Phoenix-Mesa Gateway Airport (2682) as ports of entry served by the Tucson field office. Phoenix Sky Harbor International is a large-hub airport in the FAA's final CY2025 enplanement table.
For this brief the relevant part of that base is automotive: Lucid Motors states it selected a 500-acre property in Casa Grande, Arizona, between Phoenix and Tucson, for its factory, described as the first purpose-built EV factory in North America.
Semiconductor packaging, tool and equipment manufacturing around Phoenix needs deburred, low-particle surfaces on machined stainless and aluminium parts, because residual media, compound or metal fines are a contamination risk on parts that go near a bond line, a vacuum chamber or a cleanroom. Aerospace and defence work in Mesa adds edge-control and surface-texture requirements tied to fatigue life and coating adhesion, and electric-vehicle drivetrain and battery-enclosure parts are typically specified for edge quality and burr-free, coating-ready surfaces. In all three cases the finish specification is set by the downstream process, not by appearance.
For Phoenix buyers the first question is what happens to the part downstream: a cleanroom, vacuum or bond-line part needs a documented cleaning and particle limit and a finishing process whose media cannot embed or shed, whereas an aerospace or EV part is usually governed by edge-radius and coating-adhesion callouts. Settling the residue or cleanliness test and the edge callout before trialling media is what prevents a finish that looks correct but fails the customer's validation.
Freight context: Phoenix Sky Harbor International Airport (PHX), Phoenix, Arizona (CBP port of entry 2605) and Phoenix-Mesa Gateway Airport (2682). FAA final CY2025 enplanement data list Phoenix Sky Harbor International with 25,094,817 boardings, and CBP's Arizona table lists Phoenix, Arizona (2605) and Phoenix-Mesa Gateway Airport (2682) as ports of entry under the Tucson field office. Metro Phoenix has no seaport, so containerised machines from China normally arrive at a West Coast port and move inland by rail or truck, clearing CBP at the port of unlading or at the Phoenix port of entry; air consignments such as sample parts clear at Sky Harbor.
The customs authority is U.S. Customs and Border Protection (CBP), part of the Department of Homeland Security. The importer of record files an entry and then an entry summary (CBP Form 7501): '"Entry Summary" refers to the documentation necessary to enable U.S. Customs and Border Protection to assess duties, collect statistics, and determine whether other requirements of law have been met.' Classification is made in the Harmonized Tariff Schedule of the United States, and an importer may request a written CBP ruling on the correct HTSUS classification and rate of duty, which is the practical way to confirm the treatment of a finishing machine before shipment. Every article of foreign origin must be marked with the English name of its country of origin 'in a conspicuous place as legibly, indelibly, and permanently as the nature of the article (or container) will permit' under 19 U.S.C. 1304 and 19 CFR 134.11. The $800 de minimis (Section 321) exemption is no longer available for ordinary freight: CBP suspended it indefinitely for all modes other than the international postal network effective 24 June 2026, so even low-value sample parts and media must go through formal or informal entry and pay applicable duty. General US industry practice is that there is no single machinery conformity mark comparable to the EU's CE marking; buyers instead verify electrical components and control panels, machine guarding against workplace-safety requirements, and any customer-specific qualification.
Business is conducted in US English. Units matter: US drawings and purchase orders frequently use inches, microinch Ra and US gallons, and a supplier that quotes only metric can be asked to reissue documentation. Buyers are US legal entities with an EIN and expect an identifiable contracting entity, a correct HTSUS classification, a commercial invoice, packing list and bill of lading, country-of-origin marking, and an importer of record for customs. Procurement is normally evidence-driven: process selection is expected to be justified by a trial run on the buyer's own sample parts with measured results (burr height, edge radius, Ra, cleanliness) and by media and compound data sheets, rather than by a capability claim. Payment terms in general US industrial practice are open account with net-30 to net-60 terms for established buyers, with letters of credit or advance payment more common for a first order from a new overseas supplier; no US buyer assumes Incoterms, warranty terms or spare-parts lead times unless they are stated in the quotation.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Measurement of appearance does not detect a functional loss, so acceptance needs checks aimed at what the part does. Thread and gear gages on the features named by the drawing, pin or plug gages on cross-drilled passages, a flatness check on sealing faces, a fit or press trial on a bearing bore, and continuity or gap checks on sensor surfaces all address function directly. Edge condition deserves a dimension rather than an opinion, because a rounding of a fraction of a millimetre at the mouth of an O-ring groove changes how the seal seats, and a deburred edge on a fatigue-relevant hole behaves differently from a polished one. Cleanliness is part of this set: wipe tests for residue, free-iron testing, and a borescope check of internal passages catch defects that appearance grading cannot. Agree every check and its instrument before the first production batch.
Once a line is producing, batch control protects both the finish and the traceability. Identify each load with the material heat or lot, keep grades separate through the chamber and the dry stage, record the media charge identification and compound batch, and keep the inspection record attached to the same batch identifier so a later complaint can be traced to what actually ran. For stainless, batch separation also means physical separation from carbon steel processing, including shared baskets, dryers and benches. What a trial cannot prove is worth stating plainly: it observes the parts tested under one set of conditions, it does not guarantee a surface value, cycle time, capacity or cost in production, and it does not qualify a process for any regulated application. Treat it as a way to reduce uncertainty before capital is committed, and let the buyer's own verification settle acceptance.

They are different processes with different effects, and SurfacePolish does not supply or perform electropolishing. Mechanical finishing works by media contact, so it blends, deburrs and brightens the surfaces the media can reach, and it rounds edges as it works. Electrochemical treatment removes material ionically and reaches into recesses that media cannot. Where an electropolished surface is specified for corrosion or cleanliness reasons, treat electrochemical processing as a comparison point and ask whether the specified requirement can be met by another route, then verify that on your own parts and against your own acceptance rule.
Use a test that detects iron rather than one that detects appearance. A ferroxyl-type reagent applied at agreed locations, left for the specified time, and read against its own reference is the usual method, and it detects free iron before a rust bloom becomes visible. Test the same locations on every sample, keep an untouched control part from the same batch for comparison, and record the result with the date and the part identification. Because a bloom may appear only after days of exposure, agree a defined evaluation window and storage condition. SurfacePolish reports what a trial observed; test method and acceptance level remain the buyer's decision.
Steel media generally produces the brightest result on austenitic stainless, but brightness depends on the whole progression rather than one medium. A common sequence is a hard ceramic stage that removes burrs and machine marks, a finer stage that refines the texture, then a low-amplitude stage that brightens. Media that is too soft for the work-hardened surface burnishes and dulls instead of cutting. The shape and size class also matter, because small media reaches tight features but leaves a different texture from larger forms. Treat any proposed progression as a comparison to test on real parts with your own measurement setup.
Use Phoenix, United States as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Semiconductor-equipment and cleanroom-adjacent parts are commonly specified against SEMI standards with explicit particulate, residue and surface-finish limits, while general machined parts are called out to ASME B46.1 or ISO 4287/4288; aerospace work in Mesa typically also carries AS9100 quality-system and NADCAP special-process requirements with SAE AMS process specifications on the certificate.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Phoenix.
The buyer needs the visible face brightened and the bore burr removed without touching the flatness of the sealing bead, and without iron contamination that would bloom in service.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0092; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0092 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
