In Yokohama, Japan, an automotive parts buyer needs a small stainless trim cap brought to a uniform bright finish without waviness, rust speckling or loss of a locating tab. SurfacePolish is a cross-border supplier of finishing machines, media and compounds and runs a free sample trial: parts sent to the Xiamen factory are processed and returned with observations and a proposed media, compound and cycle direction for the buyer to verify. This brief is written for a buyer in Yokohama working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
At what batch size, load fill ratio and media wear state does a trial observation still describe what series production will produce?
How will free iron, embedded particles and cross-contamination from carbon steel be prevented, and how will each be detected on the finished part?
Which surfaces on this part carry a visible appearance grade, which are hidden, and which edges have a functional requirement rather than a cosmetic one?
Stainless is a family, not one material, and the finishing window changes with it. Ferritic grades used for exhaust and trim are magnetic and generally softer, so they cut quickly and can smear; martensitic grades used for wear parts are hard and magnetic, and some high-strength conditions carry a hydrogen concern when acid chemistry is involved; austenitic grades are tough, work harden under mechanical action and are usually non-magnetic, which changes retrieval options; duplex and super-duplex grades combine high strength with chloride sensitivity, so surface contamination matters more. Cold work matters twice, because a pressing or a machined skin alters surface hardness and can shift magnetic response, and because a bright finish on a work-hardened skin may not survive a later forming operation. Record grade, delivery condition, hardness range and prior cold work, then match machine energy and media hardness to the family rather than reusing a recipe that worked elsewhere.
A medium can only cut what is softer than itself, and stainless work hardens at the surface during mechanical action, so a medium that is too soft burnishes and dulls instead of brightening. Alumina-based ceramic is the general-purpose choice for deburring, blending and satin finishes on stainless; steel media produces the brightest results on austenitic parts; plastic media suits softer or more delicate components and is usually the wrong tool for stainless cutting; dry media such as walnut shell or corn cob removes residue and moisture but does not generate a true stainless finish. The usual progression for an appearance part is a hard ceramic stage that removes the burr and machine marks, a finer stage that refines the texture, then a low-amplitude brightening stage. Whichever progression is proposed, treat it as a comparison to test on the real part rather than as a fixed recipe.

| Media | Best fit | Watch out for |
|---|---|---|
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
| Magnetic stainless pins and fine needles for magnetic finishing | Deburring and brightening of intricate small stainless features, slots, gear teeth and blind holes where media cannot be allowed to lodge. | Suits small part envelopes only, and the route needs testing on magnetic grades before it is assumed to apply to a given part. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
| Porcelain and fine high-density ceramic media | Pre-polish refining stages on austenitic stainless appearance parts before a brightening stage, where a finer texture is the objective. | Limited cutting power on hard or work-hardened surfaces, and wear changes the charge gradually, so finish can drift between batches. |
Tub vibrators exist for parts that a bowl cannot hold: long trim rails, exhaust sections, shafts and formed profiles that must be processed without being cut down. The open tub allows awkward geometry, and the long, large parts common in stainless automotive work often fit only here. The engineering consequence is that media velocity and dwell differ along the length, so one end of a long part can finish differently from the other. Verify evenness at both ends of the longest part rather than at one representative location. Media size class has to suit the tub cross-section so the charge moves as a mass instead of settling. A tub also consumes more floor space and compound volume than a bowl of similar throughput, which is part of the line concept a buyer should settle before quoting a cell.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Continuous or indexed wet line with staged media charges | Multi-stage stainless finishing where deburring, refining and brightening are separated to control edge loss and texture progression. | Needs clear segregation between stages to prevent carry-over of coarse media or iron contamination, and adds handling and floor space. |
| Barrel finishing machine, rotary barrel tumbler | Gentle deburring and finishing of delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins. | Cycles run longer than in higher-energy machines, and coverage can be uneven on large or complex parts. |
| Vibratory finishing machine, bowl type | General deburring and surface refinement of medium-sized stainless automotive parts such as brackets, small housings and flange blanks in a visible batch load. | Part size and shape are capped by chamber geometry, and thin or threaded parts may need compartments or fixtures to control part-on-part contact. |
| Dry polishing machine with heated dryer | Post-wet drying, residue control and light dry finishing of stainless parts that must leave the line dry and free of moisture in blind features. | Dry media does not cut stainless, and moisture trapped in a blind hole, hem or tight joint can cause staining if drying is not effective. |
Two failure modes produce a damaged edge and are often confused. Impingement, sometimes called a gouge or a nick, is local damage from part-on-part contact or media striking a feature at excessive energy, and it typically appears on thin stamped covers, large flat panels and unsupported webs. Its signature is randomness: the defect site moves from part to part and does not follow the geometry of the edge. Over-rounding is systematic, follows the edge itself, and repeats at the same location on every part in the load. Both are found with raking-light photographs, magnification on the suspect feature and comparison across several parts from the same batch. The remedy differs too, because impingement is addressed by load fill ratio, amplitude, compartments or fixtures, while over-rounding is addressed by cycle intensity, media size class and media hardness.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Media lodged in cross-drillings, tapped holes, hems or closed volumes | Media size class small enough to enter a passage but not guaranteed to exit, or a separation step that relies on gravity alone. | Weigh the part where sensitivity allows, inspect passages with a borescope at agreed angles, pass pin or plug gages through each passage, and reconcile media counted into and out of the batch. |
| Dimensional drift, including bores opening slightly and thin walls thinning | Sustained media contact removing material from every accessible surface, with cycle time or media size class beyond what the feature tolerances can absorb. | Measure critical dimensions with micrometers, bore gages or a CMM before and after on a fixed sample size, and track a maximum stock removal per cycle for each feature at risk. |
| Heat tint, oxide or weld discolouration remaining after a light cycle | Incoming oxide from welding or laser cutting deeper than the finishing stage is designed to remove, or a finishing sequence that only brightens the surrounding surface. | Record the incoming oxide condition with photographs at agreed locations, then compare the same locations after processing and confirm whether removal of the oxide was inside the agreed scope. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
Yokohama combines a waterfront heavy-industry zone with a large base of small and medium manufacturers. The city lists eight separate industrial accumulation areas, including the Keihin coastal zone, which it calls a major industrial region representing the Greater Tokyo area, and LINKAI Yokohama Kanazawa, where more than 1,000 companies and offices are located. The city's investment material states that Yokohama has clusters of automotive and other manufacturing, IT and life-science industries, together with R&D bases of global companies, and that it ranks first among Japan's designated cities for both the number of academic and R&D institutions and the number of engineers and researchers. The port's designated zones are predominantly industrial: of a 2,936.8 ha waterfront district, 1,712.1 ha is classified as an industrial port zone.
For this brief the relevant part of that base is automotive: Yokohama City's business-environment page states that the city has clusters of the automotive industry and other manufacturing, IT and life-science industries.
Yokohama's manufacturing base mixes automotive and general machinery production, in which deburring and edge quality affect fit, fatigue life and coating adhesion, with life-science and R&D activity, where cleanliness and documented surface condition matter. A dense supplier base across eight accumulation areas means an incoming parts specification is likely to pass through several subcontractors, so a shared, measurable finish requirement reduces rework at hand-offs.
A Yokohama buyer sourcing from an eight-area supplier base should fix one measurable edge and surface specification for the whole chain and agree who inspects it, rather than letting each subcontractor apply its own visual standard.
Freight context: Port of Yokohama (横浜港) — piers including Minami-Honmoku, Honmoku, Daikoku and Osanbashi, Haneda Airport, about 24 minutes from Yokohama Station by the city's own access description. The Port of Yokohama has a 7,218.3 ha port area and a 2,936.8 ha waterfront district, of which 1,712.1 ha is an industrial port zone, so both break-bulk and container movements of machinery sit alongside industrial waterfront users. The city publishes the Yokohama Port Statistics Yearbook and fast-report series for throughput data used in freight planning.
Chinese industrial machinery entering Japan is classified under the Customs Tariff Law, whose harmonised schedule sets the classification and the General Rate; the Temporary Tariff Measures Law sets a Temporary Rate for certain products, and where the WTO rate or an EPA rate for the goods is lower, that lower rate is applied. The applied rate therefore depends on the exact commodity code, and on whether an economic partnership agreement covers the goods and their origin, so a landed-cost figure has to be confirmed against the specific machine before it is quoted. Japan Customs' monthly country table for August 2026 records exports to China of 1,809,133 million yen and imports from China of 2,361,239 million yen, the largest single-country line in the Asian table, with imports from China up 22.5 per cent year on year.
The customs authority is Japan Customs, the Customs and Tariff Bureau of the Ministry of Finance, with regional customs at Tokyo, Yokohama, Nagoya, Osaka and Kobe. Any person importing goods must declare them to the Director-General of Customs and obtain an import permit after examination and payment of customs duty and consumption tax. The declaration is normally filed by the importer or by a customs broker acting as proxy, on a triplicate import (customs duty payment) declaration form (Customs form C-5020) supported by the invoice, the bill of lading or air waybill, a certificate of origin where a WTO rate applies, certificates of origin for preferential rates, packing lists and freight and insurance documents where required, plus any licence or certificate demanded by laws other than the Customs Law. More than 90 per cent of import procedures are computerised. A JIS Mark certificate is a separate, voluntary third-party scheme; foreign exporters are eligible to apply, and certification bodies must comply with ISO/IEC 17065.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Acceptance for a stainless automotive part should be settled before a machine or medium is proposed, because the acceptance rule determines which route is even capable. If the finish callout is a word like bright, inspection is whoever looks last; if it is a roughness range at a named location plus a physical visual master viewed under stated lighting, inspection becomes repeatable and the argument moves to the part. Set the sampling plan, the inspection method and the instrument or gage for each characteristic, and decide separately which features get a functional check as opposed to a cosmetic one. Write the rule into the purchase documentation along with the material grade, the marked measurement locations and the acceptance limits for edge condition. A supplier can then report observations against a defined rule instead of being asked to judge its own work.
A trial is more useful as a structured comparison than as a single demonstration. Decide in advance what is being compared, such as two media shapes in the same size class, two compound families on one media charge, or two cycle lengths at one energy setting, and hold everything else constant. Keep a control part that receives no finishing at all, so that post-process differences can be attributed to the process rather than to handling. Name the features that must not change and the level of change that would be unacceptable, so that a result can be judged on the spot. Write down the questions the trial must answer before parts are shipped, and rank them, because the ranking is what tells the supplier which comparison matters most when cycle time is limited.
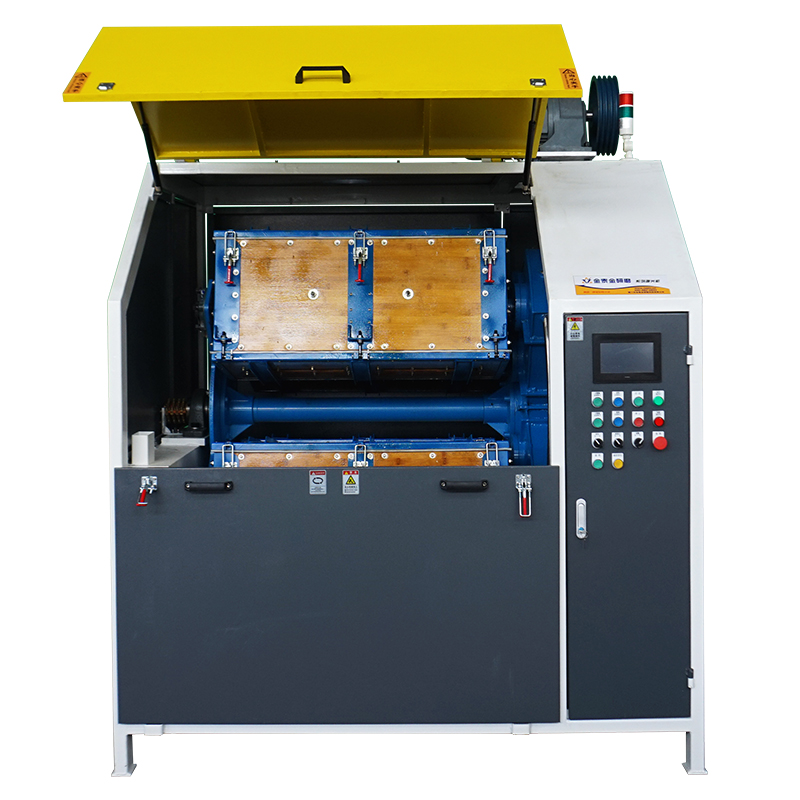

Speckled rust usually means free iron contamination rather than a material fault. Common sources are carbon steel parts run in the same machine or media, worn steel components in the chamber, steel racks and baskets, grinding dust settling on wet parts, and tools used elsewhere in the shop. A ferroxyl-type test at agreed locations confirms free iron, and a comparison against an untouched part from the same batch makes the result usable. Prevention is segregation: dedicated media and handling for stainless, covered storage, and a check on incoming media for metallic debris.
Treat them as two separate requirements rather than one. Map exterior visible surfaces, hidden surfaces and every edge that has a job such as sealing, bearing or assembly clearance. Appearance zones tolerate broad blending; functional edges need a stated limit and a measuring method. The two often pull in opposite directions, because the cycle that brightens a panel also removes material fastest at exactly the edges that must stay inside a band. Ask the designer to confirm colour, texture and direction on visible faces, and put the edge requirement in writing with its instrument before any media is chosen.
Steel media generally produces the brightest result on austenitic stainless, but brightness depends on the whole progression rather than one medium. A common sequence is a hard ceramic stage that removes burrs and machine marks, a finer stage that refines the texture, then a low-amplitude stage that brightens. Media that is too soft for the work-hardened surface burnishes and dulls instead of cutting. The shape and size class also matter, because small media reaches tight features but leaves a different texture from larger forms. Treat any proposed progression as a comparison to test on real parts with your own measurement setup.
Use Yokohama, Japan as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Yokohama buyers reference JIS, maintained by the Japanese Industrial Standards Committee, with the mechanical engineering and ferrous materials divisions covering machined metal parts, and the JIS Mark scheme available for third-party product certification, including to foreign exporters. For finishing, the customer's drawing and incoming-inspection sheet define burr, edge and roughness acceptance.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Yokohama.
The buyer needs the cap brought to a uniform bright finish without waviness, cross-contamination speckling or loss of the locating tab geometry.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0832; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0832 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
