Process Troubleshooting Why Stainless Steel Parts Are Not Bright After Tumbling and How to Improve the Finish Surface finishing defects are often caused by interactions between mul
Production Separation Guide How to Separate Small Parts from Tumbling Media: Screens, Size Control, and Process Design A finishing cycle is not production-ready until parts can be separated from media repeatedly. This guide explains how part geometry, media wear, screen design, orientation, and external separation methods affect labor, carryover, and the risk of trapped media. Part-media separatio...
Process Comparison Dry Polishing vs Wet Polishing Which Surface Finish Method is Best Choosing between two finishing processes requires understanding how each method applies energy
Surface Finishing How to Achieve Mirror Finish on Stainless Steel with Mechanical Polishing This guide covers the key factors to consider when planning a surface finishing process
Process Comparison Vibratory Finishing vs Barrel Tumbling Which Process Fits Your Parts Choosing between two finishing processes requires understanding how each method applies ener
Process Troubleshooting Why Stainless Steel Parts Are Not Bright After Tumbling and How to Improve the Finish Surface finishing defects are often caused by interactions between mul
Process Troubleshooting How to Prevent Tumbling Media from Lodging in Holes Slots and Threads Surface finishing defects are often caused by interactions between multiple process va
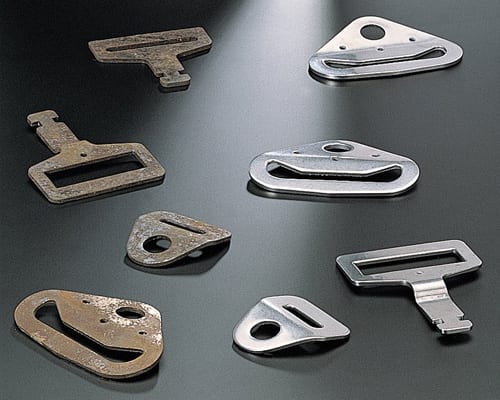
Stamped Parts Finishing Guide How to Deburr Stamped Metal Parts Without Tangling, Distortion, or Part-on-Part Damage Stamped washers, clips, brackets, and thin sheet-metal parts can be efficient mass-finishing candidates, but their geometry creates risks that solid machined parts do not have. This guide explains how to evaluate the burr, select a machine and media, control part interaction, and bu...
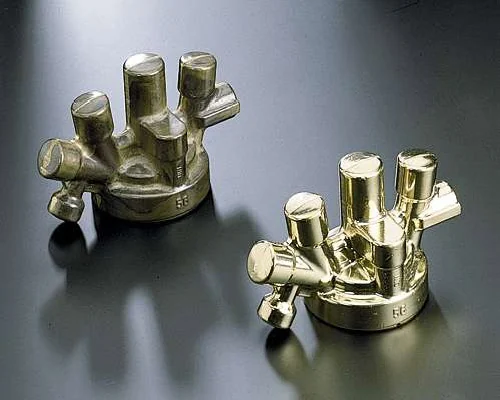
Brass Component Finishing Guide How to Finish Brass Valves and Fittings Without Damaging Threads or Sealing Surfaces Brass valve bodies, pipe fittings, sleeves, and connectors can be deburred and surface-finished in batches, but their threads, bores, sealing faces, flats, and thin edges require separate protection and inspection. The best process removes the actual defect without changing how the ...
We use essential storage to keep this site working. With your permission, Google Analytics 4 helps us understand visits and improve the site. Advertising storage, ad user data, and ad personalization always stay off.




 IPv6 network supported


 +86-592-2381506