An aluminium stage plate for medical devices is mostly datum: dowel holes, a tapped pattern and a flatness callout leave very little room for rounding or distortion. A buyer in Nottingham, United Kingdom can send a representative plate to SurfacePolish, a cross-border supplier of finishing machines, media and compounds, for a free sample trial. This brief is written for a buyer in Nottingham working on medical devices; it describes equipment, media and a scoped sample review, not a local polishing service.
What are the alloy and temper, and has machining, casting, welding or heat treatment already changed the surface hardness and porosity?
What is the minimum wall thickness and unsupported span, and which internal features could trap media?
What edge radius or chamfer is allowed at each mating, sealing and press-fit feature, and how will it be measured?
A finishing route is only as good as the parts fed into it, so characterise the starting condition first. Note the machining process, the depth and direction of tool marks, whether the part was linished or hand-sanded already, whether it carries heat-treat scale or an as-cast skin, and which surfaces were scratched in handling. A batch of mixed starting conditions produces a mixed finish, because a cycle that removes a twenty-micron tool mark on 6061 will not remove a deep gouge without rounding the part. Record batch size, the mix of part numbers and the quantity of each, since an underloaded bowl or barrel runs differently from a full one. Segregate parts by alloy, by temper and by pre-finish condition before they enter the same machine.
Media shape decides which features receive work. Angle-cut triangles, stars and wedges reach into corners and produce an edge break; spheres and ellipsoids blend surface and remove very little edge material; cylinders and pins work inside bores and slots; flattened or lens shapes reach recesses a rounded body cannot. On aluminium components with mixed features this distinction is the whole decision: a sphere-heavy charge protects a sealing edge but leaves a burr at a bore exit, while a sharp-edged charge removes the burr and rounds the very edge that has to stay accurate. Size matters just as much. Large media cannot enter a small slot but produce a more open, less clogged charge; small media follow tighter geometry but lodge in pockets, pack blind holes and are harder to screen out of the load. Define the smallest feature to be worked before specifying size class.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media, corn cob with a polishing compound charge | Final dry polish and drying assistance on small aluminium parts where a wet rinse and dry would leave spotting | Compound loading saturates with use and the media cakes; the charge needs regular replacement, and soft aluminium can still smear |
| Plastic-bonded media, ball and ellipsoid shapes | Surface refinement and blending on cosmetic aluminium faces where edges, seal lands and dowel bores must stay close to drawing | Removes very little edge material, so a burr at a bore exit or a thread crest may survive the cycle and need a separate step |
| Plastic-bonded media, light to medium abrasive grade, cone and triangle shapes | General deburring and satin finishing on 6061 and 7075 where galling risk rules out dense ceramic | Wears quickly and loses edge definition; cut rate drops as the charge ages and the cosmetic result drifts unless media is screened and topped up |
| Ceramic media, spheres and low-density ceramic, fine size class | Bright surface development and light edge work on small aluminium components with mixed cosmetic and internal features | Fine media lodges in blind holes, cross-drillings and thin-wall pockets and is harder to screen out of the load |
Disc finishing machines generate high energy at the disc face and remove material and round edges quickly, which is attractive when a batch of aluminium parts needs a burr gone in a short cycle. That same energy is what makes them risky on soft wrought aluminium and on thin castings. Part-on-part contact is high, so parts impinge, peen each other and develop a hammered or uneven surface, and 6061 will smear rather than cut if the compound is wrong or the load too heavy. Fixturing helps: a carrier that holds each part in a fixed attitude reduces random contact but adds load and unload labour to every cycle. Disc routes are also unforgiving on edge control because removal is neither uniform nor easy to localise. Use them where a robust part needs a fast radius.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Dry polishing machine and dryer | Post-wet drying and dry polishing of aluminium parts before anodising, laser marking, bonding or packaging | Does not remove a burr or refine a surface on its own; residual media dust and incomplete drying still cause marking and coating defects |
| Tub vibrator | Long and large aluminium parts such as extruded frames and housings that can be oriented in a linear working channel | Slower uniform coverage, a tendency for parts to settle in one attitude, and greater floor space and media volume than a bowl |
| Magnetic finishing machine | Small aluminium parts with fine internal features such as cross-holes, slots and recesses that tumbling media cannot reach | Small working envelope and low throughput; pins and fine media can lodge in blind features, and mixed part families are awkward |
| Rotary barrel finishing machine | Gentle, low-energy deburring of small precise aluminium parts in high volume, including thin and light components | Longer cycles for the same result; flat or light parts may slide rather than tumble, and an overloaded barrel stops working the load |
Media cannot tell a cosmetic edge from a sealing edge, so a cycle that breaks a burr nicely on the outside of a housing can round a seal land, a dowel bore or a press-fit shoulder until it no longer functions. The drift is gradual and cumulative: each pass removes a little more material, and a batch that was within tolerance at the start of a media charge may be outside it by the end. Watch for a seal face that has lost its flat land, a bore edge closed to a radius, or a chamfer grown past the drawing. Detect it with an optical comparator or radius gauge on a cross-section, or by measuring the feature with a CMM before and after. Protection comes from shielding the functional edge, rounder and lighter media, and a first-article check.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Damaged thread or media wedged in a thread root | Threads left exposed to the media field, sharp media entering the crest, insufficient plugging or masking of ports before the cycle | Run a go and no-go gauge through every sampled thread and inspect the root with a borescope or a thread impression |
| Dimensional drift on a critical bore, dowel hole or press-fit diameter | Aggressive media attacking a feature the cycle should not touch, cumulative removal over repeated runs, no masking of close-tolerance geometry | Measure the feature with a CMM or bore gauge at first article and at the end of the media charge, and chart the trend against drawing limits |
| Sealing land or dowel bore edge rounded past the drawing limit | Long or energetic cycle on an unprotected functional edge, sharp-edged media, cumulative material removal across repeated passes | Measure the edge with an optical comparator or radius gauge on a cross-section, or compare a CMM scan of the feature before and after finishing |
| Media or abrasive fragment lodged in a blind hole, cross-drilling or thin-wall pocket | Media size class too small for the feature, unshielded pockets, flexing thin wall gripping the fragment, no dedicated retrieval step | Borescope the internal features, weigh against a known-clean reference, tap over white paper, and inspect the residue from an ultrasonic clean |
Nottingham is a Nottinghamshire authority inside the East Midlands Freeport, the only inland UK freeport, whose three sites are East Midlands Airport and Gateway Industrial Cluster (EMAGIC) in Leicestershire, the Ratcliffe-on-Soar power station site in Nottinghamshire, and the East Midlands Intermodal Park in Derbyshire. The freeport states its sites are connected by road, rail and air and within easy reach of East Midlands Airport, which it calls the UK's largest dedicated airfreight airport, and it reports that a share of the UK's major freight rail lines are serviced through the East Midlands. Nottingham City Council provides the city's business licensing, trading standards and procurement services, and the East Midlands Chamber is the regional chamber of commerce.
The nearest part of that base to this brief is machinery: The freeport reports that a share of the UK's major freight rail lines are serviced through the East Midlands, the freight context for the area's engineering firms.
The East Midlands Freeport is built around freight and low-carbon industry sites rather than a legacy machining cluster, so finishing requirements in the Nottingham area follow the parts being made and moved rather than any single local process tradition. Because the freeport's sites connect by road, rail and air and the East Midlands is a major goods-importing region, deburring, edge and cleanliness specifications should be taken from the component drawing and its downstream assembly rather than from a general local practice.
A Nottingham buyer should tie the finishing specification to the part's actual route out of a freeport or industrial site - air, rail or road - and confirm media and compound handling and waste arrangements before the machine is ordered.
Freight context: East Midlands Airport (described by East Midlands Freeport as the UK's largest dedicated airfreight airport), East Midlands Intermodal Park, Derbyshire, Ratcliffe-on-Soar power station site, Nottinghamshire. East Midlands Freeport describes itself as the only inland UK Freeport, with sites connected by road, rail and air and within easy reach of East Midlands Airport; it states that a share of the UK's major freight rail lines are serviced through the East Midlands.
China does not appear in the alphabetical list of trade agreements in effect published by the Department for Business and Trade, so Chinese-origin machinery imported into the UK cannot claim a preferential agreement rate. Duty is instead determined by the commodity code declared on the import declaration, and the UK's customs authority is HM Revenue and Customs (HMRC), which ONS also names as the largest single data source behind UK trade-in-goods statistics. Because a GB-prefixed EORI number is a precondition for importing into England, Scotland or Wales, a Chinese seller's UK buyer must already hold that registration before any machine ships.
Importers need a GB-prefixed Economic Operators Registration and Identification (EORI) number, an import declaration carrying the correct commodity code, and retained commercial invoices plus the Import VAT Certificate (C79) so import VAT can be reclaimed. Machinery placed on the Great Britain market must be marked UKCA or CE: the manufacturer must draw up and retain technical documentation including a Declaration of Conformity, apply the correct marking with identification details, and cooperate with market surveillance; an authorised representative must be established in the UK. Under the Product Safety and Metrology (Amendment) Regulations 2024 the UK continues to recognise CE marking alongside or in place of UKCA for the Great Britain market, so either route can be used for most product types. Duty and import VAT are calculated from the customs value declared, and the commodity code also determines whether an import licence is needed.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A roughness number without a location and a cut-off is not a specification. On an aluminium device component, name each surface that carries a roughness requirement, the direction of measurement relative to the machining or polishing marks, and the cut-off and evaluation length to be used, since a profile measured over a short length with a short cut-off reads differently from one measured across the full face. ISO 4287 and ISO 4288 describe profile parameters and the rules for selecting cut-off, ISO 25178 covers areal texture if a three-dimensional description is needed, and ASME B46.1 is the equivalent North American reference. Aluminium is soft, so stylus force and tip radius can mark the surface being measured; agree the instrument and the force, or use an optical method, and retain the measured part as the physical reference.
Send parts that represent the real production condition, not a polished bench sample. A useful set includes the worst case: the thinnest wall, the tightest sealing edge, the deepest tool mark, the casting with visible porosity, the smallest hole and the feature most likely to trap media. Include two or three pieces of each condition so one can be sectioned or inspected internally, and include an untreated part as the comparison reference. Label every part with its alloy and temper, its part number, the surfaces that are cosmetic, the surfaces that are functional, and the edge radius or chamfer allowed at each critical feature. State the current process and the defect that prompted the enquiry, plus the downstream operation such as anodising, laser marking or assembly.
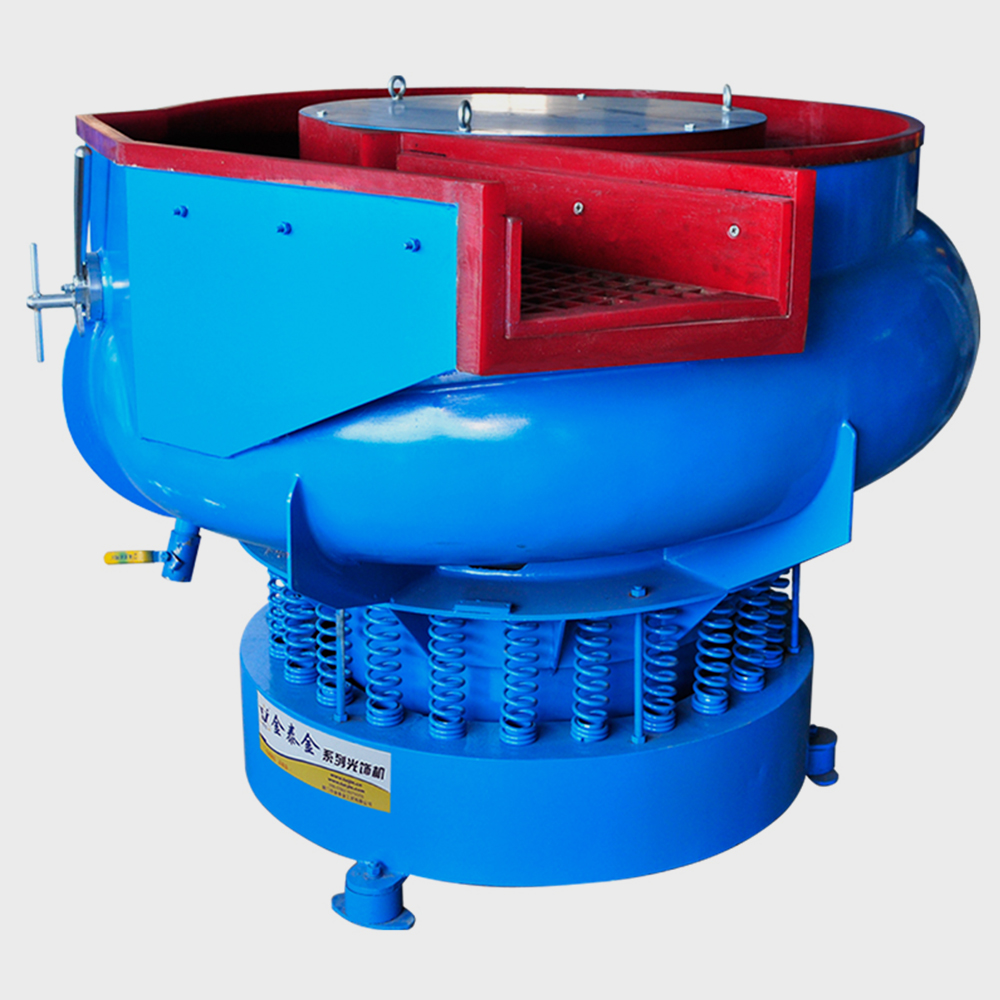

A bowl vibrator circulates a load through a media field at moderate energy, with good uniformity on small parts that tumble freely and easy discharge. A centrifugal barrel presses media and parts together at high force in a much shorter cycle, producing a fine finish and controlled edge quickly, but bending thin walls, distorting light sections and rounding edges faster. Bowl routes suit mixed small parts and gentle work; centrifugal routes suit a narrow part family that fits the barrel and accepts the energy. Parts made in United Kingdom should be trialled in the specific geometry before a machine size is fixed, because barrel dimensions limit part length and load size.
Lodging is a geometry problem before it is a media problem. Blind holes, cross-drillings, thread roots, undercuts and thin-wall pockets trap fragments, and a pocket that flexes under load grips them harder. Options include shielding or plugging the trapping features, changing the media size class so pieces cannot enter, moving to a route whose loading geometry differs, and adding an inspection step with a borescope or a weighed reference part. A visual pass on an exterior face proves nothing about a cavity. For parts made in United Kingdom, agree with the buyer which internal features are checked and how, before the first batch is run.
It will if the edge is exposed to the media for long enough. Media cannot distinguish a cosmetic edge from a seal land, a dowel bore or a press-fit shoulder, and rounding accumulates gradually, so a batch inside tolerance at the start of a media charge can be outside it later. Protection comes from shielding or masking the functional edge, using rounder and lighter media, shortening the cycle, and checking the feature with an optical comparator, radius gauge or CMM rather than by eye. A buyer in United Kingdom should state the allowed edge radius per feature on the drawing, because a blanket edge-break note will be read literally.
Use Nottingham, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Equipment placed on the Great Britain market requires UKCA or CE marking with a Declaration of Conformity, and HSE's work equipment and machinery and COSHH regimes cover finishing machines, media and compounds. Nottingham City Council's trading standards service and business licensing function are the local points of contact for product and trading rules.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Nottingham.
The buyer must remove machining burrs from the hole pattern without moving the dowel hole edges or disturbing the plate's flatness.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0293; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0293 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
