A cleaning equipment maker in Fukuoka, Japan supplying food processing equipment has a 316L spray ball whose drilled holes and thread start carry burrs. The internal channel is small and enclosed, so any medium that enters may never come out, and the buyer needs to weigh that risk before selecting a machine. SurfacePolish supplies finishing equipment, media and compounds across borders, and runs a free sample trial on shipped parts. This brief is written for a buyer in Fukuoka working on food processing equipment; it describes equipment, media and a scoped sample review, not a local polishing service.
What free-iron and chloride exposure does the process itself introduce, and can the buyer's own cleanliness test detect it before the part is released?
Which surfaces on this part touch product, and what does each one have to satisfy in roughness, oxide freedom, edge condition and cleanliness?
Which internal surfaces can a mechanical route physically reach, and what happens to the zones it cannot?
Before any trial, fix the starting condition in a way that can be compared later. Take roughness readings at agreed locations, photograph the part under consistent lighting, note visible burrs, tint and scratches, and keep one untouched part as a reference. Describe the batch: how many pieces of each size, whether they are identical, and whether mixed sizes will share a chamber. Decide how parts will be separated, racked or compartmented, and which surfaces may touch each other or a fixture. Handling rules matter as much as process settings on stainless, because a bench, a rack or a glove that has touched carbon steel can leave the contamination that later appears as a rust bloom. Write the baseline down, because a trial without an incoming record produces observations nobody can interpret.
A tub vibrator gives a long, open chamber that accepts parts a bowl cannot, including tube spools, chute sections, small vessels and long fabrications. The part can be repositioned, rotated or left static depending on what has to be reached, and the open design makes it easier to watch what is happening to a weld during the cycle. The trade-off is evenness: coverage depends on how the part sits relative to the media mass, so banding and untouched shadow zones are common unless fixture and part orientation are planned. Internal surfaces of a long small-bore tube remain out of reach regardless of tub size. Tub capacity, media volume, how the part is supported and how it is lifted in and out should be settled before the route is accepted.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Barrel finishing machine, rotary barrel tumbler | Large batches of small robust fittings, fasteners and valve trim that can tumble freely without damage. | Part-on-part contact is unavoidable, and fine threads, sealing lips and thin diaphragms are poor candidates. |
| Tub vibrator | Long parts, tube spools, chute sections and small vessels that a bowl cannot accept, with the part repositioned as needed. | Coverage depends on how the part sits in the media mass, so banding and shadow zones are common without a planned fixture. |
| Magnetic finishing machine | Small precise parts and short internal features such as slots, small bores and blind recesses. | Part size and surface area are limited, large panels and long tubes are out of scope, and it will not dress a weld cap. |
| Vibratory finishing machine, bowl type | Edge and weld-toe blending plus surface refinement on mid-sized parts, with a visible load and adjustable energy. | Chamber geometry caps part size, and the inside of a long tube or a narrow crevice stays out of reach. |
Media that leaves the chamber with the parts is a defect, not a housekeeping issue, so separation is designed rather than improvised. Screens sized below the smallest medium and above the largest acceptable chip, magnetic separators for steel media, and a counted retrieval step for any feature that can trap a piece all belong in the plan. Media wear management is the other half: as ceramic wears the load loses cut, so a schedule for top-up, screening out fines and removing broken pieces keeps the process from drifting. Compound carryover into threads, gasket grooves and tube ends is controlled by rinse volume, rinse water quality, orientation while draining and drying. Sludge and spent compound disposal is a production cost and a housekeeping discipline that should be costed before a line is specified.

| Media | Best fit | Watch out for |
|---|---|---|
| Ceramic media, angle-cut triangles | Heavier weld-zone refinement and edge blending on 304 and 316L parts where a corner or a toe line has to be reached. | Wears down and changes its effective size class, produces sludge, and can over-round a thin edge or a soft detail. |
| Dry media, walnut shell and corn cob | Light dry burnishing and cosmetic refinement where retained water in a crevice or assembly is a problem. | Generates dust requiring extraction, removes no oxide, and leaves a surface character different from a wet abrasive cycle. |
| Plastic media, cones and triangles | Gentle edge blending and cosmetic refinement on softer non-ferrous fittings, thin sections and delicate parts. | Cannot remove heat tint, mill scale or a weld cap, so it must follow the operation that does that work. |
| Liquid compound, abrasive cleaning slurry family | Cleaning, descaling and fine abrasive work through the cycle, with dosing and flow matched to the load and the alloy. | Chloride content and pH matter on stainless, foam can cushion the cut, and residue left in a crevice becomes a later defect. |
Removing material always changes the part, and the change is not always wanted. A weld toe can be rounded past the radius the drawing implies, a sealing lip can lose its bite, a gasket seat can dish enough to leak, and a thin tank panel can deflect under a heavy load. Media size class and density drive this: a large dense piece on a soft detail rounds it quickly, while a small light piece barely touches it. Detection uses an optical comparator or radius gauge on edges, a flatness check on sealing faces, and dimensional measurement of any feature that carries a tolerance. Dye penetrant or a visual check finds an undercut created by over-grinding a weld cap. Thin-wall parts deserve measurement before and after, because distortion in a small load only worsens at production fill levels.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| A shiny but burnished surface with intact oxide beneath it | Abrasive media smearing the oxide instead of cutting through it, often where a cleaning compound was relied on to do the cutting. | Examine the transition zone rather than the cap, compare a mechanically worked area with a freshly ground control area, and cross-section one sample part under magnification. |
| Rust bloom or free-iron staining appearing after finishing | Carbon steel brushes, iron-bearing media, shared racks or contaminated rinse water depositing free iron on a 304 or 316L surface. | Run a ferroxyl-type test or the buyer's own equivalent at agreed locations including crevices and internal surfaces, after rinsing and drying, and record the result with the batch. |
| Edge or weld toe rounded beyond the specified limit | Dense or large media running too long at high energy, or a part left free to tumble when it should have been fixtured. | Measure edges with an optical comparator or radius gauge and compare with the drawing limit, and measure a weld toe before and after the cycle on the same part. |
| Gasket seat or sealing face dished so it no longer seals | Over-finishing a machined face, part-on-part contact in an unseparated load, or media hammering a face that should have been masked. | Check flatness of the sealing face with a straight edge, a feeler gauge or a surface plate before and after, and confirm against the sealing requirement the buyer's specification states. |
Fukuoka City is the economic core of Fukuoka Prefecture on Kyushu's north coast, and the prefecture's industrial policy is organised around two formally designated clusters: it has published regional industrial cluster plans for the semiconductor field and the advanced-mobility field under the national Regional Future Strategy, presented as promoting a total of JPY 600 billion of investment, and it maintains an annual map and database of automotive and car-electronics suppliers that listed 1,251 companies across Kyushu in December 2025, 647 of them in Fukuoka Prefecture. The city promotes hydrogen-related industry through its Hydrogen Leader City Project, and states that it opened a hydrogen station producing hydrogen from municipal sewage biogas for fuel-cell vehicles in 2015, which it describes as a world first.
The nearest part of that base to this brief is semiconductor: Fukuoka Prefecture has drawn up a regional industrial cluster plan for the semiconductor field under the national Regional Future Strategy, announced together with a plan for the advanced-mobility field.
Automotive and car-electronics suppliers in the prefecture machine metal parts and housings where burrs and edge condition affect fit, electrical contact and coating adhesion, so deburring and edge control sit on the normal production route rather than in rework. Semiconductor-related equipment work adds a cleanliness requirement, and the city's hydrogen and environmental-equipment activity adds valve, manifold and plate components whose sealing faces depend on surface finish.
For a Fukuoka-area semiconductor-equipment or automotive supplier the first question is which specification governs the feature in question - a JIS or customer-drawing callout for edge condition and surface roughness on a sealing face, an electrical contact or a cosmetic surface - because that decides whether a vibratory or centrifugal barrel process, a disc finishing machine, or a scoped media-and-compound sample trial is the right starting point.
Freight context: 博多港 (Port of Hakata), including the Island City container terminal, 博多港 中央ふ頭 (Chuo Pier). The city's port pages state that Hakata Port is the sea gateway for Kyushu and western Japan and that about 910,000 TEU of international maritime containers were handled in 2025 (Reiwa 7), with Island City and Chuo Pier serving as logistics gateways. Hakata Port is therefore the practical point of entry for incoming finishing machines and for outbound sample parts.
Documentation and technical communication are Japanese-language in practice: JISC states that the documents submitted for JIS certification-body accreditation must be written in Japanese, and drawings, inspection sheets and purchase specifications from Japanese buyers are normally issued in Japanese. Import declarations are filed in triplicate and importers commonly use licensed customs brokers, so the commercial invoice, packing list and origin documents must be complete and consistent with the declared commodity code. As general industry practice in Japan, industrial buyers qualify a supplier on documentation, quality-management evidence and a defined inspection standard before volume orders, and expect a named Japanese-speaking contact for technical and commercial follow-up.
Chinese industrial machinery entering Japan is classified under the Customs Tariff Law, whose harmonised schedule sets the classification and the General Rate; the Temporary Tariff Measures Law sets a Temporary Rate for certain products, and where the WTO rate or an EPA rate for the goods is lower, that lower rate is applied. The applied rate therefore depends on the exact commodity code, and on whether an economic partnership agreement covers the goods and their origin, so a landed-cost figure has to be confirmed against the specific machine before it is quoted. Japan Customs' monthly country table for August 2026 records exports to China of 1,809,133 million yen and imports from China of 2,361,239 million yen, the largest single-country line in the Asian table, with imports from China up 22.5 per cent year on year.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Acceptance has to exist before finishing begins, otherwise every batch becomes a negotiation about appearance. Write the requirement per zone: which surfaces are product-contact, what roughness band applies to each, which edges keep a radius, which faces stay flat, what cleanliness and residue condition is required, and which features come back untouched. Name the inspection method and instrument for each requirement and the person who accepts or rejects. Where a requirement comes from a design code or a customer specification, the buyer's own quality function states and verifies it. A first article fully inspected and retained as the physical reference removes most later argument, particularly on welds, where a kept part says far more than a written description. Re-confirm the requirement whenever drawing, material or upstream fabrication changes.
A trial load is small, hand-observed and run by someone who knows what is being tested; a producing line is larger, repeatable and operated by whoever is on shift. That gap is where results are lost. Fix the load fill level, the part-to-media ratio, the fixture positions and the cycle time as written settings, then check that a shift operator can reproduce them. Expect drift from media wear, compound concentration, water quality and part mix, and put a check in place that detects it before a batch is finished rather than after. Mixed-size loads, changes in upstream welding and new material heats are all reasons to re-verify. Where a finish depends on a hand operation, variation between operators becomes part of process capability and has to be managed, not assumed away.
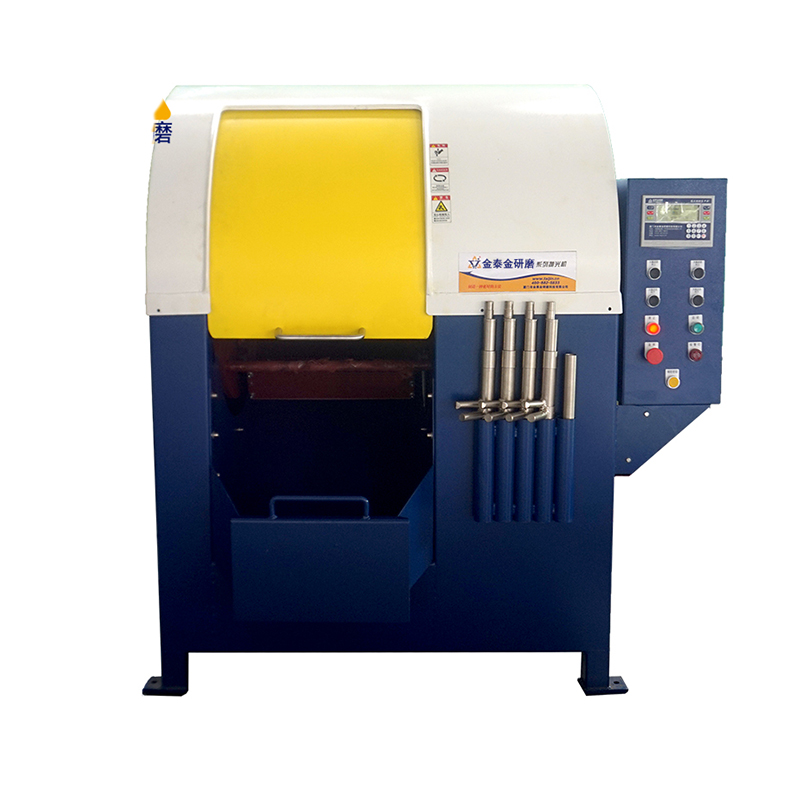

Heat tint is oxide, so it is removed by cut rather than by cleaning. Ceramic media with an aggressive shape and bonding, or a grinding stage followed by refinement, are the usual mechanical answers on accessible weld zones. The limit is reach: a tint line that runs into a toe, a crevice or a small bore may survive a cycle that polishes the cap, which is why the toe should be inspected rather than judged by the shine of the weld face. Media size, shape and cycle energy must suit the oxide thickness. A trial on your own parts shows what was removed on the geometry tested.
Specify it with a location, a cut-off and a direction, not as a single number. Mark the measurement points on the drawing and say whether each sits on base metal, a dressed weld or the heat-affected zone, because those are different surfaces. State the cut-off and evaluation length, and require readings across the lay at each point rather than one convenient traverse. Also state what Ra is not being asked to prove: it does not describe a crevice, an oxide film, embedded contamination or an edge condition. A buyer in Japan should record the instrument and the calibration specimen on every report.
No. Mechanical finishing removes material and can strip oxide and free iron from the surfaces it touches, but it does not restore a passive film and it does not perform a chemical passivation step. Passivation, whether by a paste, a bath or an electrochemical process, is a separate operation with its own method and verification that belongs to your own specification and supply chain. Mechanical work can leave a surface in better or worse condition for that step, which is one reason media and compound selection on 316L should consider what comes afterwards rather than only the finish you see at the end of the cycle.
Use Fukuoka, Japan as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Japanese buyers work to JIS (Japanese Industrial Standards), enacted and revised under the Industrial Standardization Act and administered through the Japanese Industrial Standards Committee (JISC) at METI; the JISC site publishes JIS enactments and revisions while allowing JIS documents to be read but not printed. Surface-finish and material requirements are normally cited on drawings as JIS or as customer-specific specifications, and management-system certification to ISO 9001 is commonly requested as general industry practice.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Fukuoka.
The buyer must deburr the drilled holes and the thread start while keeping the internal channel clear of media.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0874; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0874 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
