An industrial machinery buyer in Marseille, France has a cast aluminium gearbox end cover whose machined o-ring groove must hold tolerance while the visible face is brightened. The offer here is cross-border equipment, media and compounds plus a free sample trial: representative parts ship to Xiamen and come back with observations and a proposed process direction, not a guarantee. This brief is written for a buyer in Marseille working on industrial machinery; it describes equipment, media and a scoped sample review, not a local polishing service.
Can available media actually reach the geometry, and what finish is realistic in the recesses and internal features it cannot reach?
Which faces must reach a mirror and which only need to be clean and uniform, and how is each one judged?
What batch size, part mix and media maintenance routine will production really run, and does the trial describe that condition?
Every mirror sequence removes metal, and the removal is rarely uniform across a large face. Datum pads, dowel registers, bearing seats and seal lands carry assembly geometry, so measure them before finishing and agree a dimensional and flatness allowance. Where an allowance is tight, mask the feature, finish around it by hand, or plan a light final lapping pass that keeps the face flat. A part that looks correct but has lost flatness on a mounting face will not assemble squarely, and a curved cover panel shows a distorted reflection after only a few hundredths of a millimetre of uneven stock removal. Record incoming values with the same instruments that will accept the finished part, at the same marked locations.
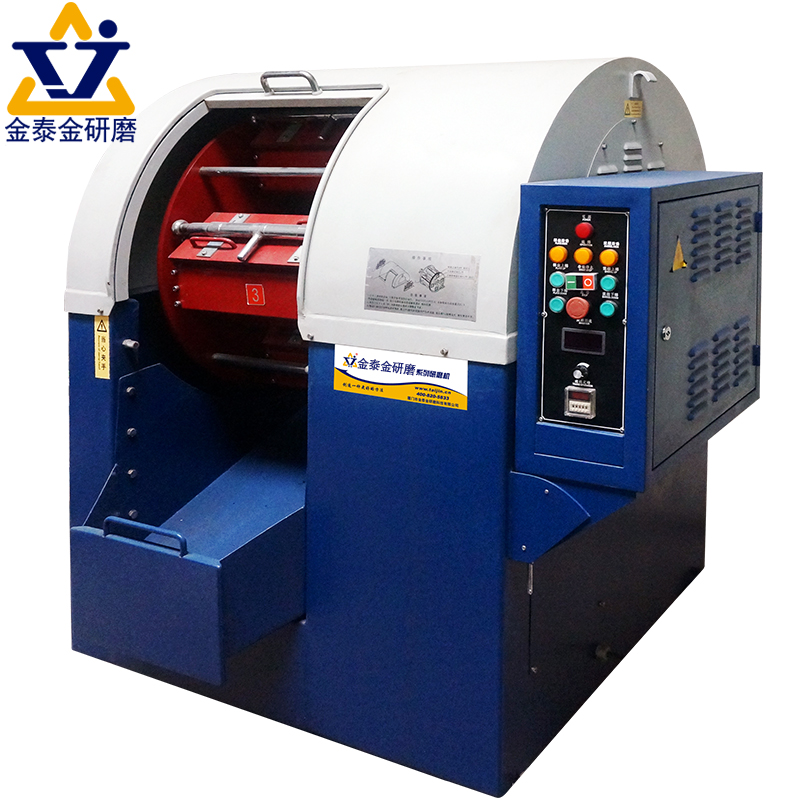
Rotary barrels work by sliding contact and suit parts that tolerate tumbling, giving a dense, uniform colour on small hardware. They cannot process anything longer than the barrel diagonal, so long shafts, extrusions and frame members belong in a tub vibrator, where a part can pass through the mass without being folded. Slender parts need support or careful load balancing, because the same energy that brightens a shaft can bow it or nick it against a neighbour. Barrel and tub routes reach some external areas a bowl cannot, such as a long groove, but they are poor at bores running parallel to the long axis. Verify straightness and roundness after the cycle, not only appearance.
| Machine route | Where it fits | What it will not do |
|---|---|---|
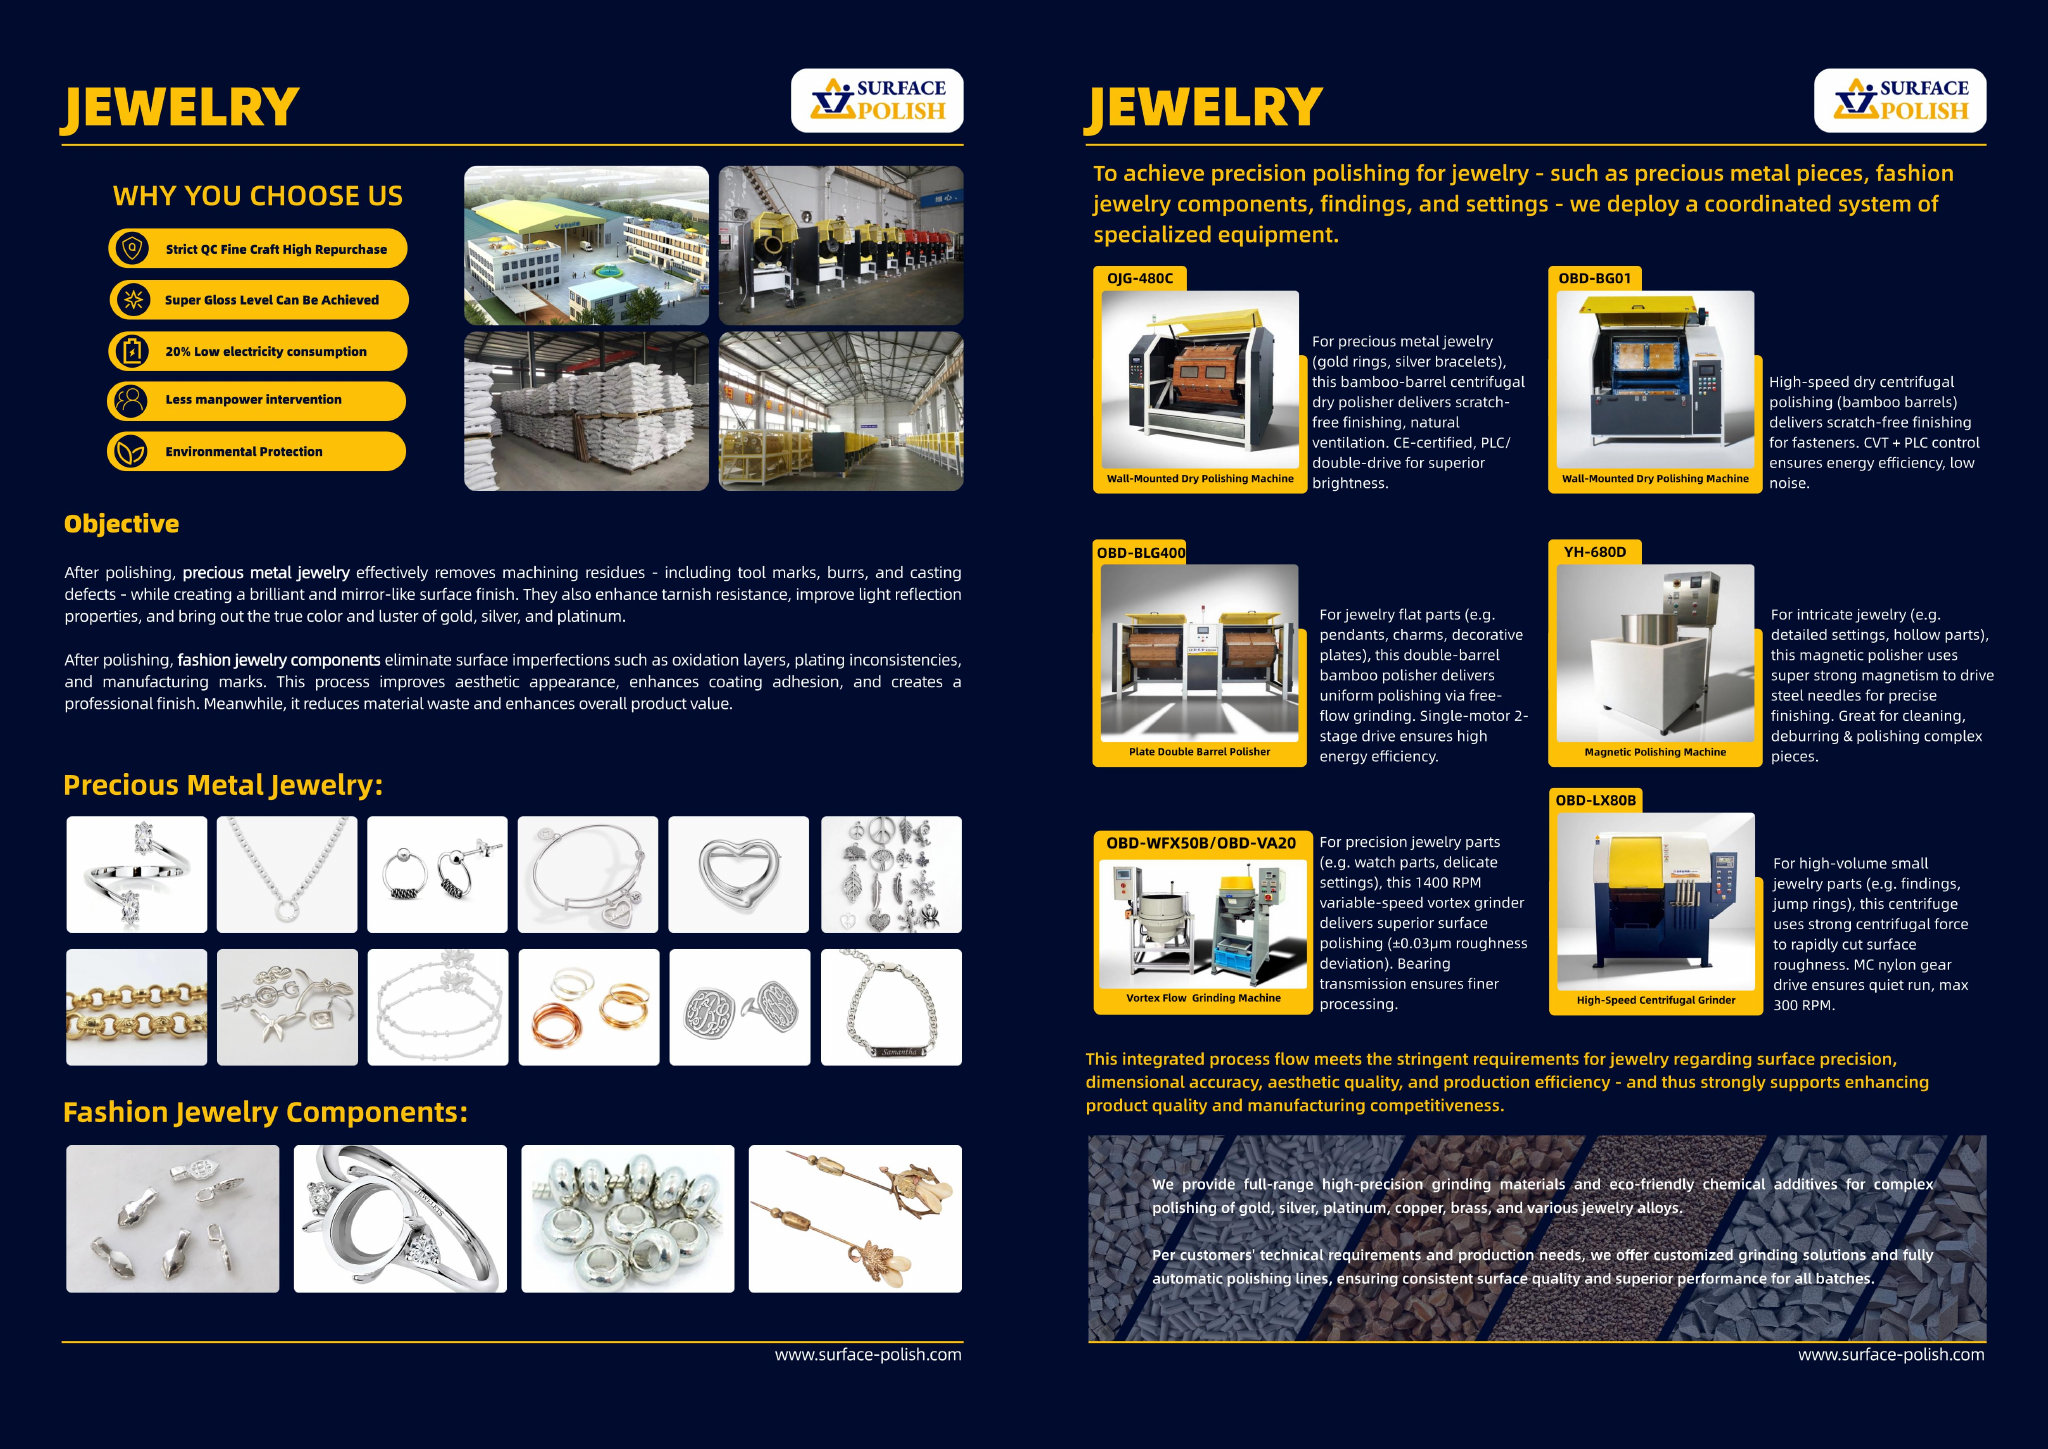
| Grinding finishing machine | The heavier stock-removal stage before a mirror sequence, cutting back grinding damage, scale and recast layers on robust parts. | High removal also rounds edges and can work harden or distort thin sections, so it needs a defined depth target and a sample check. |
| Vibratory finishing machine (bowl or tub) | Cut-to-colour sequences on rigid, mostly open parts such as housings, covers, brackets and frames, with adjustable energy and no fixturing. | Cannot present media uniformly into pockets with narrow mouths or deep internal bores, and broad flat faces finish more slowly than edges. |
| Barrel finishing machine / rotary barrel tumbler | Dense, uniform colour on small hardware that tolerates sliding contact, especially with steel media for a burnished appearance. | Nothing longer than the barrel diagonal can be processed, and slender parts can bend or nick against neighbours in the load. |
| Magnetic finishing machine | Refinement and edge conditioning of small precise parts with internal edges, cross holes and fine detail that media cannot enter. | Working envelope and part mass restrict size, removal is very small, and coverage falls off wherever the field cannot drive the pins. |
Media handling is where good sequences are quietly spoiled. Parts must be separated from the charge completely, using screens or a separation deck matched to the smallest media in use, with a counted charge so losses stay visible. Screen out worn media on a schedule and top the charge up, because a blend of very small and original-size media finishes unevenly. Keep steel and ceramic media in dedicated machines or dedicated charges: a few steel pieces in a ceramic load leave bright speckle and iron pickup on stainless, while ceramic fines in a steel charge cause sleeks. Store dry media sealed against moisture, and clean the machine between material families when switching from ferrous to stainless work.

| Media | Best fit | Watch out for |
|---|---|---|
| Hardened steel media, balls and shaped shot | Bright burnishing of stainless and hardened steel, and the final wet lustre stage where a dense medium can peen a surface smooth. | Can transfer iron and rust to stainless, dents soft or thin parts, and must be kept in a dedicated charge away from ceramic media. |
| Coarse ceramic angle-cut cylinders or triangles | First cut stage on rigid parts with open faces, removing grinding or machining damage on cast iron, steel and stainless before refinement. | Leaves a deep pattern the next stage must fully erase, chips thin edges, and its wear debris carries fine abrasive into later stages if the charge is not screened. |
| Dry media - corn cob | Softer dry lustre and drying steps, absorbent polishing of small parts, and light work on brass, aluminium and plated-look surfaces. | Breaks down faster than walnut shell and must be replaced regularly; it removes almost no material and cannot correct a surface defect. |
| Small high-density ceramic spheres or ovals | Colour and pre-lustre stages where a uniform, soft-looking finish matters more than stock removal, including curved and contoured faces. | Very slow cut, easily lost through screens sized for larger media, and ineffective in deep recesses because it cannot reach or press against the surface. |
Beyond a certain point, more polishing makes a surface worse. Excess cycle time or contact pressure rolls metal over instead of cutting it, burying abrasive and debris under a smeared skin that looks bright until it is disturbed. On dry or high-speed operations, friction raises local temperature enough to tint the surface and soften a hardened layer, and thin sections can distort from the heat. High-energy routes add part-on-part impingement, leaving nicks and small dents that polishing cannot remove. Watch for a bright surface that dulls or streaks when wiped with a clean cloth, for colour variation near edges where contact is highest, and for dimensional or flatness change. The remedy is a shorter or gentler cycle, better cooling and a real end point instead of a longer run.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Media lodged in blind holes, slots, undercuts or threaded features | Media size too close to the opening, a slot or cavity that traps the charge, or no defined retrieval step before rinsing and drying. | Reconcile a counted media charge before and after the cycle, borescope each cavity at an agreed angle, and pin or thread gauge the features the charge could enter. |
| Compound residue film, water spots or a dull bloom after drying | Incomplete rinsing, hard or contaminated rinse water, a dose above target, or drying that leaves a cavity to bleed residue onto the finished face. | Wipe a defined area with a clean white cloth after drying, inspect cavities for bleed-out, and check rinse water hardness or conductivity at the point of use. |
| Dimensional drift or lost flatness on datums, seals and bearing seats | Uneven stock removal across a large or asymmetric face, over-long cycles, or unprotected functional features exposed to the full charge energy. | Measure flatness and critical dimensions with a CMM or surface plate at the same marked points used for the incoming survey, and compare the change against the allowance. |
| Orange peel, a slow wave that distorts the reflected image | Soft or work-hardened surface deformed rather than cut, a heavy cut stage followed by too little refinement, or a dry or buffing stage at high speed with excess pressure. | Reflect a straight edge or fluorescent tube in the face at a shallow angle, compare the shape of the image against a physical master in the same lighting, and repeat at several viewing angles. |
Marseille's industrial identity is inseparable from the port: the Grand Port Maritime de Marseille operates the Fos-sur-Mer industrial-port zone, created by the State in 1964 and described by the port as one of the largest in Europe at 10 000 hectares, concentrating steel, energy and petrochemical plants including ArcelorMittal, Marcegaglia, KEM One, Air Liquide and Covestro, with two methane terminals and two wind farms, and the port is adding new industrial projects (H4 sustainable aviation fuel, Gravithy direct-reduced iron, a Marcegaglia electric steel plant, Neocarb e-fuels). In the commune, INSEE counted 31 646 establishments at the end of 2024, 4,2 % of them industrial, and 10,4 % in construction - the highest construction share of the ten cities studied. Marseille is also the Mediterranean's leading ship-repair centre, with ten repair forms in the Marseille basins and Forme 10, which the port describes as the third largest ship-repair dock in the world.
For this brief the relevant part of that base is machinery: The port's industry page records steel and metal processing capacity on site, including Marcegaglia's 2024 takeover of the former Ascometal site for a EUR 600 million electric steelworks project targeting 2,2 million tonnes of finished products.
Fos and the Marseille basins are a heavy-metal environment: steel strip, tube and long products, welded structures, pumps, valves and process equipment need scale and heat-tint removal, weld dressing and controlled surface finish for coating adhesion and corrosion resistance. Ship repair adds a second, different surface problem - large-area preparation, weld seam dressing on hulls and tanks, and cleanliness before coating - carried out under tight dry-docking schedules. Both environments put a premium on equipment that is robust, dust- and slurry-tolerant, and simple to maintain, rather than on fine cosmetic polishing.
A buyer in Marseille should settle whether the finishing cell will work on large welded structures and repair work with variable geometry, or on repeatable machined components, because that determines whether the shop needs a flexible manual/barrel process with forgiving media or a tightly controlled, documented series process.
Freight context: Grand Port Maritime de Marseille (Marseille and Fos-sur-Mer), Marseille Provence Airport, Fos container and ro-ro terminals. Marseille-Fos is the Mediterranean deep-sea gateway for southern France, with container traffic up 9 % in 2024 to 1,45 MEVP and revenue of EUR 224,5 million; the port is multimodal (maritime, river, rail, road) and handles heavy and oversized industrial cargo. For a finishing-equipment buyer this is the natural discharge port for containerised machines and the natural export route for sample parts, with Fos better suited to heavy lifts than the city basins.
France applies the EU common commercial policy, so industrial machinery arriving from China enters under the Union Customs Code and the Common Customs Tariff rather than under any bilateral French regime; the EU has no free-trade agreement with China, so no preferential duty rate applies and normal third-country duties are due on the customs value. Importers classify the machine in the tariff nomenclature and lodge a customs declaration; French Customs publishes the common and national tariff through its RITA online service and states that three notions are fundamental: the tariff classification of the product, its origin or destination, and the value of the goods.
The French national standards body is AFNOR (Association francaise de normalisation), which coordinates French participation in standardisation and publishes the NF and NF EN standards that transpose ISO and CEN work; AFNOR also runs the certification activity attached to many of those standards. A French buyer of finishing equipment would normally reference ISO/NF EN surface-texture standards for roughness and profile parameters, ISO/NF EN cleanliness or residue specifications for critical parts, and management-system or sector schemes such as ISO 9001, IATF 16949 for automotive and EN 9100 for aerospace.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A mirror surface changes with the observer, so viewing conditions belong in the specification. Agree the light source type, the distance and angle, the viewing direction, and whether inspection happens in a booth or in the machine environment. A physical master approved by both parties, kept clean and stored protected, is more reliable than a photograph; photographs of reflective parts mostly record the light source. Define what is acceptable, such as a limited number of fine marks, a haze limit inside a stated area, and no visible peel, and state where the standard does not apply, for instance inside a recess that will be painted or covered. Re-confirm the master whenever the sequence or media family changes.
A trial runs a small, hand-selected load on equipment that has just been set up. Production runs mixed batches on a media charge of unknown age, with transfer time between stages, variable rinse quality, operators on different shifts, and parts arriving with different incoming damage. Plan a defined pilot batch that uses the intended line configuration and a full first-article inspection, then compare it with the trial observations before committing volume. Watch the variables that scale badly: drying time in a humid season, water chemistry, load density and the handling between cut, colour and lustre stages. Treat the pilot as the real test of stability and keep its settings record with the parts so any drift can be traced.

Each stage removes the pattern left by the one before it. A coarse cut removes grinding or machining damage, a refinement stage erases the cut pattern, a colour stage removes the refinement marks, and a lustre stage produces the final reflected image. Skipping or shortening a stage leaves a ghost of it in the surface that finer work only polishes around. Because the steps use different media, compounds and often different machines, a line is planned as a route with a defined finish at each stage, including the rinses and drying between them.
A mirror surface is damaged by contact, so handling begins before the parts leave the machine. Rinse and dry thoroughly to remove compound and fines, because residue trapped in a cavity bleeds out later and a damp surface can stain stainless. Then protect: interleave or sleeve faces that will touch, keep parts separated in trays, avoid sliding them across each other, and use gloves or a clean cloth when they are picked up. Agree packaging with the buyer, including whether parts travel individually wrapped, and inspect on arrival for marks that occurred in transit.
Ra alone is not enough. It is an average over a defined cutoff length, so a surface with a low Ra can still show waviness, orange peel or directional marks that dominate what a viewer sees, while a slightly rougher surface can look brighter if it scatters light evenly. Specify the measurement setup as well as the value, and where appearance is what matters, add a reflectance or gloss reading at a stated angle together with a physical master and viewing conditions. For Marseille buyers working to a functional surface requirement, specify the profile and the appearance requirement separately.
Use Marseille, France as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Marseille buyer would reference ISO/NF EN surface-texture standards for finish, the EN 1090 and pressure-equipment regimes for welded steel structures and vessels, and coating-system specifications where surface preparation precedes painting; marine and offshore work is normally governed by classification-society and owner specifications on top of the ISO 9001 baseline. Material conformity certificates and traceability are standard requirements in the steel and petrochemical supply chain.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Marseille.
The buyer needs the outer face brightened for appearance while the sealing groove holds its tolerance and the porosity stops telegraphing through the finish.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0539; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0539 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
