A buyer in Mumbai, India building industrial machinery needs a machine-tool enclosure cover plate brightened to a consistent reflective face without losing flatness at the flange or trapping media in the insert threads. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial, returning the tested parts with observations and a proposed media, compound and cycle direction. This brief is written for a buyer in Mumbai working on industrial machinery; it describes equipment, media and a scoped sample review, not a local polishing service.
Can available media actually reach the geometry, and what finish is realistic in the recesses and internal features it cannot reach?
What is the substrate condition - cast, welded, forged or machined - and which defects already in it will become visible once the metal is smooth?
What batch size, part mix and media maintenance routine will production really run, and does the trial describe that condition?
Bright polishing rounds edges, and the more energy and time the sequence needs, the more rounding appears. Some edges are cosmetic and rounding is welcome; others define function, such as a scraper edge on a machine-tool slideway, a knife edge on a metering blade, a thread start, or the lapped lip of a valve seat. Mark those features on the drawing and state a maximum edge radius or a no-touch zone before media is selected. Inspection can use radius gauges, a cast impression or an optical comparator against the incoming edge form. Where a crisp edge and a bright face conflict, the practical order is to finish the face first and restore the edge with a controlled hand operation, or to accept a slightly duller face that preserves the edge.
Magnetic finishing drives small pins or needles with a moving magnetic field, so the abrasive follows internal edges, cross holes, slots and fine detail that no tumbling medium of usable size can enter. It is the practical route for small precise parts such as valve spools, small gears, nozzle bodies and instrument components where a bright edge or a cleaned intersection matters. It removes very little material, so it is a refinement and edge-conditioning step rather than a way to erase coarse grinding marks. Working envelope and part mass are the main limits: large faces and heavy parts do not fit, and the effect falls off where the field cannot drive the pins. Check coverage on a sample with magnification and a borescope.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Barrel finishing machine / rotary barrel tumbler | Dense, uniform colour on small hardware that tolerates sliding contact, especially with steel media for a burnished appearance. | Nothing longer than the barrel diagonal can be processed, and slender parts can bend or nick against neighbours in the load. |
| Vibratory finishing machine (bowl or tub) | Cut-to-colour sequences on rigid, mostly open parts such as housings, covers, brackets and frames, with adjustable energy and no fixturing. | Cannot present media uniformly into pockets with narrow mouths or deep internal bores, and broad flat faces finish more slowly than edges. |
| Tub vibrator | Long and large parts such as shafts, extrusions and frame members that cannot be folded into a barrel, including external grooves. | Poor at bores running parallel to the long axis, and slender parts still need support or balanced loading to hold straightness. |
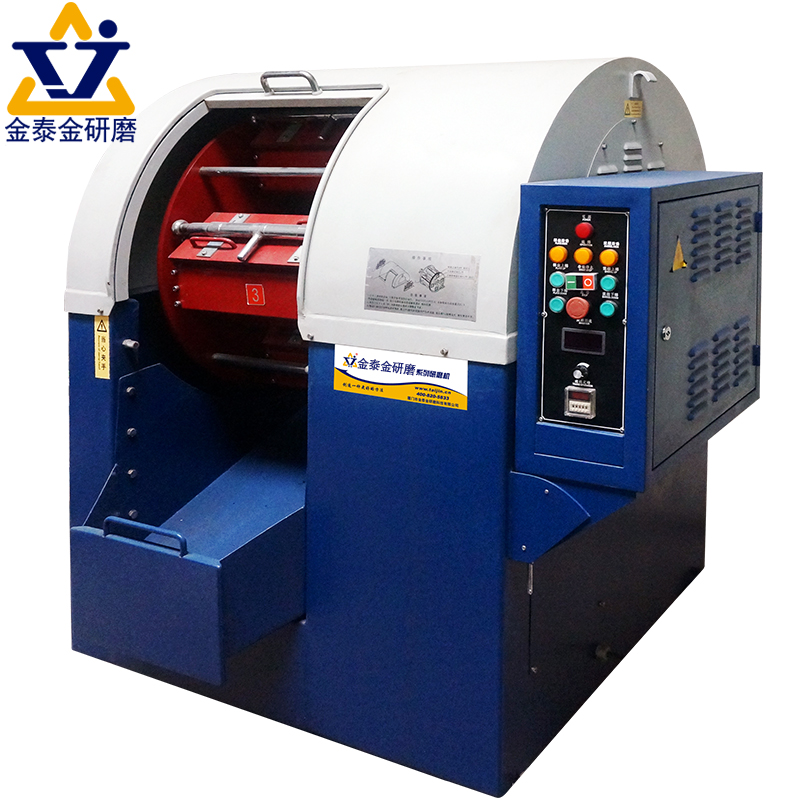
| Grinding finishing machine | The heavier stock-removal stage before a mirror sequence, cutting back grinding damage, scale and recast layers on robust parts. | High removal also rounds edges and can work harden or distort thin sections, so it needs a defined depth target and a sample check. |
Compound concentration is a process variable that drifts. Dosing on a timer is convenient but ignores carry-out, evaporation and the fines load, so a batch that starts at target can finish well above or below it. Meter dose against water flow, check pH and, where available, conductivity at the start and end of a cycle, and record those values with the batch. Water quality shapes the final image: hard water leaves mineral spots that read as haze, and high chloride or iron content can stain stainless during rinsing. The rinse after each stage deserves the same control as the finishing stage, with enough volume and flow to remove compound and loose fines before the part dries, because dried residue is far harder to remove without disturbing the finish.

| Media | Best fit | Watch out for |
|---|---|---|
| Small high-density ceramic spheres or ovals | Colour and pre-lustre stages where a uniform, soft-looking finish matters more than stock removal, including curved and contoured faces. | Very slow cut, easily lost through screens sized for larger media, and ineffective in deep recesses because it cannot reach or press against the surface. |
| Medium ceramic triangles or angle-cut shapes | Blending, edge conditioning and the refinement step that removes the coarse cut pattern on housings, brackets, covers and frames. | Media that cannot enter a slot or recess leaves those areas at a different finish, so those faces need a separate operation or a stated lower standard. |
| Dry media - corn cob | Softer dry lustre and drying steps, absorbent polishing of small parts, and light work on brass, aluminium and plated-look surfaces. | Breaks down faster than walnut shell and must be replaced regularly; it removes almost no material and cannot correct a surface defect. |
| Plastic or polyester media | Gentle processing of aluminium, brass, copper and thin panels where metal smearing, nicks and distortion must be avoided. | Low density gives little contact force, so cycles run long and heavy grinding marks may survive; plastic also wears quickly and can float above the working mass. |
Beyond a certain point, more polishing makes a surface worse. Excess cycle time or contact pressure rolls metal over instead of cutting it, burying abrasive and debris under a smeared skin that looks bright until it is disturbed. On dry or high-speed operations, friction raises local temperature enough to tint the surface and soften a hardened layer, and thin sections can distort from the heat. High-energy routes add part-on-part impingement, leaving nicks and small dents that polishing cannot remove. Watch for a bright surface that dulls or streaks when wiped with a clean cloth, for colour variation near edges where contact is highest, and for dimensional or flatness change. The remedy is a shorter or gentler cycle, better cooling and a real end point instead of a longer run.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Smearing or a rolled surface with abrasive and debris buried in it | Excessive cycle time or contact pressure, insufficient compound lubricity, or a final stage run at energy the material cannot absorb without deforming. | Wipe a defined area with a clean white cloth and look for streaks or dulling, then examine at magnification and compare microhardness or etch response against an unmachined reference. |
| Haze, a general loss of image clarity with no directional pattern | Worn media shedding an oversized fine fraction, agglomerated abrasive in the compound line, or fine grit carried into a late stage from screens, machine walls or a shared rinse. | View under raking light at low magnification against a master, then trace the pattern by machine and by rinse line to separate a charge problem from a rinse or transfer problem. |
| Media lodged in blind holes, slots, undercuts or threaded features | Media size too close to the opening, a slot or cavity that traps the charge, or no defined retrieval step before rinsing and drying. | Reconcile a counted media charge before and after the cycle, borescope each cavity at an agreed angle, and pin or thread gauge the features the charge could enter. |
| Edge radius beyond the allowed limit | A cut stage longer or more energetic than the edge allowance supports, insufficient masking or fixturing, or a sequence repeated to remove a defect and run past the edge allowance. | Measure with a radius gauge, a cast impression or an optical comparator at the marked edges, and compare against the edge form and dimensions recorded before finishing. |
Mumbai is the capital and the largest industrial and commercial centre of Maharashtra, the state Invest India records as contributing 13.5% of India's nominal GDP in FY 2023-24 and roughly 31% of the country's total FDI inflows (s1). The city is the base of the Bombay Chamber of Commerce and Industry, founded in 1836, which describes itself as located in Mumbai, the country's industrial, financial and commercial capital (s3). Industrial land across the state is organised through the Maharashtra Industrial Development Corporation, which has developed 289-292 industrial areas over more than 1.0 lakh hectares, including sector-specific parks for food processing, textiles, IT and biotechnology (s2). The region's freight system rests on the state's two major ports, with JNPT and Vadhvan port connectivity expanding, together with the Navi Mumbai International Airport that came into operation in 2025 (s2).
For this brief the relevant part of that base is machinery: India's capital goods sector accounts for 21.5% of total manufacturing (s5), and the Bombay Chamber's Mumbai membership is dominated by manufacturing and commercial companies, with expanding manufacturing setups named as one of its major current focuses (s3).
The Mumbai region's port, engineering and general manufacturing base generates deburring and surface-finish work on machined and fabricated metal parts, and the harbour and marine cluster adds corrosion-resistant finishing requirements on marine hardware and structural components. Because much of the base is small and medium-sized contract manufacturing feeding larger OEMs, finish consistency, edge condition and cleanliness of the part as delivered to the customer are the practical quality levers rather than the capabilities of a single high-volume line.
A Mumbai buyer should settle whether the requirement is a specified surface roughness and edge condition on a named alloy, or a broader cosmetic finish, because that decides the process (vibratory, barrel or centrifugal), the media type and the cycle time - and whether any BIS obligation attaches to the imported consumable before landed cost is calculated.
Freight context: Jawaharlal Nehru Port (JNPT), Vadhvan Port, Mumbai Port, Navi Mumbai International Airport, Chhatrapati Shivaji Maharaj International Airport. The metropolitan region's container and bulk gateway is the state's major-port complex at JNPT and Vadhvan, with Navi Mumbai International Airport operational since 2025 (s2). Inbound finishing machines and outbound sample parts move through this port and airport pair, so HS classification, the bill of entry and the applicable customs duty are settled at the Nhava Sheva / Navi Mumbai end before inland delivery.
India classifies every imported item in the ITC(HS) schedule, a compilation of codes for all merchandise for export and import whose Schedule I lays down the import policy regime for each item, maintained at 8-digit level under the First Schedule of the Customs Tariff Act, 1975 and aligned at 6 digits with the WCO Harmonized System (c1, c3). Importability is judged by the policy in force on the date of import, and when a policy moves from free to restricted, goods already committed through an irrevocable commercial letter of credit opened before the change can still be imported up to the balance quantity, value and period in that ICLC (c4). Preferential customs treatment is available only through the preferential trade agreements, free trade agreements, CECAs and CEPAs that India notifies and that are in operation (c5), so Chinese-origin industrial machinery is assessed at the applicable rate of the customs tariff rather than under any India-China preferential rate; India's commerce leadership has separately pointed to exports under free trade pacts growing faster than imports (c12). For capital goods specifically, DGFT operates the Export Promotion Capital Goods (EPCG) scheme, whose stated objective is to facilitate import of capital goods for producing quality goods and services (c7), which Indian firms use when they want duty relief on imported plant against an export obligation.
An Importer-Exporter Code (IEC) issued by DGFT is a key business identification number which is mandatory for exports or imports, and since the introduction of GST the IEC number is the same as the PAN of the firm (c6). The post-incorporation clearance list published by Invest India includes the IEC, a Customs- Special Valuation Branch reference and the grant of a Bureau of Indian Standards (BIS) licence, and it names the Central Board of Excise and Customs among the agencies in the framework (c10). The Foreign Trade Policy fixes the mandatory import documents as a bill of lading / airway bill / lorry receipt / railway receipt, a commercial invoice cum packing list and a bill of entry, with additional documents or NOCs possible for goods subject to product-specific compliance (c3); it also states that domestic laws, rules, orders, technical specifications and environmental, safety and health norms applicable to domestically produced goods apply mutatis mutandis to imports unless specifically exempted (c2), which is the basis on which a BIS quality-control order can bite on imported machinery. A landed-cost plan therefore needs the correct ITC(HS) classification and the basic customs duty and IGST that follow from it, plus the IEC, the bill of entry documentation and any BIS licence or registration obligation, and a related-party import can additionally be pulled into special customs valuation.
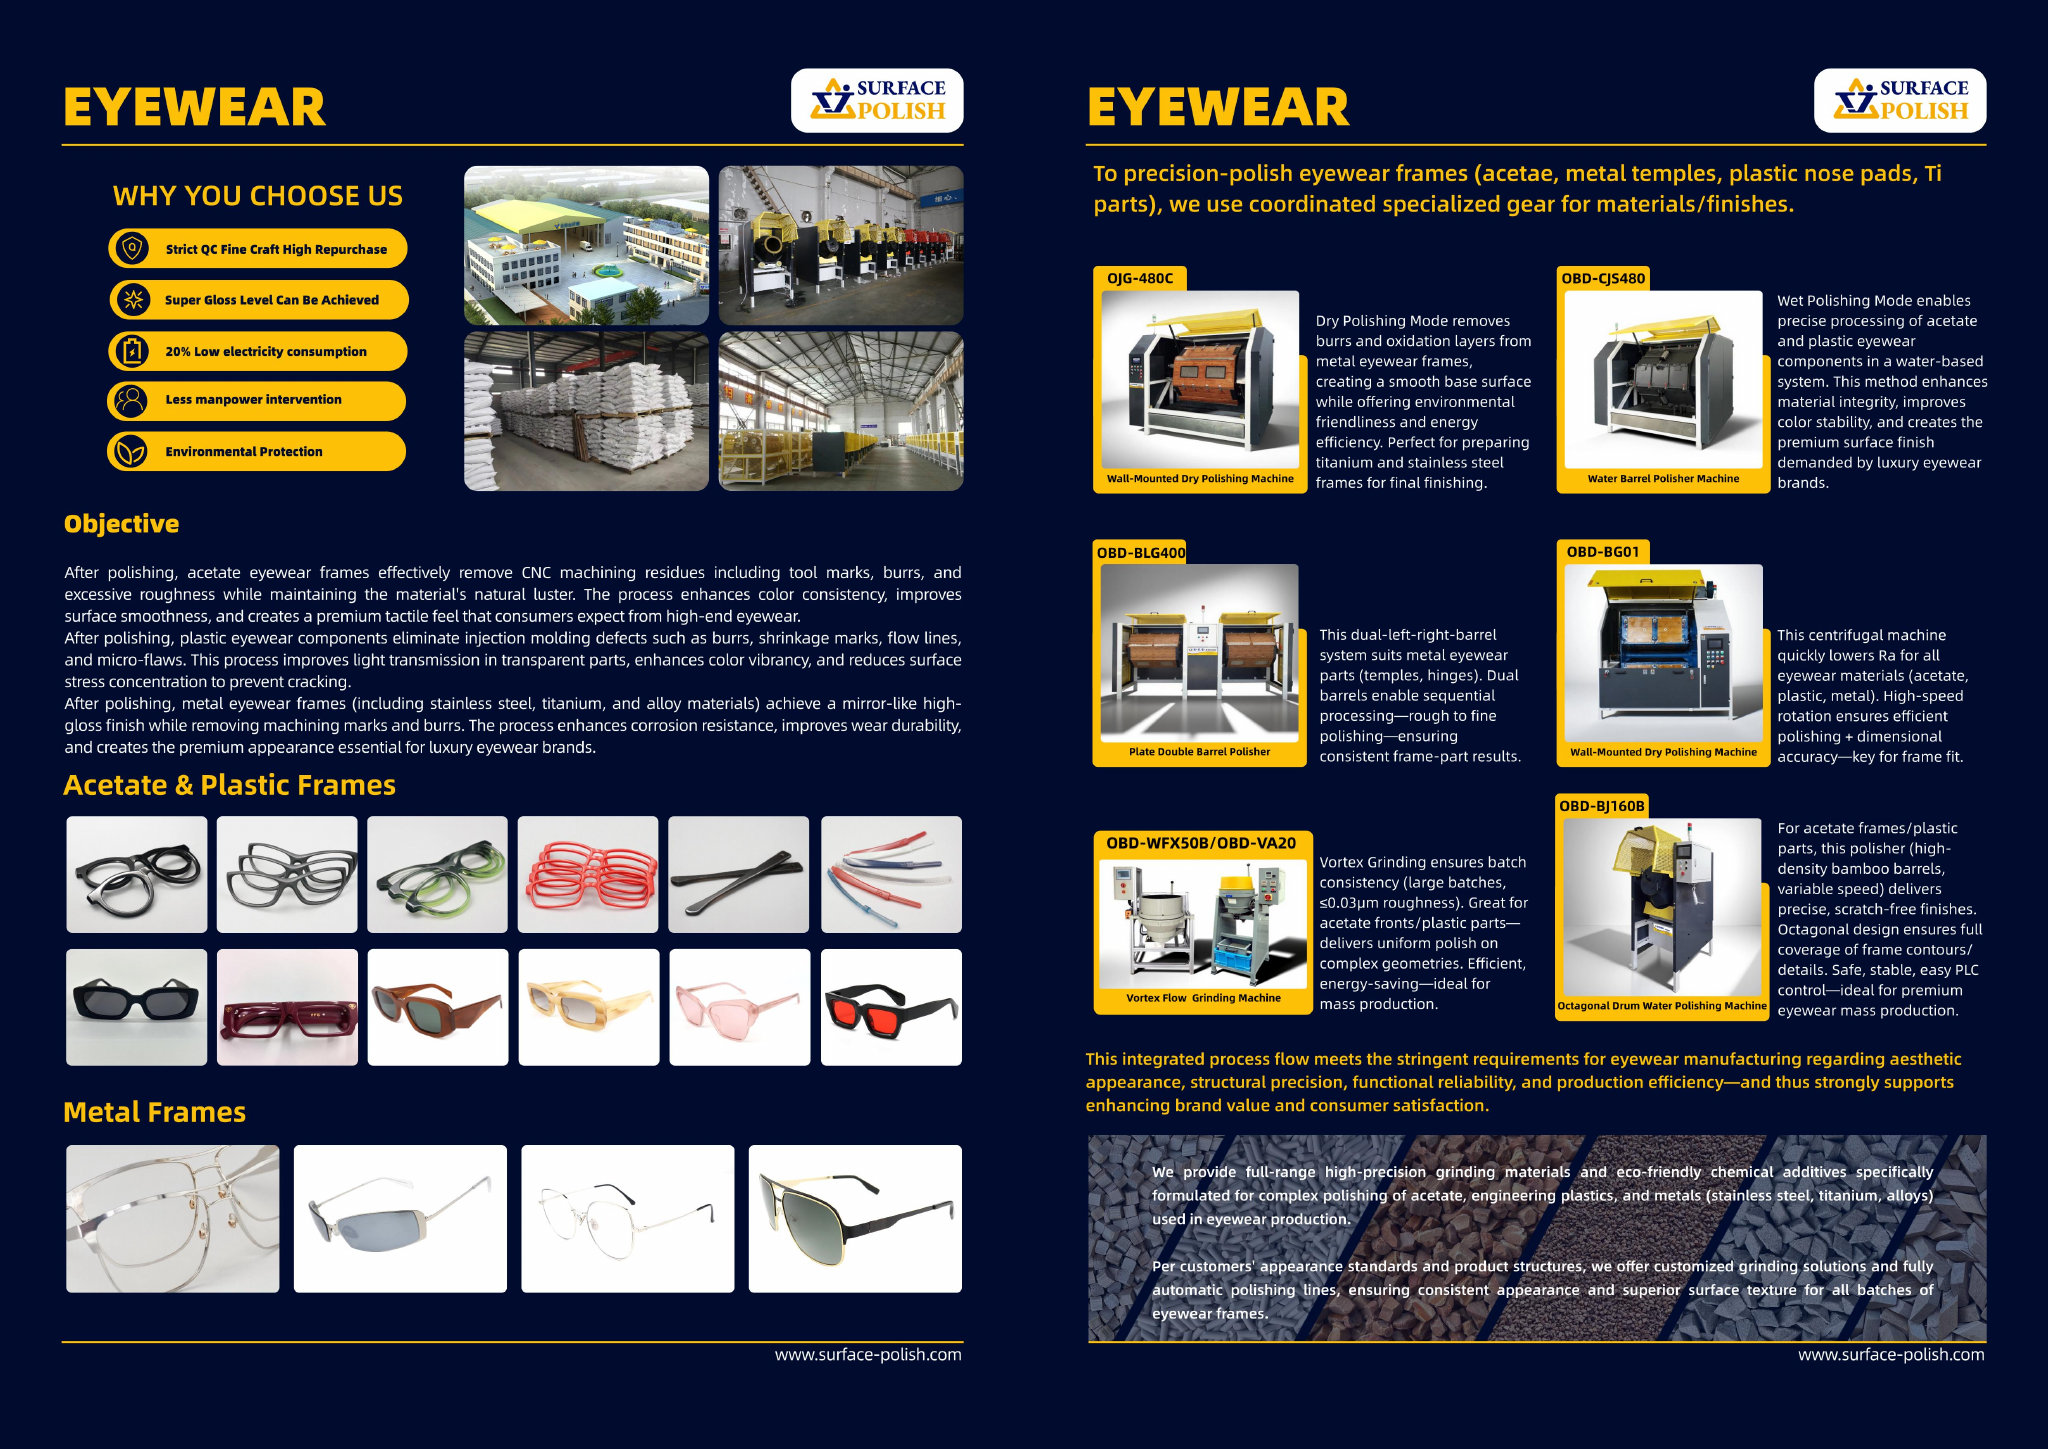
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Cosmetic acceptance is only half a disposition. Measure the dimensions and flatness that assembly depends on, gauge or thread-check features that media could enter or round, and run the functional check the part actually needs, whether that is seal condition, bearing fit, sliding contact, flow or leak. Cleanliness needs its own verification rather than an assumption: flush blind holes and passage intersections, borescope them at an agreed angle, and examine what the flush carries out. Wipe a defined area with a clean white cloth and record what appears, since compound residue and iron pickup often show only after drying. Confirm cleanliness after drying, not before, and record the method so the next batch is judged on the same basis.
A trial reports what was observed on the parts it received, under the settings used. It cannot prove that every casting in a lot will respond the same way, that a worn media charge will behave identically over months, or that the finish satisfies a regulated or safety-critical requirement; those are questions for the buyer's own engineering and quality functions, using their own verification. It also cannot promise a reflectance value, an Ra value, a cycle time, a price or a capacity. Before shipping parts, decide whether a mirror finish is plausible at all: check the substrate for porosity and inclusions, confirm that available media can reach the geometry, and define the acceptance method first. If the requirement cannot be measured or viewed consistently, no trial result will settle it.

Design the charge around the smallest opening rather than the average part. Use media clearly smaller than the hole, or mask and plug the features before the cycle, count the media into and out of the load as a reconciliation, and add a retrieval step with a defined check such as a borescope or pin gauge. For India buyers sending parts for a trial, include the part with the tightest feature so the media class is chosen against real geometry. The small pins used in magnetic finishing embed easily in soft metal, so those features need extra inspection.
Send representative production parts including the thinnest wall, the tightest feature that must stay clear and the worst edge, plus a witness coupon of the same material and condition, a drawing extract covering the finished faces and the acceptance requirement you intend to apply. Label every piece and note its incoming condition with photographs, readings and measurements. The return is the tested parts with observations and a proposed media, compound and cycle direction for the buyer's own evaluation. A trial on parts shipped from India is a comparison, not a qualification, and it establishes no capacity or delivered surface value.
No to both. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and it does not supply or perform electropolishing or operate a plant, branch, dealer or technician service in India or any other market. What is offered is equipment and consumables, a scoped discussion of a finishing line concept, and a free sample trial in which representative parts are shipped to Xiamen and returned with observations and a proposed process direction. Where an electrochemical finish is under consideration, the discussion stays a comparison with a mechanical route.
Use Mumbai, India as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Surface, coating and material specifications for a Mumbai buyer are written against Indian Standards (IS) published by the Bureau of Indian Standards, the National Standards Body of India (s4). Where the machine, media or compound falls under a BIS quality-control order, the licence or registration requirement attaches to the product placed on the Indian market, so the applicable IS number and certification route should be confirmed before the order is placed (s4).
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Mumbai.
The buyer wants a uniform reflective face on the enclosure while keeping the flange flat and the insert threads free of media.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0909; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0909 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
