A buyer in Nottingham, United Kingdom working in industrial machinery wants a thin steel fascia brightened evenly without thinning the sheet, distorting the folded return or leaving handling scratches visible in the reflection. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial that returns the tested panels with observations and a proposed media, compound and cycle direction. This brief is written for a buyer in Nottingham working on industrial machinery; it describes equipment, media and a scoped sample review, not a local polishing service.
How will the finish be measured or viewed, with which instrument, angle, cutoff and master, and who holds that master?
What batch size, part mix and media maintenance routine will production really run, and does the trial describe that condition?
How much stock may the sequence remove before datums, seal faces, flatness or edge form fall outside their allowance?
Bright polishing rounds edges, and the more energy and time the sequence needs, the more rounding appears. Some edges are cosmetic and rounding is welcome; others define function, such as a scraper edge on a machine-tool slideway, a knife edge on a metering blade, a thread start, or the lapped lip of a valve seat. Mark those features on the drawing and state a maximum edge radius or a no-touch zone before media is selected. Inspection can use radius gauges, a cast impression or an optical comparator against the incoming edge form. Where a crisp edge and a bright face conflict, the practical order is to finish the face first and restore the edge with a controlled hand operation, or to accept a slightly duller face that preserves the edge.
Ceramic media cuts well and holds shape, which keeps the working geometry predictable, but dense ceramic can chip thin edges and its wear debris becomes fine abrasive that carries into later stages. Plastic media is light and gentle, which suits aluminium and brass, though lower density means less contact force and a longer cut stage. Steel media burnishes rather than cuts and gives the brightest wet result on stainless and hardened steel, but it can transfer iron and rust if compound and rinse do not protect the load. Dry media such as walnut shell or corn cob is used for lubricity and drying rather than stock removal. Every medium wears, so measure size loss and replace on a schedule: a worn charge finishes differently and no longer describes an earlier trial result.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media - walnut shell | Dry polishing, light deburring and lubricity on parts where a residual oil film is acceptable, and drying or lustre steps after wet processing. | Not a stock-removal medium, generates dust that needs extraction, and can leave an oily film that interferes with a later cleaning or coating requirement. |
| Small high-density ceramic spheres or ovals | Colour and pre-lustre stages where a uniform, soft-looking finish matters more than stock removal, including curved and contoured faces. | Very slow cut, easily lost through screens sized for larger media, and ineffective in deep recesses because it cannot reach or press against the surface. |
| Hardened steel media, balls and shaped shot | Bright burnishing of stainless and hardened steel, and the final wet lustre stage where a dense medium can peen a surface smooth. | Can transfer iron and rust to stainless, dents soft or thin parts, and must be kept in a dedicated charge away from ceramic media. |
| Plastic or polyester media | Gentle processing of aluminium, brass, copper and thin panels where metal smearing, nicks and distortion must be avoided. | Low density gives little contact force, so cycles run long and heavy grinding marks may survive; plastic also wears quickly and can float above the working mass. |
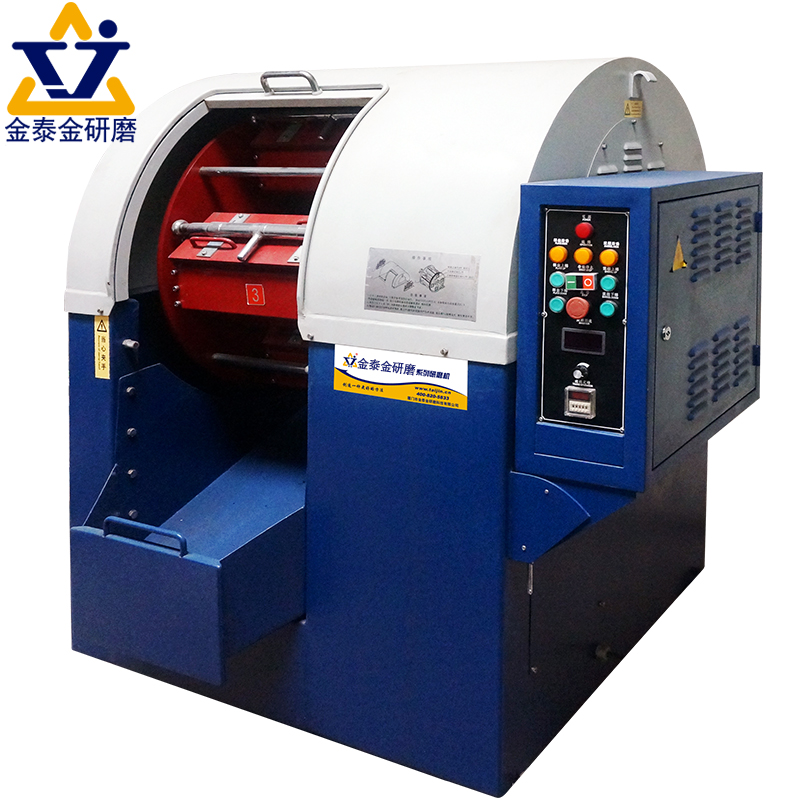
When a part must lose a measurable amount of stock before colour stages, disc finishing and centrifugal barrel machines deliver far more energy than a conventional vibrator. That energy shortens the cut stage but also rounds edges, work hardens soft alloys and can distort thin sections. Load the parts so they cannot jam against the disc wall, and bracket cycle time tightly, because the difference between enough removal and too much is small. Centrifugal barrels suit small to medium parts with simple geometry. Neither route removes the need for refinement: the surface they leave still needs finer media and a polishing compound before a reflected image becomes coherent, and the depth achieved has to be verified on a sample rather than assumed from a setting.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Barrel finishing machine / rotary barrel tumbler | Dense, uniform colour on small hardware that tolerates sliding contact, especially with steel media for a burnished appearance. | Nothing longer than the barrel diagonal can be processed, and slender parts can bend or nick against neighbours in the load. |
| Vibratory finishing machine (bowl or tub) | Cut-to-colour sequences on rigid, mostly open parts such as housings, covers, brackets and frames, with adjustable energy and no fixturing. | Cannot present media uniformly into pockets with narrow mouths or deep internal bores, and broad flat faces finish more slowly than edges. |
| Disc finishing machine | Fast, high-energy cut down on small to medium parts with simple geometry where cycle time matters and edge rounding is tolerable. | Part-on-part contact and wall pressure can chip or deform parts, and the difference between sufficient and excessive removal is narrow. |
| Dry polishing machine and dryer | Final lustre, dry colour and post-wet drying where the last reflected image cannot be produced by a wet mass-finishing stage. | Works on accessible faces only, generates dust and heat that need control, and offers no way to correct a defect left by an earlier stage. |
Beyond a certain point, more polishing makes a surface worse. Excess cycle time or contact pressure rolls metal over instead of cutting it, burying abrasive and debris under a smeared skin that looks bright until it is disturbed. On dry or high-speed operations, friction raises local temperature enough to tint the surface and soften a hardened layer, and thin sections can distort from the heat. High-energy routes add part-on-part impingement, leaving nicks and small dents that polishing cannot remove. Watch for a bright surface that dulls or streaks when wiped with a clean cloth, for colour variation near edges where contact is highest, and for dimensional or flatness change. The remedy is a shorter or gentler cycle, better cooling and a real end point instead of a longer run.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Dimensional drift or lost flatness on datums, seals and bearing seats | Uneven stock removal across a large or asymmetric face, over-long cycles, or unprotected functional features exposed to the full charge energy. | Measure flatness and critical dimensions with a CMM or surface plate at the same marked points used for the incoming survey, and compare the change against the allowance. |
| Iron pickup or rust bloom on a stainless surface | Carbon steel particles or steel media sharing a machine or charge, contaminated rinse water, or a damp surface left in contact with packaging after drying. | Wipe or swab the surface and look for a brown trace, check the charge and machine for ferrous pieces, and inspect parts after a short dwell in the packaging they will ship in. |
| Smearing or a rolled surface with abrasive and debris buried in it | Excessive cycle time or contact pressure, insufficient compound lubricity, or a final stage run at energy the material cannot absorb without deforming. | Wipe a defined area with a clean white cloth and look for streaks or dulling, then examine at magnification and compare microhardness or etch response against an unmachined reference. |
| Media lodged in blind holes, slots, undercuts or threaded features | Media size too close to the opening, a slot or cavity that traps the charge, or no defined retrieval step before rinsing and drying. | Reconcile a counted media charge before and after the cycle, borescope each cavity at an agreed angle, and pin or thread gauge the features the charge could enter. |
Nottingham is a Nottinghamshire authority inside the East Midlands Freeport, the only inland UK freeport, whose three sites are East Midlands Airport and Gateway Industrial Cluster (EMAGIC) in Leicestershire, the Ratcliffe-on-Soar power station site in Nottinghamshire, and the East Midlands Intermodal Park in Derbyshire. The freeport states its sites are connected by road, rail and air and within easy reach of East Midlands Airport, which it calls the UK's largest dedicated airfreight airport, and it reports that a share of the UK's major freight rail lines are serviced through the East Midlands. Nottingham City Council provides the city's business licensing, trading standards and procurement services, and the East Midlands Chamber is the regional chamber of commerce.
For this brief the relevant part of that base is machinery: The freeport reports that a share of the UK's major freight rail lines are serviced through the East Midlands, the freight context for the area's engineering firms.
The East Midlands Freeport is built around freight and low-carbon industry sites rather than a legacy machining cluster, so finishing requirements in the Nottingham area follow the parts being made and moved rather than any single local process tradition. Because the freeport's sites connect by road, rail and air and the East Midlands is a major goods-importing region, deburring, edge and cleanliness specifications should be taken from the component drawing and its downstream assembly rather than from a general local practice.
A Nottingham buyer should tie the finishing specification to the part's actual route out of a freeport or industrial site - air, rail or road - and confirm media and compound handling and waste arrangements before the machine is ordered.
Freight context: East Midlands Airport (described by East Midlands Freeport as the UK's largest dedicated airfreight airport), East Midlands Intermodal Park, Derbyshire, Ratcliffe-on-Soar power station site, Nottinghamshire. East Midlands Freeport describes itself as the only inland UK Freeport, with sites connected by road, rail and air and within easy reach of East Midlands Airport; it states that a share of the UK's major freight rail lines are serviced through the East Midlands.
BSI is the UK's National Standards Body, and British Standards (BS, including adopted BS EN ISO texts) are the documents a UK buyer's surface-finish, edge and cleanliness specifications are normally written against and purchased through. On the plant side, HSE maintains the work equipment and machinery topic covering the safe supply and use of machinery, and the COSHH regime, which requires employers to identify, assess and control risks from hazardous substances - the regime that applies to finishing compounds, abrasive media and the dust and effluent they generate.
Importers need a GB-prefixed Economic Operators Registration and Identification (EORI) number, an import declaration carrying the correct commodity code, and retained commercial invoices plus the Import VAT Certificate (C79) so import VAT can be reclaimed. Machinery placed on the Great Britain market must be marked UKCA or CE: the manufacturer must draw up and retain technical documentation including a Declaration of Conformity, apply the correct marking with identification details, and cooperate with market surveillance; an authorised representative must be established in the UK. Under the Product Safety and Metrology (Amendment) Regulations 2024 the UK continues to recognise CE marking alongside or in place of UKCA for the Great Britain market, so either route can be used for most product types. Duty and import VAT are calculated from the customs value declared, and the commodity code also determines whether an import licence is needed.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Ask for a settings record with every batch: machine and stage, media type and size class, charge mass and age, compound product and measured dose, load ratio, cycle time and rinse conditions. Retain a fully inspected first article as the physical reference, together with its measurement data and photographs at fixed scale and lighting. Write the disposition rule in advance, covering what passes, what is reworked and what is scrapped, and name who decides. The record should state plainly that the reported condition applies to the parts tested, at the locations measured, with the settings used; it is a description, not a guarantee of future output or of fitness for any regulated application. Certificate and approval requests belong with the buyer's own quality function.
A trial runs a small, hand-selected load on equipment that has just been set up. Production runs mixed batches on a media charge of unknown age, with transfer time between stages, variable rinse quality, operators on different shifts, and parts arriving with different incoming damage. Plan a defined pilot batch that uses the intended line configuration and a full first-article inspection, then compare it with the trial observations before committing volume. Watch the variables that scale badly: drying time in a humid season, water chemistry, load density and the handling between cut, colour and lustre stages. Treat the pilot as the real test of stability and keep its settings record with the parts so any drift can be traced.
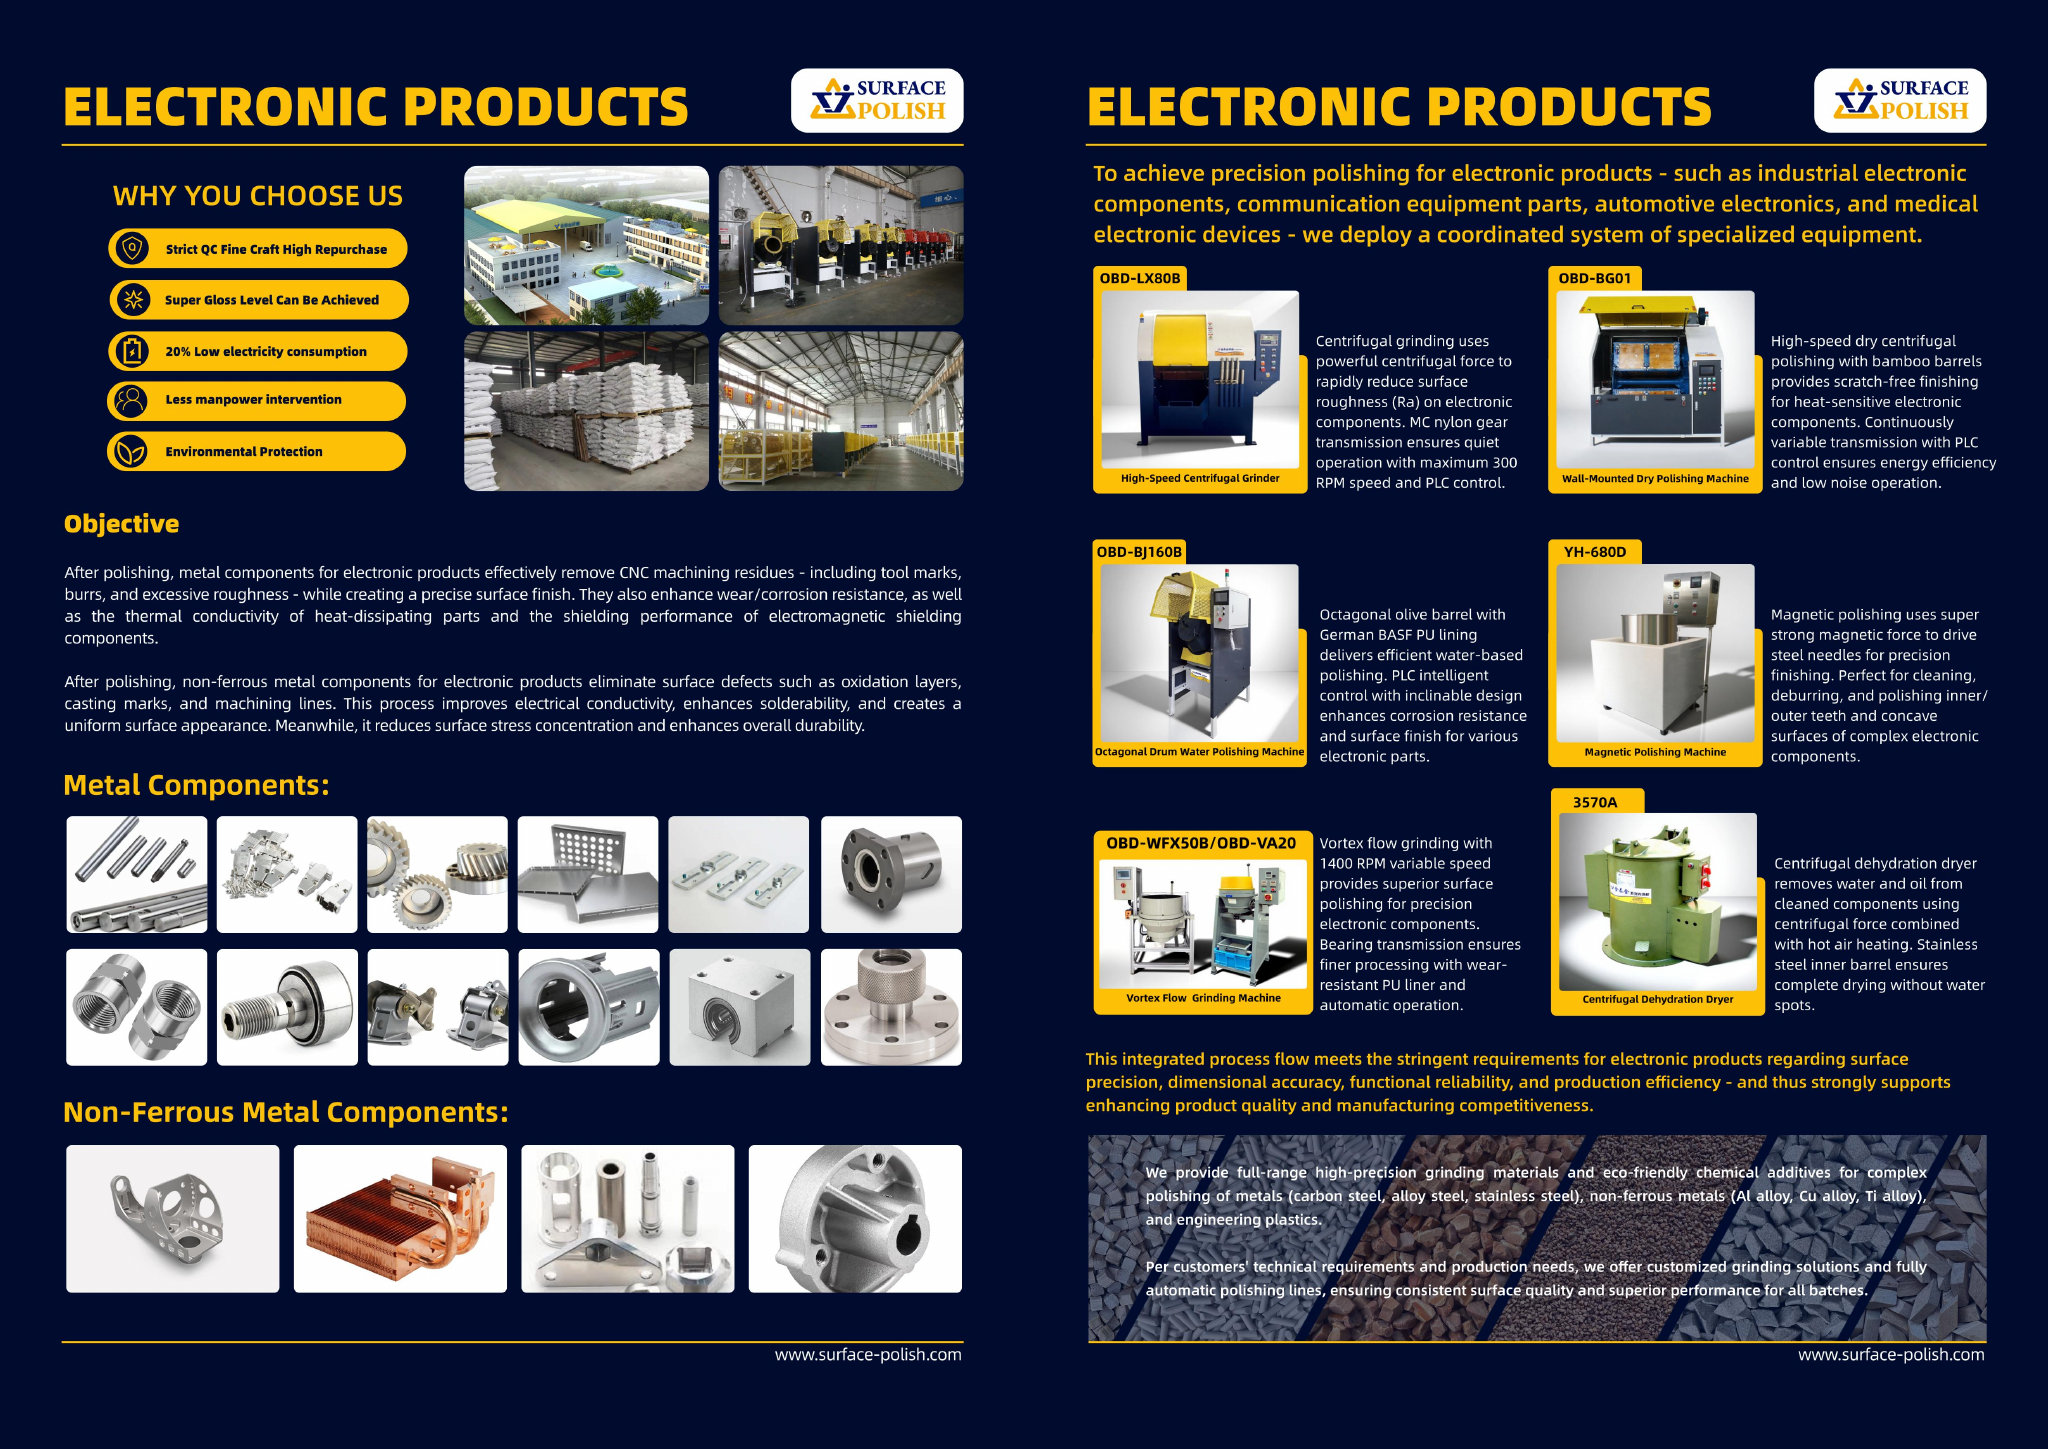

Haze and sleeks usually come from contamination rather than from a wrong final medium. Worn media shed an oversized fine fraction, abrasive can agglomerate in the compound line, screens and machine walls carry grit from an earlier coarse stage, and a shared or under-controlled rinse moves particles forward. Inspect under raking light against a master and trace the pattern: defects that appear in one machine point to the charge, while those spread across machines point to rinsing or handling. Clean the charge, screen the media and re-establish the rinse before changing the compound.
Ra alone is not enough. It is an average over a defined cutoff length, so a surface with a low Ra can still show waviness, orange peel or directional marks that dominate what a viewer sees, while a slightly rougher surface can look brighter if it scatters light evenly. Specify the measurement setup as well as the value, and where appearance is what matters, add a reflectance or gloss reading at a stated angle together with a physical master and viewing conditions. For Nottingham buyers working to a functional surface requirement, specify the profile and the appearance requirement separately.
No to both. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and it does not supply or perform electropolishing or operate a plant, branch, dealer or technician service in United Kingdom or any other market. What is offered is equipment and consumables, a scoped discussion of a finishing line concept, and a free sample trial in which representative parts are shipped to Xiamen and returned with observations and a proposed process direction. Where an electrochemical finish is under consideration, the discussion stays a comparison with a mechanical route.
Use Nottingham, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Equipment placed on the Great Britain market requires UKCA or CE marking with a Declaration of Conformity, and HSE's work equipment and machinery and COSHH regimes cover finishing machines, media and compounds. Nottingham City Council's trading standards service and business licensing function are the local points of contact for product and trading rules.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Nottingham.
The buyer needs the fascia reflective and uniform without thinning the panel, distorting the fold or leaving the handling scratches visible.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0299; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0299 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
