A buyer in Nantes, France working on energy equipment has an Inconel turbine disk whose broached rim slot edges need a consistent break without disturbing the profile. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial, sending representative parts to Xiamen and returning them with an observation record plus a proposed media, compound and cycle direction for the buyer's engineers. This brief is written for a buyer in Nantes working on energy equipment; it describes equipment, media and a scoped sample review, not a local polishing service.
What must the part be clean of, and what method and limit does the buyer use to verify cleanliness before assembly, welding, coating or a leak test?
Which edges on this part are functional, such as gasket lands, seat bands, stem guides, metering lands and thread entries, and which only need to be free of a sharp edge?
Which material families and heat-treatment states share the equipment, and what separation is needed to avoid ferrous or graphite carry-over onto stainless parts?
Treat the batch, not the individual part, as the unit that gets controlled. A charge holds a defined mass of parts sharing a material family, a burr condition and an edge requirement. Mix a thin heat-exchanger plate with a heavy valve body and the light part absorbs energy it did not need while the heavy part shields its own critical edges. Batch definition also fixes traceability. If two heats of duplex stainless or two casting lots run together, a defect found later cannot be tied back to a charge, a media age or a compound batch. Keep part numbers, material grades and heat-treatment states in separate runs, label the charge, and record how many parts were loaded and in what orientation.
Every mass-finishing route is also a contact problem. Parts touch each other, the machine wall and any fixture, and each contact is a chance to mark, peen or bend a finished face. Compartmenting a charge, racking parts individually or running a smaller load with more media between parts changes the contact pattern, and it changes throughput in the same move. Where a machined gasket land, a ground spigot or a lapped sealing face must arrive unmarked, decide which faces are allowed to bear contact and design the load around that. A fixture can hold a part out of the mass, but it also shields the area behind it, so the shielded zone has to be finished another way or left as-machined. Record the contact plan with the load.
| Machine route | Where it fits | What it will not do |
|---|---|---|
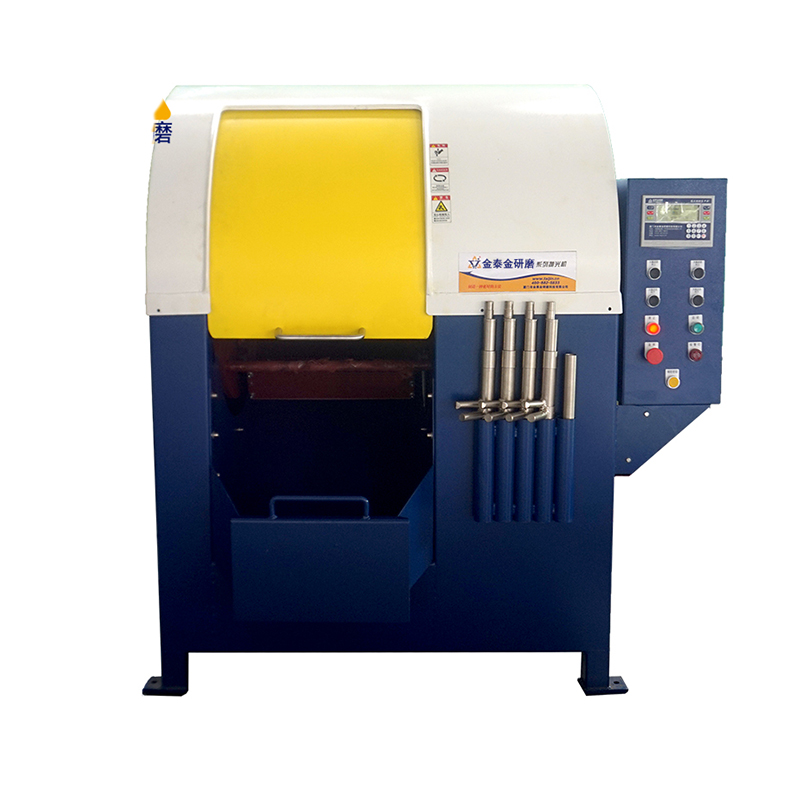
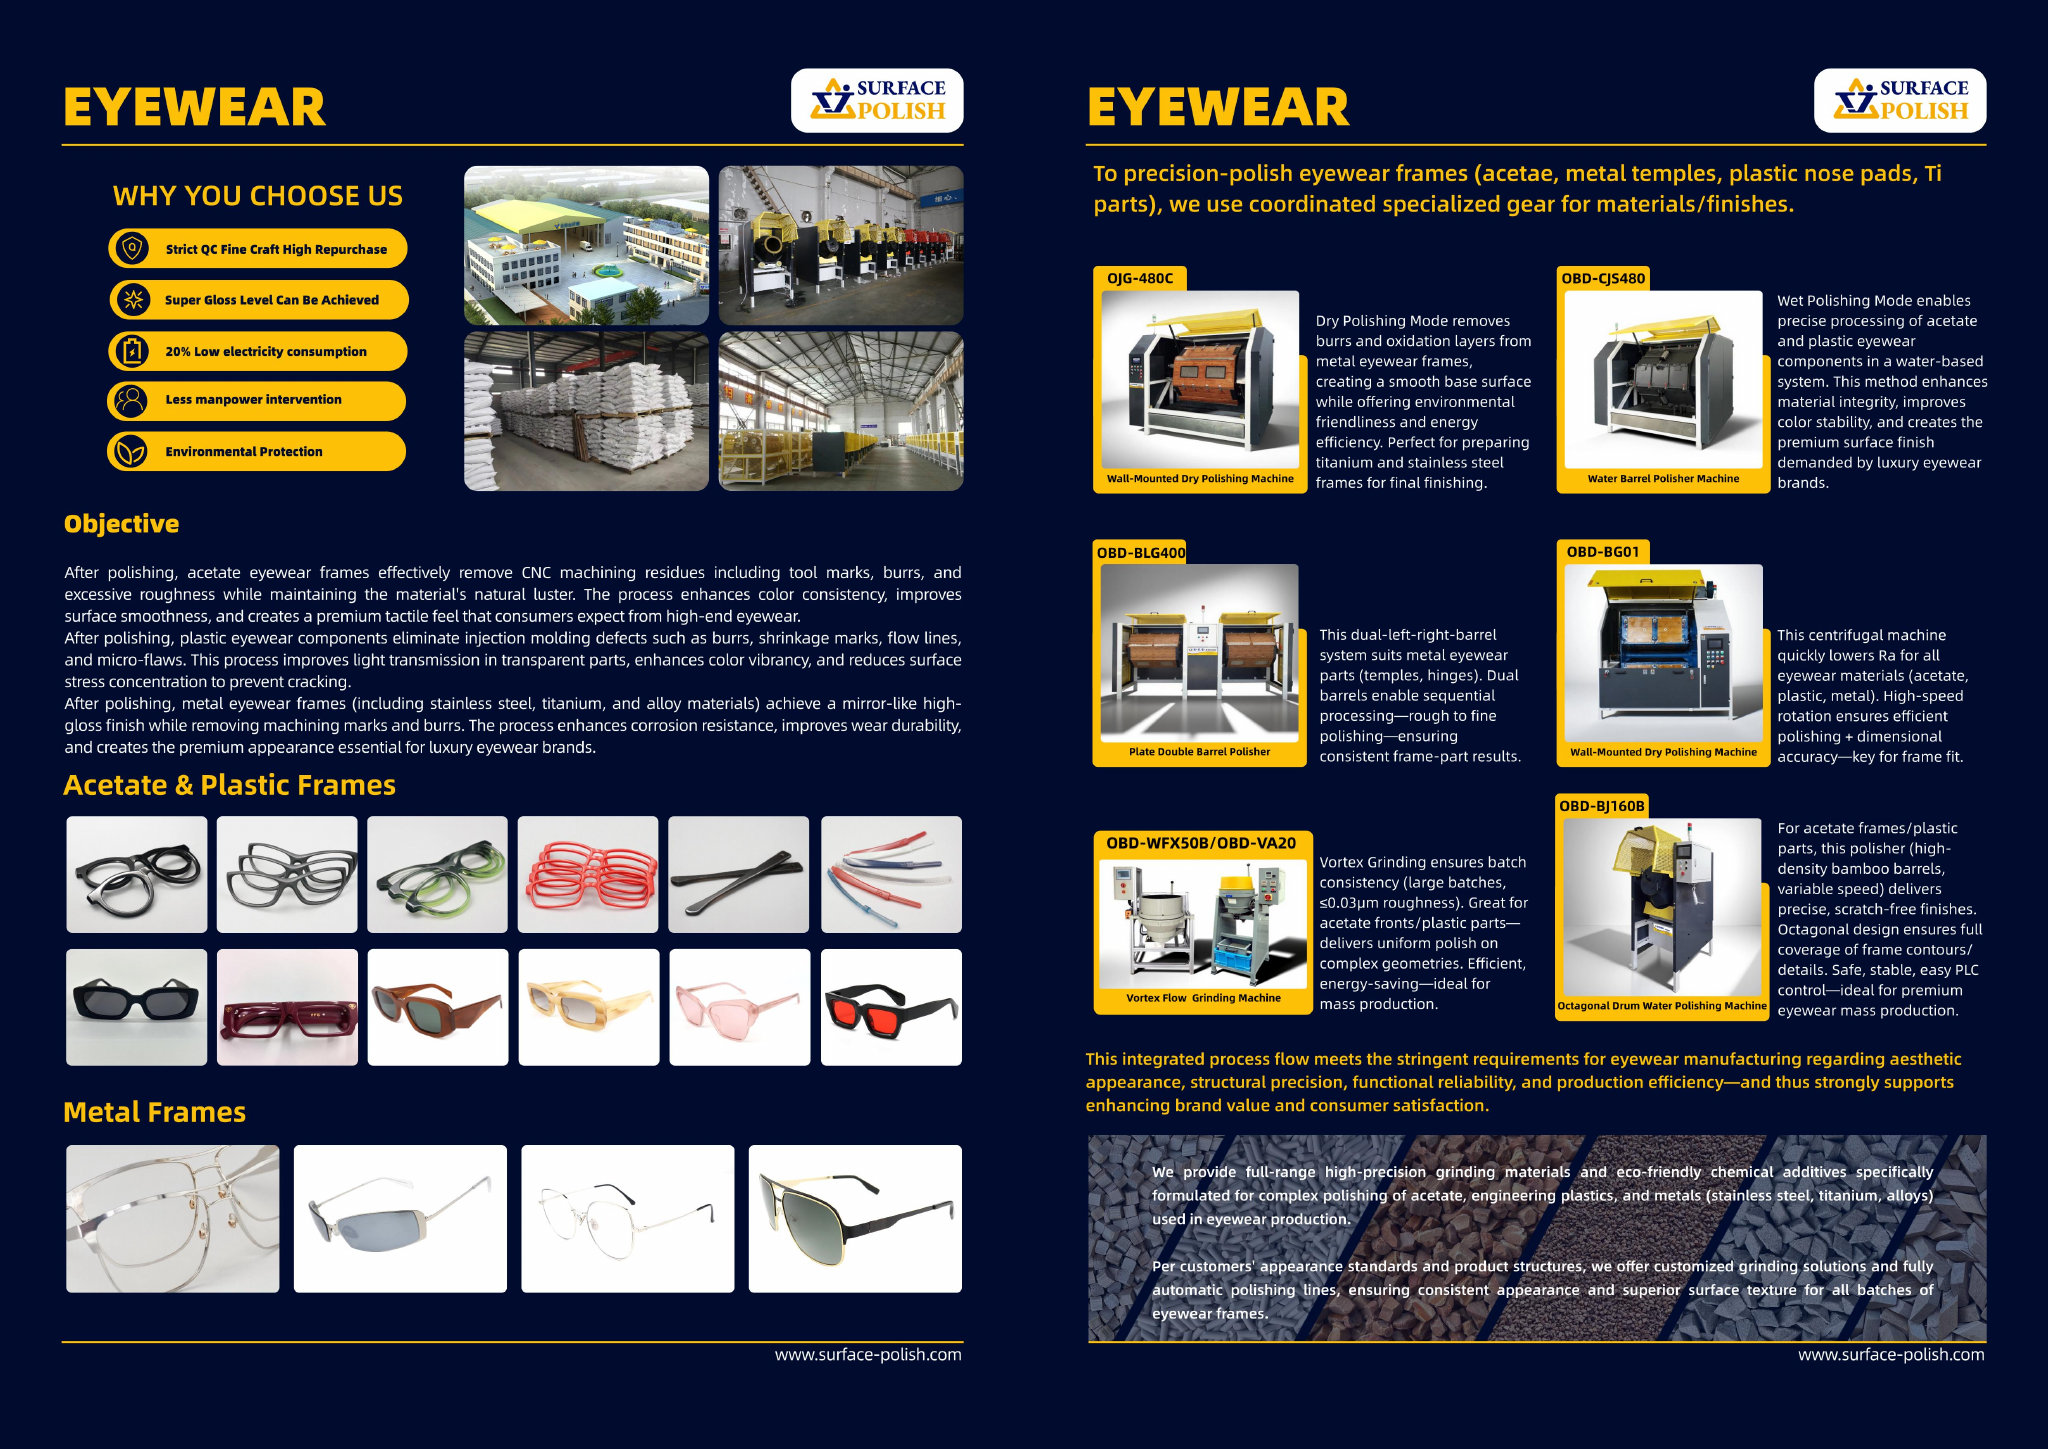
| Vibratory finishing machine (bowl) | General deburring and refinement of valve bodies, flange plates, pump components and fittings that fit the bowl and can move freely in the charge | No access to deep internal passages, constant part-on-part contact, and finished faces need separation or fixture protection |
| Tub vibrator | Long parts such as manifold rails, shafts, long housings and stacked plate sets that cannot tumble in a bowl, with support or rotation along their length | Lower energy per unit area so heavy burrs take longer, and the tub needs floor space plus a defined part support method |
| Centrifugal barrel finishing machine | Short high-pressure cycles on small precision parts such as spools, sleeves, small valve bodies and drilled fittings | Rounds edges and can distort thin unsupported sections quickly, and needs balanced barrel loading, controlled stop time and careful fixturing |
| Grinding finishing machine | Heavier stock removal and thick burr roots on robust parts where clearing material in a shorter cycle matters more than the surface result | Aggressive edge rounding and a coarser surface, so it fits lapped seats, thin sections and tight edge bands poorly |
Compound delivered at the wrong concentration or flow makes the same media behave like a different charge. Too little and the abrasive cut becomes dry and marking increases; too much and cutting slows while foam and carry-over rise. Flow rate matters as much as dose, because it is the flow that carries fines away from the part and keeps the working zone consistent across a long cycle. Water quality belongs in the same discussion: hardness, pH and dissolved solids in the make-up water shift the compound's behaviour, and a plant that changes its water source can change its results without touching a machine setting. Where the fluid is recirculated, filtration and turnover decide how much swarf and broken media stay in suspension and how often the bath is dumped.

| Media | Best fit | Watch out for |
|---|---|---|
| Magnetic pin or needle charge | Reaching small internal intersections, radial holes and thread entries on small precision parts such as spools, sleeves and drilled fittings | Limited by part size and shape, pins must be retrieved and inspected for breakage, and the result depends heavily on fixture and field design |
| Heavy-cut ceramic, angle-cut triangles in a coarse size class | Removing a substantial or thick burr root from open external edges, flange corners, cast bosses and large tapped entries on steel and stainless parts | Cuts controlled edges and gasket lands as readily as burrs, leaves a coarse surface, and lodges in slots whose width approaches the media section |
| Plastic media triangles and pyramids in a soft to medium grade | Deburring aluminium, brass and other soft or thin-walled parts where surface marking and edge rounding must stay minimal | Slow cut rate, media deforms and wears out of shape, and a worn charge behaves noticeably differently from a fresh one |
| Fine ceramic spheres or small porcelain shapes in a light size class | Refinement and edge blending after a cutting stage, and light deburring of small fittings, thread entries and tighter external geometry | Small sizes enter and retain in fine passages and cross-drillings, and the charge changes size and cut rate as it wears |
Contamination in this process is mostly invisible at the machine and is discovered downstream. Three forms matter on energy-equipment parts. Media fragments and abrasive fines can embed in soft surfaces or in a machined groove and later appear as particles in a fluid system. Material carryover happens when carbon steel fines or cast-iron graphite from an earlier batch stay in the charge, the machine, the rinse tank or the drying cloth and transfer to stainless parts. Compound residue and its reaction products can sit in a gasket groove, a thread or a blind hole and interfere with welding, passivation or a coating step. Control is separation and cleaning discipline, verified with a wipe or tape lift, magnification, and a flush residue check.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Media fragments or abrasive fines embedded in a soft surface or machined groove | Impingement from excessive energy or charge mass, fractured media left in the working charge, or cross-contamination from a previous material family | Inspect at magnification under angled light, use a tape lift or solvent wipe on the suspect area, and screen the charge for broken media and accumulated fines |
| Staining, pitting or a corrosion question on a hardened high-strength part after a wet cycle | Acid-bearing compound or contaminated rinse water, long dwell between finishing and drying, or no protective rinse for the interval before the buyer's next operation | Inspect within an agreed interval after drying, wipe a defined area with a white cloth, compare against a retained reference, and route any embrittlement question to whoever owns the downstream coating or plating specification |
| Part-on-part or fixture witness marks and peening on a finished face | Insufficient separation in the load, too high a load ratio for the part mass, sharp or worn fixture contact points, or the same faces bearing contact throughout the cycle | Inspect at magnification under angled light against a retained reference, map the mark positions against the load arrangement, and check fixtures and compartments for burrs and wear |
| Loss of flatness or a dimensional shift on thin plates, thin walls and long unsupported sections | Part-on-part impacts and fixture pressure in a high-energy route, too high a load ratio, or insufficient support along a slender part | Check flatness on a surface plate or a coordinate measuring machine at marked points before and after finishing, and check the same points across parts from different load positions |
Nantes sits on the Loire estuary industrial axis, whose port authority - Nantes Saint-Nazaire Port, the fourth largest French seaport, handling about 30 million tonnes of traffic a year - describes itself as a logistics and industrial platform connected by sea, river, rail, road and air, with 1 460 ha of industrial-port land and more than 600 companies in the industrial-port complex. INSEE counted 11 718 establishments in the commune at the end of 2024 with 3,3 % in industry and 215 178 jobs at the place of work in 2023. The estuary economy combines shipbuilding and offshore-wind fabrication at Saint-Nazaire, aerostructures and composites, agri-food and agricultural machinery in the wider Loire region, and naval/aeronautical engineering in Nantes itself.
For this brief the relevant part of that base is energy: The port reports 5 973 thousand tonnes of natural gas and 7 630 thousand tonnes of crude oil traffic, and is adapting its infrastructure for offshore wind assembly through the Eole project following the first French offshore wind farm.
The Loire estuary combines two finishing problems: large welded and fabricated steelwork for shipbuilding, offshore wind and heavy industry, where weld dressing, edge preparation and surface cleanliness govern coating performance and fatigue life; and smaller precision components in aerostructures and mechanical equipment where deburring and surface finish are tolerance-driven. Agri-food equipment in the region adds stainless fabrication where surface smoothness and residue-free cleaning are hygiene requirements rather than cosmetic preferences. Both cases reward a process that can be documented and repeated, because the customers here are audited industrial buyers.
A Nantes buyer should settle whether the target is surface preparation before coating on large fabricated assemblies or deburring and finish on machined components, and then check that the proposed process can handle the part mix without cross-contamination between ferrous and stainless work.
Freight context: Nantes Saint-Nazaire Port (Nantes, Montoir-de-Bretagne, Saint-Nazaire, Donges), Nantes Atlantique Airport, Montoir container and ro-ro terminals. The port states it connects to five continents through regular maritime services linked to the main European transhipment hubs, with 209 container ship calls and 198 ro-ro calls in 2025, plus 800 freight trains and river barge convoys; 25 ha of industrial-port land reserve is available. That makes it practical to receive containerised finishing machines and bulk media through Montoir and to ship sample parts by air from Nantes Atlantique or by courier.
France applies the EU common commercial policy, so industrial machinery arriving from China enters under the Union Customs Code and the Common Customs Tariff rather than under any bilateral French regime; the EU has no free-trade agreement with China, so no preferential duty rate applies and normal third-country duties are due on the customs value. Importers classify the machine in the tariff nomenclature and lodge a customs declaration; French Customs publishes the common and national tariff through its RITA online service and states that three notions are fundamental: the tariff classification of the product, its origin or destination, and the value of the goods.
The working language of French industrial procurement is French: tenders, drawings, inspection plans and technical dossiers are normally issued and answered in French, and quotations that omit French documentation slow down qualification. Buyers qualify a machine against a written specification and expect traceable material certificates, machine safety documentation and, where applicable, a CE declaration of conformity and a risk assessment; acceptance is often staged (documentary review, factory acceptance test, then commissioning). Payment and documentation norms are conventional EU practice: euro invoicing, SEPA or SWIFT bank transfer, Incoterms agreed in writing, and customs paperwork (commercial invoice, packing list, transport document, proof of origin where a preference is claimed) prepared for the declarant or customs representative. Because customs and tax authorisations are handled jointly through SOPRANO, non-EU sellers are normally advised to sell to an established French/EU importing entity rather than to act as importer of record themselves.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Edge acceptance needs a reference object, because words like lightly broken or slightly rounded mean different things to different inspectors. Build a physical or photographic master at a stated magnification: a part or coupon showing the acceptable edge, the borderline case and the reject. For each controlled edge, express the requirement as either an edge break, meaning the sharp corner is removed to a small defined size, or an edge round, meaning a controlled radius band the edge must sit inside. Give a maximum where over-rounding is the risk, and a minimum where the edge must not stay sharp. State how the edge will be checked, whether by radius gauge, optical comparator, moulded replica or tactile comparison against the master, and at what frequency.
The value of a sample trial comes from the range of parts sent, not from the quantity. A box of identical nominal parts tests one geometry and one burr condition; it cannot show how the proposed route behaves on the tightest passage, the thinnest wall or the hardest material in the family. Send a small set chosen to cover the extremes: the part with the smallest internal opening, the part with the longest unsupported section, the part with the most protected edge, one part in the hardest heat-treatment state the family sees, and one as-received reject that already fails. Label every part so its identity survives the trip, and send enough pieces that some can be sectioned or measured destructively.

Mass finishing removes material mainly at edges and corners, so a critical dimension across a flat face usually moves very little, but thin and slender parts can distort. Part-on-part impacts, fixture pressure and long cycles in a high-energy machine can dish a heat-exchanger plate, bend a thin diaphragm or spring a long unsupported section. The effect depends on section stiffness, load ratio, media mass and support method, and it can be small enough to be missed until assembly. If flatness matters, say so before the trial, nominate the measurement points, and check the same points after finishing rather than judging the plate by eye.
Both positions are used, and the choice follows the burr and the edge requirement. Deburring before hardening removes the machining burr while the material is still soft and the charge cuts predictably, but hardening can then introduce scale and slight distortion, and edges may need a light blend afterwards. Deburring only after the final thermal step keeps every edge operation in one place and works on the finished metallurgical state, at the cost of a harder material that cuts more slowly and a risk of brittle edge chipping. Discuss the sequence with the heat treater and the process engineer, and record the condition the part arrives in for finishing.
The finishing step is part of the route, and what it leaves behind matters to the next operation. Compound residue in a gasket groove or thread can interfere with welding, passivation or a coating bond, and a surface finished with an acid-bearing compound may need a defined rinse and neutralisation first. Mechanical work also changes the edge geometry a coating must cover, so an edge deliberately broken or rounded takes a coating differently from a sharp one. Tell the finishing route what comes next and agree the rinse, dry and handling between them. Where a hardened, high-strength steel is later plated, raise the embrittlement question with whoever owns that specification.
Use Nantes, France as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Nantes buyer would reference ISO/NF EN surface-texture standards for finish and roughness, EN 1090 and the classification-society rules for welded steel and marine structures, and hygiene-related surface requirements for food-contact equipment; ISO 9001 is the common baseline, with EN 9100 where aerospace work is involved. Coating and surface-preparation specifications for offshore and marine fabrication are usually set by the client or the classification society on top of those standards.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Nantes.
The buyer must break the sharp slot edges consistently around the disk without reworking the broached profile or rounding the bolted flange face.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0558; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0558 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
