A automotive parts buyer in Rotterdam, Netherlands has a thin formed sensor bracket whose laser-cut edges carry dross that must come off without distorting the bend or damaging a threaded insert. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and its free sample trial processes parts sent to Xiamen and returns them with observations and a proposed media, compound and cycle direction for the buyer to verify. This brief is written for a buyer in Rotterdam working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which internal features must be deburred without lodging media, and what retrieval and verification step proves the passage and thread form are clean?
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
How will free iron, embedded particles and cross-contamination from carbon steel be prevented, and how will each be detected on the finished part?
Stainless is a family, not one material, and the finishing window changes with it. Ferritic grades used for exhaust and trim are magnetic and generally softer, so they cut quickly and can smear; martensitic grades used for wear parts are hard and magnetic, and some high-strength conditions carry a hydrogen concern when acid chemistry is involved; austenitic grades are tough, work harden under mechanical action and are usually non-magnetic, which changes retrieval options; duplex and super-duplex grades combine high strength with chloride sensitivity, so surface contamination matters more. Cold work matters twice, because a pressing or a machined skin alters surface hardness and can shift magnetic response, and because a bright finish on a work-hardened skin may not survive a later forming operation. Record grade, delivery condition, hardness range and prior cold work, then match machine energy and media hardness to the family rather than reusing a recipe that worked elsewhere.
Disc finishing machines run a shallow, fast-moving charge that deburrs heavier machined stainless parts quickly: valve bodies, fittings, machined brackets and parts whose edges can lose material. The energy is an advantage for cycle time and a liability for thin walls and delicate features, so tooling and compartments often decide whether the route is acceptable at all. Centrifugal barrel finishing uses a planetary barrel motion that produces very high energy in short cycles, useful for aggressive edge radiusing on small, hard parts. The same energy rounds edges quickly, can exceed a tight radius callout within a short run, has part size and shape limits, and needs a larger load to justify the cycle. Treat both routes as candidates for heavy deburring and blending, and verify edge results on the actual part rather than assuming a shorter cycle means a safer one.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Magnetic finishing machine | Small precise stainless parts with internal features, slots and blind holes that must be deburred without media lodging in the passages. | Works within a small part envelope, and the route has to be tested per grade because it depends on the part's magnetic response. |
| Vibratory finishing machine, bowl type | General deburring and surface refinement of medium-sized stainless automotive parts such as brackets, small housings and flange blanks in a visible batch load. | Part size and shape are capped by chamber geometry, and thin or threaded parts may need compartments or fixtures to control part-on-part contact. |
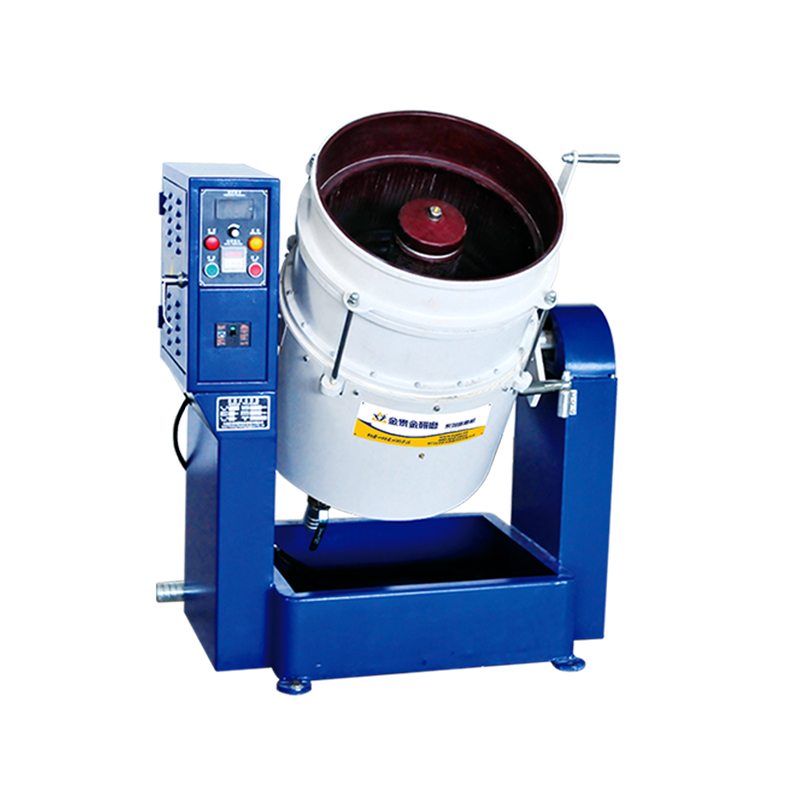
| Disc finishing machine | Fast deburring and blending of heavier machined stainless parts whose edges can accept a higher removal rate. | The higher energy can damage thin walls and delicate features, so tooling or compartments are often needed to protect them. |
| Dry polishing machine with heated dryer | Post-wet drying, residue control and light dry finishing of stainless parts that must leave the line dry and free of moisture in blind features. | Dry media does not cut stainless, and moisture trapped in a blind hole, hem or tight joint can cause staining if drying is not effective. |
Once media and machine are fixed, the variables a buyer can actually control are compound concentration, flow rate and water quality. Concentration influences cut rate, foam and residue; running lean to save money usually costs more in finish variation than it saves in consumable. Flow rate removes swarf and heat from the mass, and an under-flowed chamber loads up, smells, and starts depositing sludge on the parts. Water hardness, chloride content and suspended solids matter directly on stainless, because hard water leaves mineral films and chloride-bearing supply raises pitting risk on austenitic grades. Get a water analysis for the site, dose by measured concentration rather than by eye, and monitor pH and clarity at the machine. Record the actual water source used during a trial, because a good result obtained on one supply may not survive a change.

| Media | Best fit | Watch out for |
|---|---|---|
| Porcelain and fine high-density ceramic media | Pre-polish refining stages on austenitic stainless appearance parts before a brightening stage, where a finer texture is the objective. | Limited cutting power on hard or work-hardened surfaces, and wear changes the charge gradually, so finish can drift between batches. |
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
| Dry media, walnut shell and corn cob | Post-wet drying, light residue and scale removal, and dry polishing of surfaces that must not be re-wetted. | Does not cut stainless, generates dust, and leaves organic residue on parts if the medium is not kept clean and dry. |
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
The defect that ends most stainless finishing trials is not a bad appearance but an edge that moved further than the drawing allows. Threads and gear teeth are the classic casualties, because mechanical action removes material from crests quickly, changing effective pitch diameter and flank form; a part can still thread by hand and still fail a gage. Radiused or chamfered edges behave similarly, since the process removes stock precisely at the edge where a callout is tightest. Start the trial with an edge record and repeat it afterwards: thread and gear gages before and after, edge radius at marked locations with an optical comparator or a cast impression, and a written allowable band agreed before any cycle runs. Treat the shortest cycle that achieves the required appearance as the control condition, and be suspicious of any proposal that adds cycle time to improve a finish that was already acceptable.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Rust blooms or speckling on austenitic or duplex parts after finishing | Free iron transferred from carbon steel, ferritic stainless or worn steel machine parts sharing the same media, chamber, racks or bench area. | Run a ferroxyl-type test for free iron at agreed locations, compare against an untouched part from the same batch, and repeat the check after a defined exposure period to catch delayed blooms. |
| Hazing or waviness on a part specified as mirror or bright | An intermediate refining stage skipped or cut short, media too coarse for the final texture, or a media charge that has worn out of its working size range. | View under defined lighting against a physical master at the acceptable and marginal limits, measure roughness across the lay with a fixed instrument setup, and screen the media charge for size and condition. |
| Media lodged in cross-drillings, tapped holes, hems or closed volumes | Media size class small enough to enter a passage but not guaranteed to exit, or a separation step that relies on gravity alone. | Weigh the part where sensitivity allows, inspect passages with a borescope at agreed angles, pass pin or plug gages through each passage, and reconcile media counted into and out of the batch. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
Rotterdam is the Dutch mainport and the centre of Europe's largest maritime, port and industrial complex, with refining, chemicals, bulk and container handling concentrated in the port and industrial area. Deltalinqs represents over 95% of the logistics, port and industrial enterprises in the mainport, with more than 700 member companies drawn from fourteen sectors; the mainport accounts for 2.9% of Dutch GDP and roughly 192,000 jobs in Rotterdam-Rijnmond, while the port as a whole supports over 500,000 jobs and more than EUR 60 billion of added value nationally. Municipal and provincial policy documents describe the cluster as the largest industry and energy cluster in Europe.
The nearest part of that base to this brief is energy: The municipality of Rotterdam and the province of Zuid-Holland, together with Deltalinqs and the Port of Rotterdam Authority, describe the port as the largest industry and energy cluster in Europe in their ten-point plan for the harbour.
Refining, chemical, bulk and maritime maintenance in the port generates a steady flow of valves, pump and heat-exchanger components, flanges and machined spares, where burrs, sharp edges and surface condition affect sealing, flow and coating adhesion. This is mostly repair and overhaul work rather than high-volume series production, so batch flexibility and cross-contamination control between carbon steel, stainless and higher-alloy parts matter more than cycle time.
A Rotterdam-area buyer should first settle which material families one finishing line must handle — carbon steel, stainless, duplex or nickel alloy — and whether the parts are pre-coating (needing a defined Ra and cleanliness) or in-service spares (needing edge and burr control only), because that fixes the media and compound choice.
Freight context: Port of Rotterdam (Europoort and Botlek industrial areas, Waalhaven). The port combines deep-sea, short-sea, inland barge and rail freight, and 192,000 jobs in Rotterdam-Rijnmond are linked to the harbour. Machines and sample parts arriving from outside the EU are declared to Dutch Customs at the point of entry; the Deltalinqs membership base is dominated by logistics, port and industrial enterprises.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
The Netherlands applies the EU's common commercial policy, so imports of Chinese industrial machinery enter under EU customs rules and WTO tariff treatment rather than under a bilateral EU-China free-trade agreement; the European Commission also maintains trade-defence measures on selected Chinese product categories, and China is a WTO member. EU-China trade in goods reached EUR 732 billion in 2024, and in 2025 manufactured goods were 97.3% of EU imports from China, with machinery and vehicles alone accounting for 54.4% — the single largest category. Chinese finishing machines, media and compounds therefore arrive in a very large, well-established EU import stream, and the buyer should expect MFN duty plus trade-defence measures where a specific product is covered.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Measurement of appearance does not detect a functional loss, so acceptance needs checks aimed at what the part does. Thread and gear gages on the features named by the drawing, pin or plug gages on cross-drilled passages, a flatness check on sealing faces, a fit or press trial on a bearing bore, and continuity or gap checks on sensor surfaces all address function directly. Edge condition deserves a dimension rather than an opinion, because a rounding of a fraction of a millimetre at the mouth of an O-ring groove changes how the seal seats, and a deburred edge on a fatigue-relevant hole behaves differently from a polished one. Cleanliness is part of this set: wipe tests for residue, free-iron testing, and a borescope check of internal passages catch defects that appearance grading cannot. Agree every check and its instrument before the first production batch.
Once a line is producing, batch control protects both the finish and the traceability. Identify each load with the material heat or lot, keep grades separate through the chamber and the dry stage, record the media charge identification and compound batch, and keep the inspection record attached to the same batch identifier so a later complaint can be traced to what actually ran. For stainless, batch separation also means physical separation from carbon steel processing, including shared baskets, dryers and benches. What a trial cannot prove is worth stating plainly: it observes the parts tested under one set of conditions, it does not guarantee a surface value, cycle time, capacity or cost in production, and it does not qualify a process for any regulated application. Treat it as a way to reduce uncertainty before capital is committed, and let the buyer's own verification settle acceptance.

Control direction, texture depth and coverage, not only a roughness number. Mechanical finishing tends to create directionality, so agree with the customer whether the grain runs in one direction across the whole part order and how visible variation may be. Keep a physical master for the satin finish and view parts under the same lighting, distance and angle as the master, because lighting changes appearance judgements more than small process changes do. Fix media shape, size class and cycle settings in a work instruction, and re-verify the finish whenever the media charge is replaced or a new supplier batch of compound is introduced.
Cost is governed by cycle time and the number of parts that fit in a load, by media consumption and replacement rate, and by labour for loading, unloading, separation, inspection and masking. Parts with several protected features cost more before the machine starts, because plugging and fixturing consume labour. A cycle that needs several stages for deburring, refining and brightening multiplies handling. Drying time and cleanliness verification add further steps, and mixing stainless with carbon steel in shared equipment forces either segregation or extra contamination checks. Ask for cost as a function of volume and batch size rather than as a single figure.
No, and relying on it creates two problems. Ferritic and martensitic grades are strongly magnetic, annealed austenitic grades are effectively non-magnetic but become weakly magnetic after cold work, and duplex grades sit between. A magnet cannot separate those cases, so it cannot support grade segregation or media selection. Worse, a mixed load lets a magnetic part transfer free iron to an austenitic neighbour. Identify parts positively from material certificates, heat numbers and markings, and settle separation by retrieval method, because magnetic retrieval works well on some grades and not at all on others.
Use Rotterdam, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers here work to the CE machinery regime (Machinery Regulation replacing the Machinery Directive, compliance by 20 January 2027) and to the Dutch/EN-ISO surface-finishing standards published by NEN, such as NEN-EN-ISO 2080 for metal-finishing terminology. In the port and process industries, client specifications for coating preparation, cleanliness and material conformity usually sit on top of those base standards.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Rotterdam.
The buyer needs the laser-cut dross and edge burrs removed without distorting the formed bend, rounding the slots beyond limit, or altering the thread insert.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0612; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0612 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
