An automotive parts buyer in Breda, Netherlands has a thin stainless grille frame that must reach a consistent bright finish without distortion or impingement at its pierced openings. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to Xiamen, returning the tested parts with observations and a proposed media, compound and cycle direction for the buyer to verify. This brief is written for a buyer in Breda working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which alloy family is the part, and has cold work, welding or heat treatment already changed its hardness, magnetic response or corrosion behaviour?
Which dimensions, seal faces and thread forms carry functional geometry, and what limit on stock removal per cycle can those features tolerate?
How will free iron, embedded particles and cross-contamination from carbon steel be prevented, and how will each be detected on the finished part?
Stainless automotive parts usually carry two requirements that pull against each other: an appearance grade on surfaces the customer sees, and an edge or function requirement on features that must keep working. Map the part into exterior visible surfaces, hidden surfaces, and edges with a functional role such as sealing, bearing, fatigue resistance or assembly clearance. An edge that only needs a burr broken can take an energetic cycle; a bore edge that sets a seal or a press fit cannot. Ask which faces are graded after assembly, because a bright panel that meets a specification by itself may look mismatched against the mating panel next to it. A marked-up drawing that states, per surface, whether it is graded, functional or indifferent is the cheapest document in the whole finishing project.
A medium can only cut what is softer than itself, and stainless work hardens at the surface during mechanical action, so a medium that is too soft burnishes and dulls instead of brightening. Alumina-based ceramic is the general-purpose choice for deburring, blending and satin finishes on stainless; steel media produces the brightest results on austenitic parts; plastic media suits softer or more delicate components and is usually the wrong tool for stainless cutting; dry media such as walnut shell or corn cob removes residue and moisture but does not generate a true stainless finish. The usual progression for an appearance part is a hard ceramic stage that removes the burr and machine marks, a finer stage that refines the texture, then a low-amplitude brightening stage. Whichever progression is proposed, treat it as a comparison to test on the real part rather than as a fixed recipe.

| Media | Best fit | Watch out for |
|---|---|---|
| Plastic media, polyester and urea based | Gentle deburring of delicate or thin stainless parts and of softer metals in mixed production, where edge loss must be minimised. | Low cutting power on stainless, can load with metal particles, and is generally the wrong tool for generating a stainless appearance finish. |
| Dry media, walnut shell and corn cob | Post-wet drying, light residue and scale removal, and dry polishing of surfaces that must not be re-wetted. | Does not cut stainless, generates dust, and leaves organic residue on parts if the medium is not kept clean and dry. |
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
| Alumina-based ceramic triangles and angle-cut forms | Heavy deburring, edge blending and machine-mark removal on stainless brackets, flanges and housings where corners and recesses must be reached. | Wears down in size and sharpness, so cutting rate falls without any setting change; broken pieces and fines can lodge in small features and must be screened out. |
Three routes answer narrow needs. Barrel and rotary finishing is the gentlest common bulk method, well suited to delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins, at the cost of longer cycles and less uniform coverage on large parts. Magnetic finishing uses small steel pins driven by a rotating field to deburr and brighten intricate internal features, slots, gear teeth and blind holes without lodging media in narrow passages, but it suits small part envelopes, and parts made from magnetic grades need to be tested before the route is assumed to apply. Dry polishing with a heated dryer handles post-wet drying, light scale and residue control after a wet stage; dry media alone does not cut stainless, and moisture left in a blind hole or a folded hem becomes a stain during storage.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Magnetic finishing machine | Small precise stainless parts with internal features, slots and blind holes that must be deburred without media lodging in the passages. | Works within a small part envelope, and the route has to be tested per grade because it depends on the part's magnetic response. |
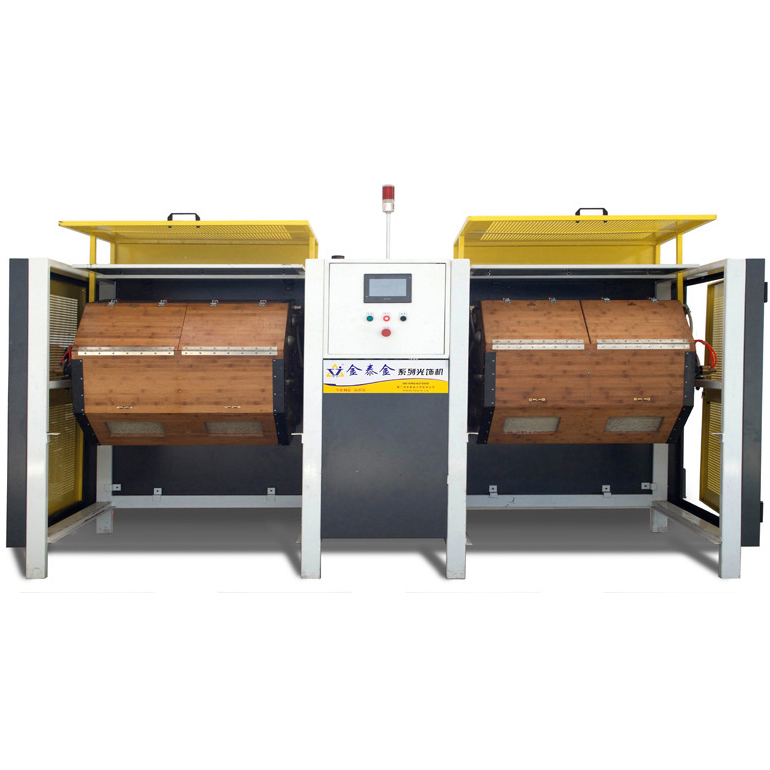
| Vibratory finishing machine, bowl type | General deburring and surface refinement of medium-sized stainless automotive parts such as brackets, small housings and flange blanks in a visible batch load. | Part size and shape are capped by chamber geometry, and thin or threaded parts may need compartments or fixtures to control part-on-part contact. |
| Continuous or indexed wet line with staged media charges | Multi-stage stainless finishing where deburring, refining and brightening are separated to control edge loss and texture progression. | Needs clear segregation between stages to prevent carry-over of coarse media or iron contamination, and adds handling and floor space. |
| Barrel finishing machine, rotary barrel tumbler | Gentle deburring and finishing of delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins. | Cycles run longer than in higher-energy machines, and coverage can be uneven on large or complex parts. |
Cross-drillings, tapped holes, folded hems and closed volumes are lodging sites, and a lodged medium is worse than a visible defect because it can travel to the customer, escape during cleaning, or damage a mating surface in service. Detection needs a defined routine rather than a shake and a look: weigh the part where that is sensitive enough, inspect internal passages with a borescope at agreed angles, confirm each passage with a pin or plug gage, and record the media count into and out of the batch. Weighing alone catches only gross lodges, since a retained chip may be a fraction of a gram. Where a feature cannot be inspected reliably after processing, the better answer is to plug or mask it before the cycle rather than to add inspection afterwards. Any media found downstream is a signal to redesign the separation step, not to add more inspection.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Uneven finish, with one region bright and another dull on the same part | Positional effects in the media mass, dead zones in the chamber, shielding by neighbouring parts, or a poor fill ratio in the load. | Mark reference locations, photograph under fixed raking light, and measure the same feature at multiple points on the part and across parts in the load to separate positional variation from process variation. |
| Heat tint, oxide or weld discolouration remaining after a light cycle | Incoming oxide from welding or laser cutting deeper than the finishing stage is designed to remove, or a finishing sequence that only brightens the surrounding surface. | Record the incoming oxide condition with photographs at agreed locations, then compare the same locations after processing and confirm whether removal of the oxide was inside the agreed scope. |
| Discolouration or mottling that appears only after drying | Mineral or compound residue carried in the final rinse, hard or chloride-bearing water, or slow drying that leaves a film on the brightened surface. | Compare wet and dry appearance under fixed lighting on the same parts, wipe a sample with a white lint-free cloth and solvent, and check the site water supply for hardness and chloride content. |
| Impingement marks, nicks or gouges on thin stainless panels and webs | Part-on-part contact in an under-filled chamber, excessive amplitude, or free parts striking each other where no compartment or fixture controls them. | Inspect the suspect feature under magnification and raking light before and after processing, and compare its location across several parts from the same load to confirm the defect is random rather than systematic. |
Breda combines logistics and distribution with an applied-technology and creative-technology base. The municipality is developing Innovatiedistrict Breda around two clusters, Robotics & AI and Games & Creative Technology, across the Slingerweg area, 't Zoet, the harbour area, the Chassekwartier and the Avans, BUas and Curio campuses. The Slingerweg area is being positioned as a hotspot for innovative makers with an emphasis on robotisation, where the Breda Robotics cluster and the Triple O Campus are located and more than 100 companies in the technology and creativity sector work. The city also operates the B'WISE startup incubator and provides business locations such as Rithmeesterpark, and its own business portal notes that local firms operate internationally in logistics.
The nearest part of that base to this brief is machinery: The Slingerweg area is designated as a hotspot for innovative makers with an emphasis on robotisation, offering space for experimentation, research and prototyping, and housing more than 100 companies in the technology and creativity sector including the Triple O Campus.
Breda's maker and robotics base, together with its logistics and business parks, generates demand for deburring and edge finishing of machined metal and plastic parts, sheet-metal enclosures, robot and machine frames and prototypes. Prototyping and small-series production place a premium on fast changeover and on processes that cope with mixed materials rather than on raw throughput.
A buyer should settle the batch profile first — prototype and small series versus repeat production — together with the material mix of aluminium, stainless, steel and plastics, because that determines whether a barrel, vibratory or disc process is the right starting point.
Freight context: Havengebied (harbour area within Innovatiedistrict Breda), Rithmeesterpark business park. Breda is a West-Brabant distribution location with business parks and a harbour area inside the innovation district, and local firms operate internationally in logistics. Machinery imported from outside the EU is declared to Dutch Customs at its point of entry, which for sea freight to this region will normally mean Rotterdam or Moerdijk.
Goods entering the Netherlands from outside the EU must be declared to Dutch Customs (Douane, part of the Belastingdienst); the importer needs an EORI number, import duty is calculated on the customs value (goods value plus transport and insurance to the EU external border), and import VAT is paid at the border unless an article 23 permit or a fiscal representative is used. CE marking is mandatory for most machinery placed on the EEA market: the Machinery Regulation replaced the Machinery Directive and manufacturers must comply with the new requirements by 20 January 2027. The importer must verify that the conformity assessment was carried out correctly, that CE marking is applied properly, that the technical file is present and complete, and that the user manual is supplied in the correct language; the manufacturer's EC Declaration of Conformity must be kept. Dutch companies imported over EUR 140 billion of machinery and appliances in 2024, 24% of total Dutch goods imports.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Appearance grading on stainless is best served by physical masters: one part at the acceptable limit and one at the marginal limit, viewed under the same lighting, at the same distance and at the same angle as production inspection. Lighting is the dominant variable in appearance judgment, so a master viewed beside a window in the morning will not agree with parts viewed under a machine light at night. Record the viewing conditions with the master, keep the master protected and dated, and photograph it as a supplement rather than as a replacement. For satin and brushed finishes, the master should also fix the direction and uniformity of the texture, since a part can meet a roughness figure and still look wrong beside a mating panel. Keep a small library of masters for the finishes this process actually produces, because a single nominal sample cannot cover a batch.
Moving from a trial to a producing line changes the process in ways the trial cannot show. Media wears during a long run, the compound bath accumulates swarf and dissolved metal, the load fill ratio changes with part mix, and handling steps multiply. A condition that held for a short cycle on five parts may drift over a full shift. Plan scale-up as a deliberate ramp: confirm that machine capacity and chamber geometry suit the real part, run the intended media charge to a representative wear state before judging results, and freeze the settings in a written work instruction with a media maintenance schedule. Decide in advance what will be measured during the ramp, at what frequency, and who is authorized to change a setting. Ramp-up risk is highest where the trial succeeded easily, because nobody is watching for the drift.

Hydrogen uptake is a documented concern for high-strength martensitic stainless steels when acid chemistry and mechanical work are combined, and it is not visible on the surface. The practical route is to state the material and hardness in the enquiry, ask which compound families are proposed and at what concentration, and confirm with your own engineering function whether any post-finishing treatment is required and within what window. SurfacePolish can describe the compound family and the process conditions used on a trial, but fitness for a given strength level, and any treatment specification that follows, must be defined and verified by the buyer.
They are different processes with different effects, and SurfacePolish does not supply or perform electropolishing. Mechanical finishing works by media contact, so it blends, deburrs and brightens the surfaces the media can reach, and it rounds edges as it works. Electrochemical treatment removes material ionically and reaches into recesses that media cannot. Where an electropolished surface is specified for corrosion or cleanliness reasons, treat electrochemical processing as a comparison point and ask whether the specified requirement can be met by another route, then verify that on your own parts and against your own acceptance rule.
Treat them as two separate requirements rather than one. Map exterior visible surfaces, hidden surfaces and every edge that has a job such as sealing, bearing or assembly clearance. Appearance zones tolerate broad blending; functional edges need a stated limit and a measuring method. The two often pull in opposite directions, because the cycle that brightens a panel also removes material fastest at exactly the edges that must stay inside a band. Ask the designer to confirm colour, texture and direction on visible faces, and put the edge requirement in writing with its instrument before any media is chosen.
Use Breda, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers here would reference the CE machinery regime (Machinery Regulation from 20 January 2027) and the Dutch/EN-ISO surface-finishing standards published by NEN, such as NEN-EN-ISO 2080. Where parts feed logistics-equipment or robotics customers, the customer's own supplier specification for edges, roughness and cleanliness is normally the binding requirement.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Breda.
The buyer needs a consistent bright finish on the visible face without distorting the thin frame or impinging the pierced openings.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0682; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0682 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
