A column-cover fabricator in Nottingham, United Kingdom for architectural metalwork handles 6 m lengths of 168 mm stainless tube at 3 mm wall and needs an even finish on the visible half without losing roundness or denting the wall in handling. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on cut sections and one full length shipped to Xiamen. This brief is written for a buyer in Nottingham working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
What is the longest length in the order, and how will it be supported, carried and packed at every stage between finishing, fabrication and installation?
Which wall thickness and section shape in the order is most likely to distort, and what fixture, cradle or support will protect it?
What texture direction is required, and how will that direction be preserved and compared across lengths that are finished in different lots?
Not every face of a profile deserves the same effort. On a wall-mounted handrail the top and the outward face are read from standing height and from an angle, while the underside and the face against the wall are largely out of view. On a cladding mullion the sun-facing plane carries the reflection and the returns do not. Build a simple exposure map: which face, viewed from where, under what light, at what distance. That map settles where the tighter finish is specified and where a coarser one is honest. It also prevents over-finishing hidden faces, which costs cycle time and raises the risk of distortion on thin sections, and it tells the finishing supplier which face must be protected in every rack and stillage.
The compound carries cut debris away, keeps the media from loading, and buffers the chemistry against the metal. For stainless work the choice sits between mildly acidic, neutral and alkaline families, with the selection driven by the alloy, the incoming surface and the buyer's own residue limits rather than by a fixed rule. The behaviour that matters most on tube is rinsing. A compound that clings inside a six-metre bore will bleed out later onto a visible face and read as a stain or a patch. Pick a family that rinses cleanly, specify the rinse stages and the drying step, and agree how the interior of a sample length will be checked after the trial rather than assuming it is clean.

| Media | Best fit | Watch out for |
|---|---|---|
| Steel media, pins and balls | Bright, strongly linear appearance on stainless where a higher-lustre finish is wanted on accessible faces. | Heavy, needs tight compound control to stay clean and separated, and any iron-bearing debris is a contamination question the buyer has to define and verify. |
| Plastic media, cones and triangles | Gentle work on thin-wall sections and softer alloys, and where marking or distortion is the main risk to be managed. | Slower cut and shorter media life, with limited effect on a deep scratch or a heavy seam. |
| Plastic media, cylindrical | Light surface refinement on thin rectangular sections where holding the shape matters more than cutting power. | Little cut power, and the size class changes quickly as the media wears, which shifts the texture pitch over a run. |
| Grinding media, alumina-based | Higher material removal where a mill seam, a joint weld or a deep transit scratch has to be cut back before refining. | Aggressive on thin wall, can over-round edges and change cross-section geometry, and needs tight depth control. |
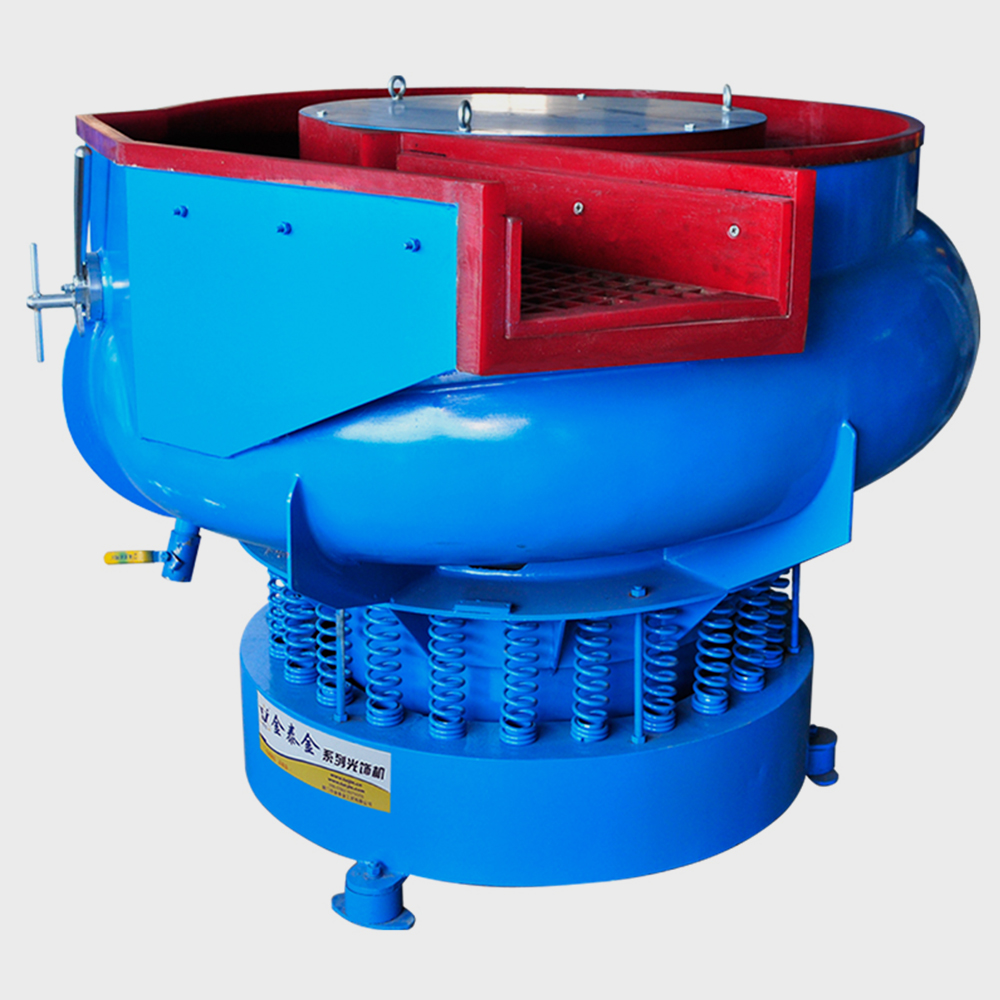
A tub vibrator uses a long rectangular chamber, so the process length can be extended along one axis while the bed depth stays modest. That allows a length to be carried through a media bed deep enough to work the visible face and shallow enough to keep the load moving. Decisions to settle with the equipment supplier are the usable chamber length against the longest part, whether lengths run one at a time or several end to end, how the part is supported so it does not ride on top of the media, and how the open ends are kept clear of media. A tub also tolerates the mid-length supports that thin rectangular sections need, which a circular chamber cannot accommodate without a purpose-built fixture.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Vibratory finishing machine, bowl type | General edge blending and surface refinement on brackets, base plates, cut spindles and other small fittings. | Chamber diameter caps the part length, and a long tube cannot be worked evenly in the circular bed. |
| Dry polishing machine and dryer | Post-wet drying and dry luster work, particularly where a hollow section must come out clean and dry inside. | Dry routes cut less than wet media, and dust control and media separation need planning. |
| Magnetic finishing machine | Small precise parts and localised areas that are difficult to reach with loose media in a conventional chamber. | Size and mass limits keep it away from architectural lengths and large diameter profiles. |
| Disc finishing machine | Fast, high-energy cycles for small to medium fittings and hardware where a short cycle is the priority. | The high energy that makes it fast will distort, mark or bend thin and long parts. |
A surface can measure inside a roughness band and still fail visually. Orange peel, a mottled texture with a pitch of a few millimetres, appears when the surface is over-worked with a coarse medium or worked with too much pressure on a soft or thin section. Hazing is the diffuse, milky appearance that follows a fine but non-uniform cut. Both are geometry effects rather than amplitude effects, so a profilometer reading across them may be entirely acceptable while a reflection test shows a broken image. This is why an architectural finish cannot be accepted on a roughness number alone, and why a visual standard viewed under defined light at a defined distance has to sit beside the numeric one. Ra and appearance answer different questions.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Twist along the length | Differential working of opposite faces, or clamping and stacking that loads the section unevenly. | Rest the length on a reference surface and compare the angular orientation of the two end sections with a square. |
| Shade change or discolouration at a welded area | The heat-affected zone responds differently to the same media and compound cycle than the parent metal. | Compare the area with adjacent metal under the agreed light and distance, and photograph it with a scale alongside the retained reference. |
| Bow along the length | Unsupported part in the bed, resting on hard supports, or lengths stacked while still wet. | Place on a surface plate or straight reference and measure the gap with a feeler gauge at several stations, against the incoming straightness record. |
| Orange peel mottling on the visible face | Over-working with a coarse medium, or excessive pressure on a soft or thin section, which deforms the surface rather than cutting it. | Reflect a straight edge or a linear light source in the surface, and take a roughness reading at the same spot to show the divergence between number and appearance. |
Nottingham is a Nottinghamshire authority inside the East Midlands Freeport, the only inland UK freeport, whose three sites are East Midlands Airport and Gateway Industrial Cluster (EMAGIC) in Leicestershire, the Ratcliffe-on-Soar power station site in Nottinghamshire, and the East Midlands Intermodal Park in Derbyshire. The freeport states its sites are connected by road, rail and air and within easy reach of East Midlands Airport, which it calls the UK's largest dedicated airfreight airport, and it reports that a share of the UK's major freight rail lines are serviced through the East Midlands. Nottingham City Council provides the city's business licensing, trading standards and procurement services, and the East Midlands Chamber is the regional chamber of commerce.
The nearest part of that base to this brief is energy: East Midlands Freeport lists the Ratcliffe-on-Soar power station site in Nottinghamshire among its three sites and states it is accelerating the region's commitment to decarbonisation through sustainable development and low-carbon energy investments.
The East Midlands Freeport is built around freight and low-carbon industry sites rather than a legacy machining cluster, so finishing requirements in the Nottingham area follow the parts being made and moved rather than any single local process tradition. Because the freeport's sites connect by road, rail and air and the East Midlands is a major goods-importing region, deburring, edge and cleanliness specifications should be taken from the component drawing and its downstream assembly rather than from a general local practice.
A Nottingham buyer should tie the finishing specification to the part's actual route out of a freeport or industrial site - air, rail or road - and confirm media and compound handling and waste arrangements before the machine is ordered.
Freight context: East Midlands Airport (described by East Midlands Freeport as the UK's largest dedicated airfreight airport), East Midlands Intermodal Park, Derbyshire, Ratcliffe-on-Soar power station site, Nottinghamshire. East Midlands Freeport describes itself as the only inland UK Freeport, with sites connected by road, rail and air and within easy reach of East Midlands Airport; it states that a share of the UK's major freight rail lines are serviced through the East Midlands.
Importers need a GB-prefixed Economic Operators Registration and Identification (EORI) number, an import declaration carrying the correct commodity code, and retained commercial invoices plus the Import VAT Certificate (C79) so import VAT can be reclaimed. Machinery placed on the Great Britain market must be marked UKCA or CE: the manufacturer must draw up and retain technical documentation including a Declaration of Conformity, apply the correct marking with identification details, and cooperate with market surveillance; an authorised representative must be established in the UK. Under the Product Safety and Metrology (Amendment) Regulations 2024 the UK continues to recognise CE marking alongside or in place of UKCA for the Great Britain market, so either route can be used for most product types. Duty and import VAT are calculated from the customs value declared, and the commodity code also determines whether an import licence is needed.
China does not appear in the alphabetical list of trade agreements in effect published by the Department for Business and Trade, so Chinese-origin machinery imported into the UK cannot claim a preferential agreement rate. Duty is instead determined by the commodity code declared on the import declaration, and the UK's customs authority is HM Revenue and Customs (HMRC), which ONS also names as the largest single data source behind UK trade-in-goods statistics. Because a GB-prefixed EORI number is a precondition for importing into England, Scotland or Wales, a Chinese seller's UK buyer must already hold that registration before any machine ships.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A six-metre length cannot be examined in every square millimetre, so the acceptance plan has to say where the checked zones are and how often they are checked. Define stations along the length, for example near each end and at one or two intermediate points, decide whether the visible face of every length is checked or only a percentage of the batch, and set the reaction when a station fails: quarantine the lot, measure the rest of the lot, and record the finding. Keep the first accepted length as a physical reference and re-photograph it under the agreed light whenever the lighting setup changes. Photographs taken on different days with different cameras are a poor substitute for the retained part, though they are useful supporting evidence when the setup is fixed.
The first production batch is usually the best one, because the media charge is fresh and the fluid is at its set point. What changes over a run is media wear, which reduces cut and shifts the surface toward a finer and dimmer appearance; the build-up of swarf and fines in the fluid; and the arrival of material from a different heat or mill finish. Plan for it: a media top-up and screening routine with a defined interval, a fluid change criterion based on measurement rather than appearance, and a check length kept from each lot for comparison. Agree in advance what will be done if a later lot does not match the retained reference, so the decision is procedural rather than improvised.

No. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and runs a free sample trial on parts the buyer sends. The tube, pipe and profiles remain the buyer's own material from their own mill or stockholder, and we do not verify its grade, mill certificate or corrosion performance. Keeping those roles separate matters, because the appearance a finishing line can reach is limited by the incoming material: its alloy, its hardness, its existing grain and the condition it arrives in. Send material from the actual delivery rather than a hand-picked offcut.
No. SurfacePolish does not supply or carry out electropolishing. Where electrochemical treatment is part of the buyer's requirement, we treat it as a comparison point and as a reason to look at what a mechanical route can achieve on the same part, and we can discuss media, compound and machine options for that mechanical route. A mechanical finish should not be presented as equivalent to an electropolished surface, and the choice between the two, together with any specification that depends on it, belongs to the buyer's own engineering decision.
A round bowl moves its load on a circular path in a chamber whose diameter caps the part length, and extending that chamber to take a six-metre length stops being practical. The deeper issue is the bed: a long tube occupies too much of the load for the media to circulate around it, so the part is dragged and struck instead of worked evenly. Long sections are better run in a tub, where the process length can be extended along one axis, or on a dedicated arrangement that moves the part or the heads along the length.
Use Nottingham, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Equipment placed on the Great Britain market requires UKCA or CE marking with a Declaration of Conformity, and HSE's work equipment and machinery and COSHH regimes cover finishing machines, media and compounds. Nottingham City Council's trading standards service and business licensing function are the local points of contact for product and trading rules.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Nottingham.
The visible half needs an even finish while the roundness and the wall are held through every handling step.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0297; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0297 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
