PURCHASING SCOPE GUIDE How to Compare Mass Finishing Quotations for CNC Metal Parts Compare trial evidence, equipment scope, separation, drying and acceptance conditions before choosing a mass finishing quotation for industrial CNC parts. Quick answer: Two quotations with similar machine capacities may describe very different production systems. For CNC metal parts, compare the part specification ...
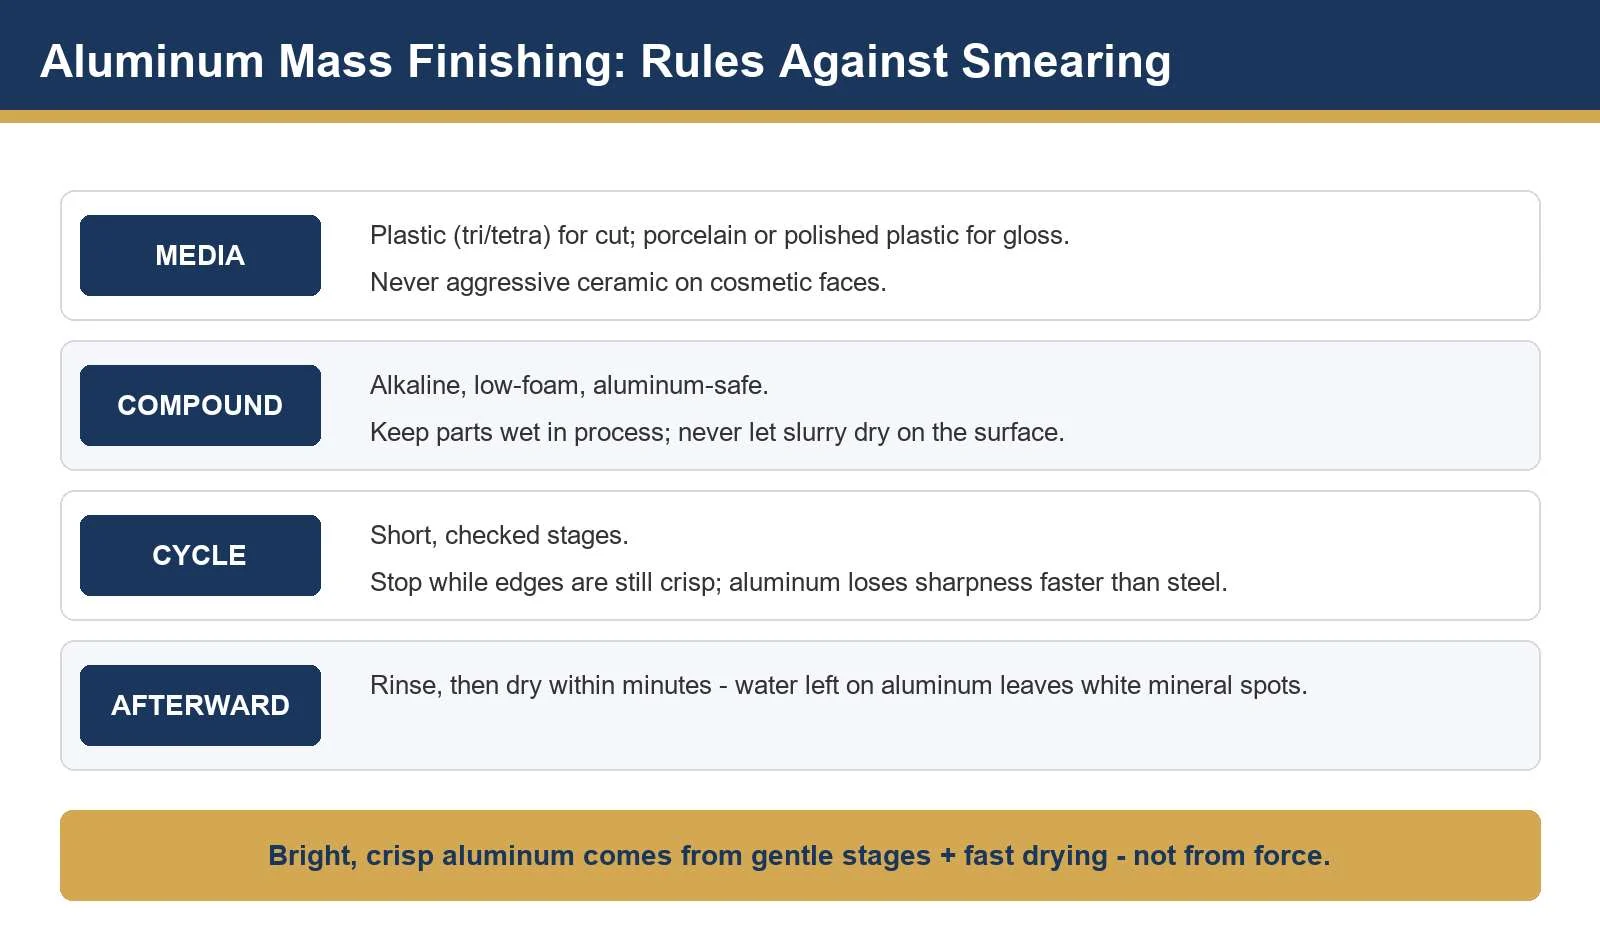
Mass Finishing Aluminum Parts: Deburr, Smooth and Brighten Without Smearing Aluminum surface finishing • Media, compound and cycle selection • From CNC parts to cosmetic components Aluminum is one of the most rewarding — and least forgiving — metals to mass finish. It deburrs fast, smooths beautifully, and polishes to an attractive satin-bright look. But it also smears under aggressive media, stai...
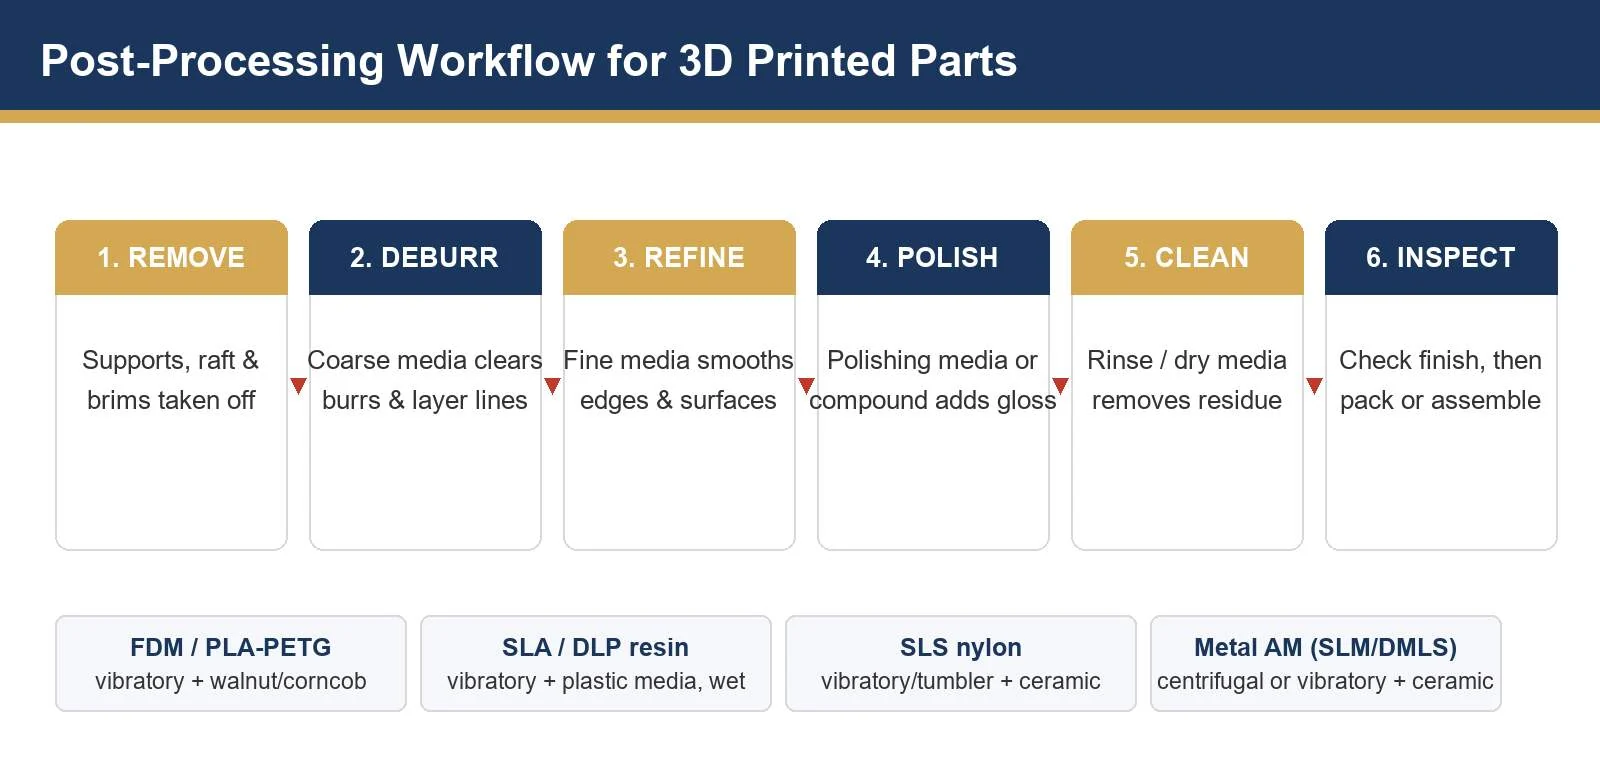
Mass Finishing for 3D Printed Parts: Deburring and Polishing Additive Manufacturing Components Additive manufacturing post-processing • Deburring, smoothing & polishing • FDM, SLA/DLP, SLS & metal AM parts 3D printing turns out parts close to final shape, but almost never close to final surface. Support scars, layer lines, partially fused powder, and sharp edges stand between a fresh print...
Printable Process-Control Resource Mass Finishing Sample Trial Record for Small Precision Parts Use this non-promotional worksheet to define the incoming part, record one controlled finishing trial, compare results, and decide whether the process is ready for a repeat run. Important: This record does not replace a drawing, control plan, safety procedure, material compatibility review, or customer ...
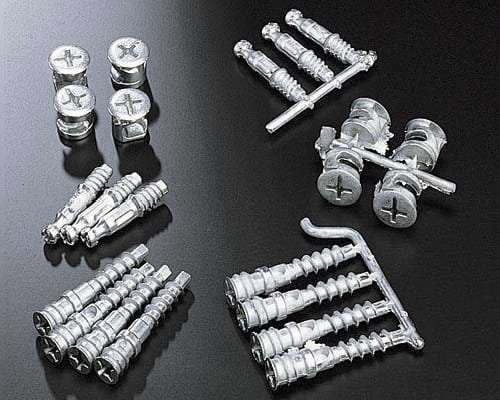
Small Parts Finishing Guide How to Deburr Small Fasteners Without Damaging Threads, Points, or Recesses Screws, bolts, nails, pins, and rivets can be processed in bulk, but their functional features make them less forgiving than simple metal blanks. The right mass finishing process must remove loose burrs while protecting threads, points, drive recesses, hollow sections, and dimensional fit. Small...
Plastic and Rubber Part Finishing Guide How to Deburr Plastic and Rubber Parts: Mass Finishing, Media, and Process Limits Flash, gate marks, machining burrs, and rough build lines do not all respond to the same finishing method. This guide explains when mass finishing is a practical option for plastic and rubber parts, how to select equipment and media, and when trimming, blasting, or cryogenic de...
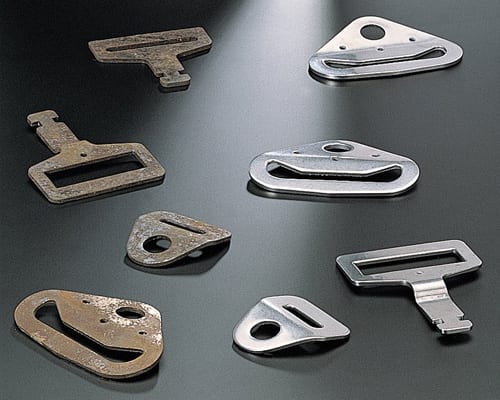
Stamped Parts Finishing Guide How to Deburr Stamped Metal Parts Without Tangling, Distortion, or Part-on-Part Damage Stamped washers, clips, brackets, and thin sheet-metal parts can be efficient mass-finishing candidates, but their geometry creates risks that solid machined parts do not have. This guide explains how to evaluate the burr, select a machine and media, control part interaction, and bu...
Wet Finishing Troubleshooting How to Prevent Water Spots,White Film,and Cloudy Stainless Steel After Tumbling A stainless steel part can look clean while wet and develop spots,h
Production Separation Guide How to Separate Small Parts from Tumbling Media: Screens, Size Control, and Process Design A finishing cycle is not production-ready until parts can be separated from media repeatedly. This guide explains how part geometry, media wear, screen design, orientation, and external separation methods affect labor, carryover, and the risk of trapped media. Part-media separatio...
We use essential storage to keep this site working. With your permission, Google Analytics 4 helps us understand visits and improve the site. Advertising storage, ad user data, and ad personalization always stay off.





 IPv6 network supported


 +86-592-2381506
