In Grenoble, France, an industrial machinery buyer wants a cast iron handwheel rim and spokes brought to an even bright finish despite the graphite structure and small voids in the casting. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial, returning the tested parts with observations and a proposed process direction for the buyer's own review. This brief is written for a buyer in Grenoble working on industrial machinery; it describes equipment, media and a scoped sample review, not a local polishing service.
What is the substrate condition - cast, welded, forged or machined - and which defects already in it will become visible once the metal is smooth?
Can available media actually reach the geometry, and what finish is realistic in the recesses and internal features it cannot reach?
Which faces must reach a mirror and which only need to be clean and uniform, and how is each one judged?
Every mirror sequence removes metal, and the removal is rarely uniform across a large face. Datum pads, dowel registers, bearing seats and seal lands carry assembly geometry, so measure them before finishing and agree a dimensional and flatness allowance. Where an allowance is tight, mask the feature, finish around it by hand, or plan a light final lapping pass that keeps the face flat. A part that looks correct but has lost flatness on a mounting face will not assemble squarely, and a curved cover panel shows a distorted reflection after only a few hundredths of a millimetre of uneven stock removal. Record incoming values with the same instruments that will accept the finished part, at the same marked locations.
Compound concentration is a process variable that drifts. Dosing on a timer is convenient but ignores carry-out, evaporation and the fines load, so a batch that starts at target can finish well above or below it. Meter dose against water flow, check pH and, where available, conductivity at the start and end of a cycle, and record those values with the batch. Water quality shapes the final image: hard water leaves mineral spots that read as haze, and high chloride or iron content can stain stainless during rinsing. The rinse after each stage deserves the same control as the finishing stage, with enough volume and flow to remove compound and loose fines before the part dries, because dried residue is far harder to remove without disturbing the finish.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media - walnut shell | Dry polishing, light deburring and lubricity on parts where a residual oil film is acceptable, and drying or lustre steps after wet processing. | Not a stock-removal medium, generates dust that needs extraction, and can leave an oily film that interferes with a later cleaning or coating requirement. |
| Dry media - corn cob | Softer dry lustre and drying steps, absorbent polishing of small parts, and light work on brass, aluminium and plated-look surfaces. | Breaks down faster than walnut shell and must be replaced regularly; it removes almost no material and cannot correct a surface defect. |
| Small high-density ceramic spheres or ovals | Colour and pre-lustre stages where a uniform, soft-looking finish matters more than stock removal, including curved and contoured faces. | Very slow cut, easily lost through screens sized for larger media, and ineffective in deep recesses because it cannot reach or press against the surface. |
| Coarse ceramic angle-cut cylinders or triangles | First cut stage on rigid parts with open faces, removing grinding or machining damage on cast iron, steel and stainless before refinement. | Leaves a deep pattern the next stage must fully erase, chips thin edges, and its wear debris carries fine abrasive into later stages if the charge is not screened. |
Rotary barrels work by sliding contact and suit parts that tolerate tumbling, giving a dense, uniform colour on small hardware. They cannot process anything longer than the barrel diagonal, so long shafts, extrusions and frame members belong in a tub vibrator, where a part can pass through the mass without being folded. Slender parts need support or careful load balancing, because the same energy that brightens a shaft can bow it or nick it against a neighbour. Barrel and tub routes reach some external areas a bowl cannot, such as a long groove, but they are poor at bores running parallel to the long axis. Verify straightness and roundness after the cycle, not only appearance.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Tub vibrator | Long and large parts such as shafts, extrusions and frame members that cannot be folded into a barrel, including external grooves. | Poor at bores running parallel to the long axis, and slender parts still need support or balanced loading to hold straightness. |
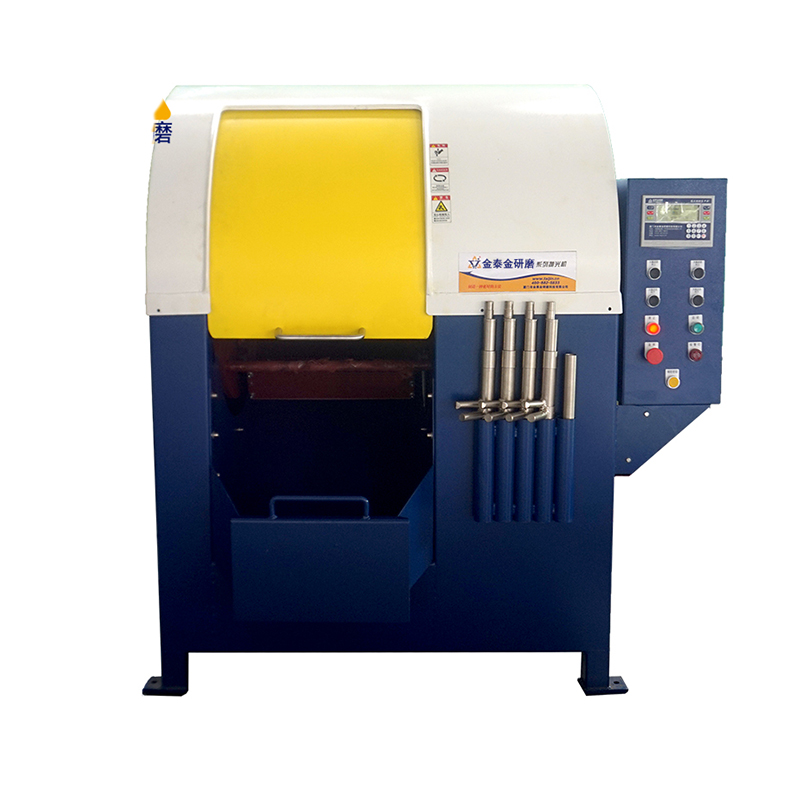
| Centrifugal barrel finishing machine | High-speed cut down and refinement on small to medium parts where a short, energetic cycle is needed before colour stages. | Aggressive on edges and thin sections, requires tight cycle control, and does not replace a finer refinement stage. |
| Disc finishing machine | Fast, high-energy cut down on small to medium parts with simple geometry where cycle time matters and edge rounding is tolerable. | Part-on-part contact and wall pressure can chip or deform parts, and the difference between sufficient and excessive removal is narrow. |
| Grinding finishing machine | The heavier stock-removal stage before a mirror sequence, cutting back grinding damage, scale and recast layers on robust parts. | High removal also rounds edges and can work harden or distort thin sections, so it needs a defined depth target and a sample check. |
Beyond a certain point, more polishing makes a surface worse. Excess cycle time or contact pressure rolls metal over instead of cutting it, burying abrasive and debris under a smeared skin that looks bright until it is disturbed. On dry or high-speed operations, friction raises local temperature enough to tint the surface and soften a hardened layer, and thin sections can distort from the heat. High-energy routes add part-on-part impingement, leaving nicks and small dents that polishing cannot remove. Watch for a bright surface that dulls or streaks when wiped with a clean cloth, for colour variation near edges where contact is highest, and for dimensional or flatness change. The remedy is a shorter or gentler cycle, better cooling and a real end point instead of a longer run.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Smearing or a rolled surface with abrasive and debris buried in it | Excessive cycle time or contact pressure, insufficient compound lubricity, or a final stage run at energy the material cannot absorb without deforming. | Wipe a defined area with a clean white cloth and look for streaks or dulling, then examine at magnification and compare microhardness or etch response against an unmachined reference. |
| Haze, a general loss of image clarity with no directional pattern | Worn media shedding an oversized fine fraction, agglomerated abrasive in the compound line, or fine grit carried into a late stage from screens, machine walls or a shared rinse. | View under raking light at low magnification against a master, then trace the pattern by machine and by rinse line to separate a charge problem from a rinse or transfer problem. |
| Compound residue film, water spots or a dull bloom after drying | Incomplete rinsing, hard or contaminated rinse water, a dose above target, or drying that leaves a cavity to bleed residue onto the finished face. | Wipe a defined area with a clean white cloth after drying, inspect cavities for bleed-out, and check rinse water hardness or conductivity at the point of use. |
| Orange peel, a slow wave that distorts the reflected image | Soft or work-hardened surface deformed rather than cut, a heavy cut stage followed by too little refinement, or a dry or buffing stage at high speed with excess pressure. | Reflect a straight edge or fluorescent tube in the face at a shallow angle, compare the shape of the image against a physical master in the same lighting, and repeat at several viewing angles. |
Grenoble is a high-technology manufacturing city rather than a heavy-industry one: INSEE counted 6 428 establishments in the commune at the end of 2024 with a 4,0 % industry share - high for a city of 156 140 inhabitants - plus 100 725 jobs at the place of work in 2023, concentrated in research, engineering and precision industry. The Alpine conurbation is a recognised microelectronics and semiconductor centre hosting major device and equipment operations, and Minalogic, the digital-transformation cluster for Auvergne-Rhone-Alpes, runs a dedicated micro/nano/electronics theme alongside industry-of-the-future and photonics themes from its Grenoble-area base. Tenerrdis and the local energy research ecosystem add a second pillar in energy and electrochemistry.
For this brief the relevant part of that base is machinery: INSEE records 6 428 establishments in Grenoble at end-2024 with a 4,0 % industry share and 100 725 jobs at the place of work in 2023, a base of precision manufacturing and equipment engineering serving the technology clusters.
Precision and micro-technical manufacturing leaves little tolerance for burrs: fluidic and vacuum components, instrument bodies, valve and manifold parts and machined fixtures must be burr-free at edges that are too small to inspect visually, and surface roughness affects sealing, flow and particle generation. Contamination control is a live issue because cleanroom and vacuum environments reject both metallic debris and organic residue from compounds. The instrumentation and energy-equipment side of the Grenoble base also needs repeatable cosmetic and functional finishes on stainless and aluminium parts.
A Grenoble buyer should settle which surfaces are functionally critical and how cleanliness will be measured, because in precision and vacuum work the acceptance test - not the machine specification - decides whether a vibratory or centrifugal process is acceptable at all.
Freight context: Grenoble Alpes-Isere Airport, Lyon-Saint Exupery Airport (regional long-haul gateway), Port Edouard Herriot / Rhone-Saone waterway (Lyon corridor). Grenoble has no seaport and relies on Lyon's airport and river terminal plus road haulage from the Rhone corridor and Mediterranean ports; the metro is served by Grenoble Alpes-Isere airport for regional and business traffic. Precision parts and media samples move by express courier, while machines come by road from the ports, which makes unloading access and floor-space planning at the plant the practical constraint.
France applies the EU common commercial policy, so industrial machinery arriving from China enters under the Union Customs Code and the Common Customs Tariff rather than under any bilateral French regime; the EU has no free-trade agreement with China, so no preferential duty rate applies and normal third-country duties are due on the customs value. Importers classify the machine in the tariff nomenclature and lodge a customs declaration; French Customs publishes the common and national tariff through its RITA online service and states that three notions are fundamental: the tariff classification of the product, its origin or destination, and the value of the goods.
For imports from outside the EU the declarant must file a customs declaration whose form and content are fixed by the Union Customs Code and its implementing provisions; French Customs identifies classification, origin and value as the three fundamental notions and makes the common/national tariff consultable via RITA. The customs authority is the Direction generale des douanes et droits indirects (DGDDI), which also runs the Info Douane Service for formalities questions. Buyers should expect to need an EORI number and an EU VAT treatment, because customs and tax authorisations are handled together (SOPRANO). For machinery, the CE marking and the applicable EU product-safety directives are the compliance gate items to settle before shipment, and the French market surveillance authority is the DGCCRF; the tariff rate itself must be confirmed per HS code in RITA or the EU Access2Markets tariff tool, since it varies by machine type.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Cosmetic acceptance is only half a disposition. Measure the dimensions and flatness that assembly depends on, gauge or thread-check features that media could enter or round, and run the functional check the part actually needs, whether that is seal condition, bearing fit, sliding contact, flow or leak. Cleanliness needs its own verification rather than an assumption: flush blind holes and passage intersections, borescope them at an agreed angle, and examine what the flush carries out. Wipe a defined area with a clean white cloth and record what appears, since compound residue and iron pickup often show only after drying. Confirm cleanliness after drying, not before, and record the method so the next batch is judged on the same basis.
Send parts that represent the real production spread, not the one clean sample on the desk. Include the thinnest wall, the tightest internal feature that must stay clear, the worst edge, and one as-received reject if you have one. Add a witness coupon of the same material and condition for texture measurement, and label every piece so a returned part can be matched to its settings. Supply the material and heat treatment, the drawing extract covering the finished faces, and the acceptance requirement you intend to apply. Photograph the incoming condition at fixed scale before packing, protect edges and bright faces in transit, and state what the trial must answer. Unlabelled, unrepresentative parts produce observations that cannot be used.

No to both. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and it does not supply or perform electropolishing or operate a plant, branch, dealer or technician service in France or any other market. What is offered is equipment and consumables, a scoped discussion of a finishing line concept, and a free sample trial in which representative parts are shipped to Xiamen and returned with observations and a proposed process direction. Where an electrochemical finish is under consideration, the discussion stays a comparison with a mechanical route.
Haze and sleeks usually come from contamination rather than from a wrong final medium. Worn media shed an oversized fine fraction, abrasive can agglomerate in the compound line, screens and machine walls carry grit from an earlier coarse stage, and a shared or under-controlled rinse moves particles forward. Inspect under raking light against a master and trace the pattern: defects that appear in one machine point to the charge, while those spread across machines point to rinsing or handling. Clean the charge, screen the media and re-establish the rinse before changing the compound.
The pits were in the casting before polishing. Bright finishing compresses the surface into a narrow reflected image, so gas porosity, shrinkage voids and non-metallic inclusions become far more visible once the surrounding metal is smooth, and additional fine polishing only makes them clearer. The options are to move the requirement to a satin or blasted finish that tolerates the surface, change the casting route or the location of the visible face, or accept a written level of visible pits. A trial can show how current castings respond; it cannot remove a defect below the surface.
Use Grenoble, France as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Grenoble buyer would specify surface texture with ISO/NF EN surface-texture standards and add cleanliness requirements (particle and residual-film limits) where components go into vacuum, fluidic or cleanroom service; ISO 9001 is the baseline, with ISO 13485 where medical devices are involved and customer-specific semiconductor-equipment specifications layered on top. AFNOR publishes the NF/NF EN versions of the ISO standards used on the drawings.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Grenoble.
The buyer wants the rim and spokes to look uniformly bright despite the graphite structure and small surface voids of the casting.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0569; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0569 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
