An industrial machinery buyer in Groningen, Netherlands needs a copper electrode plate finished bright and clean, with no embedded media or compound residue left on the contact face. SurfacePolish supplies finishing machines, media and compounds internationally and offers a free sample trial, returning the tested plates with observations and a proposed media, compound and cycle direction rather than a guarantee. This brief is written for a buyer in Groningen working on industrial machinery; it describes equipment, media and a scoped sample review, not a local polishing service.
What is the substrate condition - cast, welded, forged or machined - and which defects already in it will become visible once the metal is smooth?
Can available media actually reach the geometry, and what finish is realistic in the recesses and internal features it cannot reach?
How much stock may the sequence remove before datums, seal faces, flatness or edge form fall outside their allowance?
Bright polishing rounds edges, and the more energy and time the sequence needs, the more rounding appears. Some edges are cosmetic and rounding is welcome; others define function, such as a scraper edge on a machine-tool slideway, a knife edge on a metering blade, a thread start, or the lapped lip of a valve seat. Mark those features on the drawing and state a maximum edge radius or a no-touch zone before media is selected. Inspection can use radius gauges, a cast impression or an optical comparator against the incoming edge form. Where a crisp edge and a bright face conflict, the practical order is to finish the face first and restore the edge with a controlled hand operation, or to accept a slightly duller face that preserves the edge.
Ceramic media cuts well and holds shape, which keeps the working geometry predictable, but dense ceramic can chip thin edges and its wear debris becomes fine abrasive that carries into later stages. Plastic media is light and gentle, which suits aluminium and brass, though lower density means less contact force and a longer cut stage. Steel media burnishes rather than cuts and gives the brightest wet result on stainless and hardened steel, but it can transfer iron and rust if compound and rinse do not protect the load. Dry media such as walnut shell or corn cob is used for lubricity and drying rather than stock removal. Every medium wears, so measure size loss and replace on a schedule: a worn charge finishes differently and no longer describes an earlier trial result.

| Media | Best fit | Watch out for |
|---|---|---|
| Medium ceramic triangles or angle-cut shapes | Blending, edge conditioning and the refinement step that removes the coarse cut pattern on housings, brackets, covers and frames. | Media that cannot enter a slot or recess leaves those areas at a different finish, so those faces need a separate operation or a stated lower standard. |
| Plastic or polyester media | Gentle processing of aluminium, brass, copper and thin panels where metal smearing, nicks and distortion must be avoided. | Low density gives little contact force, so cycles run long and heavy grinding marks may survive; plastic also wears quickly and can float above the working mass. |
| Dry media - corn cob | Softer dry lustre and drying steps, absorbent polishing of small parts, and light work on brass, aluminium and plated-look surfaces. | Breaks down faster than walnut shell and must be replaced regularly; it removes almost no material and cannot correct a surface defect. |
| Hardened steel media, balls and shaped shot | Bright burnishing of stainless and hardened steel, and the final wet lustre stage where a dense medium can peen a surface smooth. | Can transfer iron and rust to stainless, dents soft or thin parts, and must be kept in a dedicated charge away from ceramic media. |
A mirror finish is a sequence of progressively finer steps, each removing the pattern left by the one before it, and no single machine substitutes for the whole sequence. A typical line separates cut down, refinement, colour and final lustre, with rinse, inspection and drying between stages so coarse particles and dried residue do not travel forward. Running one vibrator longer at one media specification tends to plateau: the surface reaches the limit of that media and stops improving while edges keep rounding and dimensions keep shrinking. Plan the line as a route with a defined finish at each stage, decide which stages share a machine and which need their own equipment, and treat transfer, rinsing and drying as process steps with their own controls.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Centrifugal barrel finishing machine | High-speed cut down and refinement on small to medium parts where a short, energetic cycle is needed before colour stages. | Aggressive on edges and thin sections, requires tight cycle control, and does not replace a finer refinement stage. |
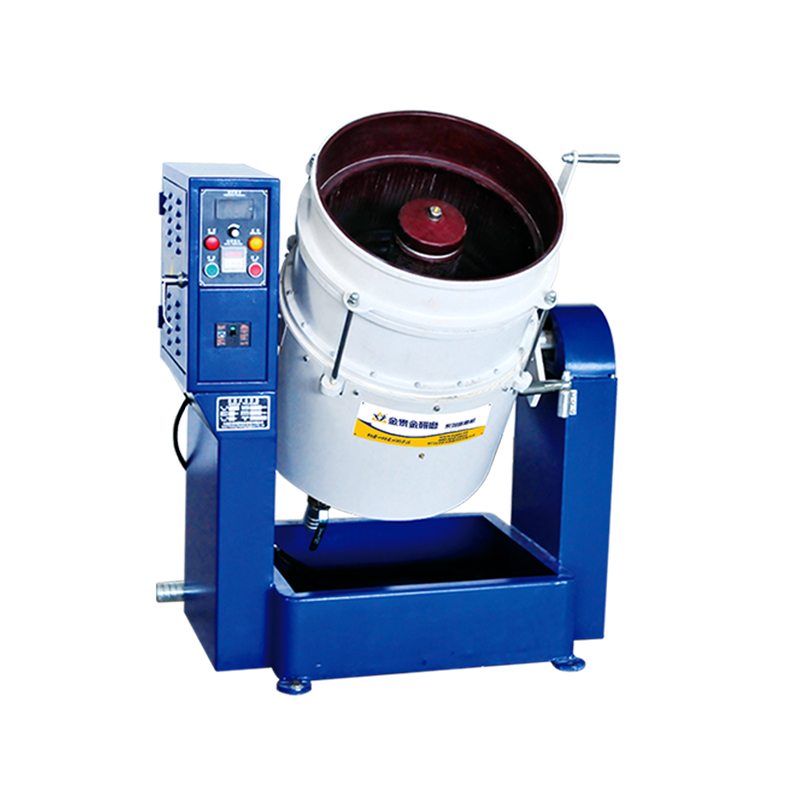
| Barrel finishing machine / rotary barrel tumbler | Dense, uniform colour on small hardware that tolerates sliding contact, especially with steel media for a burnished appearance. | Nothing longer than the barrel diagonal can be processed, and slender parts can bend or nick against neighbours in the load. |
| Disc finishing machine | Fast, high-energy cut down on small to medium parts with simple geometry where cycle time matters and edge rounding is tolerable. | Part-on-part contact and wall pressure can chip or deform parts, and the difference between sufficient and excessive removal is narrow. |
| Vibratory finishing machine (bowl or tub) | Cut-to-colour sequences on rigid, mostly open parts such as housings, covers, brackets and frames, with adjustable energy and no fixturing. | Cannot present media uniformly into pockets with narrow mouths or deep internal bores, and broad flat faces finish more slowly than edges. |
A bright face can carry a ghost of every earlier stage. When a coarse grinding or cut pattern is not fully removed, the finer stages polish the crests and leave the valleys, producing visible lines or a woven crosshatch that reappears as the viewing angle changes. The causes are a stage that removed too little, a refinement step that reused a contaminated charge, or a crosshatch direction that was never rotated between steps. Each successive stage should run across the previous direction at a clear angle, so an operator can see when the earlier pattern is gone. Inspect by reflecting a light source at a shallow angle and rotating the part: a mark that vanishes at one angle and returns at another is still in the surface.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Dimensional drift or lost flatness on datums, seals and bearing seats | Uneven stock removal across a large or asymmetric face, over-long cycles, or unprotected functional features exposed to the full charge energy. | Measure flatness and critical dimensions with a CMM or surface plate at the same marked points used for the incoming survey, and compare the change against the allowance. |
| Edge radius beyond the allowed limit | A cut stage longer or more energetic than the edge allowance supports, insufficient masking or fixturing, or a sequence repeated to remove a defect and run past the edge allowance. | Measure with a radius gauge, a cast impression or an optical comparator at the marked edges, and compare against the edge form and dimensions recorded before finishing. |
| Haze, a general loss of image clarity with no directional pattern | Worn media shedding an oversized fine fraction, agglomerated abrasive in the compound line, or fine grit carried into a late stage from screens, machine walls or a shared rinse. | View under raking light at low magnification against a master, then trace the pattern by machine and by rinse line to separate a charge problem from a rinse or transfer problem. |
| Embedded media particles or finishing pins in a soft surface | High contact pressure on aluminium, brass or copper, worn media with sharp fractured edges, or magnetic-finishing pins driven into a surface that cannot resist them. | Examine at magnification under raking light, wipe with a clean cloth and check for pulled particles, and consider a dye penetrant or etching check on a sample part. |
Groningen's industrial base is the Eemsdelta port and industry complex. Groningen Seaports manages the industrial areas of the Eemshaven and the port of Delfzijl, including the inland harbours Farmsumerhaven and Oosterhornhaven, the business parks Fivelpoort, Farmsumerpoort, De Delta, Weiwerd and MKB Park Eemshaven, and Groningen Railport in Veendam. The company concentrates on two clusters: energy and energy-related activity, circular industry and biobased chemistry; its stated 2030 vision is that the Eemshaven's energy and data sector is of international importance and that the chemical and recycling industry in Delfzijl is fully biobased. It runs the Chemport Innovation Center for scale-ups and participates in the Portlands Campus with maritime, energy and chemistry companies and knowledge institutions.
For this brief the relevant part of that base is machinery: The Chemport Innovation Center hosts scale-up companies testing production innovations, including Butter Bridge, which is building a pilot plant to test an electric melting furnace for recovering critical raw materials from industrial by-products and residual streams.
The Eemshaven and Delfzijl complex combines energy installations, offshore wind logistics, chemical and recycling plants and maritime services, so finishing demand is dominated by maintenance and fabrication work: pipe spools, valves, pump and turbine components, heat-exchanger parts and structural steel, where weld dressing, edge control and surface preparation before coating matter. Stainless and corrosion-resistant alloys are common because of the marine and chemical service environment.
A buyer here should settle the material and environment combination first — carbon steel for structures versus stainless or duplex for wet, saline or chemical service — and then decide whether the requirement is pre-coating surface preparation or in-service edge and burr control.
Freight context: Eemshaven (seaport and offshore wind logistics), Port of Delfzijl, Farmsumerhaven and Oosterhornhaven inland harbours, Groningen Railport in Veendam. Groningen Seaports operates both sea and inland harbours plus a rail terminal, and handled 116 offshore wind foundations in 2025, so the region has direct deep-sea and project-cargo capability for machinery. Rail freight to the region declined in 2025 after DB Cargo scaled back its Delfzijl service, which makes road transport the practical default for inland onward movement of machine tools.
Goods entering the Netherlands from outside the EU must be declared to Dutch Customs (Douane, part of the Belastingdienst); the importer needs an EORI number, import duty is calculated on the customs value (goods value plus transport and insurance to the EU external border), and import VAT is paid at the border unless an article 23 permit or a fiscal representative is used. CE marking is mandatory for most machinery placed on the EEA market: the Machinery Regulation replaced the Machinery Directive and manufacturers must comply with the new requirements by 20 January 2027. The importer must verify that the conformity assessment was carried out correctly, that CE marking is applied properly, that the technical file is present and complete, and that the user manual is supplied in the correct language; the manufacturer's EC Declaration of Conformity must be kept. Dutch companies imported over EUR 140 billion of machinery and appliances in 2024, 24% of total Dutch goods imports.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A mirror surface changes with the observer, so viewing conditions belong in the specification. Agree the light source type, the distance and angle, the viewing direction, and whether inspection happens in a booth or in the machine environment. A physical master approved by both parties, kept clean and stored protected, is more reliable than a photograph; photographs of reflective parts mostly record the light source. Define what is acceptable, such as a limited number of fine marks, a haze limit inside a stated area, and no visible peel, and state where the standard does not apply, for instance inside a recess that will be painted or covered. Re-confirm the master whenever the sequence or media family changes.
A trial reports what was observed on the parts it received, under the settings used. It cannot prove that every casting in a lot will respond the same way, that a worn media charge will behave identically over months, or that the finish satisfies a regulated or safety-critical requirement; those are questions for the buyer's own engineering and quality functions, using their own verification. It also cannot promise a reflectance value, an Ra value, a cycle time, a price or a capacity. Before shipping parts, decide whether a mirror finish is plausible at all: check the substrate for porosity and inclusions, confirm that available media can reach the geometry, and define the acceptance method first. If the requirement cannot be measured or viewed consistently, no trial result will settle it.

Send representative production parts including the thinnest wall, the tightest feature that must stay clear and the worst edge, plus a witness coupon of the same material and condition, a drawing extract covering the finished faces and the acceptance requirement you intend to apply. Label every piece and note its incoming condition with photographs, readings and measurements. The return is the tested parts with observations and a proposed media, compound and cycle direction for the buyer's own evaluation. A trial on parts shipped from Netherlands is a comparison, not a qualification, and it establishes no capacity or delivered surface value.
Design the charge around the smallest opening rather than the average part. Use media clearly smaller than the hole, or mask and plug the features before the cycle, count the media into and out of the load as a reconciliation, and add a retrieval step with a defined check such as a borescope or pin gauge. For Netherlands buyers sending parts for a trial, include the part with the tightest feature so the media class is chosen against real geometry. The small pins used in magnetic finishing embed easily in soft metal, so those features need extra inspection.
Rounding depends on the energy and duration of the sequence and on how exposed the edge is. A light refinement pass may barely touch it, while a long cut stage on a soft alloy can visibly round it. Mark the edges that must stay crisp, state a maximum radius or a no-touch zone before media is selected, and measure with a radius gauge, an optical comparator or a cast impression against the incoming form. Where a bright face and a crisp edge conflict, the practical order is to finish the face and then restore or protect the edge rather than to keep polishing.
Use Groningen, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers here would reference the CE machinery regime (Machinery Regulation from 20 January 2027) and the Dutch/EN-ISO surface-finishing standards published by NEN, such as NEN-EN-ISO 2080. Equipment destined for chemical, marine or offshore-wind service normally carries additional client specifications for material conformity, corrosion protection and coating preparation.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Groningen.
The buyer wants a clean bright face with no embedded abrasive or residue, because contamination would affect the electrical contact.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0679; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0679 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
