In Atlanta, United States, an automotive parts buyer has a duplex stainless clamp band whose rivet-hole burrs must be removed without rounding latch edges that have to engage. SurfacePolish is a cross-border supplier of finishing equipment, media and compounds and offers a free process sample trial in which the buyer's parts travel to Xiamen and return with observations and a proposed media, compound and cycle direction for the buyer's own verification. This brief is written for a buyer in Atlanta working on automotive parts; it describes equipment, media and a scoped sample review, not a local polishing service.
Which surfaces on this part carry a visible appearance grade, which are hidden, and which edges have a functional requirement rather than a cosmetic one?
Which dimensions, seal faces and thread forms carry functional geometry, and what limit on stock removal per cycle can those features tolerate?
At what batch size, load fill ratio and media wear state does a trial observation still describe what series production will produce?
Magnetic response is a sorting aid, not a material identification. Ferritic exhaust grades are strongly attracted, martensitic wear grades are magnetic, austenitic grades are effectively non-magnetic in the annealed state but become weakly magnetic after cold work, and duplex grades sit in between depending on composition and condition. A mixed load is therefore a real risk on two counts: a ferritic part can transfer free iron onto an austenitic neighbour during a shared cycle, and a magnetic retrieval or separation step can quietly fail on a grade that was assumed to be magnetic. Identify parts positively before finishing using material certificates, heat numbers and markings, and keep loads segregated by grade. Where a part is small or unmarked, settle the identification question before any consumable is chosen, because the answer changes both media chemistry and separation design.
Once media and machine are fixed, the variables a buyer can actually control are compound concentration, flow rate and water quality. Concentration influences cut rate, foam and residue; running lean to save money usually costs more in finish variation than it saves in consumable. Flow rate removes swarf and heat from the mass, and an under-flowed chamber loads up, smells, and starts depositing sludge on the parts. Water hardness, chloride content and suspended solids matter directly on stainless, because hard water leaves mineral films and chloride-bearing supply raises pitting risk on austenitic grades. Get a water analysis for the site, dose by measured concentration rather than by eye, and monitor pH and clarity at the machine. Record the actual water source used during a trial, because a good result obtained on one supply may not survive a change.

| Media | Best fit | Watch out for |
|---|---|---|
| Grinding and cutting media, fused alumina and silicon carbide based | Aggressive stock removal on heavy stainless burrs, weld dressing and rough cast surfaces before a refining stage. | Removes edge material quickly, can embed abrasive fragments in soft or gummy surfaces, and is usually too coarse for a final appearance stage. |
| Dry media, walnut shell and corn cob | Post-wet drying, light residue and scale removal, and dry polishing of surfaces that must not be re-wetted. | Does not cut stainless, generates dust, and leaves organic residue on parts if the medium is not kept clean and dry. |
| Alumina-based ceramic triangles and angle-cut forms | Heavy deburring, edge blending and machine-mark removal on stainless brackets, flanges and housings where corners and recesses must be reached. | Wears down in size and sharpness, so cutting rate falls without any setting change; broken pieces and fines can lodge in small features and must be screened out. |
| Porcelain and fine high-density ceramic media | Pre-polish refining stages on austenitic stainless appearance parts before a brightening stage, where a finer texture is the objective. | Limited cutting power on hard or work-hardened surfaces, and wear changes the charge gradually, so finish can drift between batches. |
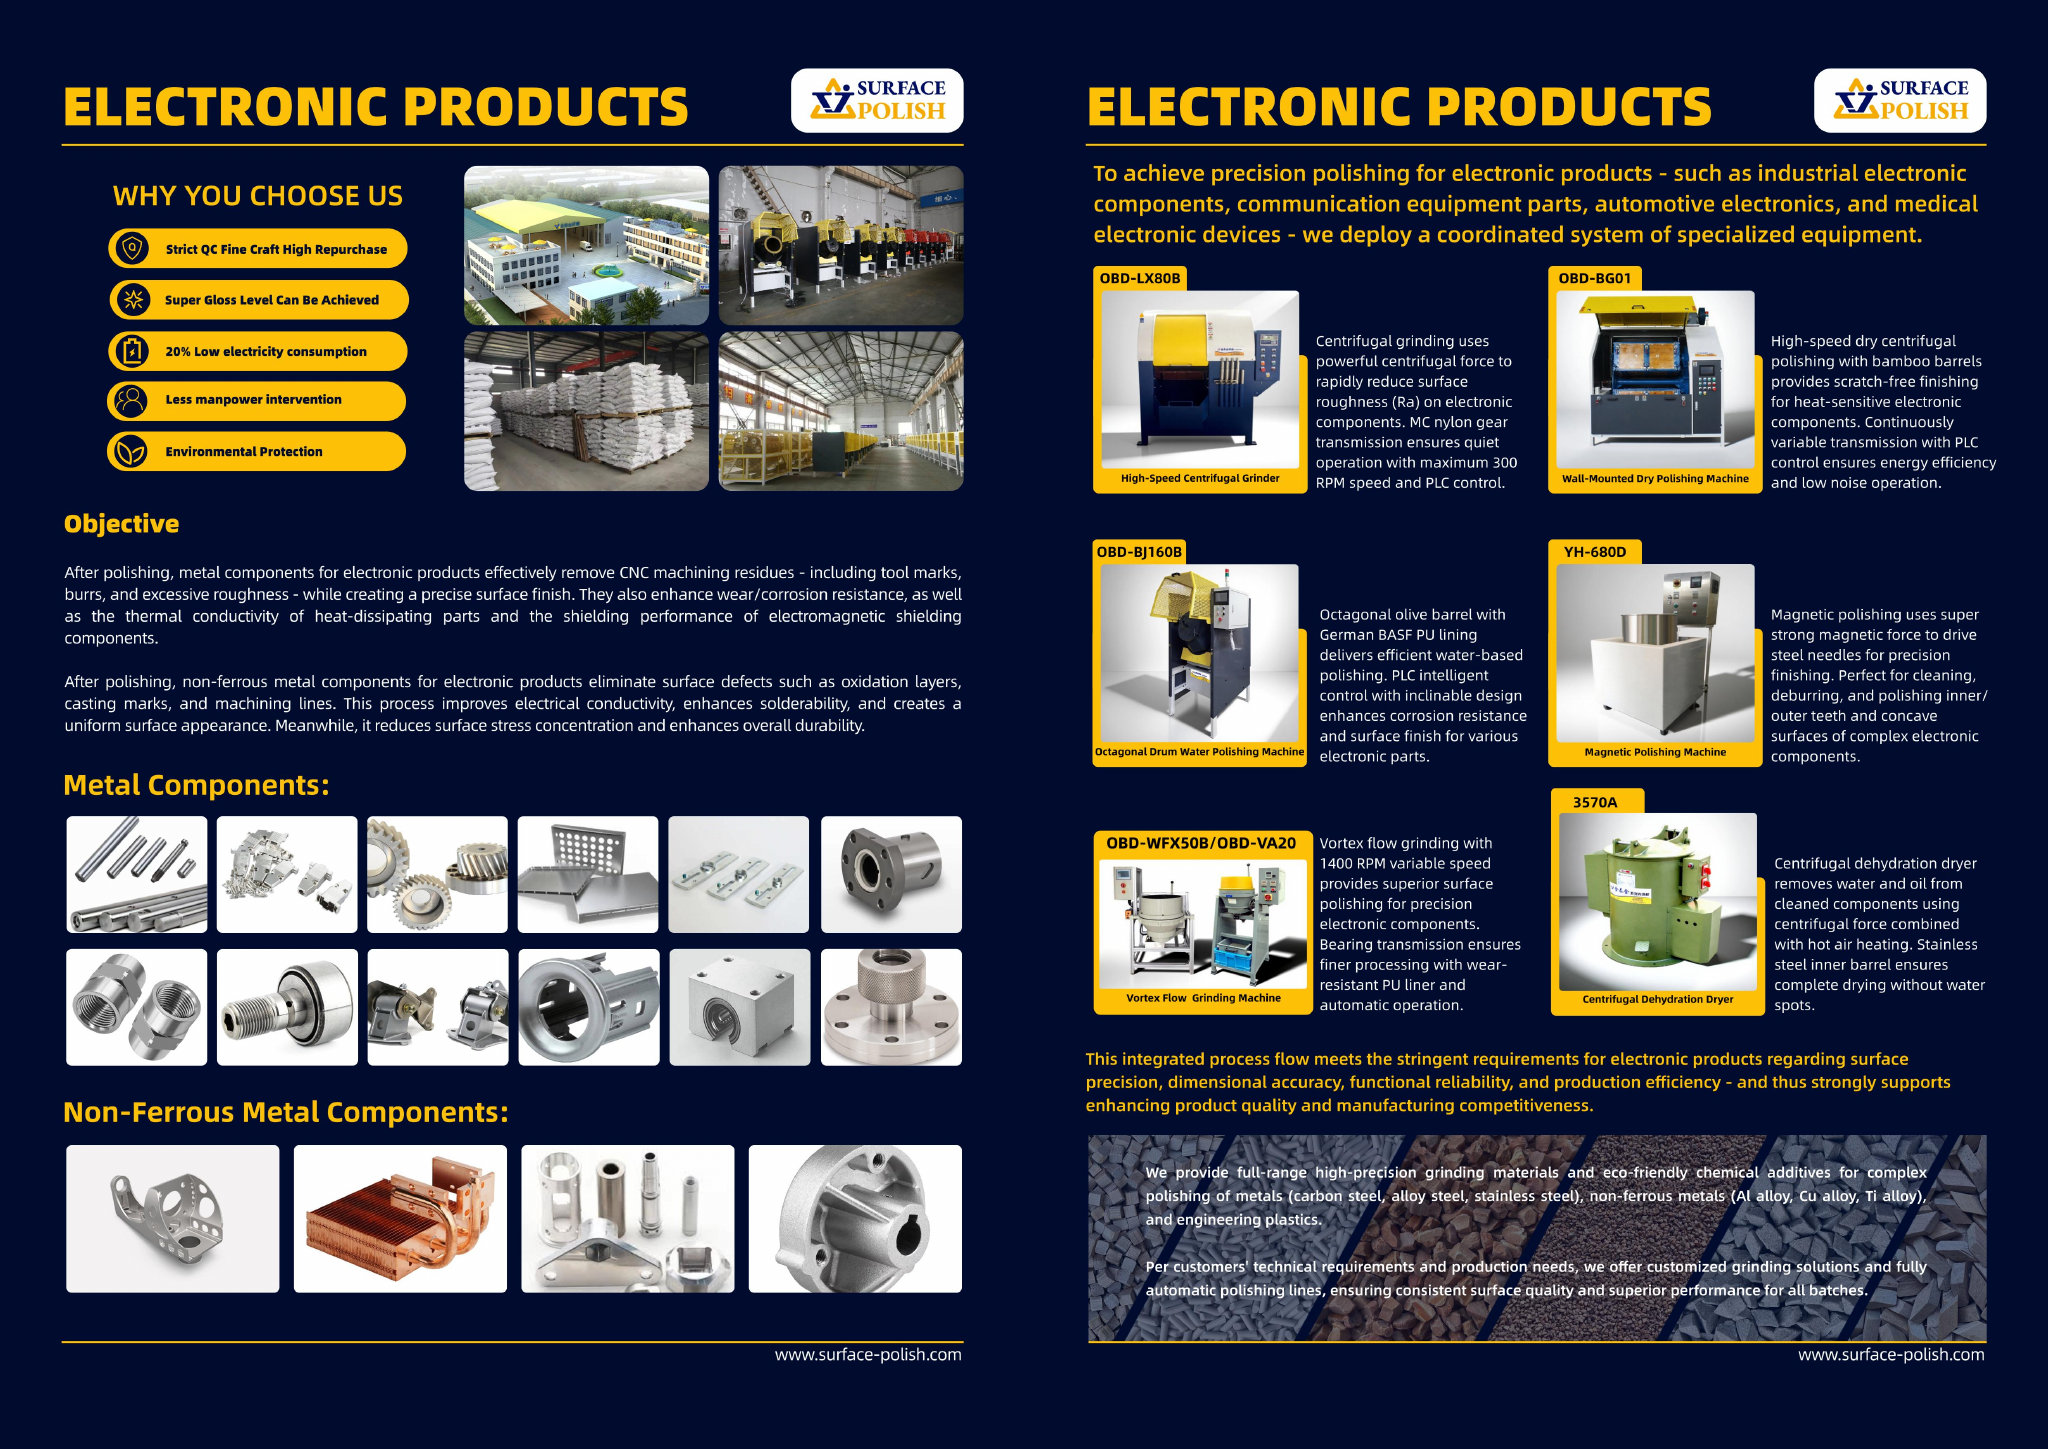
Three routes answer narrow needs. Barrel and rotary finishing is the gentlest common bulk method, well suited to delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins, at the cost of longer cycles and less uniform coverage on large parts. Magnetic finishing uses small steel pins driven by a rotating field to deburr and brighten intricate internal features, slots, gear teeth and blind holes without lodging media in narrow passages, but it suits small part envelopes, and parts made from magnetic grades need to be tested before the route is assumed to apply. Dry polishing with a heated dryer handles post-wet drying, light scale and residue control after a wet stage; dry media alone does not cut stainless, and moisture left in a blind hole or a folded hem becomes a stain during storage.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Barrel finishing machine, rotary barrel tumbler | Gentle deburring and finishing of delicate, thin or threaded stainless parts such as small fittings, sensor bodies and precision pins. | Cycles run longer than in higher-energy machines, and coverage can be uneven on large or complex parts. |
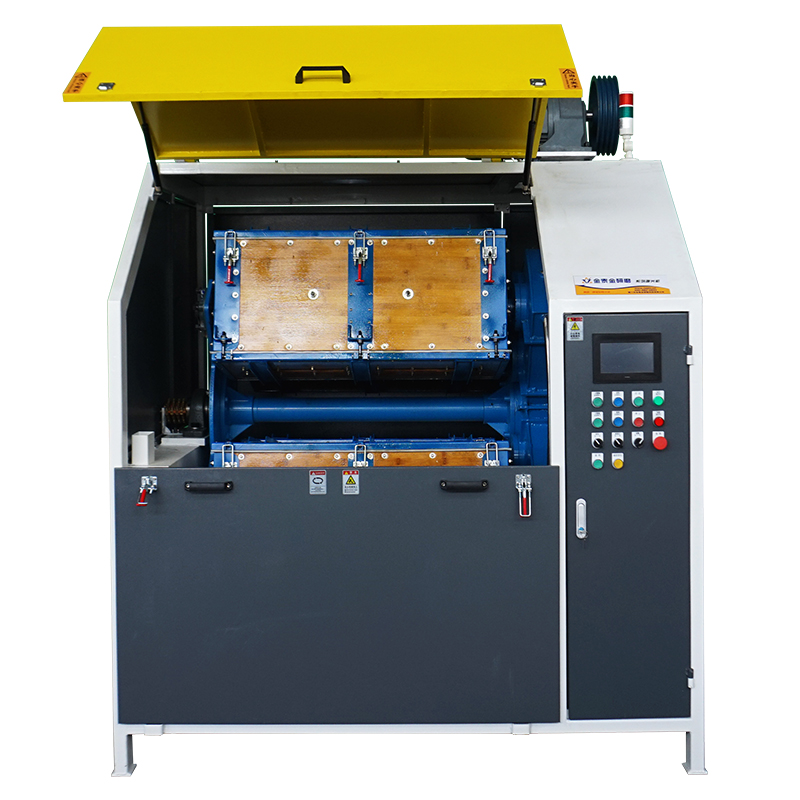
| Centrifugal barrel finishing machine | Very high energy deburring and edge radiusing of small, hard stainless parts in short cycles. | Rounds edges quickly and can exceed a tight radius within a short run; part size and shape are restricted and a substantial load is needed to justify the cycle. |
| Tub vibrator | Long stainless parts such as trim sections, exhaust profiles and shafts that cannot be loaded into a bowl without being cut down. | Media velocity varies along the length, so finish evenness must be verified at both ends, and the machine occupies more floor space and compound volume. |
| Dry polishing machine with heated dryer | Post-wet drying, residue control and light dry finishing of stainless parts that must leave the line dry and free of moisture in blind features. | Dry media does not cut stainless, and moisture trapped in a blind hole, hem or tight joint can cause staining if drying is not effective. |
Three further failure modes deserve their own place in a stainless finishing plan. Heat tint and oxide from welding or laser cutting often survive a light finishing cycle and then read as a defect once the surrounding surface is brightened, so the incoming oxide condition has to be recorded and its removal put in scope. Discolouration can also appear after drying, when dissolved minerals and compound residue concentrate in a film; the remedy is rinse quality, water quality and prompt drying rather than more cycle time. For high-strength martensitic grades, acid-bearing chemistry plus mechanical work raises a hydrogen concern that is not visible on the surface, so the material and process requirements need to be defined and verified by the buyer, and the finishing route checked against them. Dimensional drift is cumulative and quiet: thin walls, bores and seal faces can move within a batch while every visual check passes, so critical dimensions need before-and-after measurement at a fixed sample size.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Hazing or waviness on a part specified as mirror or bright | An intermediate refining stage skipped or cut short, media too coarse for the final texture, or a media charge that has worn out of its working size range. | View under defined lighting against a physical master at the acceptable and marginal limits, measure roughness across the lay with a fixed instrument setup, and screen the media charge for size and condition. |
| Dimensional drift, including bores opening slightly and thin walls thinning | Sustained media contact removing material from every accessible surface, with cycle time or media size class beyond what the feature tolerances can absorb. | Measure critical dimensions with micrometers, bore gages or a CMM before and after on a fixed sample size, and track a maximum stock removal per cycle for each feature at risk. |
| Impingement marks, nicks or gouges on thin stainless panels and webs | Part-on-part contact in an under-filled chamber, excessive amplitude, or free parts striking each other where no compartment or fixture controls them. | Inspect the suspect feature under magnification and raking light before and after processing, and compare its location across several parts from the same load to confirm the defect is random rather than systematic. |
| Embedded particles or grey smut on the finished surface | Media fines, broken ceramic fragments or metallic debris from the charge becoming trapped or smeared into the surface during the finishing cycle. | Examine under magnification with raking light and on a wipe test, check the compound bath and media charge for fines and broken pieces, and screen a media sample to identify the source. |
Atlanta's industrial base combines transportation and logistics head offices with aerospace, defence and specialty metal fabrication, plus food and beverage production and a large academic medical centre. The Federal Reserve's Sixth District Beige Book, which covers Georgia, reports manufacturing activity growing at a moderate pace, with a fabricator of specialty metal products seeing particularly strong demand for aerospace and defence-related goods and a military shipbuilder expecting a decade of defence-driven demand. Hartsfield/Jackson Atlanta International tops the FAA's final CY2025 enplanement table, and CBP lists Atlanta, Georgia (port 1704) as a port of entry with its field office in the city. The Coca-Cola Company's own history page records the drink's first serving in downtown Atlanta in 1886, Norfolk Southern's corporate address is 650 W. Peachtree Street NW in Atlanta, and Emory University, based in the city, presents health and medical research as central to its mission.
The nearest part of that base to this brief is machinery: The same Beige Book reports manufacturing growing at a moderate pace in the Sixth District, with advanced manufacturers reporting consistent volumes and sustained pricing power.
Aerospace, defence and general machinery fabrication in the Atlanta region produces machined and formed metal parts whose burrs and edge condition affect fatigue life, coating adhesion and assembly fit, so edge blending and surface preparation before priming, anodising or plating are routine process steps. Fabricated sheet-metal and tube assemblies typically need weld dressing and edge radiusing, while food and beverage equipment adds a hygiene requirement: stainless product-contact parts are usually finished to a cleanable, pit-free surface with controlled roughness rather than to a decorative polish.
The first decision is whether the part is governed by an aerospace or defence special-process requirement (for example NADCAP-approved passivation, anodising or painting) or by a general industrial finish, because that sets the acceptable media, compound chemistry and documentation package. Confirming the inspection method for edge radius, Ra and burr limits before any media trial avoids qualifying a finish against the wrong criterion.
Freight context: Hartsfield/Jackson Atlanta International Airport (ATL), Atlanta, Georgia (CBP port of entry 1704 with the Atlanta field office), Norfolk Southern rail network, corporate headquarters at 650 W. Peachtree Street NW, Atlanta. FAA final CY2025 enplanement data rank Hartsfield/Jackson Atlanta International first in the country with 51,459,786 boardings, and CBP's Georgia table lists Atlanta, Georgia (1704) with the field office in the city; Norfolk Southern's published corporate address is 650 W. Peachtree Street NW, Atlanta, Georgia 30308. Metro Atlanta has no seaport, so containerised machines from China normally land at a US East or Gulf coast port and reach Atlanta by rail or truck, with air consignments and sample parts clearing at the Atlanta port of entry.
The United States has no single mandatory national finishing standard. The national standards system is voluntary and consensus-based, coordinated at national level by the American National Standards Institute (ANSI): ANSI published the United States Standards Strategy (USSS) 2025 on 6 January 2026, a strategy that 'guides how the U.S. develops standards and participates in international standardization', while the National Institute of Standards and Technology (NIST) is the federal measurement and standards agency and states that 'Technical standards keep us safe, enable technology to advance, and help businesses succeed.' In practice a buyer specifies surface finish, deburring, cleaning and coating requirements on the drawing or in the purchase order using the voluntary consensus standards maintained by bodies such as ASME and ASTM International and their ISO equivalents, and the acceptance criterion is the buyer's own specification rather than a government-issued finishing standard. Where a part is destined for a regulated product - pressure equipment, food-contact equipment, aerospace or medical devices - the relevant industry code or the customer's qualification requirement governs instead.
The United States has no free-trade agreement with China, so Chinese industrial machinery enters under normal-trade-relations (MFN) duty rates in the Harmonized Tariff Schedule of the United States plus any Section 301 duty that applies to the specific HTSUS subheading. USTR's four-year-review modification of the Section 301 China technology-transfer investigation imposed additional Section 301 duties or increased existing rates on certain Chinese products in strategic sectors, and created a temporary exclusion process for machinery used in domestic manufacturing: chapters 84 and 85 of the HTSUS, which cover most machinery used in manufacturing processes, are the chapters that were made eligible for exclusion requests. CBP still administers Section 301 China duties, the four-year-review increases and product exclusions. The IEEPA-based additional ad valorem duties of 2025 - including the reciprocal-tariff actions and the China synthetic-opioid supply-chain duties imposed under Executive Orders 14195 and 14257 - were ordered terminated by Executive Order 14389 of 20 February 2026 and, as soon as practicable, are no longer collected. A buyer should therefore price the MFN rate plus any applicable Section 301 rate and check whether the machine's exact subheading is covered by a current exclusion, rather than assuming either the 2025 IEEPA tariffs or a blanket China rate still applies.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Roughness values on stainless automotive parts are only comparable when the setup is fixed. Pin down instrument, cutoff, evaluation length, filter and stylus tip, because each shifts the number; state the measurement direction relative to the dominant lay, and note that measuring across the lay is usually what reveals a directional brushed texture while measuring along it flatters the result. Very bright finishes fall below the practical limit of common stylus instruments, so add a gloss or haze reading or a defined visual comparison to make the grade repeatable. Mark the measurement locations on a drawing, keep the same locations, and record the reading as one number among several rather than as a description of the whole part. Note where a measurement is truly not meaningful, and use a functional or appearance check there instead.
A trial is more useful as a structured comparison than as a single demonstration. Decide in advance what is being compared, such as two media shapes in the same size class, two compound families on one media charge, or two cycle lengths at one energy setting, and hold everything else constant. Keep a control part that receives no finishing at all, so that post-process differences can be attributed to the process rather than to handling. Name the features that must not change and the level of change that would be unacceptable, so that a result can be judged on the spot. Write down the questions the trial must answer before parts are shipped, and rank them, because the ranking is what tells the supplier which comparison matters most when cycle time is limited.

They are different processes with different effects, and SurfacePolish does not supply or perform electropolishing. Mechanical finishing works by media contact, so it blends, deburrs and brightens the surfaces the media can reach, and it rounds edges as it works. Electrochemical treatment removes material ionically and reaches into recesses that media cannot. Where an electropolished surface is specified for corrosion or cleanliness reasons, treat electrochemical processing as a comparison point and ask whether the specified requirement can be met by another route, then verify that on your own parts and against your own acceptance rule.
Steel media generally produces the brightest result on austenitic stainless, but brightness depends on the whole progression rather than one medium. A common sequence is a hard ceramic stage that removes burrs and machine marks, a finer stage that refines the texture, then a low-amplitude stage that brightens. Media that is too soft for the work-hardened surface burnishes and dulls instead of cutting. The shape and size class also matter, because small media reaches tight features but leaves a different texture from larger forms. Treat any proposed progression as a comparison to test on real parts with your own measurement setup.
Hydrogen uptake is a documented concern for high-strength martensitic stainless steels when acid chemistry and mechanical work are combined, and it is not visible on the surface. The practical route is to state the material and hardness in the enquiry, ask which compound families are proposed and at what concentration, and confirm with your own engineering function whether any post-finishing treatment is required and within what window. SurfacePolish can describe the compound family and the process conditions used on a trial, but fitness for a given strength level, and any treatment specification that follows, must be defined and verified by the buyer.
Use Atlanta, United States as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers in this supply chain commonly reference AS9100 and NADCAP-approved special processes for aerospace work, with SAE AMS process specifications such as AMS 2700 for passivation named on the certificate, while general industrial and food-equipment parts are specified to ASME B46.1 or ISO 4287 for texture with the customer's chosen salt-spray, adhesion or cleanliness test for coatings and hygiene.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Atlanta.
The buyer needs rivet-hole burrs removed and the visible face refreshed while keeping the latch edges sharp enough to engage.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0072; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0072 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
