A gripper and tooling maker in Bristol, United Kingdom working in robotics and automation has a recurring batch of small machined jaws where the edge break has to be consistent without losing the pivot hole or the serrated face. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial, returning a representative batch with observations and a proposed media, compound and cycle direction for the buyer to compare. This brief is written for a buyer in Bristol working on robotics and automation; it describes equipment, media and a scoped sample review, not a local polishing service.
What does the finishing step actually have to deliver before the next operation, whether that is assembly, anodising, painting or a functional test, and who defines that requirement?
Which surfaces on the part are functional, such as bearing bores, dowel holes, seal lands, ground mounting faces and threads, and which are only cosmetic?
What is the smallest hole, slot, keyway or cross-drilling the charge must not enter or plug, and how will a lodged medium be detected and removed?
Two housings made to the same drawing can need different routes because of alloy and temper. A 6061-T6 machined body is soft enough to smear and peen under a heavy ceramic charge, and it marks where a steel charge has transferred iron. A 7075 part is stronger and cuts differently. Austenitic stainless work-hardens at the surface and responds to media pressure rather than to sharp cutting. Hardened 4140 or a nitrided seat may tolerate only a light edge break, because the finishing step cannot be allowed to remove the case. Castings can open porosity that machining had closed. Record the temper, the hardness range and the heat treatment, and establish whether an anodise, passivation or paint step follows, because that step usually sets the residue and smut limits the finishing cycle has to respect.
Inside any machine, the way parts are carried decides whether the finish is even and the geometry survives. Parts left loose together nibble each other along contact lines and produce bright impact marks on visible faces. Cradles that follow a casting, compartments, dividers and clip-on carriers present the same face to the media on every part and protect machined lands. Load ratio matters as much: too many parts in the charge reduces circulation and leaves shielded pockets unworked, while too few allows parts to be thrown against the chamber wall. Build the arrangement around the most delicate and the heaviest part in the family rather than an average one. Where a buyer plans automated loading or transfer between operations, the fixture interface, the orientation and the pick points belong to the buyer's own engineering scope and are defined and verified on that side.
| Machine route | Where it fits | What it will not do |
|---|---|---|
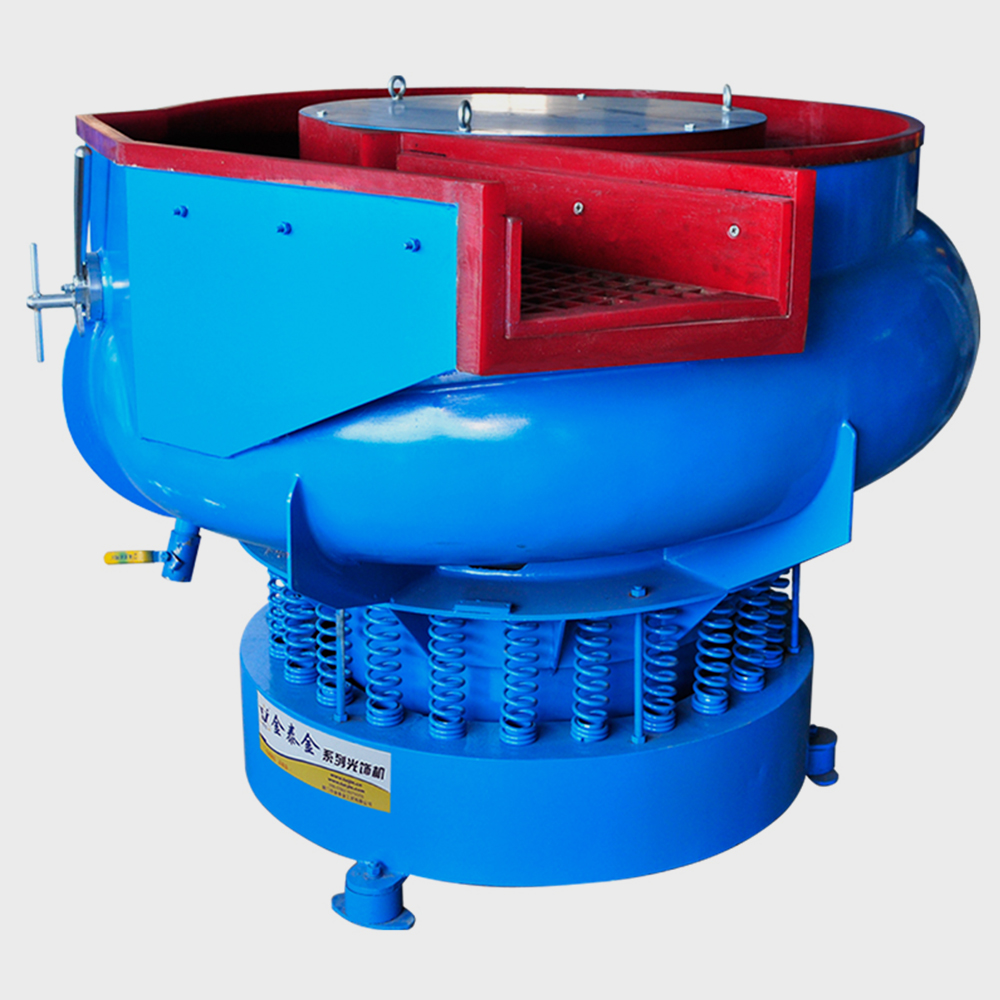
| Vibratory finishing machine, bowl type | General deburring and refinement of machined housings, plates and brackets that fit and can tumble without racking, with easy mid-cycle inspection | Continuous part-on-part contact and no access to deep internal passages; thin plates and finished mounting faces need separation |
| Disc finishing machine | Fast, high-energy edge breaking and surface refinement on small robust parts and uniform batches of gripper jaws, blocks and fittings | High impingement and edge-loss risk on thin, soft or aluminium parts, and the geometry must suit the disc working gap |
| Barrel finishing machine, rotary barrel tumbling | Gentle deburring of small fragile parts and mixed batches of screw-machine components with a generous compound flow | Long cycles, no visibility while running, and internal features can collect media and compound that must be retrieved at unload |
| Grinding finishing machine | Taking off a heavy machining burr, dross or a defined stock layer before a refinement pass on robust steel and stainless work | High removal energy cuts functional edges fast and demands a tighter assessment of what may be removed and how much |
Media has to be small enough to enter the pocket or passage that must be finished and large enough not to lodge in a tapped hole, a cross-drilling, a keyway or a seal groove. Those two conditions conflict on almost every automation part, and the usual resolution is to plug or mask the openings rather than to compromise the charge. Measure the narrowest opening a medium could enter, and the depth behind it, and compare that against the smallest medium in the proposed charge. Threads are the classic retention point: a medium that enters a tapped hole is difficult to see and easy to leave behind. Where a passage genuinely needs work, plan a defined retrieval and check step rather than assuming parts come out clear. Media wear shrinks the charge over its life, so a size class that is safe when new can become a lodging risk later.

| Media | Best fit | Watch out for |
|---|---|---|
| Plastic triangles, cones and pyramids in a soft to medium grade | Deburring aluminium housings, gripper plates and other soft alloy parts where surface marking and edge rounding must be kept to a minimum | Slow cut rate, media deforms and wears, and a worn charge behaves noticeably differently from a fresh one |
| Fine ceramic or porcelain shapes in a small size class | Edge blending and surface refinement after a cutting stage, and reaching tighter external geometry on machined housings and brackets | Small sizes enter and retain in tapped holes and fine slots, and media wear shrinks the charge so the finish drifts over its life |
| Dry media such as walnut shell and corn cob | Drying assistance and light surface polish after a wet cycle, particularly on parts with pockets and threads that must not stay wet | Does not deburr or refine metal significantly, generates dust, and must not be treated as a cleanliness step |
| Plastic cylinders and cones in a harder, denser grade | Longer cycles on mixed batches of small fittings and screw-machine parts where a repeatable light edge break is wanted without ceramic impact | Can float or segregate by shape in a bowl, and cylindrical forms can wedge in slots, keyways and cross-drillings |
Parts can pass a finish check and still fail because something moved. Thin machined webs, long beams and unsupported walls relax or distort under tumbling loads, so a housing that measured flat before the cycle fails a flatness or position check afterwards, and a soft aluminium part can pick up a bow that only shows on a surface plate. At the same time, media that cannot reach deep pockets, internal corners or the shielded side of a flange leave the original machining marks intact while the exposed faces are fully refined, and the difference becomes obvious once the part is assembled against a mating surface. Both outcomes are caught by measurement rather than by looking harder at the finish: record flatness, wall thickness and critical dimensions at the same points before and after, inspect at defined locations, and treat the batch record as the first place to look for the cause.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Colour change or darkening on an aluminium face after the cycle | Compound chemistry unsuitable for aluminium, no effective corrosion inhibitor, or a delay between finishing and drying | Compare the finished face with an unprocessed coupon of the same alloy under the agreed light, and review the compound product, dose and rinse sequence for the lot |
| A ceramic, plastic or steel medium lodged in a tapped hole, keyway, cross-drilling or seal groove | Media size class too close to the opening, a charge that has worn or fractured into smaller pieces, or a retention feature that was never mapped | Count the charge in and out where practical, pin or thread gauge every hole, borescope the smallest passages at an agreed angle, and rinse through a filter for a visual check |
| Rust spotting on stainless parts appearing hours or days after finishing | Ferrous transfer from steel media, a machine or tooling that has held carbon steel, or insufficient corrosion inhibition and drying | Inspect after a defined dwell time rather than immediately, look for pinpoint spots on and near edges, and trace the media and machine history for the lot |
| Bearing bore, bore lip or dowel hole edge rounded past the drawing limit | High-energy route, over-long cycle, dense or coarse media, or a functional edge run without masking or a shielding fixture | Measure the defined edge feature before and after with an optical comparator, radius gauge or moulded replica, and compare it with the maximum radius on the drawing |
Bristol is the largest city in the West of England Mayoral Combined Authority area, which the authority states it invests for alongside Bath and North East Somerset and South Gloucestershire. Invest Bristol & Bath, the region's inward investment service, lists aerospace and advanced engineering, composites, clean tech and energy, life sciences, logistics and distribution, and space among its key sectors. ADS South West, the regional branch of the ADS trade association, took over the former West of England Aerospace Forum's operations from 1 April 2026 and keeps small bases in both Bristol and Yeovil, which it calls two hubs of manufacturing excellence. Make UK records the South West as one of the strongest-performing English regions.
The nearest part of that base to this brief is machinery: Invest Bristol & Bath lists aerospace and advanced engineering, and composites, among the region's key sectors - the machining, forming and composites base that produces parts needing edge and surface control.
Bristol's aerospace and composites cluster means machined and formed parts are accepted against a defined surface and edge condition, and composites add a second requirement because trimmed edges and prepared bonding surfaces must be conditioned without damaging the laminate. The West of England Combined Authority publishes a growth strategy for the region and operates a Growth Hub and the Invest Bristol & Bath service, which are the documented regional entry points for business and investment support.
A Bristol buyer should establish whether the acceptance criterion is an edge condition on a machined metal part or a surface-preparation standard on a composite, because the two call for different media, different process control and different inspection evidence.
Freight context: West of England road and rail freight corridor serving Bristol (Invest Bristol & Bath lists logistics and distribution as a key sector). Invest Bristol & Bath maintains a dedicated connectivity page for the region and lists logistics and distribution among its key sectors. The Bristol Port Company site and Bristol Airport site both returned bot-protection responses during this research, so no port- or airport-authority tonnage or cargo figure is quoted here.
China does not appear in the alphabetical list of trade agreements in effect published by the Department for Business and Trade, so Chinese-origin machinery imported into the UK cannot claim a preferential agreement rate. Duty is instead determined by the commodity code declared on the import declaration, and the UK's customs authority is HM Revenue and Customs (HMRC), which ONS also names as the largest single data source behind UK trade-in-goods statistics. Because a GB-prefixed EORI number is a precondition for importing into England, Scotland or Wales, a Chinese seller's UK buyer must already hold that registration before any machine ships.
English is the working language of contracts, drawings and conformity paperwork, so quotations, technical files and Declarations of Conformity should be supplied in English. UK manufacturers have now recovered above 2019 output levels in every English region and devolved nation except Northern Ireland, and the sector is concentrated in food and drink and transport equipment, with the North West the largest manufacturing region by total output. Buyers typically expect the UKCA/CE route, a Declaration of Conformity and a UK-established economic operator to be identified before order, and they need commercial invoices, customs declarations and the C79 retained in a form their finance team can use for import VAT recovery. No source verified in this research establishes a mandated payment instrument, so payment structure should be treated as commercial negotiation rather than a regulatory requirement.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A first-article part, finished under the intended production settings, is the reference every later batch is compared against. Keep it identified and protected with the measurement record and the settings that produced it. Production acceptance then rests on a sampling plan: the sample size, the frequency, which features are measured and which are only inspected visually. For a low-volume build, sampling by part may be workable; for a batch of small parts, sampling by position in the charge is more useful, because parts at different points in a bowl see different media conditions. Record where each sampled part sat. Agree the disposition rule in advance, including whether rework is allowed and how a reworked part is identified, so a failed sample leads to a defined action rather than an improvised one.
Change one variable at a time. If the question is media shape, hold the machine, load, compound, cycle time and part mix constant and change only the medium. If the question is cycle time, hold the charge and settings constant and stop at two or three defined intervals. Use adjacent coupons or parts from the same production lot so the only difference is the variable under test. Label the pieces before they run and have the returned parts judged in one session under the same light, rather than one at a time as they arrive. Where several people judge appearance, ask each to rank the parts before discussion so the strongest opinion does not set the answer. Running two changes at once produces a result that cannot be attributed to either.
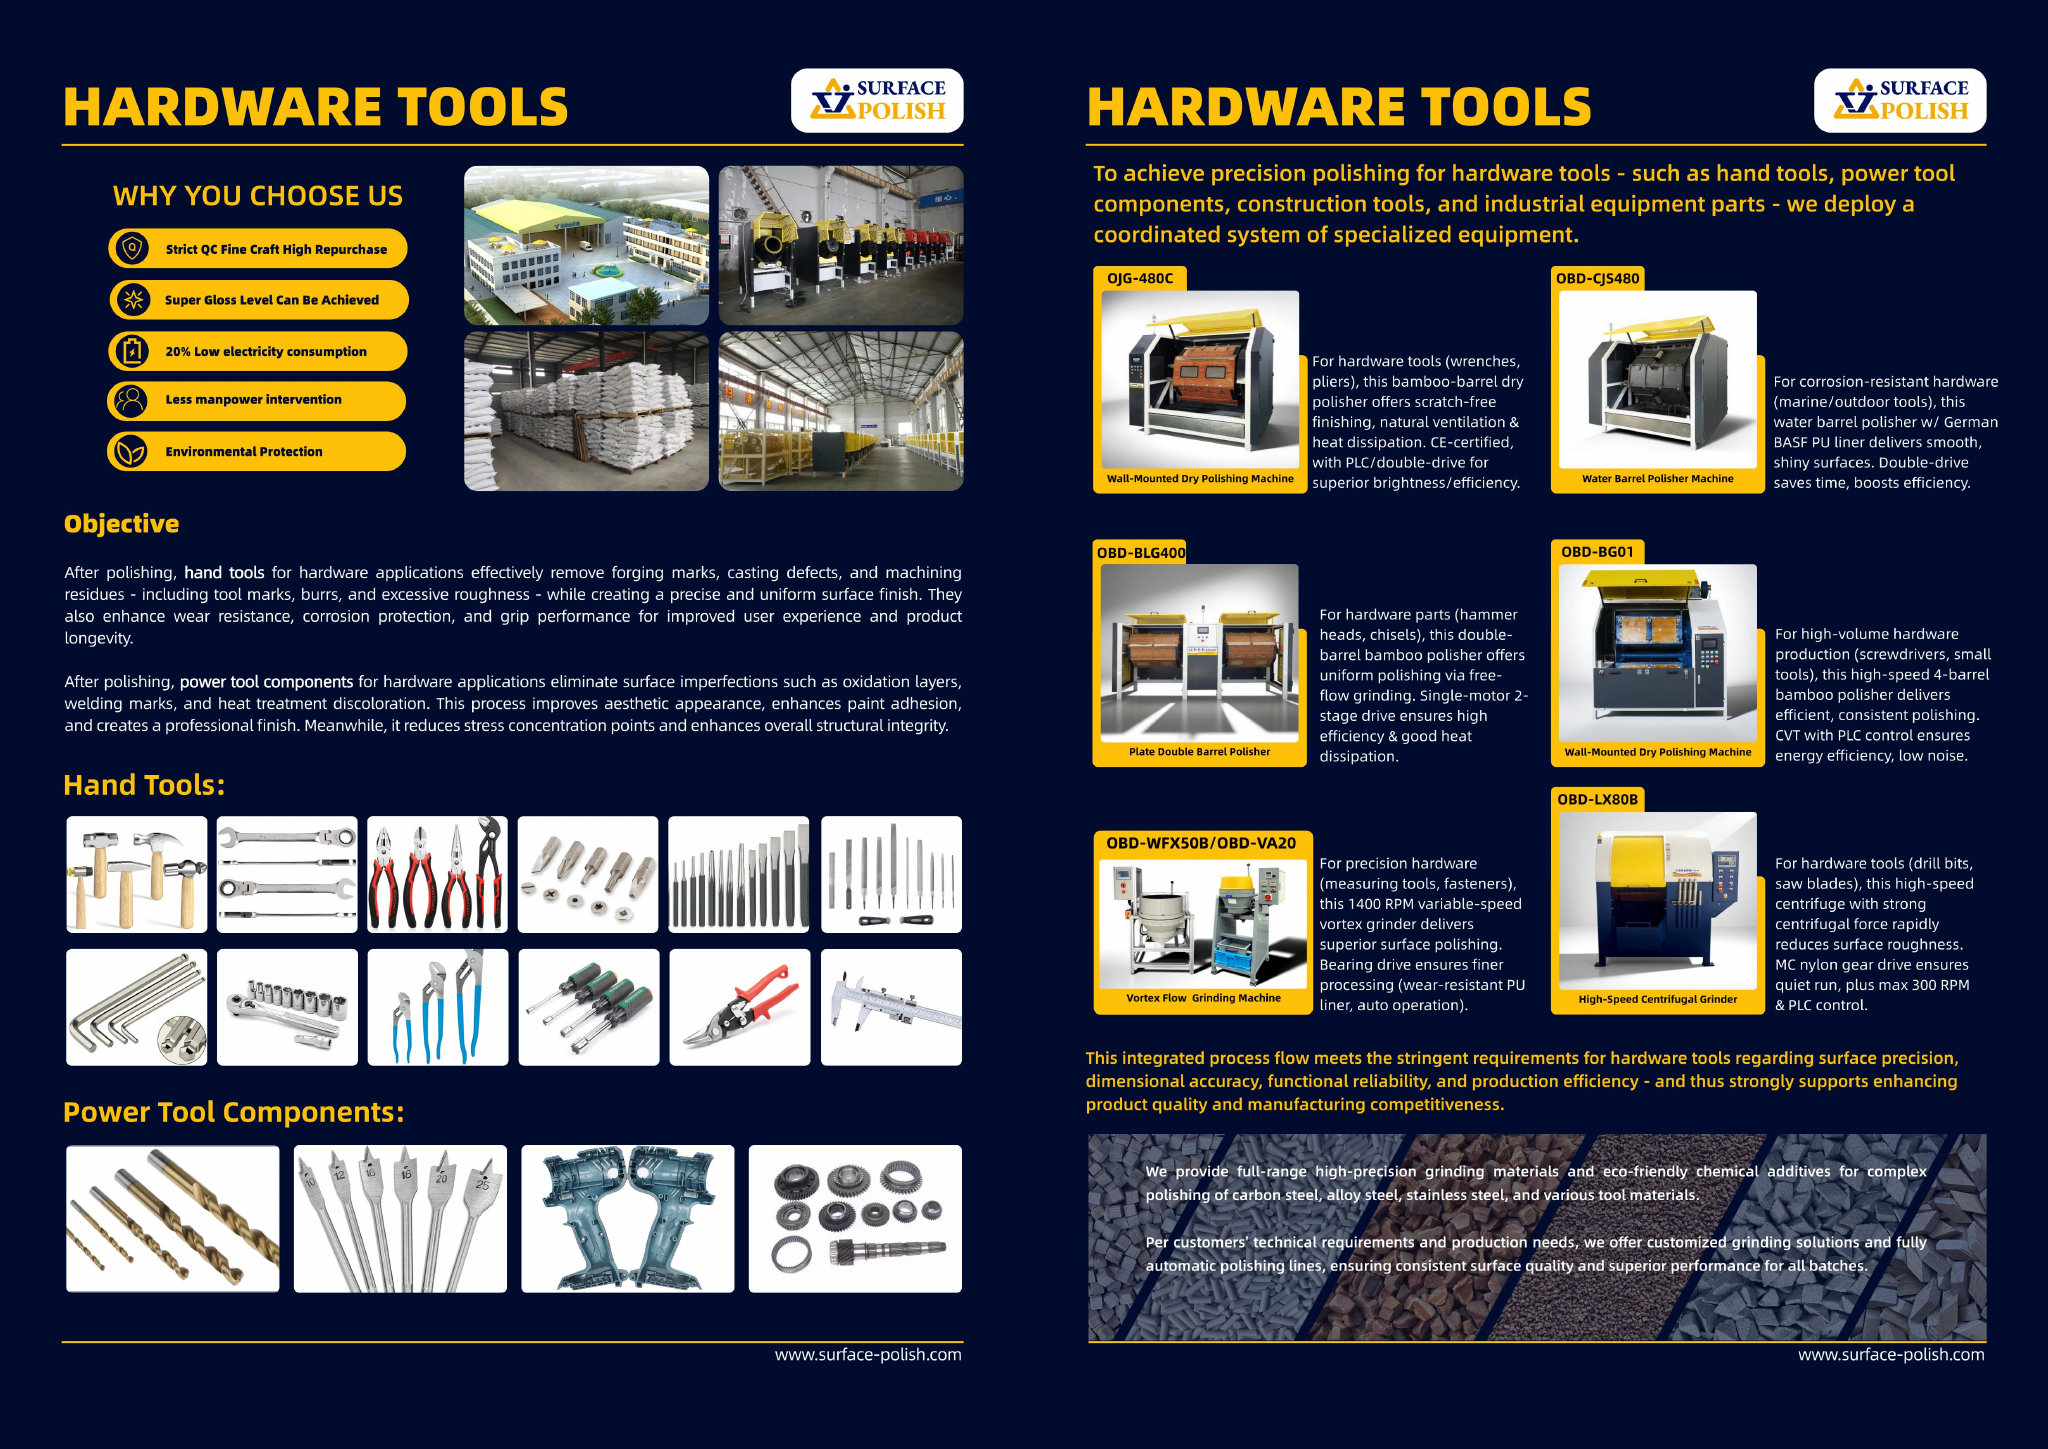

Change one variable at a time. Hold the machine, load, compound, cycle time and part mix constant and change only the medium. Use parts from the same production lot so the only difference is the variable under test. Label the pieces before they run and have the returned parts judged in one session, under the same light and at the same marked measurement points, rather than one at a time. Where several people judge appearance, ask each to rank the pieces before discussion. Where a cut stage is followed by a refinement stage, score the stages separately, because a good final result can hide an unremoved burr or an over-coarse first stage.
A bore cannot be protected by the cycle alone; it is protected by what is decided before the cycle. Masking or plugging the bore, keeping the part out of contact with heavy neighbours, choosing a lighter route and shortening the cycle all reduce the load the bore sees, but none of them guarantees a dimension. That is why the bore must be measured before and after at the same points, with a bore gauge or CMM, and compared with the drawing limit. SurfacePolish does not promise a tolerance or a result; the trial reports what was observed on the parts tested, and the dimensional acceptance decision stays with your own metrology and quality functions.
No. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to the factory in Xiamen. We do not design, integrate, program or commission robotic cells or automated handling lines, and no robotic polishing cell is offered here. What can be discussed is the part itself, the features that must be protected and the finishing step, and which loose-part machine and media route is worth testing. How parts are presented, loaded, unloaded and transferred is engineering scope you define and verify, and any machine or medium suggestion remains a starting point for your evaluation in Bristol.
Use Bristol, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
UKCA or CE marking with a Declaration of Conformity applies to machinery placed on the Great Britain market, HSE's work equipment and machinery topic and COSHH cover operation and hazardous substances, and aerospace work in the region is additionally governed by prime contractors' quality and assurance requirements, which ADS South West represents through its South West Council.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Bristol.
The buyer needs a consistent light edge break across the batch without rounding the pivot hole or blunting the serrations.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0280; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0280 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
