A balustrade maker in Chicago, United States sends architectural metalwork work in the form of 40 x 40 x 1.5 mm stainless posts, 1.1 m long and welded to base plates, and needs those welds blended into the brushed grain without a flat spot on the corner. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to Xiamen. This brief is written for a buyer in Chicago working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
How much of the incoming mill seam, joint weld or transit scratch must be removed, and what minimum wall thickness has to remain after that removal?
Will the finish be judged by a roughness number, by a physical reference panel, or by both, and who views the parts before they are accepted?
What texture direction is required, and how will that direction be preserved and compared across lengths that are finished in different lots?
An elevation is normally assembled from lengths made and finished at different times, so the lot definition matters as much as the finish itself. Decide how parts are grouped into finishing lots: by profile, by wall thickness, by alloy heat, by incoming mill finish, or by the date the material arrived. Then decide how lot identity is preserved through finishing, fabrication and despatch, because a length that cannot be traced back to a lot cannot be compared with another length in a dispute. Where an order will be produced over several weeks, keep an unprocessed reference length from the first delivery in store, and keep a finished reference panel from the first accepted lot. Both are needed before anyone can argue about whether a later length matches.
A balustrade or handrail job is never only long runs. It also contains cut-to-length spindles, elbows, brackets, base plates, ball finials and short connector sleeves, often in the same alloy and finish. Those parts are a poor fit for a longitudinal arrangement and a good fit for batch equipment, where a large number of small identical parts can be processed together with controlled part-on-part contact. Treating the two populations as one route is a common planning error: the runs are under-processed because the settings were chosen for the fittings, or the fittings are over-worked and lose their edges. Screen the order into long runs and small fittings, then specify the media class separately for each, even where the final appearance has to read the same.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Tub vibrator | Long and large parts such as architectural tube and profiles, where the process length has to extend along the part. | Bed depth and fixture design decide whether thin sections survive, and fluid flow has to be checked at the far end of the chamber. |
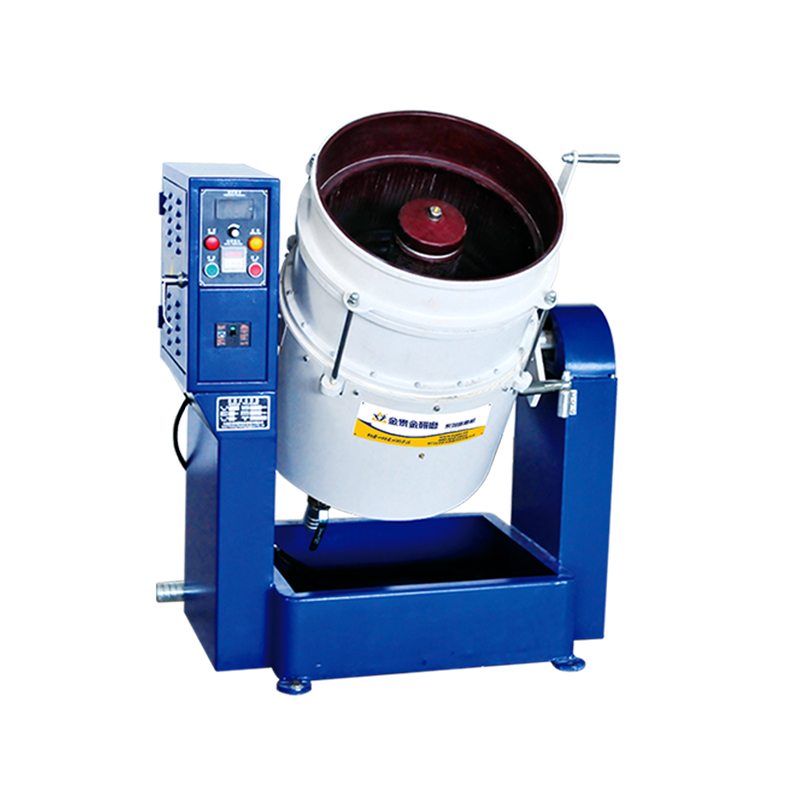
| Barrel finishing machine, rotary barrel tumbling | Gentle, precise batch processing of small parts, finials, sleeves and short connector pieces. | Part length and part-on-part contact restrict it to short fittings rather than long architectural runs. |
| Vibratory finishing machine, bowl type | General edge blending and surface refinement on brackets, base plates, cut spindles and other small fittings. | Chamber diameter caps the part length, and a long tube cannot be worked evenly in the circular bed. |
| Centrifugal barrel finishing machine | High-speed finishing of small precise parts, including where a bright appearance is required on a compact geometry. | Chamber geometry and high contact forces rule it out for long, thin-wall or easily marked sections. |
Ceramic media cuts harder, holds its shape longer and is the usual choice when a previous scratch or a weld seam has to be removed from stainless. Plastic media is gentler, lighter and less likely to mark a thin or soft section, at the cost of a slower cut and a shorter texture. Steel media produces a bright appearance and strongly linear marks, but it is heavy, it needs well-controlled compound to keep it clean and separated, and it raises a question about whether any iron-bearing debris is acceptable in the buyer's own cleanliness or contamination control. That last point is a requirement for the buyer to define and verify, and it is not something a supplier can decide on their behalf.

| Media | Best fit | Watch out for |
|---|---|---|
| Plastic media, cones and triangles | Gentle work on thin-wall sections and softer alloys, and where marking or distortion is the main risk to be managed. | Slower cut and shorter media life, with limited effect on a deep scratch or a heavy seam. |
| Plastic media, cylindrical | Light surface refinement on thin rectangular sections where holding the shape matters more than cutting power. | Little cut power, and the size class changes quickly as the media wears, which shifts the texture pitch over a run. |
| Steel media, pins and balls | Bright, strongly linear appearance on stainless where a higher-lustre finish is wanted on accessible faces. | Heavy, needs tight compound control to stay clean and separated, and any iron-bearing debris is a contamination question the buyer has to define and verify. |
| Ceramic media, cylinders and other elongated shapes | Linear, directional refinement of the visible faces of round and rectangular profiles after the seam has been cut back. | Flat sides and ends mark differently, and the length-to-diameter ratio limits how far the media reaches into a shallow cove. |
A surface can measure inside a roughness band and still fail visually. Orange peel, a mottled texture with a pitch of a few millimetres, appears when the surface is over-worked with a coarse medium or worked with too much pressure on a soft or thin section. Hazing is the diffuse, milky appearance that follows a fine but non-uniform cut. Both are geometry effects rather than amplitude effects, so a profilometer reading across them may be entirely acceptable while a reflection test shows a broken image. This is why an architectural finish cannot be accepted on a roughness number alone, and why a visual standard viewed under defined light at a defined distance has to sit beside the numeric one. Ra and appearance answer different questions.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Flat spot or thinning at a dressed weld | Too much material removed in one place while chasing the weld toe, usually with too coarse a medium or too much pressure. | Measure wall thickness with an ultrasonic gauge across the dressed area, and lay a straightedge over the joint to reveal a flat. |
| Longitudinal scratch running along the part axis | Incoming coil or straightener marks, media or swarf dragged along the surface during the cycle, or a finished length sliding over a bare support between operations. | View the surface under raking light at a low angle along the axis, compare the same station on several parts, and compare against the retained reference panel. |
| Loss of ovality or out-of-round section | A load applied across the wall during the cycle or while the part sits in a rack. | Measure the diameter across two axes at several stations along the length with a caliper or micrometer. |
| Hazy or milky patch with a dull reflection | Uneven cut, worn media in part of the chamber, or weak compound flow at the far end of a long tub. | Compare the near end and the far end of the same length, and check compound concentration and fluid flow at both ends of the chamber. |
Chicago plans its industrial base through a designated corridor and Planned Manufacturing District (PMD) system rather than a single industrial estate: the Pilsen Industrial Corridor is one of Chicago's 26 designated industrial corridors, covers 1,070 acres and contains PMD 11, and it is home to food distributors, manufacturers and industrial operators as well as segments of the South Branch of the Chicago River and the Sanitary and Ship Canal. World Business Chicago, the city's economic-development organisation, describes Chicago as having one of the largest manufacturing industries in the nation, with 400,000+ manufacturing and logistics workers across the metro area and $100B+ in annual manufacturing output, and names Manufacturing, Food Manufacturing, Transportation/Distribution/Logistics and Life Sciences among the region's priority sectors. The same source describes the local base as spanning advanced robotics, clean energy systems, aerospace, food production and precision engineering, with mHUB and UI Labs named as manufacturing innovation centres. The Seventh Federal Reserve District, which includes Chicago, is characterised by the Chicago Fed as featuring significant agricultural production, automotive and other manufacturing, and financial and insurance industries.
The nearest part of that base to this brief is food: The Pilsen Industrial Corridor is home to food distributors, manufacturers and industrial operators, and World Business Chicago lists Food Manufacturing as one of the region's priority sectors.
The corridor mix puts two different finishing problems side by side: food-processing and packaging equipment, where stainless wetted surfaces are judged on weld dressing, passivation and cleanability, and general machinery, automation and metalworking parts, where edge radius, burr height and Ra are checked before assembly. Because the work is spread across 26 industrial corridors and is largely batch and job-shop in nature, media and compound selection usually has to cover mixed stainless, aluminium and carbon-steel parts rather than a single alloy family.
The first question to settle is whether the parts are food/life-science stainless requiring validated cleanability and passivation, or structural and machinery parts requiring only edge radius and burr-height control, because that answer fixes media type, compound chemistry and cycle time far more than machine size does.
Freight context: Illinois International Port District (Iroquois Landing and Lake Calumet terminals), O'Hare International Airport, Class I rail terminals serving BNSF, CN, CP, CSX, NS and UP. The Illinois International Port District operates its own rail infrastructure connecting to six of the seven North American Class I railroads - BNSF, CN, CP, CSX, NS and UP - and its Iroquois Landing facility takes international ship traffic through the St. Lawrence Seaway; the District states it moves more general cargo than any other Great Lakes port, at over 19 million tons waterborne a year. CBP maintains a Chicago customs presence for imported and exported shipping, so machinery and sample parts would be entered and marked for country of origin at the port of entry.
The United States has no free-trade agreement with China, so Chinese industrial machinery enters under normal-trade-relations (MFN) duty rates in the Harmonized Tariff Schedule of the United States plus any Section 301 duty that applies to the specific HTSUS subheading. USTR's four-year-review modification of the Section 301 China technology-transfer investigation imposed additional Section 301 duties or increased existing rates on certain Chinese products in strategic sectors, and created a temporary exclusion process for machinery used in domestic manufacturing: chapters 84 and 85 of the HTSUS, which cover most machinery used in manufacturing processes, are the chapters that were made eligible for exclusion requests. CBP still administers Section 301 China duties, the four-year-review increases and product exclusions. The IEEPA-based additional ad valorem duties of 2025 - including the reciprocal-tariff actions and the China synthetic-opioid supply-chain duties imposed under Executive Orders 14195 and 14257 - were ordered terminated by Executive Order 14389 of 20 February 2026 and, as soon as practicable, are no longer collected. A buyer should therefore price the MFN rate plus any applicable Section 301 rate and check whether the machine's exact subheading is covered by a current exclusion, rather than assuming either the 2025 IEEPA tariffs or a blanket China rate still applies.
The customs authority is U.S. Customs and Border Protection (CBP), part of the Department of Homeland Security. The importer of record files an entry and then an entry summary (CBP Form 7501): '"Entry Summary" refers to the documentation necessary to enable U.S. Customs and Border Protection to assess duties, collect statistics, and determine whether other requirements of law have been met.' Classification is made in the Harmonized Tariff Schedule of the United States, and an importer may request a written CBP ruling on the correct HTSUS classification and rate of duty, which is the practical way to confirm the treatment of a finishing machine before shipment. Every article of foreign origin must be marked with the English name of its country of origin 'in a conspicuous place as legibly, indelibly, and permanently as the nature of the article (or container) will permit' under 19 U.S.C. 1304 and 19 CFR 134.11. The $800 de minimis (Section 321) exemption is no longer available for ordinary freight: CBP suspended it indefinitely for all modes other than the international postal network effective 24 June 2026, so even low-value sample parts and media must go through formal or informal entry and pay applicable duty. General US industry practice is that there is no single machinery conformity mark comparable to the EU's CE marking; buyers instead verify electrical components and control panels, machine guarding against workplace-safety requirements, and any customer-specific qualification.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Grain direction is the most common reason a set of individually acceptable lengths is rejected as an assembly. Where two lengths butt at a joint, their texture direction has to run the same way, and the pitch and brightness have to be close enough that the joint does not read as a line. That is a planning decision made before the lengths are run, not a sorting decision made afterwards: define the grain direction on the drawing, mark the direction on every length, and keep the orientation through fabrication and despatch. Then inspect the lengths laid end to end as they will be installed, under the agreed light, rather than one at a time on a bench. A direction reversal that is obvious in an assembly can be invisible in a single part.
The trial result is only meaningful against a documented starting point. Photograph each sample under fixed lighting with a scale in frame, note the direction of the incoming texture, and take roughness readings at marked stations with the traverse direction recorded. Note the incoming straightness with the sample on a reference surface, the edge condition at cut ends, and any existing weld, scratch or discolouration. Keep one piece unprocessed as the baseline. When the trial parts come back, the comparison is between the returned parts and these records, not against memory. This is also how a buyer distinguishes a change made by the process from a feature that was present in the material when it arrived.
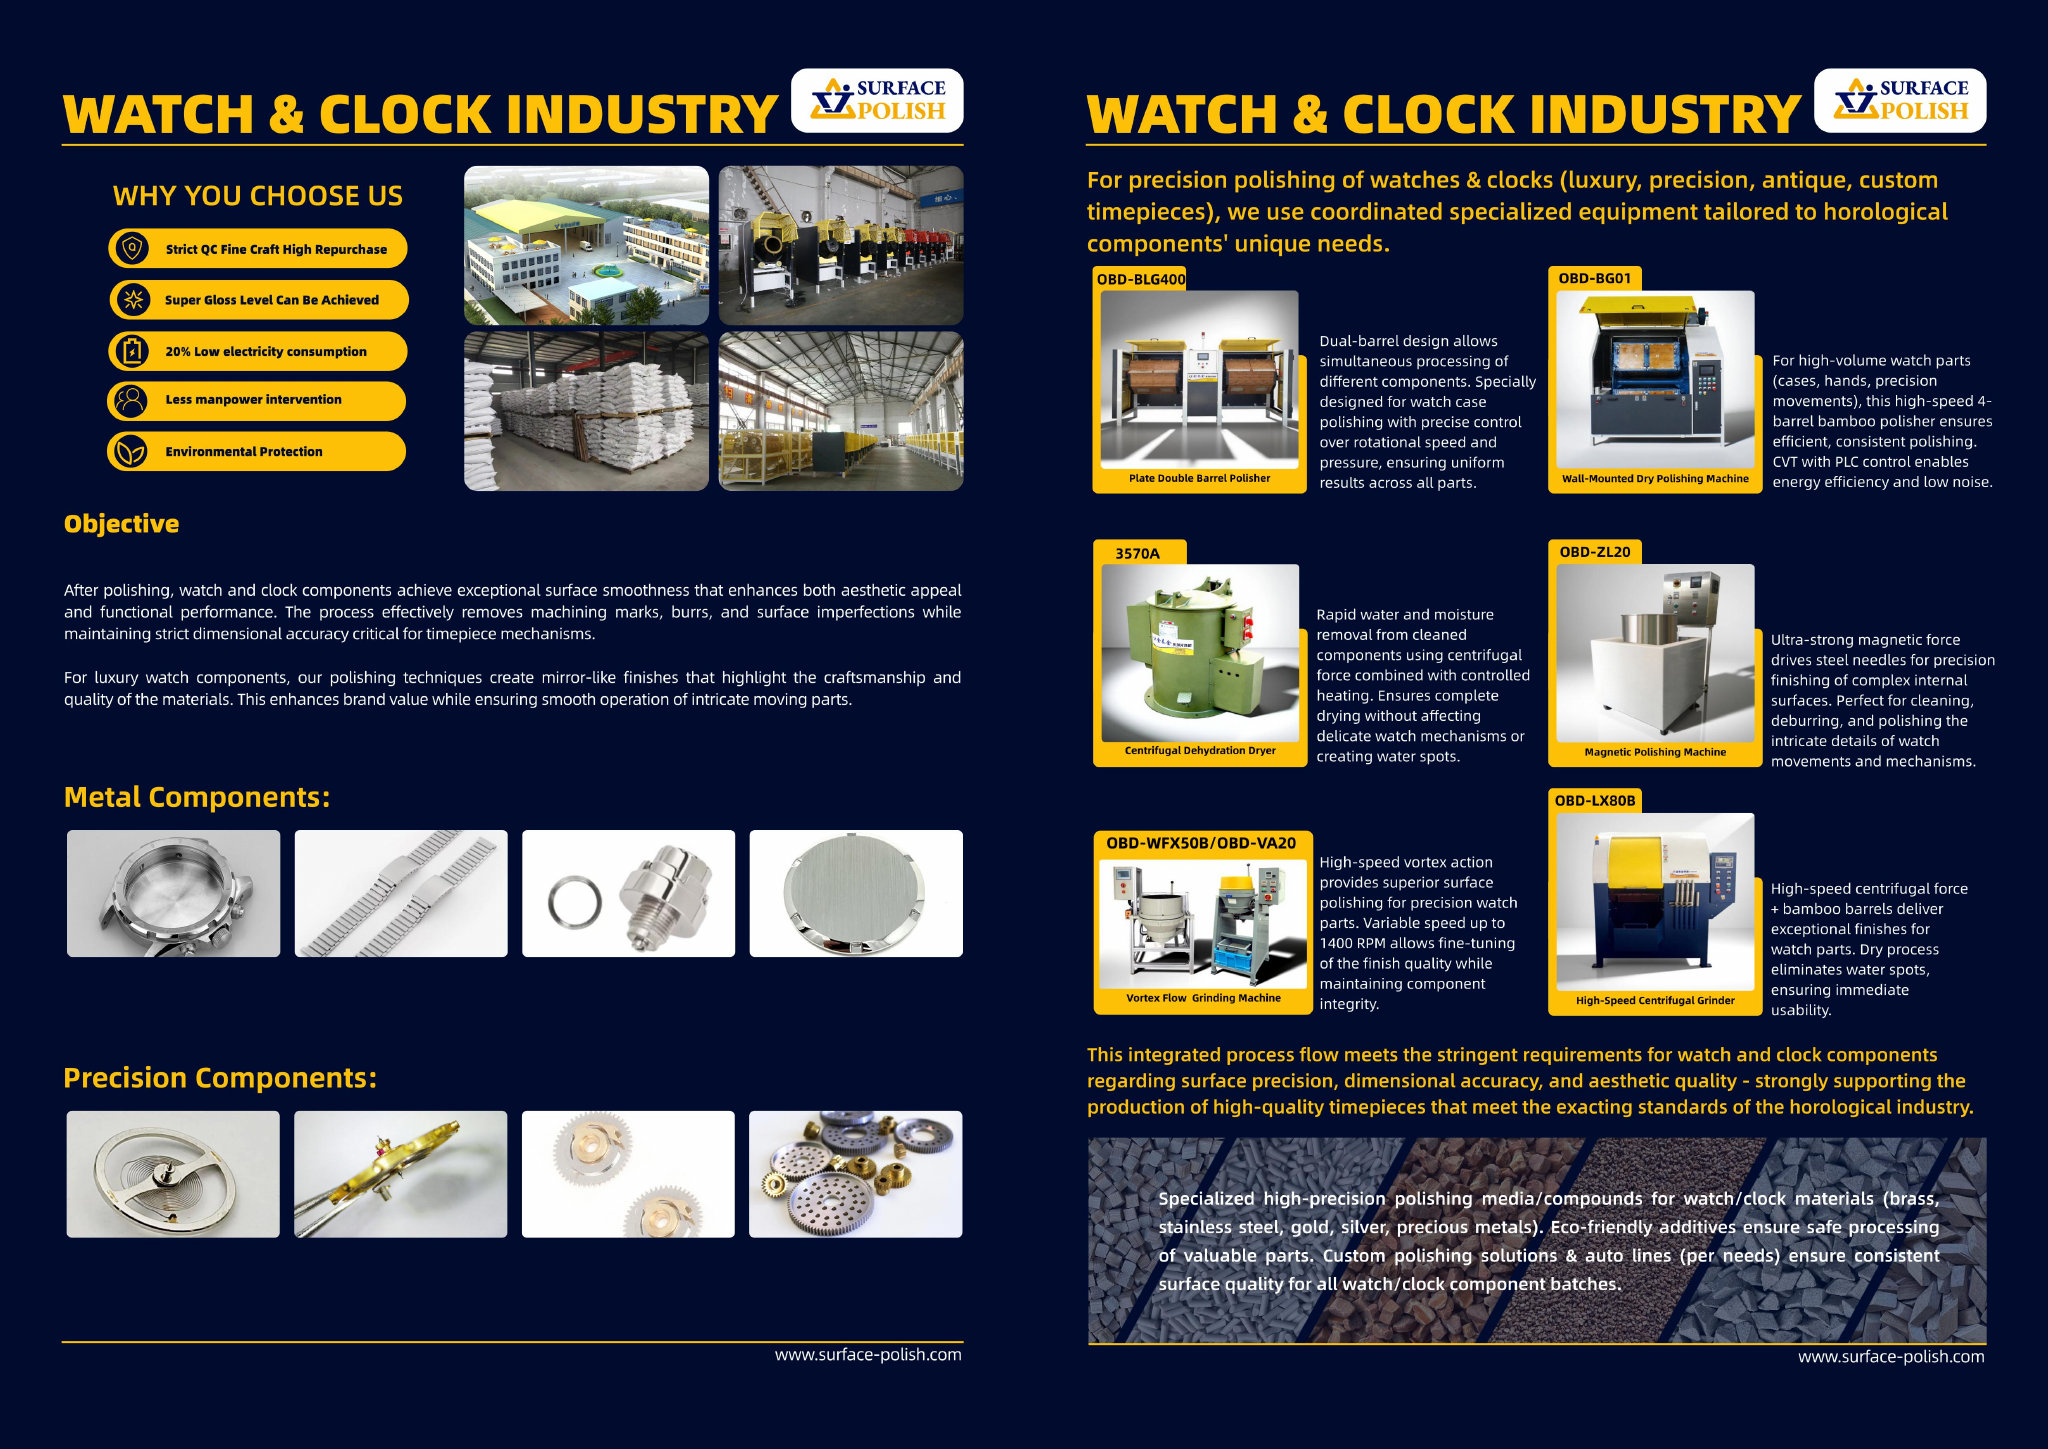

No. SurfacePolish is a cross-border supplier of finishing machines, media and compounds, and runs a free sample trial on parts the buyer sends. The tube, pipe and profiles remain the buyer's own material from their own mill or stockholder, and we do not verify its grade, mill certificate or corrosion performance. Keeping those roles separate matters, because the appearance a finishing line can reach is limited by the incoming material: its alloy, its hardness, its existing grain and the condition it arrives in. Send material from the actual delivery rather than a hand-picked offcut.
Length is a handling question before it is a finishing question. Long architectural sections are run in a tub or on a dedicated longitudinal arrangement rather than a round bowl, and the practical limit depends on the chamber length, the supports available and how the length is packed for shipping. For a trial, send cut sections from the production material and one full-length piece where bend or end effects could matter, so the arrangement is chosen against the real part rather than an average. Parts travel to our factory in Xiamen, and we do not process anything in United States or Chicago.
Support the profile rather than letting it lie loose. Cradles shaped to the section, dividers or compartments that keep lengths apart, end plugs that hold the open section, and controlled orientation in the bed all reduce the load a flat face sees. Rectangular sections are more exposed than round ones because a flat face has no hoop stiffness across its width, so the thinnest wall in the order should set the fixture design. Send the thinnest and widest section you use, not an average one, so the trial is run against the part most likely to distort.
Use Chicago, United States as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
A Chicago buyer works inside the US voluntary-consensus system coordinated by ANSI rather than against a single national finishing standard, with surface-texture, cleaning and coating requirements normally written into the drawing or purchase order. Food, life-science and medical customers add their own hygiene, material-conformity and cleanability requirements, and any machine installed in a US plant must also satisfy the applicable OSHA machine-guarding and electrical requirements.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Chicago.
The circumferential weld at the base and the mill seam have to be blended without leaving a flat spot on the corner or a colour change.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0007; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0007 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
