A steelwork fabricator in Geelong, Australia supplying architectural metalwork holds 4 m lengths of 88.9 mm stainless pipe at 5 mm wall with a heavy mill seam and a transit scratch, and needs the metal cut back without thinning the wall past the buyer's own limit. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to Xiamen. This brief is written for a buyer in Geelong working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
Which wall thickness and section shape in the order is most likely to distort, and what fixture, cradle or support will protect it?
What texture direction is required, and how will that direction be preserved and compared across lengths that are finished in different lots?
Will the finish be judged by a roughness number, by a physical reference panel, or by both, and who views the parts before they are accepted?
Once a length runs past roughly a metre and a half, handling stops being a detail and becomes the deciding constraint. A six-metre handrail cannot be turned in a chamber, cannot be stacked with its finished face against another part, and cannot be lifted by two people without risk of a bow. The screening questions are: what is the longest length in the order, how is it moved to and from finishing, is it cut to final size before or after finishing, and what supports it at every stage. Answering these sets the machine class, the cradle design and the inspection points. A buyer who fixes the finish specification first and the handling plan later usually discovers the finish cannot be held on the long lengths that matter most.
A balustrade or handrail job is never only long runs. It also contains cut-to-length spindles, elbows, brackets, base plates, ball finials and short connector sleeves, often in the same alloy and finish. Those parts are a poor fit for a longitudinal arrangement and a good fit for batch equipment, where a large number of small identical parts can be processed together with controlled part-on-part contact. Treating the two populations as one route is a common planning error: the runs are under-processed because the settings were chosen for the fittings, or the fittings are over-worked and lose their edges. Screen the order into long runs and small fittings, then specify the media class separately for each, even where the final appearance has to read the same.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Tub vibrator | Long and large parts such as architectural tube and profiles, where the process length has to extend along the part. | Bed depth and fixture design decide whether thin sections survive, and fluid flow has to be checked at the far end of the chamber. |
| Disc finishing machine | Fast, high-energy cycles for small to medium fittings and hardware where a short cycle is the priority. | The high energy that makes it fast will distort, mark or bend thin and long parts. |
| Barrel finishing machine, rotary barrel tumbling | Gentle, precise batch processing of small parts, finials, sleeves and short connector pieces. | Part length and part-on-part contact restrict it to short fittings rather than long architectural runs. |
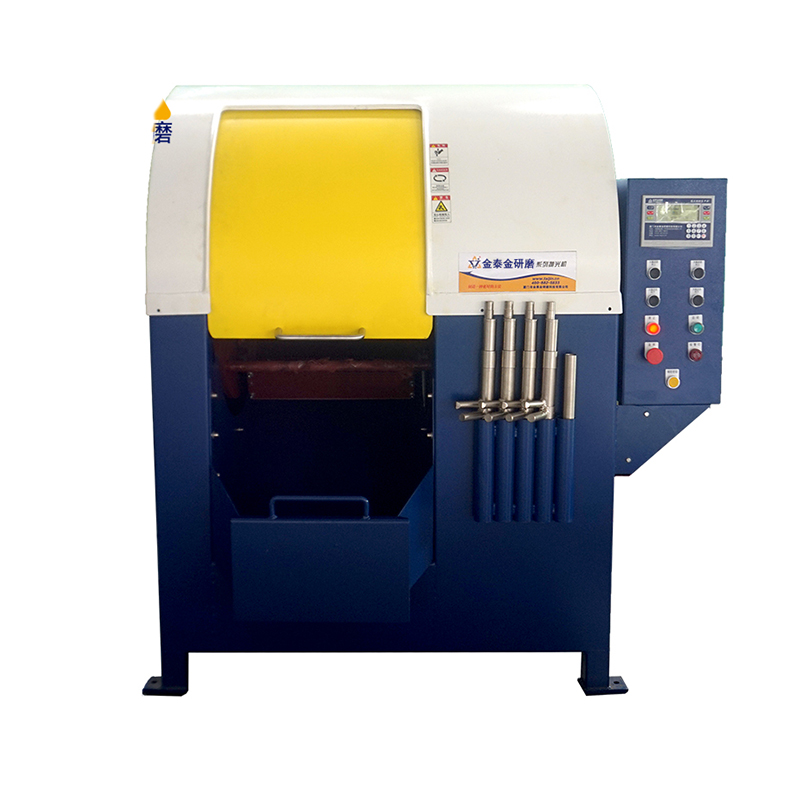
| Grinding finishing machine | Higher material removal where a mill seam, a joint weld or a deep scratch has to be cut back before surface refinement. | Removal is aggressive, so depth control and wall thickness limits have to be set before the cycle is run. |
Ceramic media cuts harder, holds its shape longer and is the usual choice when a previous scratch or a weld seam has to be removed from stainless. Plastic media is gentler, lighter and less likely to mark a thin or soft section, at the cost of a slower cut and a shorter texture. Steel media produces a bright appearance and strongly linear marks, but it is heavy, it needs well-controlled compound to keep it clean and separated, and it raises a question about whether any iron-bearing debris is acceptable in the buyer's own cleanliness or contamination control. That last point is a requirement for the buyer to define and verify, and it is not something a supplier can decide on their behalf.

| Media | Best fit | Watch out for |
|---|---|---|
| Ceramic media, spheres and balls | General deburring and edge work on cut ends, brackets and small fittings in the same order as the long runs. | Produces overlapping crater-like marks that work against a linear brushed appearance and can peen a thin wall. |
| Plastic media, cones and triangles | Gentle work on thin-wall sections and softer alloys, and where marking or distortion is the main risk to be managed. | Slower cut and shorter media life, with limited effect on a deep scratch or a heavy seam. |
| Ceramic media, angle-cut triangles | Heavier cutting and seam removal on stainless tube and profiles, where a directional linear texture on the visible face is wanted. | Wears down and changes effective size class, generates sludge, and can over-round thin sections or chip on sharp edges. |
| Ceramic media, cylinders and other elongated shapes | Linear, directional refinement of the visible faces of round and rectangular profiles after the seam has been cut back. | Flat sides and ends mark differently, and the length-to-diameter ratio limits how far the media reaches into a shallow cove. |
Open tube ends, slotted channels and drilled fixings all collect media, swarf and compound. The failure is rarely visible at the end of the cycle; it shows up after the part is installed, when compound weeps from a bore onto a visible face or when a trapped particle works loose during handling and scratches an adjacent length. Treat removal as a designed step rather than a rinse: plug or cap what should never see media, count media in and out of each batch, and agree how the interior of a sample length will be checked, using an endoscope or an internal swab where the bore matters. Ask what the drying step after a wet process does for a closed section, because a hollow part that stays wet inside is a delayed defect.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Media or swarf trapped in a bore or channel | Open ends left unplugged, a media class smaller than the opening, or no defined retrieval step at the end of the cycle. | Endoscope or internally swab every sample length, and count media into and out of the batch as a routine check. |
| Bow along the length | Unsupported part in the bed, resting on hard supports, or lengths stacked while still wet. | Place on a surface plate or straight reference and measure the gap with a feeler gauge at several stations, against the incoming straightness record. |
| Visible band or line along the mill seam | The seam crown was not cut back evenly, or the media class was too small to reach the seam root without over-working the surrounding surface. | Look along the seam line under raking light from both sides, and measure the remaining crown with a depth gauge on a sectioned sample. |
| Compound residue weeping from a hollow section | Incomplete rinsing of the interior, or a drying step that does not reach inside a closed section. | Stand the length on end over a clean cloth for a set period, then inspect the bore interior for residue after drying. |
Geelong is one of Australia's foremost manufacturing centres with a long industrial history, and manufacturing is again its fastest-growing employment sector after the closures of the Alcoa aluminium smelter and the Ford engine plant. The Geelong Manufacturing Council reports that Greater Geelong reached a record 147,234 local jobs in 2024-25, with manufacturing recording the fastest expansion for the second consecutive year, rising 12.1 per cent to more than 11,400 jobs — a level not seen since before the Alcoa and Ford closures. The region has about 700 manufacturers across transport equipment, metals, extractive industries, chemicals and petroleum, cement, engineering, textiles, timber and food, contributing more than $1.7 billion in value add and around $5.8 billion in annual output; manufacturing categories tracked by the council include advanced manufacturing, automotive, metals, engineering, chemicals and refining, food, textiles and clean economy. Research infrastructure includes Deakin University, the Geelong Technology Precinct, CSIRO facilities, the Institute for Frontier Materials and Carbon Nexus. Defence manufacturing is a growing focus: Hanwha Defence Australia will build 129 Redback infantry fighting vehicles at its Avalon Airport Industrial Precinct facility, supported by local firms including Marand, UMS, Air Radiators, RPC Technologies, IXL Group and Carbon Revolution.
The nearest part of that base to this brief is machinery: The Geelong Manufacturing Council states 'Geelong is one of Australia's foremost manufacturing centres' with 'about 700 manufacturers across industries such as transport equipment, metals, extractive industries, chemicals and petroleum, cement, engineering, textiles, timber and food', and manufacturing contributes more than $1.7 billion in value add to the regional economy.
Geelong's mix of metals, engineering, transport equipment and defence manufacturing produces machined and fabricated metal components in steel, aluminium and stainless where deburring, edge radiusing and surface preparation directly affect coating adhesion, weld quality and assembly fit. The defence vehicle programme at Avalon and its local supply chain impose documented process and inspection requirements on supplied parts, so finishing steps need to be repeatable and traceable rather than operator-judged. Food processing equipment manufacturers in the region add a further requirement: stainless surfaces must be finished without leaving media residue or embedded particles that could create hygiene or corrosion problems.
A Geelong buyer should decide whether the finishing process must produce evidence suitable for a defence or automotive customer's quality system — documented media, cycle parameters and inspection records — or whether a general engineering finish is sufficient, because the documentation burden and the resulting equipment and media choice differ substantially.
Freight context: Port of Geelong (Victoria's second-largest port), Avalon Airport (international airport and Avalon Airport Industrial Precinct), Road and rail links to Melbourne, Ballarat, Colac and the Melbourne CBD, 75 km away. The Geelong Manufacturing Council states the region 'is well connected by road, rail, sea and air, and is home to Victoria's second-largest port and an international airport that supports national and international supply chains and logistics'. Avalon Airport also hosts the industrial precinct where Hanwha Defence Australia is building the Redback infantry fighting vehicles, so the airport precinct is both a freight gateway and a defence manufacturing site. Incoming finishing machines can arrive by sea through the Port of Geelong or by air through Avalon, with Melbourne's port and airport an alternative via the 75 km road and rail corridor.
The Australian Border Force (ABF) is the customs authority and clears imported goods through customs; all goods arriving in Australia must be declared unless an exception applies, goods valued at up to A$1,000 can be imported without a formal import declaration, and entry is made through the Integrated Cargo System (Form B650 for sea or air cargo). Generally all goods imported into Australia are liable for duties and taxes unless an exemption or concession applies, and most imports are subject to 10% GST, so classification, customs valuation and any preferential tariff claim drive the landed cost; a licensed customs broker is the normal route for a first-time importer. Electrical equipment can fall under the Electrical Equipment Safety System, under which the first Australian supplier registers as a Responsible Supplier, holds an ABN, makes a Responsible Supplier Declaration and marks the equipment with the Regulatory Compliance Mark (RCM) in accordance with AS/NZS 4417.1 and AS/NZS 4417.2. Imported goods may also require a trade description naming the country of manufacture, and machinery that is not in-scope electrical equipment still has to meet state work health and safety duties covering plant.
The national standards body is Standards Australia, which publishes Australian Standards (AS) and joint Australian/New Zealand Standards (AS/NZS); on their own, standards are voluntary and there is no general requirement for the public to comply, but state and Commonwealth governments often refer to AS or AS/NZS standards in legislation and they can then become mandatory. For finishing and machinery work, the applicable documents are the ones cited in the buyer's own contract, purchase specification, licence condition or safety management system, together with the marking rules in AS/NZS 4417.1 and AS/NZS 4417.2 for in-scope electrical equipment sold under the EESS.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
Grain direction is the most common reason a set of individually acceptable lengths is rejected as an assembly. Where two lengths butt at a joint, their texture direction has to run the same way, and the pitch and brightness have to be close enough that the joint does not read as a line. That is a planning decision made before the lengths are run, not a sorting decision made afterwards: define the grain direction on the drawing, mark the direction on every length, and keep the orientation through fabrication and despatch. Then inspect the lengths laid end to end as they will be installed, under the agreed light, rather than one at a time on a bench. A direction reversal that is obvious in an assembly can be invisible in a single part.
The trial result is only meaningful against a documented starting point. Photograph each sample under fixed lighting with a scale in frame, note the direction of the incoming texture, and take roughness readings at marked stations with the traverse direction recorded. Note the incoming straightness with the sample on a reference surface, the edge condition at cut ends, and any existing weld, scratch or discolouration. Keep one piece unprocessed as the baseline. When the trial parts come back, the comparison is between the returned parts and these records, not against memory. This is also how a buyer distinguishes a change made by the process from a feature that was present in the material when it arrived.

No. A sample trial produces observations on the parts that were tested under the settings used; it is not a guarantee of a roughness value, a surface class, an appearance or a repeatable production result. Media wear, compound concentration and the condition of incoming material all move the finish over a run. What we can do is show what a given media, compound and cycle direction did to your part, and describe what would need to be controlled to hold that result. Acceptance criteria and any promise made to a client or specifier remain your own.
It should name the texture direction, the faces that carry it, the roughness limit and its measurement conditions if a number is used, the reference panel and the viewing distance, and the faces that are exempt. Add what must be protected: threads, fixing holes, cut ends and machined lands. Where the finish cannot be expressed numerically, a numbered physical reference sample with a written description of its texture direction and appearance is far more useful than an adjective such as brushed or satin. Settling this before a trial is what allows the trial result to be measured against a real requirement.
Lay the lengths end to end as they will be installed, under the light and at the distance agreed for acceptance, and look along the run rather than at each piece separately. A direction reversal or a change in texture pitch that is invisible on a single length usually shows immediately at the joint. The planning side matters more than the inspection: mark the grain direction on every length and keep the orientation through fabrication, packing and despatch. Where the finished parts come from different batches, compare each against the retained reference panel under the same conditions.
Use Geelong, Australia as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Geelong manufacturers work to Australian Standards administered by Standards Australia, and defence suppliers in the Avalon/Geelong Defence Alliance supply chain additionally work to Commonwealth defence procurement specifications and quality-management requirements. Electrically powered machinery must comply with the EESS and be marked with the Regulatory Compliance Mark under AS/NZS 4417.1 and AS/NZS 4417.2 where in scope.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Geelong.
The seam and scratch have to be cut back to an even grain without reducing the wall below the buyer's own minimum.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0787; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0787 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
