A metalwork shop in Glasgow, United Kingdom building architectural metalwork assemblies joins 1.5 m stainless tube to a cast elbow with a circumferential weld, and the joint has to disappear into the grain rather than read as a band. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on welded samples shipped to Xiamen. This brief is written for a buyer in Glasgow working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
What is the longest length in the order, and how will it be supported, carried and packed at every stage between finishing, fabrication and installation?
Which faces of each profile are actually seen when installed, from what distance and under what light, and which faces can be finished to a coarser standard without it showing?
What texture direction is required, and how will that direction be preserved and compared across lengths that are finished in different lots?
Not every face of a profile deserves the same effort. On a wall-mounted handrail the top and the outward face are read from standing height and from an angle, while the underside and the face against the wall are largely out of view. On a cladding mullion the sun-facing plane carries the reflection and the returns do not. Build a simple exposure map: which face, viewed from where, under what light, at what distance. That map settles where the tighter finish is specified and where a coarser one is honest. It also prevents over-finishing hidden faces, which costs cycle time and raises the risk of distortion on thin sections, and it tells the finishing supplier which face must be protected in every rack and stillage.
Media must be small enough to reach the root of a seam or into the concave corner of a rectangular profile, and large enough not to lodge in the bore, in a drilled fixing hole or in a slotted channel. On small sections those two conditions conflict, and the resolution is usually to plug or cap the openings rather than to compromise the media. Where the visible face has a shallow cove, a smaller media class gives better access but wears faster and produces a shorter texture pitch. Where the profile is open, a larger class cuts more evenly and separates more easily. Decide the size against the tightest feature that must be finished and the smallest opening that must stay clear, and state both in the trial request.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media, walnut shell and corn cob | Dry polishing and support for post-wet drying, particularly where a hollow section must not stay wet or carry residue inside. | Low cutting power, and dust generation and media separation need managing in the surrounding area. |
| Ceramic media, spheres and balls | General deburring and edge work on cut ends, brackets and small fittings in the same order as the long runs. | Produces overlapping crater-like marks that work against a linear brushed appearance and can peen a thin wall. |
| Steel media, pins and balls | Bright, strongly linear appearance on stainless where a higher-lustre finish is wanted on accessible faces. | Heavy, needs tight compound control to stay clean and separated, and any iron-bearing debris is a contamination question the buyer has to define and verify. |
| Plastic media, cylindrical | Light surface refinement on thin rectangular sections where holding the shape matters more than cutting power. | Little cut power, and the size class changes quickly as the media wears, which shifts the texture pitch over a run. |
A balustrade or handrail job is never only long runs. It also contains cut-to-length spindles, elbows, brackets, base plates, ball finials and short connector sleeves, often in the same alloy and finish. Those parts are a poor fit for a longitudinal arrangement and a good fit for batch equipment, where a large number of small identical parts can be processed together with controlled part-on-part contact. Treating the two populations as one route is a common planning error: the runs are under-processed because the settings were chosen for the fittings, or the fittings are over-worked and lose their edges. Screen the order into long runs and small fittings, then specify the media class separately for each, even where the final appearance has to read the same.
| Machine route | Where it fits | What it will not do |
|---|---|---|
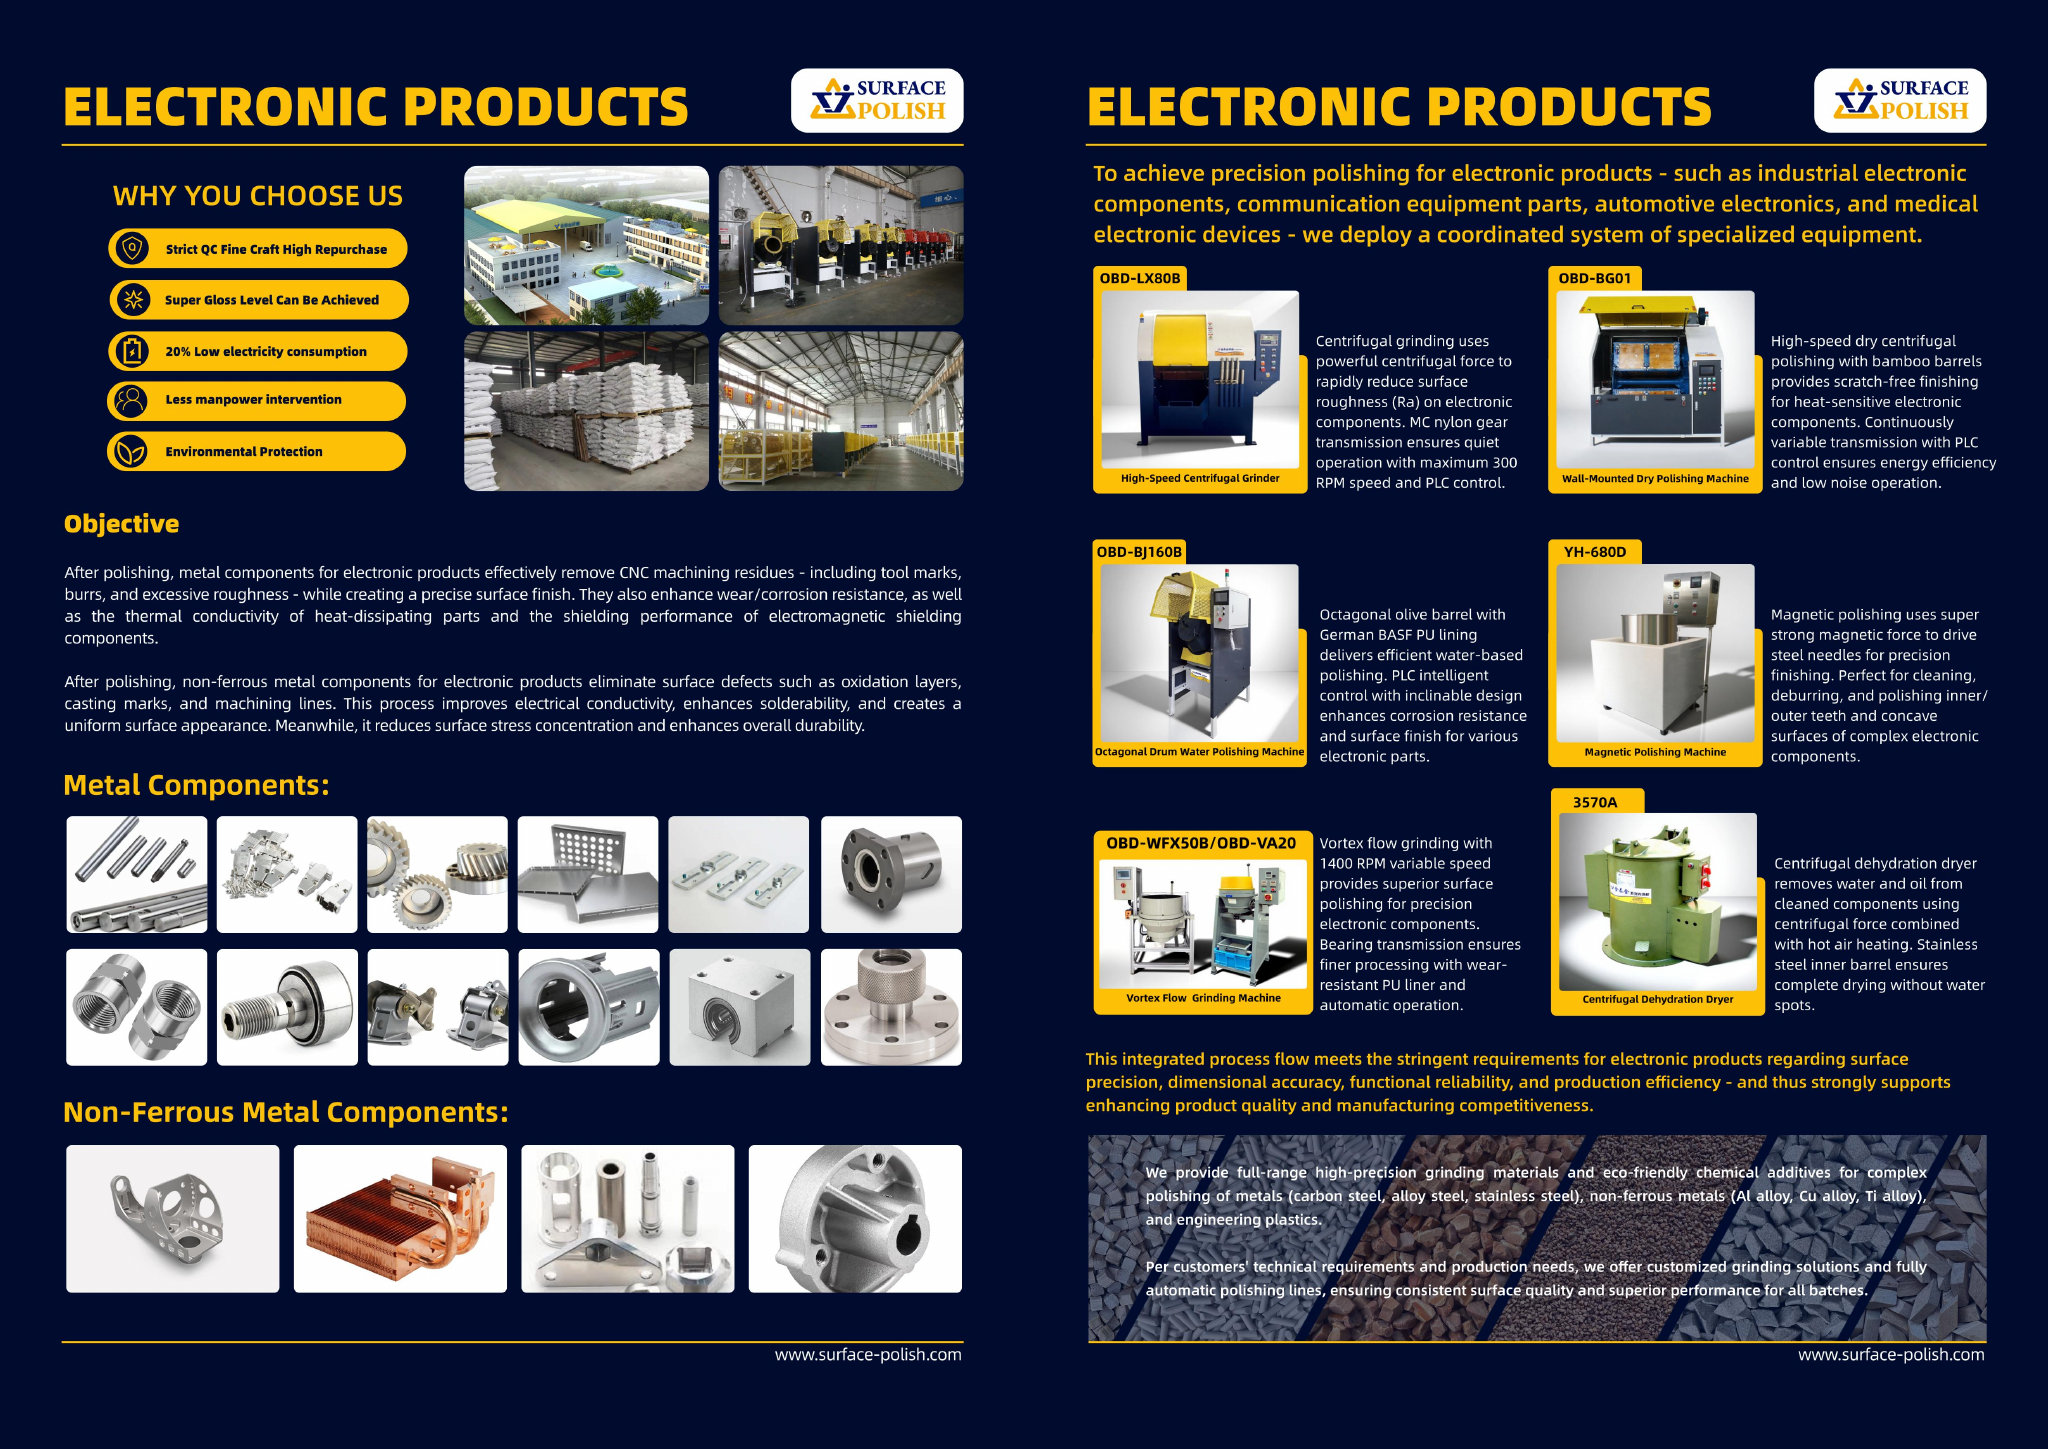
| Centrifugal barrel finishing machine | High-speed finishing of small precise parts, including where a bright appearance is required on a compact geometry. | Chamber geometry and high contact forces rule it out for long, thin-wall or easily marked sections. |
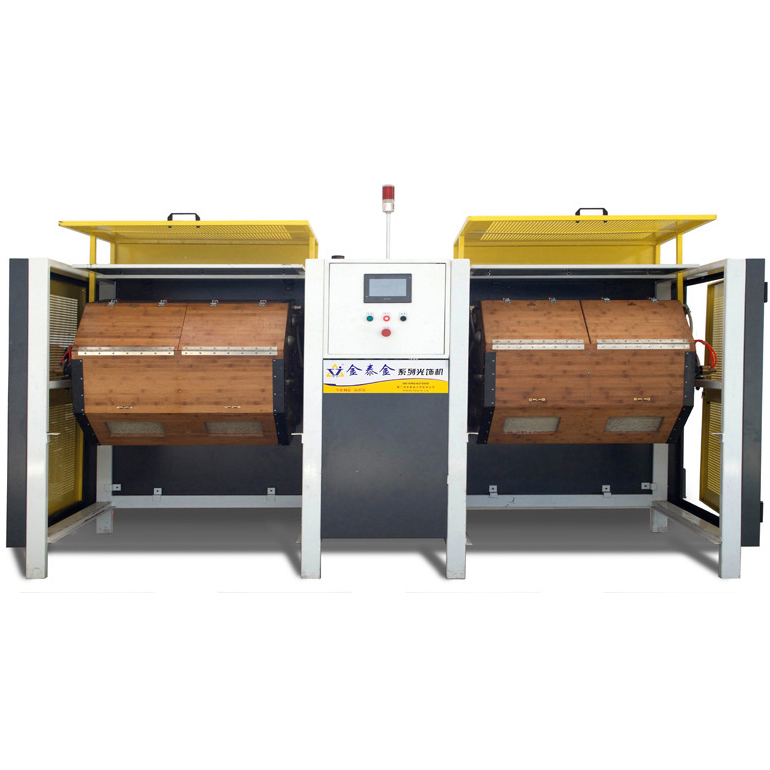
| Tub vibrator | Long and large parts such as architectural tube and profiles, where the process length has to extend along the part. | Bed depth and fixture design decide whether thin sections survive, and fluid flow has to be checked at the far end of the chamber. |
| Vibratory finishing machine, bowl type | General edge blending and surface refinement on brackets, base plates, cut spindles and other small fittings. | Chamber diameter caps the part length, and a long tube cannot be worked evenly in the circular bed. |
| Magnetic finishing machine | Small precise parts and localised areas that are difficult to reach with loose media in a conventional chamber. | Size and mass limits keep it away from architectural lengths and large diameter profiles. |
Open tube ends, slotted channels and drilled fixings all collect media, swarf and compound. The failure is rarely visible at the end of the cycle; it shows up after the part is installed, when compound weeps from a bore onto a visible face or when a trapped particle works loose during handling and scratches an adjacent length. Treat removal as a designed step rather than a rinse: plug or cap what should never see media, count media in and out of each batch, and agree how the interior of a sample length will be checked, using an endoscope or an internal swab where the bore matters. Ask what the drying step after a wet process does for a closed section, because a hollow part that stays wet inside is a delayed defect.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Dents and part-on-part nibbling | Parts running loose together in the load, or a finished part contacting a bare support or another length. | Inspect the contact line between parts with side lighting, and run a straightedge over the damaged area to judge depth. |
| Orange peel mottling on the visible face | Over-working with a coarse medium, or excessive pressure on a soft or thin section, which deforms the surface rather than cutting it. | Reflect a straight edge or a linear light source in the surface, and take a roughness reading at the same spot to show the divergence between number and appearance. |
| Hazy or milky patch with a dull reflection | Uneven cut, worn media in part of the chamber, or weak compound flow at the far end of a long tub. | Compare the near end and the far end of the same length, and check compound concentration and fluid flow at both ends of the chamber. |
| Compound residue weeping from a hollow section | Incomplete rinsing of the interior, or a drying step that does not reach inside a closed section. | Stand the length on end over a clean cloth for a set period, then inspect the bore interior for residue after drying. |
Glasgow is Scotland's largest city, with a metropolitan region of 1.85 million people that Invest Glasgow records as generating £48bn GVA, and the Glasgow City Region accounts for around a third of Scotland's output, business base, research power and employment. Invest Glasgow lists clinical life sciences and biotechnology, energy and green transition, space and satellite technology, and advanced manufacturing and precision engineering among the city region's key clusters. ADS Scotland, established in 2005, reports that the aerospace, defence, security and space industries add £3.7 billion to the Scottish economy, employ 36,900 people and reached £9 billion of turnover, and its Scotland Council includes BAE Systems, Rolls-Royce, Leonardo, Thales, GE Aerospace and Babcock International.
The nearest part of that base to this brief is energy: Invest Glasgow lists 'Energy and Green Transition' as a key cluster of the Glasgow City Region, and Peel Ports' Clydeport operates Hunterston PARC, which it reports is being developed as a key player in the offshore market.
Glasgow's combination of precision engineering, an aerospace supply chain and clinical life-sciences work means machined and formed parts usually carry defined edge and surface acceptance criteria, and those are set by the customer's specification rather than by a local process convention. Clydeport's container, project and bulk cargo handling gives the city region an established route for importing finishing machines, media and compounds, with two new £25m ship-to-shore cranes at Greenock Ocean Terminal operational from autumn 2024.
A Glasgow buyer should decide early whether the part is aerospace or defence supply-chain work - where edge and surface criteria come from the prime contractor's specification - or general precision engineering, because that determines the documentation and the process route the finishing cell has to support.
Freight context: Clydeport (Peel Ports): Greenock Ocean Terminal, King George V Dock and the River Clyde network, Eurocentral (new 353,000 sq ft industrial space under a forward-funding agreement, reported by Glasgow Chamber of Commerce). Peel Ports states that Clydeport handles more than 15.4 million tonnes of cargo a year and has invested £25m in two new ship-to-shore cranes at Greenock Ocean Terminal to accommodate increased demand and support growth in transatlantic trade; the Glasgow Chamber of Commerce is the city's business body and reports industrial development at Eurocentral.
China does not appear in the alphabetical list of trade agreements in effect published by the Department for Business and Trade, so Chinese-origin machinery imported into the UK cannot claim a preferential agreement rate. Duty is instead determined by the commodity code declared on the import declaration, and the UK's customs authority is HM Revenue and Customs (HMRC), which ONS also names as the largest single data source behind UK trade-in-goods statistics. Because a GB-prefixed EORI number is a precondition for importing into England, Scotland or Wales, a Chinese seller's UK buyer must already hold that registration before any machine ships.
English is the working language of contracts, drawings and conformity paperwork, so quotations, technical files and Declarations of Conformity should be supplied in English. UK manufacturers have now recovered above 2019 output levels in every English region and devolved nation except Northern Ireland, and the sector is concentrated in food and drink and transport equipment, with the North West the largest manufacturing region by total output. Buyers typically expect the UKCA/CE route, a Declaration of Conformity and a UK-established economic operator to be identified before order, and they need commercial invoices, customs declarations and the C79 retained in a form their finance team can use for import VAT recovery. No source verified in this research establishes a mandated payment instrument, so payment structure should be treated as commercial negotiation rather than a regulatory requirement.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A roughness reading on tube has to be taken with the same care as one on a flat coupon, and usually more. State the location by distance from a reference end, the traverse direction relative to the grain, and the cut-off and evaluation length, and keep them the same for the first article and for production checks. Along the grain and across the grain give different values on the same surface, so a reading that does not say which direction it was taken in cannot be compared with anything. Curvature limits how a skid or a shoe can sit on the surface, particularly on small-diameter tube, and a reading taken with a poorly seated pickup is not evidence. Repeat the measurement at several stations along the length, because the ends of a part often differ from the middle.
If two media classes or two cycle settings are being compared, run them on adjacent cut sections from the same original length so the only difference is the variable under test. Keep the position in the load and the cycle length the same where possible, label the pieces before they are run, and have the returned parts judged together in one session under the agreed light rather than one at a time as they arrive. Where several people are judging, ask each to rank the pieces before discussing them, so the strongest opinion does not set the answer. A handful of sections can compare two settings; what cannot be compared is one section from a trial run one week against another run later under different conditions.

Directional satin textures usually come from elongated or angular media rather than spheres. Angle-cut triangles and cylinders strike along their axis and leave a linear pattern, while rounded shapes produce overlapping craters that read soft and slightly dimpled. The size class then has to reach the root of a mill seam or the cove of a rectangular profile without lodging in the bore or a fixing hole. Media selection is confirmed against the actual part in a trial, because the incoming grain, the wall thickness and the visible face all shift the answer. Send sections from the production delivery and say which face must carry the grain.
Lay the lengths end to end as they will be installed, under the light and at the distance agreed for acceptance, and look along the run rather than at each piece separately. A direction reversal or a change in texture pitch that is invisible on a single length usually shows immediately at the joint. The planning side matters more than the inspection: mark the grain direction on every length and keep the orientation through fabrication, packing and despatch. Where the finished parts come from different batches, compare each against the retained reference panel under the same conditions.
Length is a handling question before it is a finishing question. Long architectural sections are run in a tub or on a dedicated longitudinal arrangement rather than a round bowl, and the practical limit depends on the chamber length, the supports available and how the length is packed for shipping. For a trial, send cut sections from the production material and one full-length piece where bend or end effects could matter, so the arrangement is chosen against the real part rather than an average. Parts travel to our factory in Xiamen, and we do not process anything in United Kingdom or Glasgow.
Use Glasgow, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
UKCA or CE marking with a Declaration of Conformity applies to machinery placed on the Great Britain market, HSE's work equipment and machinery and COSHH regimes cover operation and hazardous substances, and Scotland's aerospace and defence buyers normally receive quality and assurance requirements flowed down from primes such as those represented on the ADS Scotland Council.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Glasgow.
The joint weld has to disappear into the grain so the joint does not read as a dark or bright band in the finished run.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0267; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0267 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
