A stair and balustrade supplier in The Hague, Netherlands working on architectural metalwork has a mixed order of 200 cut spindles at 12 mm diameter and 900 mm long, plus 40 ball finials in the same alloy and finish. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to Xiamen. This brief is written for a buyer in The Hague working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
Will the finish be judged by a roughness number, by a physical reference panel, or by both, and who views the parts before they are accepted?
How much of the incoming mill seam, joint weld or transit scratch must be removed, and what minimum wall thickness has to remain after that removal?
What is the longest length in the order, and how will it be supported, carried and packed at every stage between finishing, fabrication and installation?
For architectural tube the first screening number is the ratio of wall thickness to outside diameter or to width across the flat. A 60 mm round tube at 1.5 mm wall and the same tube at 3 mm wall are not the same finishing problem: the thin one will show ovality, bow and dents long before the finish is acceptable, and the media that works on the heavy wall will mark the light one. Ask for the mill's nominal wall plus the tolerance band, confirm the actual wall at three places with an ultrasonic gauge or a sectioned offcut, and note any thinning at bends or swaged ends. Record the as-received straightness as well, because a bowed length will read as a finish fault when it is really a handling fault.
A tub vibrator uses a long rectangular chamber, so the process length can be extended along one axis while the bed depth stays modest. That allows a length to be carried through a media bed deep enough to work the visible face and shallow enough to keep the load moving. Decisions to settle with the equipment supplier are the usable chamber length against the longest part, whether lengths run one at a time or several end to end, how the part is supported so it does not ride on top of the media, and how the open ends are kept clear of media. A tub also tolerates the mid-length supports that thin rectangular sections need, which a circular chamber cannot accommodate without a purpose-built fixture.
| Machine route | Where it fits | What it will not do |
|---|---|---|
| Dry polishing machine and dryer | Post-wet drying and dry luster work, particularly where a hollow section must come out clean and dry inside. | Dry routes cut less than wet media, and dust control and media separation need planning. |
| Grinding finishing machine | Higher material removal where a mill seam, a joint weld or a deep scratch has to be cut back before surface refinement. | Removal is aggressive, so depth control and wall thickness limits have to be set before the cycle is run. |
| Disc finishing machine | Fast, high-energy cycles for small to medium fittings and hardware where a short cycle is the priority. | The high energy that makes it fast will distort, mark or bend thin and long parts. |
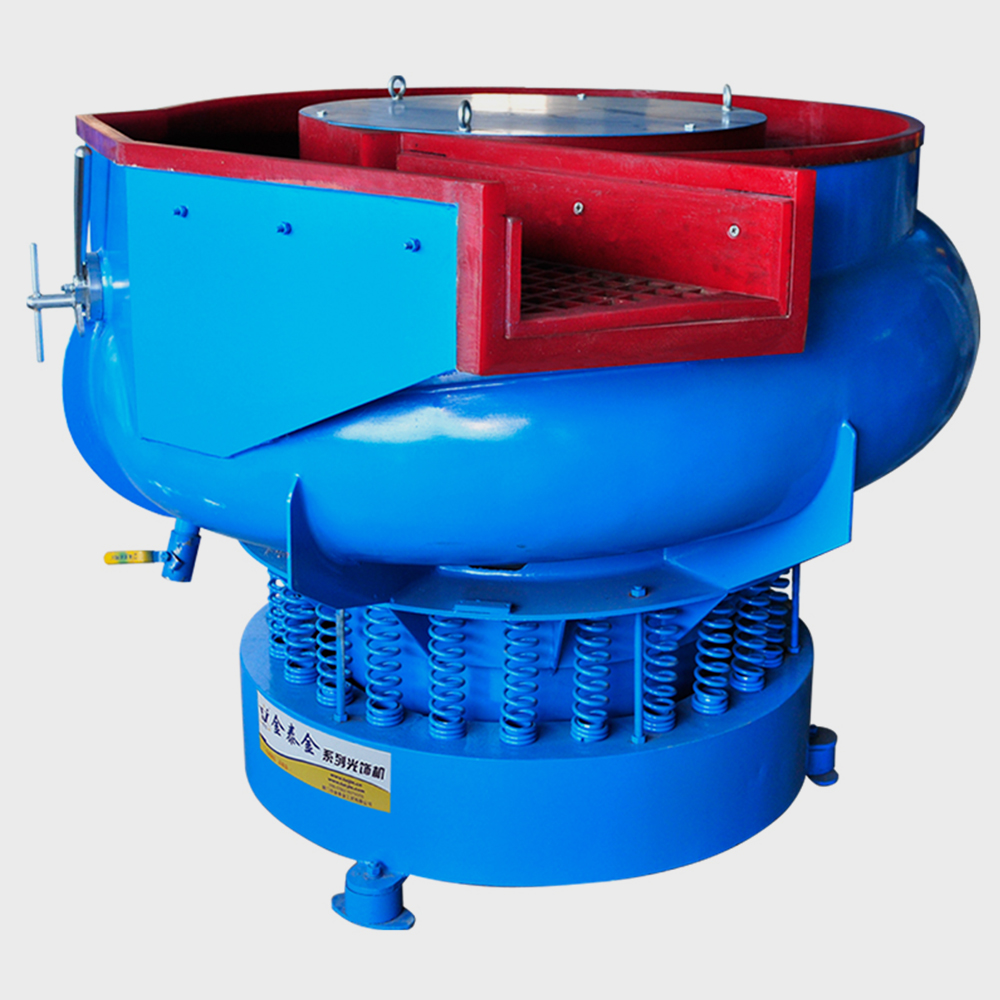
| Vibratory finishing machine, bowl type | General edge blending and surface refinement on brackets, base plates, cut spindles and other small fittings. | Chamber diameter caps the part length, and a long tube cannot be worked evenly in the circular bed. |
Ceramic media cuts harder, holds its shape longer and is the usual choice when a previous scratch or a weld seam has to be removed from stainless. Plastic media is gentler, lighter and less likely to mark a thin or soft section, at the cost of a slower cut and a shorter texture. Steel media produces a bright appearance and strongly linear marks, but it is heavy, it needs well-controlled compound to keep it clean and separated, and it raises a question about whether any iron-bearing debris is acceptable in the buyer's own cleanliness or contamination control. That last point is a requirement for the buyer to define and verify, and it is not something a supplier can decide on their behalf.

| Media | Best fit | Watch out for |
|---|---|---|
| Dry media, walnut shell and corn cob | Dry polishing and support for post-wet drying, particularly where a hollow section must not stay wet or carry residue inside. | Low cutting power, and dust generation and media separation need managing in the surrounding area. |
| Steel media, pins and balls | Bright, strongly linear appearance on stainless where a higher-lustre finish is wanted on accessible faces. | Heavy, needs tight compound control to stay clean and separated, and any iron-bearing debris is a contamination question the buyer has to define and verify. |
| Plastic media, cones and triangles | Gentle work on thin-wall sections and softer alloys, and where marking or distortion is the main risk to be managed. | Slower cut and shorter media life, with limited effect on a deep scratch or a heavy seam. |
| Plastic media, cylindrical | Light surface refinement on thin rectangular sections where holding the shape matters more than cutting power. | Little cut power, and the size class changes quickly as the media wears, which shifts the texture pitch over a run. |
A surface can measure inside a roughness band and still fail visually. Orange peel, a mottled texture with a pitch of a few millimetres, appears when the surface is over-worked with a coarse medium or worked with too much pressure on a soft or thin section. Hazing is the diffuse, milky appearance that follows a fine but non-uniform cut. Both are geometry effects rather than amplitude effects, so a profilometer reading across them may be entirely acceptable while a reflection test shows a broken image. This is why an architectural finish cannot be accepted on a roughness number alone, and why a visual standard viewed under defined light at a defined distance has to sit beside the numeric one. Ra and appearance answer different questions.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Dents and part-on-part nibbling | Parts running loose together in the load, or a finished part contacting a bare support or another length. | Inspect the contact line between parts with side lighting, and run a straightedge over the damaged area to judge depth. |
| Media or swarf trapped in a bore or channel | Open ends left unplugged, a media class smaller than the opening, or no defined retrieval step at the end of the cycle. | Endoscope or internally swab every sample length, and count media into and out of the batch as a routine check. |
| Orange peel mottling on the visible face | Over-working with a coarse medium, or excessive pressure on a soft or thin section, which deforms the surface rather than cutting it. | Reflect a straight edge or a linear light source in the surface, and take a roughness reading at the same spot to show the divergence between number and appearance. |
| Longitudinal scratch running along the part axis | Incoming coil or straightener marks, media or swarf dragged along the surface during the cycle, or a finished length sliding over a bare support between operations. | View the surface under raking light at a low angle along the axis, compare the same station on several parts, and compare against the retained reference panel. |
The Hague is the seat of the Dutch government and the international city of peace and justice, so its economic base is services, international organisations and technology rather than heavy manufacturing. The city supports Stichting The Hague Security Delta, which brings government, knowledge institutions and companies together on innovation, talent development and digital resilience, and it hosts the National Cyber Security Centre, Europol, Eurojust, NATO bodies and the HSD Campus. The Hague & Partners lists cybersecurity, IT and tech, impact, humanity, legal and policy, rule of law and new energy as the city's key sectors, and notes that many energy companies, including Shell, Orsted and Total, have located there. Scheveningen harbour is the city's port, for which the municipality maintains a harbour vision through 2050.
The nearest part of that base to this brief is automation: The Hague & Partners states that the city benefits from an excellent IT infrastructure and a flexible multilingual and multinational talent pool.
The Hague has little heavy manufacturing, so finishing demand is concentrated in maintenance of building-services, port and marine equipment around Scheveningen and in technical hardware used by the city's energy, IT and security organisations. For those users the typical requirement is small-batch edge control, cleaning and surface preparation of stainless, aluminium and steel components rather than production-scale deburring.
A buyer here should first decide whether the need is a small in-house finishing capability for maintenance and prototyping or an outsourced batch process, and then fix the material mix and the required edge and roughness specification, because a maintenance workload and a production workload point to different machine types.
Freight context: Scheveningen harbour, Rotterdam The Hague Airport. Scheveningen is the city's harbour and is covered by a municipal harbour vision through 2050; the city also has Rotterdam The Hague Airport and is roughly 30 minutes from Schiphol. Machines imported from outside the EU are declared to Dutch Customs at their point of entry, and machine tools arriving by sea will normally clear customs at Rotterdam before road transport to The Hague.
Business is conducted in Dutch, but engineering and procurement communication in these sectors is routinely handled in English. Buyers are KVK-registered legal entities and expect a clear commercial entity to contract with, an EORI number for customs, correct HS/TARIC classification, and a full CE technical file including the EC Declaration of Conformity and a manual in the correct language; a technical construction file held by the manufacturer is normally part of the qualification pack. For EU-internal supply the invoice carries 0% VAT with the customer's VAT identification number and the customer accounts for 21% Dutch VAT in its own return, so a Chinese seller shipping directly from outside the EU must be clear about who is importer of record and who carries the duty and import VAT. Trade and investment support is organised through bodies such as KVK, RVO, the regional development agencies and the Trade and Innovate NL network, and the Dutch technology industry is represented by FME.
Goods entering the Netherlands from outside the EU must be declared to Dutch Customs (Douane, part of the Belastingdienst); the importer needs an EORI number, import duty is calculated on the customs value (goods value plus transport and insurance to the EU external border), and import VAT is paid at the border unless an article 23 permit or a fiscal representative is used. CE marking is mandatory for most machinery placed on the EEA market: the Machinery Regulation replaced the Machinery Directive and manufacturers must comply with the new requirements by 20 January 2027. The importer must verify that the conformity assessment was carried out correctly, that CE marking is applied properly, that the technical file is present and complete, and that the user manual is supplied in the correct language; the manufacturer's EC Declaration of Conformity must be kept. Dutch companies imported over EUR 140 billion of machinery and appliances in 2024, 24% of total Dutch goods imports.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A roughness reading on tube has to be taken with the same care as one on a flat coupon, and usually more. State the location by distance from a reference end, the traverse direction relative to the grain, and the cut-off and evaluation length, and keep them the same for the first article and for production checks. Along the grain and across the grain give different values on the same surface, so a reading that does not say which direction it was taken in cannot be compared with anything. Curvature limits how a skid or a shoe can sit on the surface, particularly on small-diameter tube, and a reading taken with a poorly seated pickup is not evidence. Repeat the measurement at several stations along the length, because the ends of a part often differ from the middle.
The first production batch is usually the best one, because the media charge is fresh and the fluid is at its set point. What changes over a run is media wear, which reduces cut and shifts the surface toward a finer and dimmer appearance; the build-up of swarf and fines in the fluid; and the arrival of material from a different heat or mill finish. Plan for it: a media top-up and screening routine with a defined interval, a fluid change criterion based on measurement rather than appearance, and a check length kept from each lot for comparison. Agree in advance what will be done if a later lot does not match the retained reference, so the decision is procedural rather than improvised.

Support the profile rather than letting it lie loose. Cradles shaped to the section, dividers or compartments that keep lengths apart, end plugs that hold the open section, and controlled orientation in the bed all reduce the load a flat face sees. Rectangular sections are more exposed than round ones because a flat face has no hoop stiffness across its width, so the thinnest wall in the order should set the fixture design. Send the thinnest and widest section you use, not an average one, so the trial is run against the part most likely to distort.
Directional satin textures usually come from elongated or angular media rather than spheres. Angle-cut triangles and cylinders strike along their axis and leave a linear pattern, while rounded shapes produce overlapping craters that read soft and slightly dimpled. The size class then has to reach the root of a mill seam or the cove of a rectangular profile without lodging in the bore or a fixing hole. Media selection is confirmed against the actual part in a trial, because the incoming grain, the wall thickness and the visible face all shift the answer. Send sections from the production delivery and say which face must carry the grain.
A round bowl moves its load on a circular path in a chamber whose diameter caps the part length, and extending that chamber to take a six-metre length stops being practical. The deeper issue is the bed: a long tube occupies too much of the load for the media to circulate around it, so the part is dragged and struck instead of worked evenly. Long sections are better run in a tub, where the process length can be extended along one axis, or on a dedicated arrangement that moves the part or the heads along the length.
Use The Hague, Netherlands as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Buyers here would reference the CE machinery regime (Machinery Regulation from 20 January 2027) and the Dutch/EN-ISO surface-finishing standards published by NEN, such as NEN-EN-ISO 2080. Where equipment is used in marine or coastal conditions, corrosion-protection and coating-preparation specifications are normally added by the asset owner on top of those base standards.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in The Hague.
The long spindles and the small finials need different handling, yet the finished appearance has to read the same on both.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0657; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0657 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
