A steelwork fabricator in Liverpool, United Kingdom supplying architectural metalwork holds 4 m lengths of 88.9 mm stainless pipe at 5 mm wall with a heavy mill seam and a transit scratch, and needs the metal cut back without thinning the wall past the buyer's own limit. SurfacePolish supplies finishing machines, media and compounds across borders and runs a free sample trial on parts shipped to Xiamen. This brief is written for a buyer in Liverpool working on architectural metalwork; it describes equipment, media and a scoped sample review, not a local polishing service.
Which faces of each profile are actually seen when installed, from what distance and under what light, and which faces can be finished to a coarser standard without it showing?
Which wall thickness and section shape in the order is most likely to distort, and what fixture, cradle or support will protect it?
What texture direction is required, and how will that direction be preserved and compared across lengths that are finished in different lots?
Once a length runs past roughly a metre and a half, handling stops being a detail and becomes the deciding constraint. A six-metre handrail cannot be turned in a chamber, cannot be stacked with its finished face against another part, and cannot be lifted by two people without risk of a bow. The screening questions are: what is the longest length in the order, how is it moved to and from finishing, is it cut to final size before or after finishing, and what supports it at every stage. Answering these sets the machine class, the cradle design and the inspection points. A buyer who fixes the finish specification first and the handling plan later usually discovers the finish cannot be held on the long lengths that matter most.
Inside whichever machine is chosen, the fixture or the load arrangement decides whether thin sections survive. A thin-wall rectangular profile will flatten under its own weight in a deep bed, and two loose lengths finished together will nibble each other along the contact line. Practical measures are cradles that follow the profile, dividers or compartments that keep parts apart, end caps or plugs for open tube ends, and clip-on carriers that present the visible face to the media evenly. The fixture also fixes the finish: a part that rotates freely receives an inconsistent texture, while a part held at a controlled orientation receives a directional one. Build the fixture around the longest and thinnest part in the order, not the average one.
| Machine route | Where it fits | What it will not do |
|---|---|---|
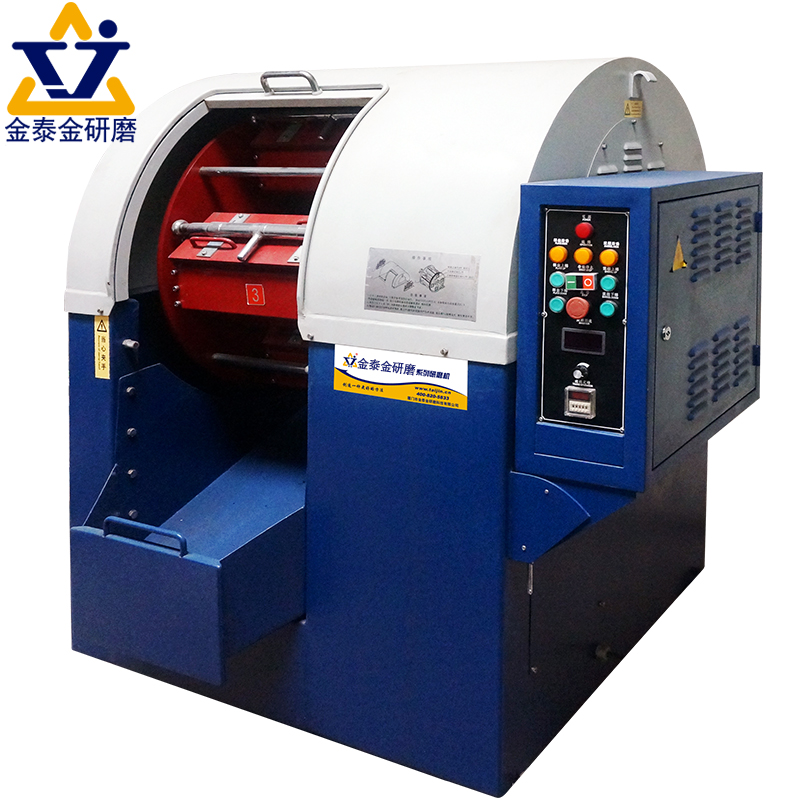
| Centrifugal barrel finishing machine | High-speed finishing of small precise parts, including where a bright appearance is required on a compact geometry. | Chamber geometry and high contact forces rule it out for long, thin-wall or easily marked sections. |
| Disc finishing machine | Fast, high-energy cycles for small to medium fittings and hardware where a short cycle is the priority. | The high energy that makes it fast will distort, mark or bend thin and long parts. |
| Barrel finishing machine, rotary barrel tumbling | Gentle, precise batch processing of small parts, finials, sleeves and short connector pieces. | Part length and part-on-part contact restrict it to short fittings rather than long architectural runs. |
| Vibratory finishing machine, bowl type | General edge blending and surface refinement on brackets, base plates, cut spindles and other small fittings. | Chamber diameter caps the part length, and a long tube cannot be worked evenly in the circular bed. |
The shape of the working media sets the character of the surface as much as its size does. Spheres and other rounded shapes produce overlapping craters, which read as a soft, slightly dimpled surface and work against a linear brushed appearance. Angle-cut triangles, cylinders, cones and other elongated shapes strike along their axis and leave a more linear pattern, which is what architectural tube usually needs. Where a weld seam or a deep longitudinal scratch must be cut back, the aggressiveness comes from the contact geometry and the media mass rather than from extra speed. For a run that has to show a consistent direction, choose a shape class whose marks align with the intended grain direction, and then keep that class stable as the media wears.

| Media | Best fit | Watch out for |
|---|---|---|
| Ceramic media, angle-cut triangles | Heavier cutting and seam removal on stainless tube and profiles, where a directional linear texture on the visible face is wanted. | Wears down and changes effective size class, generates sludge, and can over-round thin sections or chip on sharp edges. |
| Plastic media, cylindrical | Light surface refinement on thin rectangular sections where holding the shape matters more than cutting power. | Little cut power, and the size class changes quickly as the media wears, which shifts the texture pitch over a run. |
| Ceramic media, spheres and balls | General deburring and edge work on cut ends, brackets and small fittings in the same order as the long runs. | Produces overlapping crater-like marks that work against a linear brushed appearance and can peen a thin wall. |
| Ceramic media, cylinders and other elongated shapes | Linear, directional refinement of the visible faces of round and rectangular profiles after the seam has been cut back. | Flat sides and ends mark differently, and the length-to-diameter ratio limits how far the media reaches into a shallow cove. |
Open tube ends, slotted channels and drilled fixings all collect media, swarf and compound. The failure is rarely visible at the end of the cycle; it shows up after the part is installed, when compound weeps from a bore onto a visible face or when a trapped particle works loose during handling and scratches an adjacent length. Treat removal as a designed step rather than a rinse: plug or cap what should never see media, count media in and out of each batch, and agree how the interior of a sample length will be checked, using an endoscope or an internal swab where the bore matters. Ask what the drying step after a wet process does for a closed section, because a hollow part that stays wet inside is a delayed defect.
| Failure mode | Likely cause | How to catch it |
|---|---|---|
| Dents and part-on-part nibbling | Parts running loose together in the load, or a finished part contacting a bare support or another length. | Inspect the contact line between parts with side lighting, and run a straightedge over the damaged area to judge depth. |
| Orange peel mottling on the visible face | Over-working with a coarse medium, or excessive pressure on a soft or thin section, which deforms the surface rather than cutting it. | Reflect a straight edge or a linear light source in the surface, and take a roughness reading at the same spot to show the divergence between number and appearance. |
| Twist along the length | Differential working of opposite faces, or clamping and stacking that loads the section unevenly. | Rest the length on a reference surface and compare the angular orientation of the two end sections with a square. |
| Shade change or discolouration at a welded area | The heat-affected zone responds differently to the same media and compound cycle than the parent metal. | Compare the area with adjacent metal under the agreed light and distance, and photograph it with a scale alongside the retained reference. |
Liverpool's industrial base is port-led: the Port of Liverpool operates two container terminals, the Royal Seaforth Container Terminal and the £400m Liverpool2 deep-water terminal, on both banks of the River Mersey. Peel Ports describes the port as the flagship handling hub of its 'Heart of Britain' steel and metals network and as a vital gateway for UK steel imports and distribution, and reports a record of over 702,000 tonnes of bulk steel and metals handled. Make UK classes the North West as the UK region with the highest total manufacturing output, and the Liverpool City Region Combined Authority is the area's statutory economic body.
For this brief the relevant part of that base is architectural: ABP describes the Port of Garston in Liverpool as handling a wide array of cargo including steel products at around 500,000 tonnes a year, the metals flow behind the city's fabrication and architectural metalwork firms.
Steel and metals handling at scale - the port reports a record of more than 702,000 tonnes of bulk steel and metals - supports a local base of stockholders, fabricators and processing firms whose plate, bar and sections need edge and surface conditioning before fabrication or dispatch. Media, machines and sample parts for that work can be landed at Liverpool2 or on the Manchester Ship Canal and moved inland on the same rail and road links that already carry the steel.
A Liverpool buyer should confirm the landed-cost and inland-movement plan at the same time as the machine specification, because equipment and media can clear through Liverpool2 or the Manchester Ship Canal, and the finishing acceptance criterion for steel work is normally defined by the customer's order rather than by a generic 'deburred' note.
Freight context: Port of Liverpool: Royal Seaforth Container Terminal and Liverpool2 (deep water), Port of Garston, Liverpool (ABP) - dry bulks and steel products, Liverpool Airport (11.5 miles from the port, per Peel Ports). Peel Ports states that the Port of Liverpool has direct deep-sea and short-sea connections including a niche Far East service, with a purpose-built rail terminal for onward movement, and lists road distances of 105 miles to Birmingham and 217 miles to London. ABP's Port of Garston, Liverpool handles around 500,000 tonnes of cargo a year including steel products, and ABP's Hams Hall terminal links the North West to Midlands distribution.
English is the working language of contracts, drawings and conformity paperwork, so quotations, technical files and Declarations of Conformity should be supplied in English. UK manufacturers have now recovered above 2019 output levels in every English region and devolved nation except Northern Ireland, and the sector is concentrated in food and drink and transport equipment, with the North West the largest manufacturing region by total output. Buyers typically expect the UKCA/CE route, a Declaration of Conformity and a UK-established economic operator to be identified before order, and they need commercial invoices, customs declarations and the C79 retained in a form their finance team can use for import VAT recovery. No source verified in this research establishes a mandated payment instrument, so payment structure should be treated as commercial negotiation rather than a regulatory requirement.
BSI is the UK's National Standards Body, and British Standards (BS, including adopted BS EN ISO texts) are the documents a UK buyer's surface-finish, edge and cleanliness specifications are normally written against and purchased through. On the plant side, HSE maintains the work equipment and machinery topic covering the safe supply and use of machinery, and the COSHH regime, which requires employers to identify, assess and control risks from hazardous substances - the regime that applies to finishing compounds, abrasive media and the dust and effluent they generate.
SurfacePolish supplies from Xiamen, China. The buyer's own destination rules, conformity marking, tariff classification and documentation responsibilities stay with the buyer; confirm them against the authorities named above before ordering.
A roughness reading on tube has to be taken with the same care as one on a flat coupon, and usually more. State the location by distance from a reference end, the traverse direction relative to the grain, and the cut-off and evaluation length, and keep them the same for the first article and for production checks. Along the grain and across the grain give different values on the same surface, so a reading that does not say which direction it was taken in cannot be compared with anything. Curvature limits how a skid or a shoe can sit on the surface, particularly on small-diameter tube, and a reading taken with a poorly seated pickup is not evidence. Repeat the measurement at several stations along the length, because the ends of a part often differ from the middle.
The trial result is only meaningful against a documented starting point. Photograph each sample under fixed lighting with a scale in frame, note the direction of the incoming texture, and take roughness readings at marked stations with the traverse direction recorded. Note the incoming straightness with the sample on a reference surface, the edge condition at cut ends, and any existing weld, scratch or discolouration. Keep one piece unprocessed as the baseline. When the trial parts come back, the comparison is between the returned parts and these records, not against memory. This is also how a buyer distinguishes a change made by the process from a feature that was present in the material when it arrived.

Start with a physical sample: if a short section can be removed without damage, send it, together with the retained reference panel from the original order if one exists. An installed surface has aged, been cleaned and possibly scratched, so a new length will not reproduce it exactly, and the visible difference is usually easier to manage by finishing a group of adjacent lengths than by matching one piece in isolation. A trial reports what the tested settings produced on the sample you sent; deciding how close is close enough remains with your own acceptance process and the people who will look at it daily.
No. A sample trial produces observations on the parts that were tested under the settings used; it is not a guarantee of a roughness value, a surface class, an appearance or a repeatable production result. Media wear, compound concentration and the condition of incoming material all move the finish over a run. What we can do is show what a given media, compound and cycle direction did to your part, and describe what would need to be controlled to hold that result. Acceptance criteria and any promise made to a client or specifier remain your own.
Length is a handling question before it is a finishing question. Long architectural sections are run in a tub or on a dedicated longitudinal arrangement rather than a round bowl, and the practical limit depends on the chamber length, the supports available and how the length is packed for shipping. For a trial, send cut sections from the production material and one full-length piece where bend or end effects could matter, so the arrangement is chosen against the real part rather than an average. Parts travel to our factory in Xiamen, and we do not process anything in United Kingdom or Liverpool.
Use Liverpool, United Kingdom as the destination on the enquiry and state whether the deliverable is equipment, media and compound, a representative sample review or a line concept. A destination does not imply local stock, a local service point or a local delivery time.
Equipment placed on the Great Britain market needs UKCA or CE marking with a Declaration of Conformity, and HSE's work equipment and machinery and COSHH regimes cover operation and the media, compounds and dust involved. Steel and metals buyers additionally work to the material, inspection and certification requirements written into their own order specification for the finished component.
Sources were retrieved on 2026-09-29 and describe the local industrial and trade context only. They do not evidence any SurfacePolish project, shipment, installation or service in Liverpool.
The seam and scratch have to be cut back to an even grain without reducing the wall below the buyer's own minimum.
Send the material, dimensions, approximate weight, batch quantity, the incoming condition and photographs of the difficult features. Mark which features must not be contacted by media and state how the result will be inspected. This form carries source reference PSEO-0257; quote it if you prefer an additional manual reference.
Open the SurfacePolish enquiry form Email a prepared enquiry
No price, lead time, certification or result is promised here. Confirm whether a sample trial is available for the specific part and what the trial can and cannot show.
Page PSEO-0257 · revised 2026-09-29 · cross-border equipment, media and scoped sample review. City context is sourced and cited above.
Use this local checker to identify missing part and inspection information. It prepares a technical-review brief; it does not approve a machine, process recipe or production result.
Complete the part details to prepare a review brief.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
