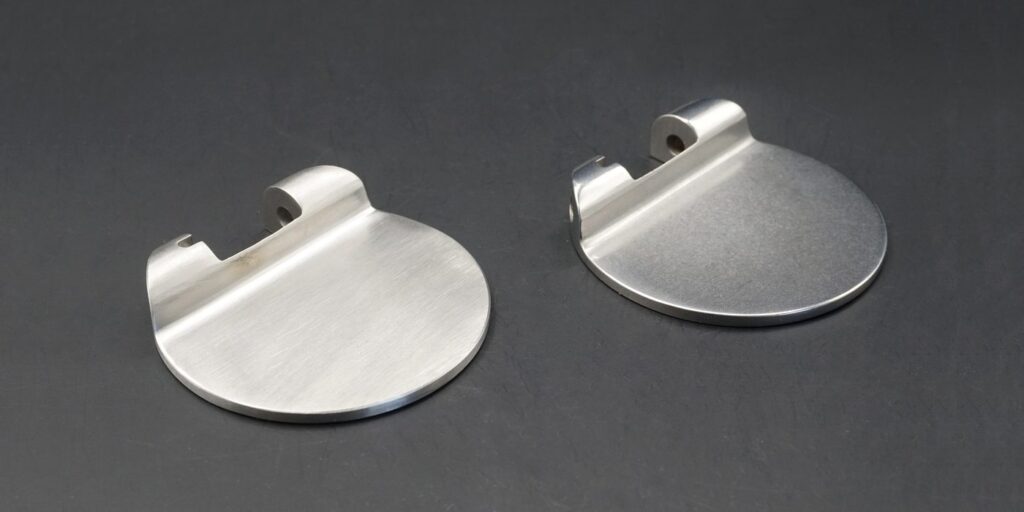
Surgical instruments are the hardest category to finish well with mass finishing, because the two things the process is good at — removing material evenly and reaching into geometry — are the two things that ruin an instrument. A cutting edge that is rounded by a fraction of a millimetre stops cutting cleanly. A hinge that traps compound residue becomes a cleaning problem. This page sets out what to check and what to adjust, feature by feature.
If the instrument is implantable or carries a specific regulatory requirement, that is outside the scope of this page. This page describes finishing directions only.
Three properties make them different from ordinary machined parts:
A working edge is a specification, not a defect. On most parts, a rounded edge is desirable. On scissors, curettes, rongeurs or osteotomes, the edge geometry is the function. Mass finishing removes material from the edge first, because that is where media makes contact. The process does not know the difference between a burr and a cutting edge.
They are usually stainless, and often hardened. Stainless work-hardens. A process that cuts slowly but presses hard can leave a surface that is harder than the base material and harder to polish in the next stage.
They have intimate features that trap media and compound. Hinges, box locks, ratchet teeth, cannulae and fine serrations are places where media lodges and where dried compound survives rinsing.
| Defect | Likely cause | What to check | Recommended adjustment |
|---|---|---|---|
| Cutting edge rounded too much | Cycle time too long, or cutting action too strong for the edge | Edge condition before finishing, media grade, processing time | Shorten the cycle and test a gentler media grade; confirm the edge on a sample part |
| Fine scratches remain | Media too coarse, or tool marks deeper than the finishing stage can reach | Starting roughness, media grade, process sequence | Add a controlled smoothing stage before final polishing rather than lengthening the final stage |
| Debris or grey film remains | Dirty water, unsuitable compound, metal fines, or residue in a hinge | Water clarity, compound concentration, media cleanliness | Improve rinsing, use a compound matched to stainless, and check media for loaded fines |
| Burrs remain in holes, slots or box locks | Media cannot reach the feature | Feature size, slot width, media shape and size | Test a smaller or differently shaped media against the actual geometry before changing anything else |
| Results differ from part to part | Batch load too high, or parts shield each other | Part-to-media ratio, nesting, loading density | Reduce the load and improve media support around each part |
| Surface dulls or discolours after drying | Water spots or compound film | Water quality, rinse sequence, drying method | Separate rinsing from drying, and check whether the drying stage is leaving a film |
> Every row is a direction to test on a representative sample, not a validated recipe. Confirm on the actual part before production.
Surgical instruments usually need two stages, not one — a cutting stage and a finishing stage. Trying to reach the final surface in one operation is the most common reason a batch comes out with either a rounded edge or a scratched surface.
| Requirement | Direction |
|---|---|
| Deburr and radius, with an edge to preserve | A gentle cutting stage, short cycle, media sized to reach the feature without touching the edge first |
| Uniform satin finish across a mixed batch | A barrel or vibratory finishing stage with a light-cutting media |
| Bright finish on stainless with fine detail | A polishing stage with a fine media, after the cutting stage has done its work |
| Small, hard-to-hold parts (screws, pins, clips) | A magnetic finishing process avoids part-on-part contact and reaches small features |
Can surgical scissors be deburred without touching the cutting edge?
Not by mass finishing alone. The edge is typically protected or finished separately, and the mass-finishing stage is scoped to the surfaces that are not the working edge.
What media should be used for stainless surgical parts?
Media is selected from the feature to be reached and the finish required, not from the material alone. Pick the media from the smallest critical feature first, then set the grade from the starting surface condition.
How long should the cycle be?
Cycle time is decided by what the process has to reach, not by a fixed number. It should be established on a sample part and confirmed by inspection, and then held constant.
Can one barrel finish both deburring and polishing?
It is possible in some cases but usually a compromise. Two stages, each with its own media, give more control — especially when an edge has to survive.
What should be in the trial record?
Document the starting condition, media type and size, compound, cycle time, loading, and what was observed on the tested parts. A short written record makes the difference between a repeatable process and a remembered one.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506