
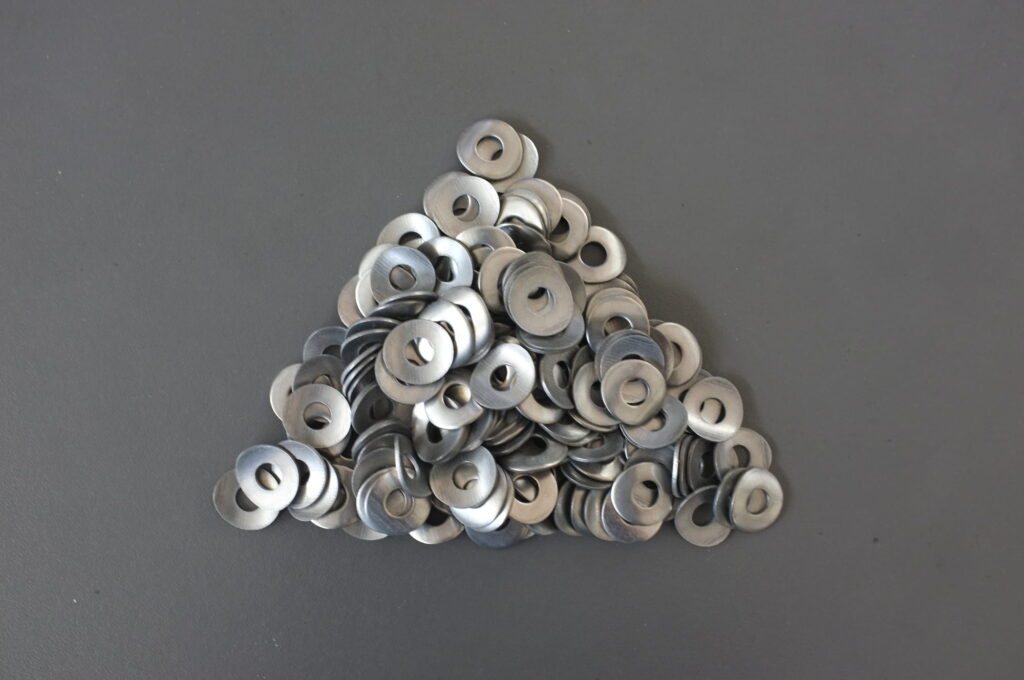
Deburring Tumbler: How to Set Grade, Stock Removal and Cycle Time
A deburring tumbler removes a burr by cutting it off, not by knocking it loose or peening it over. That single fact explains almost every disappointment: a charge that is too fine will round the part for an hour and leave the burr standing, and a charge that is too coarse will take the burr and the edge tolerance together.
So the three decisions that matter are in a fixed order — which cutting grade, how much stock is being removed, and how long the cycle runs — and each of them is set from the drawing rather than from a catalogue. The machine family does not have to be solved first: a bowl, a tub and a rotary barrel all run a deburring cycle — ranges are on the vibratory finishing machines and rotary barrel tumblers. This page is about setting those three, reading the result, and knowing when the process has stopped working. It is a deburring page: if you want brightness rather than burr removal, that is a different process with different media and a different failure mode.
What a finished deburring cycle looks like — and what a failed one looks like
"Deburred" is not a visible property, which is where most process arguments start. Use a comparison instead:
| What you find | What it means |
|---|---|
| Edge is smooth, burr gone, edge radius within tolerance | The cycle did its job — record the grade, size, time and load, and stop changing it |
| Burr gone, edge visibly rounded past the drawing tolerance | Charge too coarse, or run too long for the stock involved |
| Burr still standing after a long cycle, edges over-worked | Charge too fine — it polished the surface while failing to cut the burr |
| Burr gone on some parts in the load but not others | Load or media distribution problem, not a cycle-length problem |
| Media lodged in holes, slots or threads | Sizing problem — the media was wrong for the smallest feature before the cycle started |
| Surface grey and matte, no brightening as the cycle runs | Charge is spent, or compound is not carrying swarf away |
The third row wastes the most production time. A fine charge feels gentler and therefore safer, so it runs for two hours and the part ends up with an over-worked surface and the burr still on. A burr has a thickness; if the media cannot cut at that thickness, time does not fix it — grade does.
Why the grade decides before the time does
The grade is the media's cutting aggressiveness, and we mark it on a six-point scale that is printed on the media specification tables. For wet grinding the grades run VR / R / N / NF / F / FF; for dry grinding they run VR / R / M / MF / F / FF. The two columns do not use the same names — the wet table has no M or MF, the dry table has no N or NF — so a grade letter copied from one table onto the other is meaningless.
| Grade | Meaning | What it is for in a deburring cycle |
|---|---|---|
| VR | Very Rough — maximum stock removal | Heavy casting flash, saw burrs, a gate that has to come off |
| R | Rough — heavy cutting | Standard deburring on robust steel, the first stage of a two-stage job |
| N | Normal — standard processing | General deburring and edge breaking (wet) |
| M | Medium — general finishing | General finishing (dry) |
| NF | Normal Fine — intermediate quality | The stage after deburring, before polishing (wet) |
| MF | Medium Fine — pre-polish | The stage after deburring, before polishing (dry) |
| F | Fine | Fine finishing, edge refinement |
| FF | Fine Finish | Final brightening — a polishing stage, not a deburring one |
Read the table top-down and the logic is visible: VR and R cut, N and M generalise, NF/MF and below refine. If the burr is heavy, you start at the top and step down. If the burr is light and the edge tolerance is tight, starting at the top is how a part gets scrapped.
This is also why the honest answer on any published cycle is the same one we give on the site: a published cycle assumes a material and a removal that may not be yours. A two-stage job — VR/R to take the burr, then a clean change to NF or MF to refine — is more reproducible than one long run at a compromise grade, because the two stages are doing two different jobs.
Size the media before you size the cycle
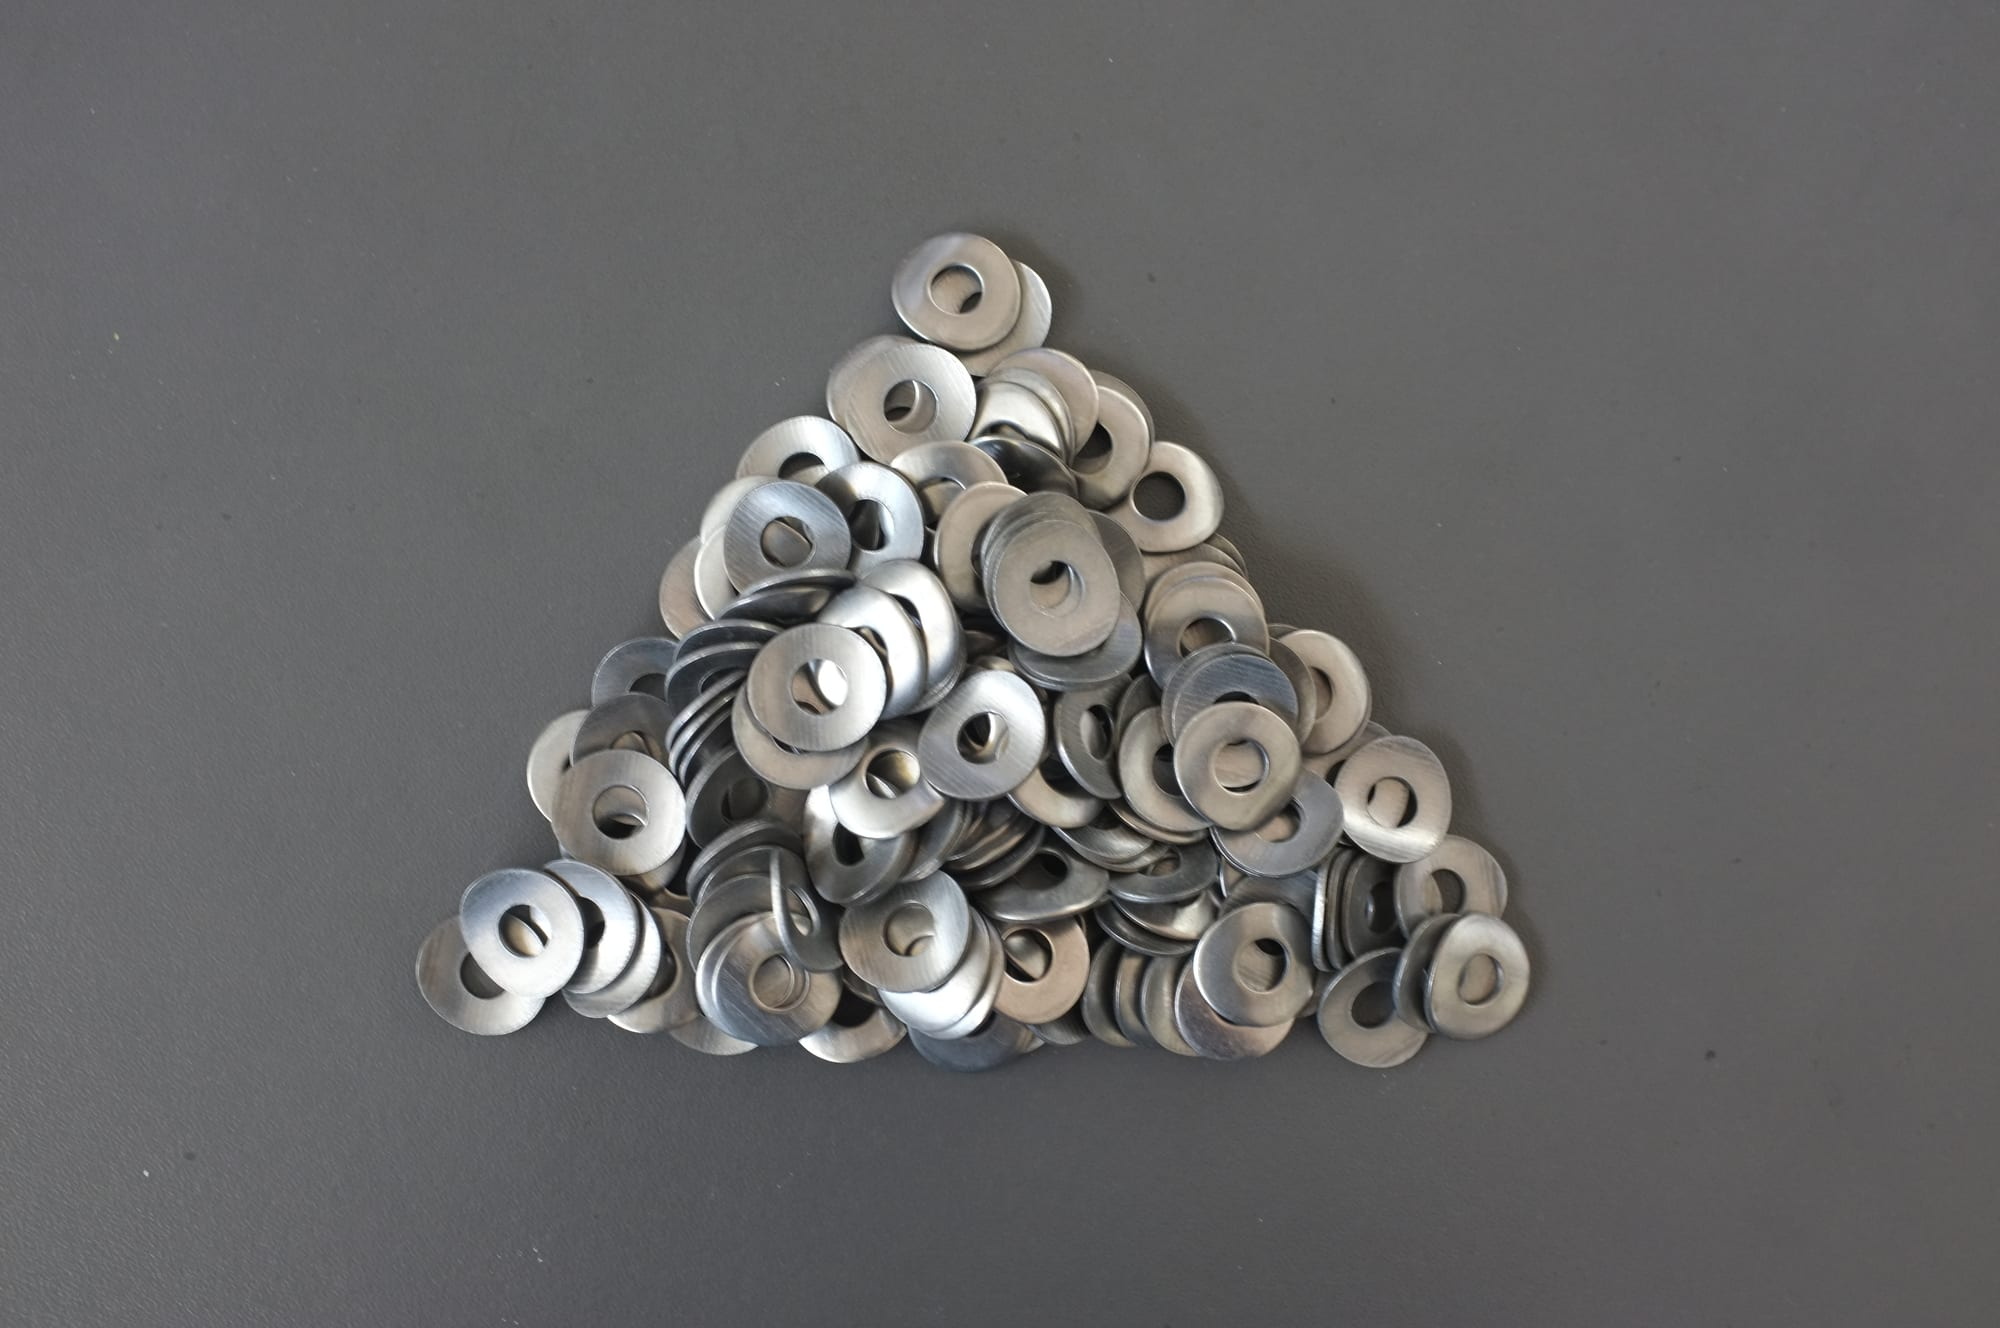
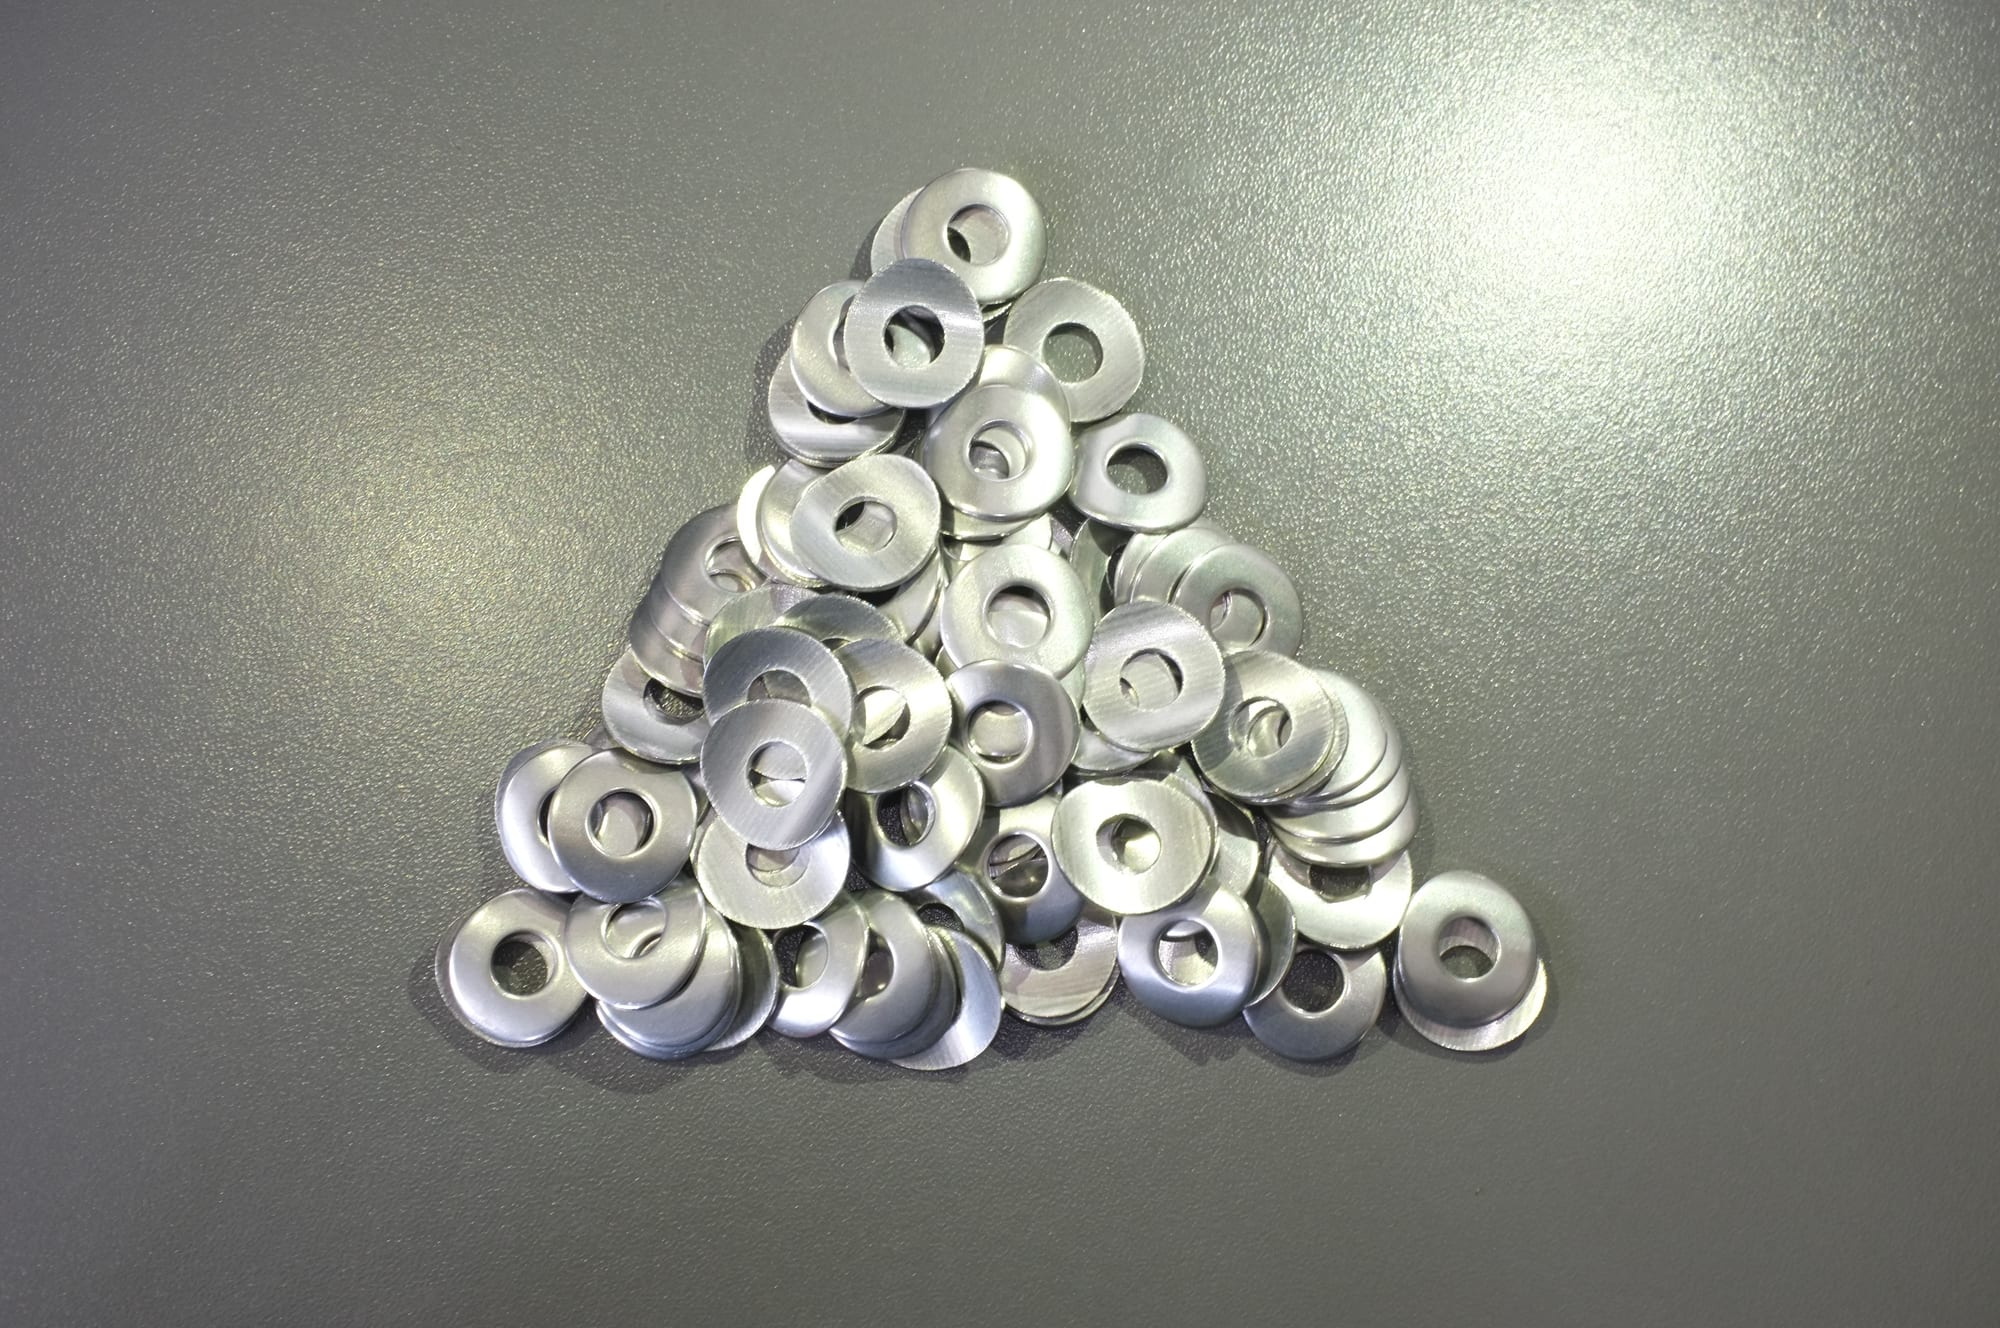
Media must not be larger than about one third of the smallest feature on the part. That is the rule, and it is a physical one rather than a preference.
The consequences are worth spelling out because they are asymmetric:
- A part with a 3 mm blind hole needs media below 3 mm. That means a fine grade, which means a longer cycle, and there is no way around it — the alternative is media wedged in the hole.
- A flat plate with a general edge break can take much larger media and run a much shorter cycle, because the only job is to knock the edges back.
- Media that is too fine is equally wasteful in the other direction: it cuts slowly, and the part tumbles rather than finishes.
A free check before anything is charged: put the part and a sample of the planned media in a bag and shake it. If the media will not enter the features by hand, it will not enter them in the machine either. The full rule and its exceptions are in how to set media size for small holes, slots and internal cavities, and the failure mode is covered in media lodging in holes, slots and threads.
The four things that set the stock removal
"Deburr this part" is not a specification. What the cycle has to remove is set by four things, and they interact:
- Burr thickness at its root, which is a function of the upstream process — a sharp tool and a worn tool leave different burrs on the same part number.
- Burr attachment, meaning how strongly it is held. A loose burr at a drilled cross-hole breaks off early; a rolled-over burr from a dull punch is work-hardened and takes far longer.
- Edge radius tolerance. If the drawing permits a generous radius, one coarse stage will do it. If the radius is held tightly, the same removal has to be taken in finer steps, and the cycle gets longer, not shorter.
- The finish the part leaves with. A deburring cycle changes the whole surface it touches, so a part that has to plate to a consistent appearance is finished to a consistent base rather than to "as clean as possible".
Write all four down before the trial. A trial without a written acceptance criterion only tells you what the parts looked like on the day.
Read the cycle, not the clock
A deburring cycle for light burrs runs 10–20 minutes; a heavy burr or a tight edge-radius control takes longer, and a polish stage after deburring runs 2–8 hours. But the clock is a bad master, and three signals tell you more:
- The finish stops improving. A working charge brightens the part visibly in the first minutes. A spent charge stops changing anything, and the part just tumbles.
- A matte grey haze appears that was not there at the start of the week. That is usually a spent charge, or coarse grit carried into the wrong stage.
- The cycle time creeps up by around 20% for the same result. That is the charge telling you it is done.
Media life runs 20–200 operating hours depending on material and cycle, so the number has to be measured on your job — the fast-cutting ceramic media and plastic deburring media ranges are where the grades above come from. Topping up with fresh media restores the cut, but blending too much new into old makes the charge inconsistent, and a full change at a defined interval is usually more reproducible than continuous top-up. The measurement side — burr height, edge change, roughness — is in how to measure burr height, edge change and Ra after deburring.
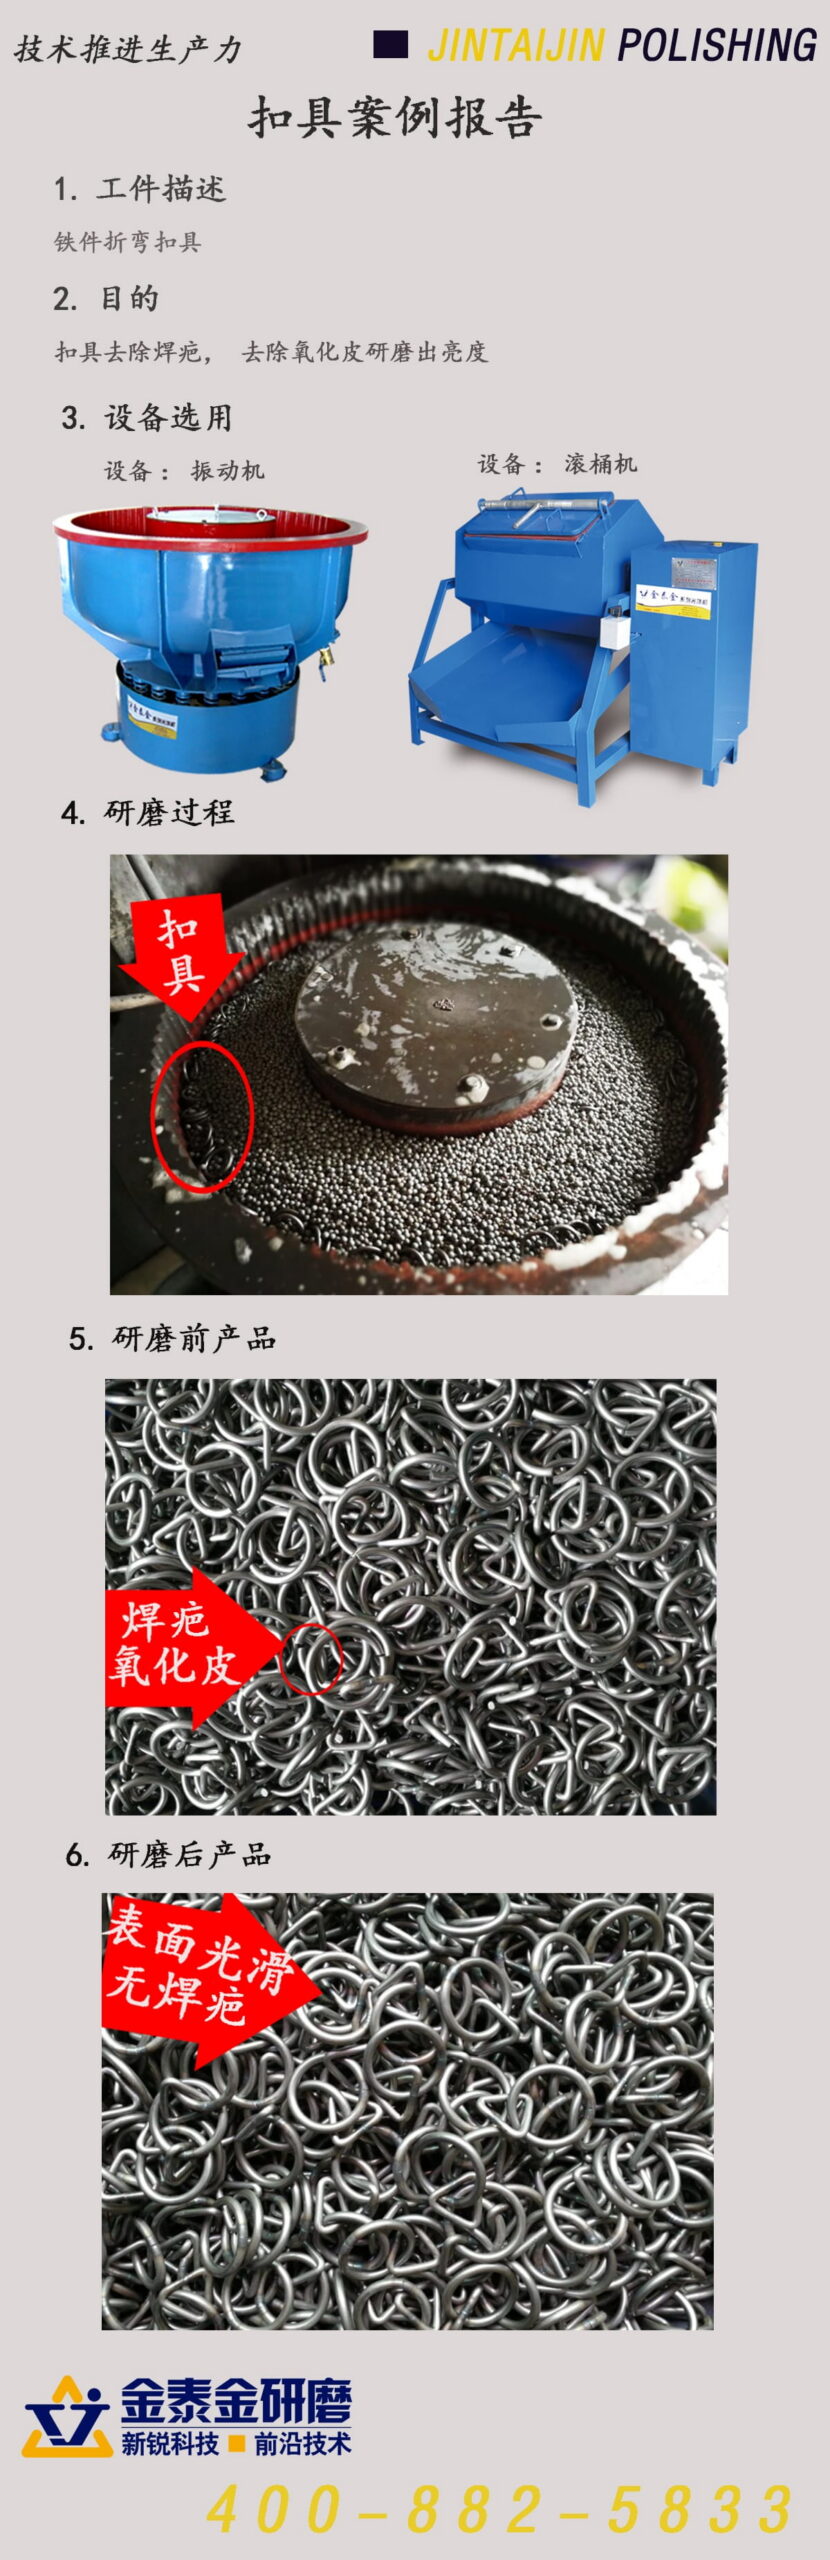
Deburring steel: the rust window is part of the deburring cycle
Deburring a steel part is not finished when the burr is gone. It is finished when the part is dry and stable, and the interval between those two moments — the rust window — is the part of a steel job that gets left out of the quotation.
Why steel is different. A deburred steel surface is freshly exposed metal with no oxide layer, and it is wet from the process. In that condition it starts to corrode within hours, and the corrosion appears first where the water sits: blind holes, thread roots, the gap under a washer face, and cut edges. The part can pass inspection and fail a week later.
What decides how long the window is:
- How wet the part leaves the process. A part that comes out of a wet cycle and sits in a basket is already in the window. A part that goes straight into a centrifugal dryer is not.
- The geometry. Flat parts with open faces dry fast; parts with blind features and threads dry slowly and hold the water exactly where corrosion starts.
- The compound. A compound with a corrosion package extends the window; a plain cutting compound does not. This is a compound decision, not a cycle decision.
- The atmosphere. A humid shop with no air movement closes the window faster than a dry one, and this is not something the finishing process controls.
How to shorten it, in order of cost:
- Separate and rinse immediately at the end of the cycle — not after the batch has been unloaded, counted and left on a pallet.
- Dry in a centrifugal dryer rather than by air or by hand. Air drying leaves a film in blind features that shows up as spotting weeks later; the dryer removes the water rather than waiting for it to leave.
- Choose the compound for the interval it has to survive, and say so when specifying — "how long before the next operation" is a question the compound choice answers.
- Plan the route so the part does not wait. A deburred steel part that spends a weekend in a basket is a part that will be re-finished on Monday.
The check that tells you whether the window is under control: take a finished part from the batch, put it in the worst place in the shop — a humid corner, not the inspection bench — and look at it the next morning. If there is a bloom in a blind feature, the window is too short for that route, and no amount of cycle tuning will change it.
Where a deburring tumbler will not do the job
Be honest about this, because it is where a project goes wrong:
- A burr inside a deep blind slot or a thread root. The media cannot reach it. A flow process with fine media gets shallow features; a deep cross-hole needs magnetic finishing. No amount of cycle time substitutes for contact.
- Thin walls, below roughly 0.5 mm. Distortion is the risk, not the burr. A high-energy machine or a heavy charge bends the part before it improves it.
- A burr that has to be removed with the edge kept sharp. Tumbling cuts everywhere it makes contact, so it radiuses the edge as it removes the burr. If the drawing has an edge-radius maximum of "sharp", this is the wrong process.
- Long slender parts. They bridge in a bowl and stop moving, so the middle gets no contact while the ends get too much.
- Parts that tangle, nest or collide. A free-tumbling charge does not respect part geometry. Part-on-part damage is a loading and separation design problem, not a cycle setting.
- A burr that is a folded flap rather than an attached edge. It tends to get peened over instead of cut off, and it reappears after plating or under load.
- Mixed-material loads. A charge used on steel and then on aluminium carries contamination that shows up as scratches. Dedicate the charge, or clean between jobs.
If your part is on that list, the answer is usually a different route rather than a different grade — a deep cross-hole burr needs magnetic finishing, a sharp-edge requirement needs a different method entirely, and a thin wall needs a lower-energy machine rather than a gentler charge. Reducing manual deburring work covers the cases where the honest answer is still a hand operation for a few features.
What to settle before the order
- A trial on the worst-case part, not the average one. Send representative parts including the one you are worried about, the material, the incoming condition, and both the finish you need and the one you will accept. The result comes back with cycle time and media consumption measured. A batch that looks fine on simple geometry can drop to half the count once a feature traps media.
- A written acceptance criterion. Burr height, edge radius or a visual sample agreed in writing. Without it, the trial cannot fail and therefore cannot pass.
- The grade and size in writing on the order — not just "ceramic media". A size written as "2 to 4 mm" covers a spread that matters on a fine feature.
- Media consumption per batch. With media life at 20–200 hours, consumption is measured on your job; that number, not the machine price, sets your cost per part.
- Separation and cleaning. Media that goes into a feature has to come out. Plan the screen, the separating unit and the drying step before the charge arrives.
- Dates in writing. A standard machine ships in 25–35 days from the deposit; built-to-order takes 45–60 days, and adding a separator or a dryer extends it. Sea freight from Xiamen to Rotterdam or Los Angeles adds 30–40 days. Terms are 30% deposit, balance against the shipping documents, the machine in a wooden case bolted to a pallet, and every machine runs with a charge of media before it ships — an unloaded machine can look perfect and behave differently under load.
On quality: the range is type-examined against Machinery Directive 2006/42/EC by UDEM International Certification Centre against EN ISO 12100 and EN 60204-1, under CE certificates M.2023.206.C88121 (vertical — the vibratory and barrel machines) and M.2023.206.C88120 (horizontal), both valid to 2028-07-24; the quality system is certified to ISO 9001:2015 under certificate 00726Q01571R001, valid 2026-06-03 to 2029-06-02. The company holds 24 granted Chinese intellectual property rights (1 invention patent, 17 utility models, 6 design patents), with twenty-one machine platforms covered by the two type-examination certificates (8 vertical, 13 horizontal, no overlap). Equipment has been built in Xiamen since 1992.
Two operating facts that affect a deburring cell: noise is 75–85 dB(A) at one metre, and the supply is three-phase 380 V or 415 V / 50 Hz, with 220 V available on smaller units. Both should be settled before the order, because both are building changes rather than machine changes.
FAQ
What is a deburring tumbler? A machine that removes burrs by putting parts in a charge of abrasive media and moving the media past them, so the burr is cut off by the abrasive rather than by a tool. Bowl, tub, barrel and centrifugal versions all do this; they differ in how the charge is moved and therefore in what they can reach.
What grade of media should I start with? Start at the coarsest grade the edge tolerance allows and step down. Heavy flash and saw burrs justify VR or R; general deburring sits at N (wet) or M (dry); anything below NF/MF is refining rather than deburring. Starting too coarse and shortening the cycle does not undo a radius that has already been cut.
How long should a deburring cycle run? A light deburr is 10–20 minutes; a heavy burr or a tight edge-radius control takes longer. Pick the time from the trial rather than from a published figure, because a published cycle assumes a material and a removal that may not be yours.
Why is the burr still there after a long cycle? Two usual causes, and they need opposite fixes. Either the charge is too fine to cut at the burr's thickness — go coarser, do not run longer — or the charge is spent and no longer cutting, in which case top up or replace it. A third cause is that the burr is in a feature the media never reaches, which no grade fixes.
Can a deburring tumbler also polish? It can run a polishing stage afterwards, but not in the same charge. Polishing wants finer media, a different compound and a longer cycle; running both in one charge means one of the two is done badly, and the usual symptom is the grey haze that gets blamed on the compound.
 +86-592-2381506


 IPv6 network supported
