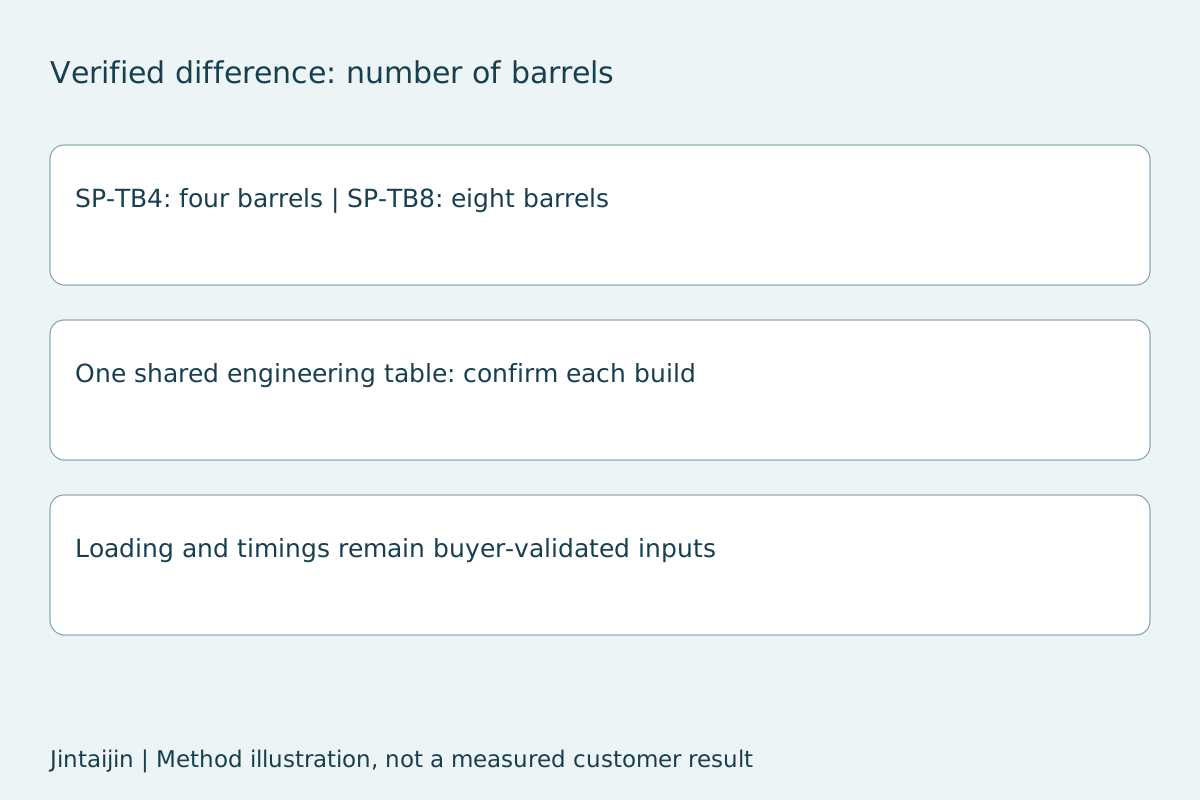
Compare the model-specific barrel counts published for SP-TB4 and SP-TB8. Enter the same validated loading and timing assumptions for each barrel to calculate complete processed batches in your available time. This isolates a layout difference without treating a shared specification table as a model-by-model performance guarantee.
Enter your recorded values, then calculate.
The current SP-TB manual identifies SP-TB4 as four barrels and SP-TB8 as eight, arranged across two tiers. It gives one shared engineering table rather than separate model columns. The shared table’s motor and electrical wording therefore remains a configuration reference requiring model-specific confirmation; it is not used to calculate energy or certify a supplied build.
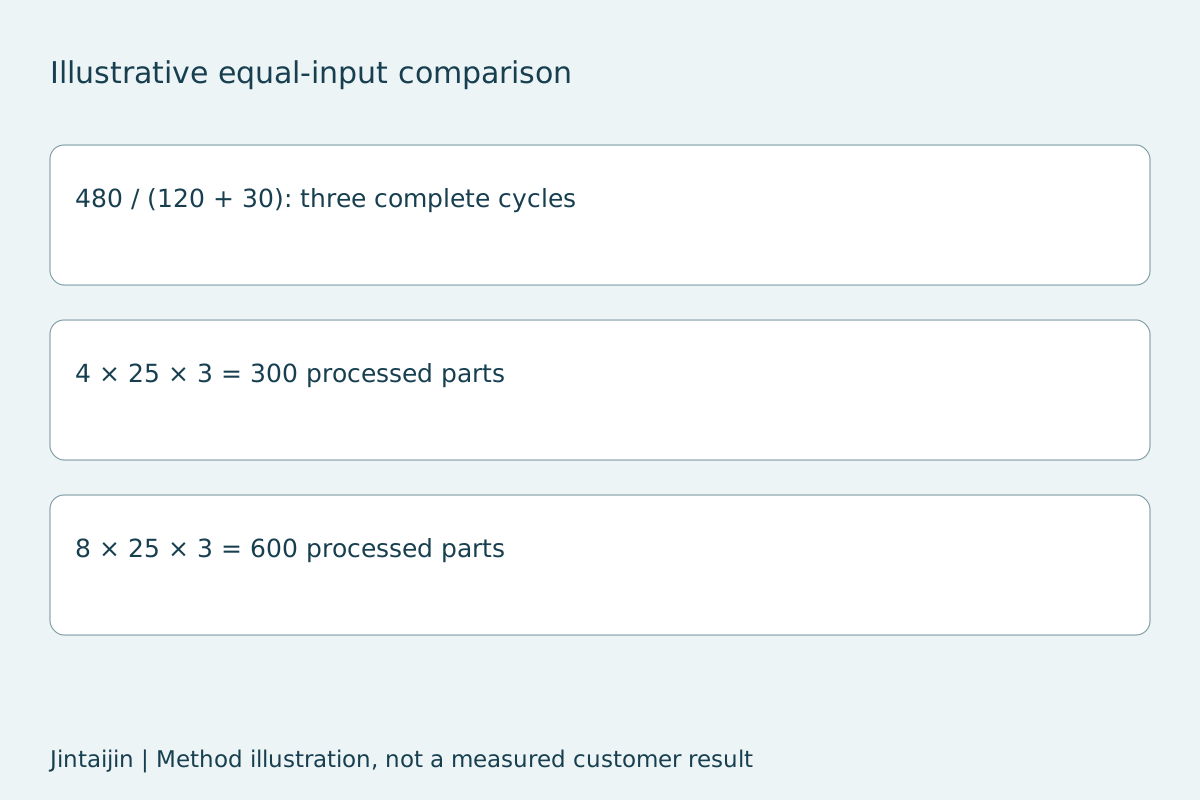
Complete cycles are the integer floor of available minutes divided by processing plus non-overlapped handling minutes. Multiply that count by your validated part count per barrel and by four or eight. This model assumes all barrels can complete the same cycle concurrently. It excludes acceptance loss and does not infer part loading from exterior dimensions or nominal volume.
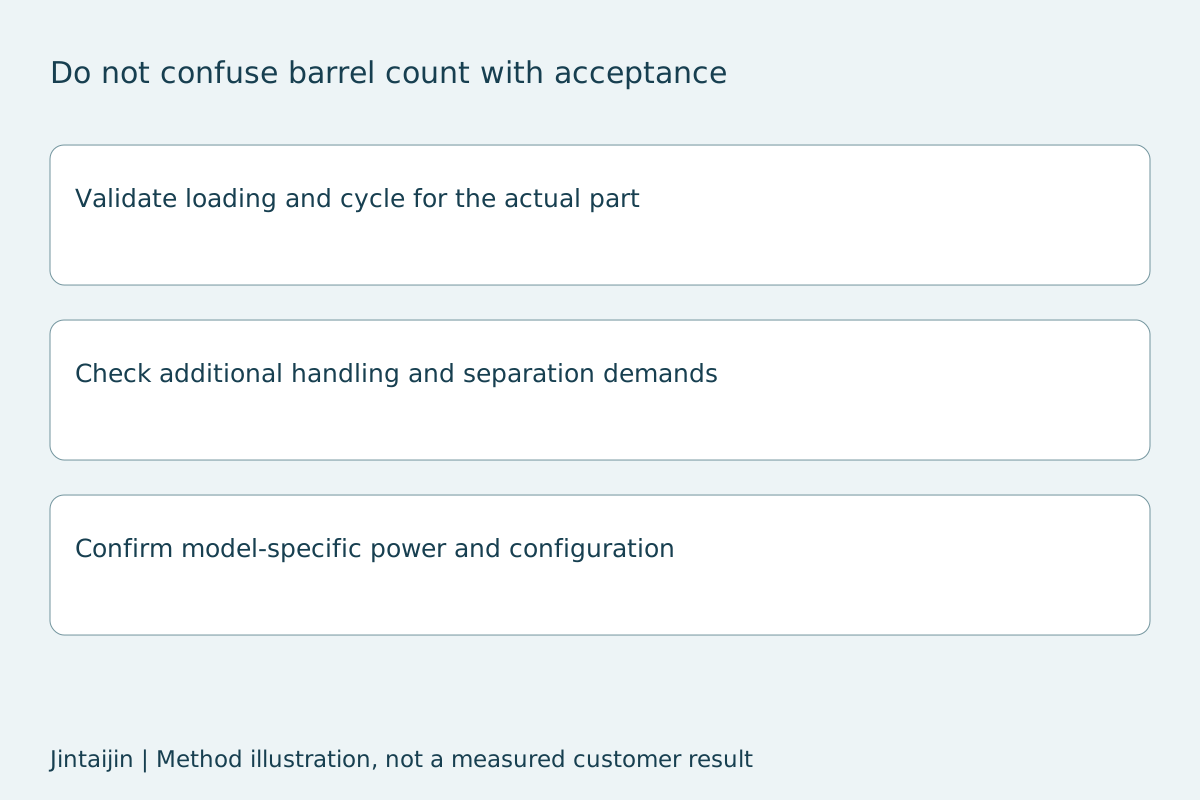
Include loading, discharge and any separation interval that prevents the next cycle from starting. If eight barrels require more handling time than four, the equal-time comparison becomes unsuitable. Run each actual model with its separately measured timings outside this equal-input worksheet, or request a production review. Extra barrels do not remove labor, screening or receiving constraints.
Use parts per barrel and processing time established for the part material, geometry, media, compound and finish target. The published operating guide is context, not evidence that every eyewear frame or hardware part accepts the same recipe. Confirm motor, supply, barrel dimensions, permitted loading and guarding for the actual ordered configuration.
An example of 25 validated pieces per barrel, 120 processing minutes and 30 handling minutes fits three complete cycles into 480 available minutes. The equal-input count is 300 processed pieces for four barrels and 600 for eight. The remaining 30 minutes do not form another completed cycle. This is a count comparison, not evidence of doubled accepted output.
Open the enquiry form with this tool reference. Calculations stay in this page and do not send an enquiry.
Context source checked 3 October 2026: Jintaijin technical guidance. The displayed method uses your inputs; no processing outcome is predicted.
Email : info@surface-polish.com


 IPv6 network supported


 +86-592-2381506
