• Centrifugal Disc vs Centrifugal Barrel Finishing: Which High-Energy Machine Fits Your Parts?
    Centrifugal Disc vs Centrifugal Barrel Finishing: Which High-Energy Machine Fits Your Parts? Aug 26 , 2026
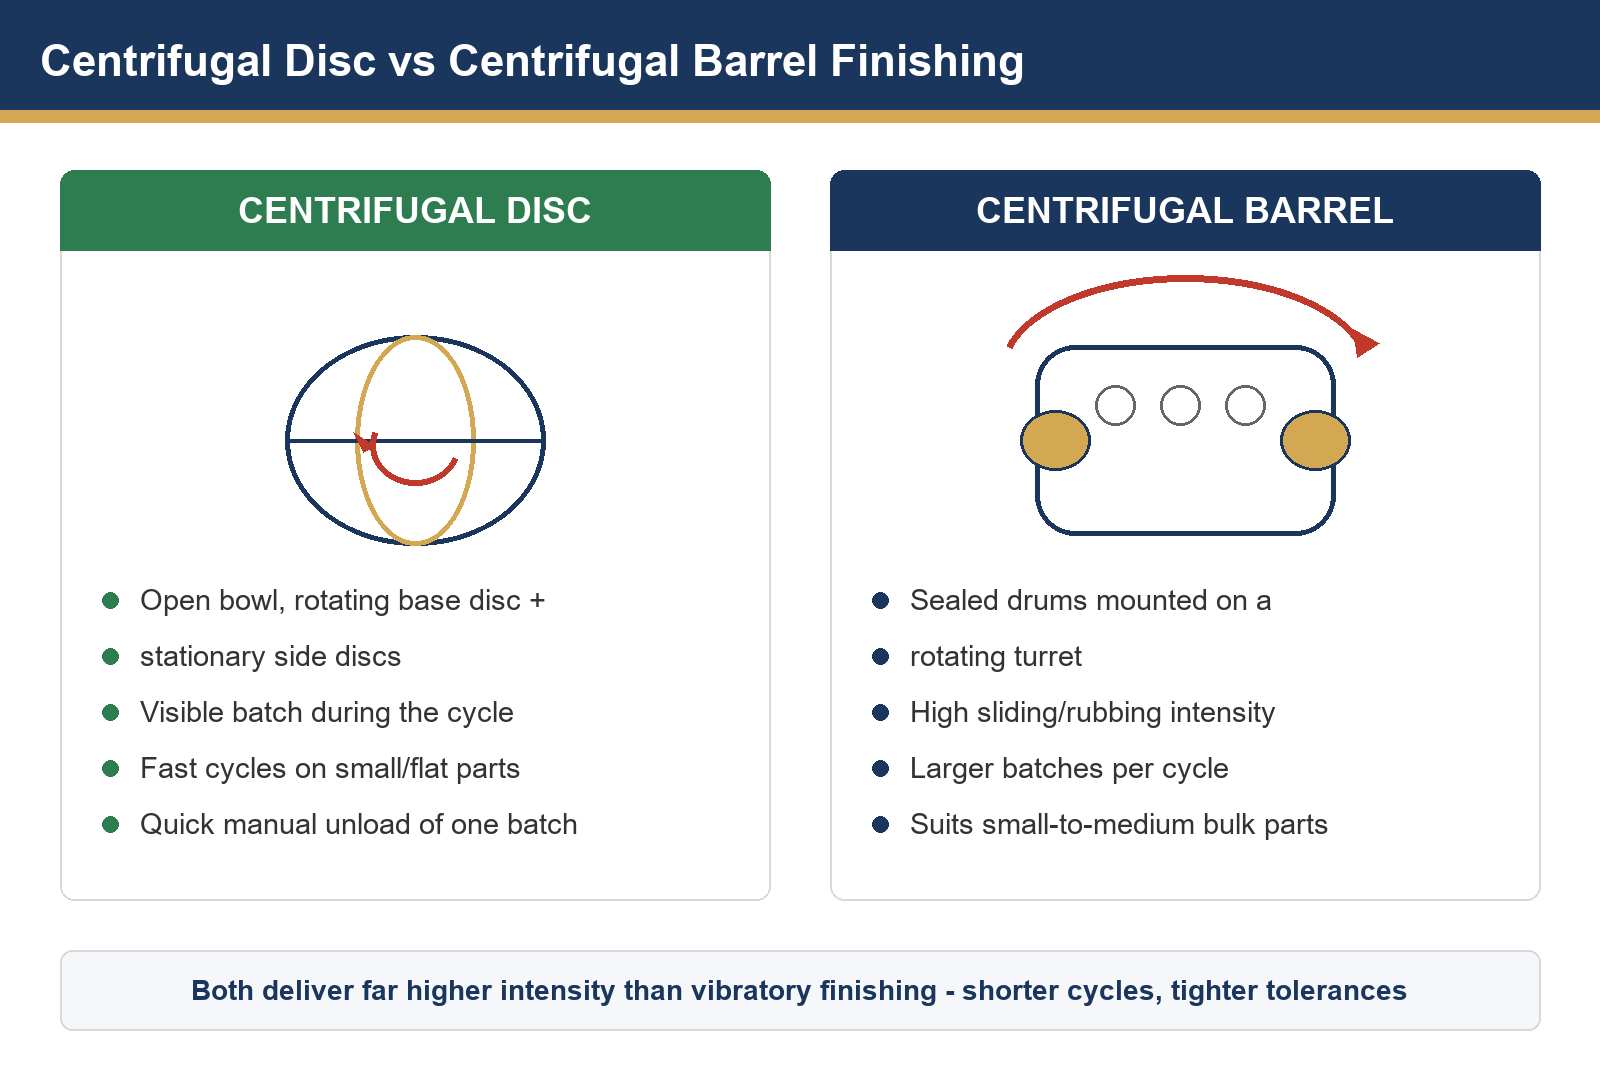
    Centrifugal Disc vs Centrifugal Barrel Finishing: Which High-Energy Machine Fits Your Parts? High-energy mass finishing comparison • Centrifugal disc & centrifugal barrel • Machine selection guide When vibratory finishing is too slow or too gentle for the result you need, the next step up in intensity is a centrifugal disc or a centrifugal barrel machine. Both multiply the effective force between media and parts, cutting cycle times dramatically on small, hard-to-finish components. But they reach that intensity in different ways — and that difference decides which machine suits your parts, batch sizes, and floor space. Working principles: open centrifugal disc bowl (left) vs sealed centrifugal barrel drums on a rotating turret (right) In one sentence. Centrifugal disc = fastest cycles with the batch always visible and easy to check; centrifugal barrel = the most intense sliding action with larger sealed batches. Both are the tools of choice when vibratory bowls would take hours to reach the same result. 1. Why High-Energy Finishing Exists Vibratory finishing is gentle and forgiving, but its abrasive action is limited by low contact pressure. Small or hard parts — fasteners, watch components, medical screws, precision gears, jewelry castings — often need far more rubbing energy to deburr, smooth, or pre-polish in a commercially acceptable time. Centrifugal machines solve this by spinning the process mass so that media presses against parts at many times the force gravity alone can provide, multiplying the rate of surface refinement while keeping the process controllable and repeatable. 2. How a Centrifugal Disc Machine Works A centrifugal disc machine is an open bowl with a powerful rotating disc at its base and stationary side discs or ribs. The base disc spins at high speed, setting media and parts into a toroidal (ring-shaped) rolling motion; the stationary sides force constant speed differences, so every part is continuously rubbed from all directions. Because the bowl is open, the operator can watch the batch, open the lid mid-cycle, and take out sample parts in seconds. Unloading is typically a tilt of the bowl or a bottom discharge door, followed by media separation on a screening tray. Centrifugal disc (vortex) machine principle: 1 fixed bowl, 2 rotary disc, 3 media and parts 3. How a Centrifugal Barrel Machine Works A centrifugal barrel machine mounts several sealed drums onto a rotating turret. As the turret spins, each drum also rotates on its own axis, so media and parts are held against the drum wall by centrifugal force and then continuously slide down the rising “shoulder” of the charge. This produces the most intense sliding/rubbing action of any batch mass-finishing process. The drums are sealed, so the process is quiet and clean; between cycles the drums swing out for loading, and finished batches are discharged through drum doors onto a separator. Centrifugal barrel finishing machine — drums open for loading 4. Side-by-Side Comparison Feature Centrifugal Disc Centrifugal Barrel Working principle Open bowl, spinning base disc + stationary side discs Sealed drums on a rotating turret (planetary motion) Batch visibility Fully visible; samples removable mid-cycle Sealed — check only at cycle end Action character Rolling toroidal flow; aggressive but controllable Maximum sliding/rubbing intensity Batch size Small to medium Medium to larger (sum of all drums) Unloading Bowl tilt or bottom door, quick manual discharge Drum doors discharge onto separator Typical parts Small flat/short parts: fasteners, stampings, jewelry, watch parts Small-to-medium bulk parts: gears, machined blanks, castings Process control Speed adjustable; visual process monitoring Turret and drum speeds adjustable; fully enclosed 5. Which Parts Fit Which Machine Choose centrifugal disc when: you need the shortest possible cycles on small parts, want to inspect or sample the batch during the run, or change part types frequently. Ideal for jewelry, watch cases, small stampings, and electronics hardware. Choose centrifugal barrel when: you need maximum smoothing or pre-polish intensity on robust small-to-medium parts in larger batches — machined blanks, forged or cast components, dental and medical implants (with validated processes), and cutting-tool blanks. Stay with vibratory when: parts are larger, fragile, or decorative surfaces must not mark each other — see our guide on choosing ceramic vs plastic media for gentler options. 6. Media and Compound Notes High-energy machines demand media that can take the extra force: precision-fired ceramic for aggressive cutting, plastic-bonded media for softer metals, and steel media where burnishing without material removal is the goal. Compound dosing is typically continuous or metered rather than batch-charged. Because contact pressure is much higher than in vibratory work, always run a dimension check on a sample batch before production — aggressive processes can move tolerances on thin or delicate features. 7. Selection Checklist and Next Step Define the objective: deburr, edge radius, surface refine, or pre-polish — and the target roughness if specified. Measure the part: smallest feature, thinnest section, and whether parts can touch each other. Size the batch: daily throughput decides whether a disc machine’s fast small batches or a barrel machine’s larger sealed batches fit better. Run a sample trial: send parts for a timed trial on both machine types and compare finish, cycle time, and dimensional change before buying. Browse our centrifugal disc finishing machines and centrifugal barrel finishing machines, or view the full finishing machine collection to compare all options. Disc or barrel? Let your parts decide. Send sample parts and your finish target. Our team will run comparative trials and recommend the machine, media, and cycle with real results. Contact Our Finishing Team Official website: www.surface-polish.com  |  Support email: info@surface-polish.com
  • Walnut Shell vs Corncob: How to Choose Dry Tumbling Media for Eyewear, Jewelry & Hardware
    Walnut Shell vs Corncob: How to Choose Dry Tumbling Media for Eyewear, Jewelry & Hardware Aug 26 , 2026
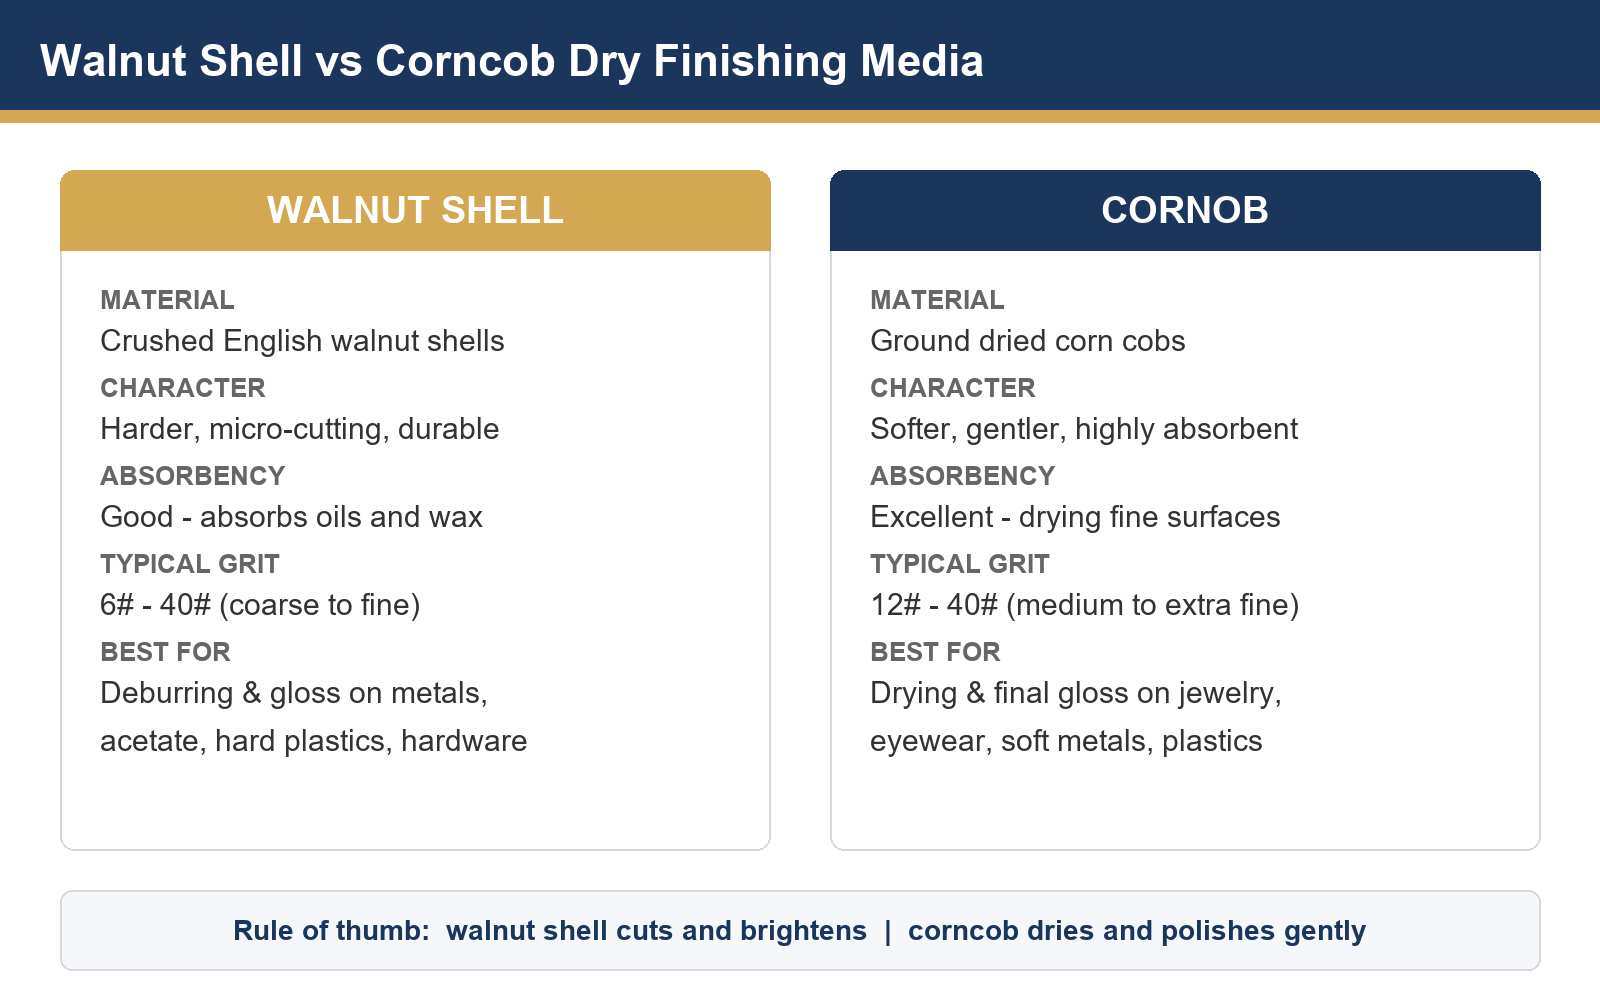
    Walnut Shell vs Corncob: How to Choose Dry Tumbling Media for Eyewear, Jewelry & Hardware Dry finishing media selection guide • Walnut shell & corncob • For dry tumbling, vibratory and centrifugal lines Dry organic media — crushed walnut shell and ground corncob — is the workhorse of dry tumbling and dry vibratory finishing. The two materials look similar in the bag, but they behave very differently in the bowl. Choosing the wrong one usually shows up as dull surfaces, stuck-on compound, or parts that are clean but not bright. This guide explains what each media does, how they compare, and how to pick the right grade for eyewear, jewelry, and precision hardware. Walnut shell vs corncob: material character, absorbency, grit ranges and typical applications Rule of thumb. Walnut shell cuts and brightens — use it when you need to remove marks, light oxides, or burrs while building gloss. Corncob dries and polishes gently — use it to absorb oils and polishing compound while producing a soft, streak-free luster on delicate parts. 1. What Dry Media Actually Does In a dry process there is no water or chemical solution doing the work. The media itself performs three jobs at once: it abrades (removing burrs, tool marks, and light tarnish), it carries compound (holding polishing wax against the workpiece), and it absorbs (soaking up oils, fingerprints, and spent compound so parts come out clean and dry). How aggressively a media abrades — and how well it absorbs — is exactly where walnut shell and corncob differ. 2. Walnut Shell Media: Character and Best Uses Walnut shell is crushed hard shell, typically from English walnuts. It is noticeably harder and sharper at the particle level than corncob, which makes it a light-cutting media rather than a pure polishing media. Walnut shell dry finishing media — hard, micro-cutting granules Light cutting action: removes light burrs, parting lines, tarnish, and heat-tint discoloration on metals and hard plastics. Gloss building: on brass, aluminum, zinc, and acetate it develops a bright, uniform sheen over 2–8 hour cycles as a typical starting range. Durable and reusable: holds its structure longer than corncob, so it suits longer production runs before replacement. Typical grades: coarse grits (6#–20#) for cleaning and deburring; finer grits (24#–40#) for smoothing and pre-polish. 3. Corncob Media: Character and Best Uses Corncob is the ground core of dried corn cobs — a soft, highly porous organic media. It cuts very little; its strengths are absorption and a gentle, burnishing polish. Corncob dry finishing media — soft, highly absorbent granules Gentle polishing: smooths micro-roughness and raises a soft luster without rounding edges or marking threads. Excellent absorbency: soaks up polishing wax, oils, and water — the standard choice for the final drying-and-gloss stage after wet finishing. Safe on delicate parts: the go-to media for jewelry, watch components, acetate eyewear, and painted or plated surfaces. Typical grades: medium (12#–20#) for general drying and polish; extra fine (30#–40#) for mirror-stage work on soft materials. 4. Side-by-Side Comparison Property Walnut Shell Corncob Cutting action Light to moderate — removes marks and tarnish Minimal — burnishing and smoothing only Absorbency Good Excellent Surface effect Bright, clean, slightly satin-to-gloss Soft, deep, streak-free luster Edge condition Lightly softened Preserved Media life Longer — resists breakdown Shorter — dusty as it wears Typical grit range 6# – 40# 12# – 40# Best applications Hardware, brass/aluminum parts, acetate frames, deburr + gloss Jewelry, watch parts, eyewear final gloss, drying after wet work 5. Pairing Media, Compound and Machine Both media carry polishing compound far better than they carry it dry — add wax or dry polishing cream in small, regular doses rather than one large charge. In rotary barrel tumbling, walnut shell at 50%–60% barrel fill is the usual starting point for cut-and-gloss stages, while corncob excels in the final gloss stage. For a worked example of stage-by-stage recipes, see our bamboo tumbling machine operation guide, and browse our full dry finishing media and finishing compounds ranges. 6. Selection Checklist by Application Acetate eyewear frames: walnut shell (24#–36#) with polishing wax to remove tool marks, then corncob (30#–40#) for the final gloss. Jewelry and watch parts: corncob extra fine with a touch of luster compound; avoid coarse walnut on delicate clasps and pins. Brass / aluminum hardware: walnut shell (12#–20#) to clear tarnish and burrs; corncob afterward if a softer cosmetic gloss is wanted. Threaded or tolerance-critical parts: corncob only, or walnut at fine grades and short cycles — check dimensions after the first trial run. Drying after wet vibratory finishing: corncob, always — its absorbency outperforms walnut for water and emulsion removal. 7. Run a Simple Media Trial Before Committing Media choice is ultimately empirical. Run a 2–4 hour trial with a marked sample batch: weigh the parts before and after, photograph surfaces under the same light, and check critical dimensions. If the surface is clean but not bright, move from corncob toward walnut (or add compound). If edges are rounding or dimensions are drifting, move toward corncob or a finer grade. Our rotary barrel tumbling machines work with both media families, and our team can recommend a starting recipe for your material and finish target. Not sure which media suits your parts? Send your part material, size, current surface condition, and target finish. Our finishing team will recommend the media grade, compound, and cycle to test first. Contact Our Finishing Team Official website: www.surface-polish.com  |  Support email: info@surface-polish.com
  • Single-Station Eco Manual Polishing Machine: Operation Manual, Maintenance Schedule & Finishing Recipes
    Single-Station Eco Manual Polishing Machine: Operation Manual, Maintenance Schedule & Finishing Recipes Aug 19 , 2026
    Single-Station Eco Manual Polishing Machine: Operation Manual, Maintenance Schedule & Finishing Recipes Model Series: SPM-ECO-1000 • Eco-Friendly Dust-Controlled Buffing Workstation • Optical & Hardware Edition The JINTAIJIN SPM-ECO-1000 single-station eco manual polishing machine is an eco-friendly precision buffing workstation engineered for high-gloss finishing of cellulose acetate eyewear, optical parts, jewelry, watch cases, and fine hardware. A 1.5 kW stepless VFD spindle (0–3,600 RPM), high-velocity negative-pressure dust extraction (1,200–1,500 m³/h), 5–10 µm multi-pocket polyester filtration, and a 15 L slide-out recovery drawer deliver superior surface gloss with zero airborne dust. This manual covers product specifications, mechanical architecture, essential safety regulations, installation and pre-commissioning, the full standard operating procedure (SOP), dust filtration and shaker operation, preventive maintenance, troubleshooting, and factory spare parts. If you are comparing equipment options first, review our finishing machine collection or the wider grinding & finishing machine range. MSDS Download (English, original document). Material Safety Data Sheet for JINTAIJIN resin abrasive polishing media — provided exactly as issued, unmodified. Download MSDS (EN) — PDF Equipment overview & capability. The SPM-ECO-1000 integrates high-torque buffing spindle mechanics with a self-contained dust extraction blower and high-efficiency filtration matrix for industrial surface polishing. Featuring a stepless VFD spindle, negative-pressure suction hood, mechanical dust shaker lever, and a sealed 15-liter recovery drawer, it suits acetate/propionate eyewear frames, optical parts, jewelry, watch cases, and fine hardware finishing. 1. Technical Parameters & Specifications The table below lists the standard engineering configuration of the SPM-ECO-1000 single-station eco manual polishing machine. Technical Parameter Engineering Value / Range Specification Notes Spindle Motor Power 1.5 kW / 2.0 HP (Continuous Duty S1) High-Torque Induction Motor with VFD Inverter Spindle Speed Range 0 – 3,600 RPM (Stepless Regulated) Digital RPM Display & Precision Potentiometer Dial Dust Extraction Blower 0.75 kW (High-Pressure Backward Centrifugal) Airflow Rate: 1,200 – 1,500 m³/h (700 – 880 CFM) Inlet Suction Velocity ≥ 18.0 m/s at Extraction Throat Direct Particle Pull with Zero Ambient Leakage Filtration Rating & Media 5 – 10 µm Needle-Punched Polyester Fabric ≥ 98.5% Dust Separation Rating (Multi-Pocket Array) Dust Collection Capacity 15 Liters Slide-Out Steel Drawer Dual Quick-Release Toggle Clamps & EPDM Seal Buffing Wheel Range Ø150 mm – Ø250 mm (6" – 10" Diameter) Core Arbor Bore: Ø16 mm or Ø25 mm Spindle Shaft Specification Precision Solid Alloy Steel Ø25 mm M16 Left-Hand Reverse Thread; Runout ≤ 0.02 mm Workstation Lighting 24W Shadowless Industrial LED Bar Illuminance ≥ 1,200 Lux at Tabletop Working Plane Power Supply & Voltage 220V 1-Phase / 380V 3-Phase, 50/60 Hz Chassis Grounding Resistance strictly < 4.0 Ω Acoustic Noise Rating ≤ 72 dB(A) at 1.0 m operator distance Compliant with ISO 11202 & OSHA 1910.95 Machine Dimensions / Weight 850 × 750 × 1,350 mm (L×W×H) | 115 kg Heavy-Duty Welded Frame + 4 Leveling Footpads 2. Mechanical Architecture & Subsystem Identification The machine integrates a buffing spindle, negative-pressure extraction, multi-pocket filtration, and a sealed recovery drawer into one dust-controlled workstation. The diagram below identifies all primary structural components and their exact English technical terms. Figure 1: Overall System Architecture, Structural Layout, and Key Component Identification 2.1 Core Subsystem Breakdown # Component Functional Description & Operational Role 1 Precision Spindle Arbor Solid Ø25mm alloy shaft with M16 reverse-thread nut and clamping flanges. 2 Aerodynamic Suction Hood Wide negative-pressure intake hood pulling dust directly behind the wheel. 3 Dust Recovery Drawer 15-liter slide-out steel bin with dual quick-release airtight toggle latches. 4 Multi-Pocket Filter Chamber Houses 4 polyester cloth filter bags (5–10µm) with ≥98.5% separation rating. 5 Polycarbonate Safety Visor Hinged, high-impact transparent shield protecting operator from flying swarf. 6 24W Shadowless LED Lamp Daylight-spectrum LED bar illuminating the polishing contact plane (≥1200 Lux). 7 Control Console Front panel with E-Stop, Power/Suction/Light switches, and VFD RPM dial. 8 Leveling Footpads Four adjustable heavy-duty rubber-cushioned M16 anti-vibration feet. 9 Dust Shaker Lever External side lever linked to internal grid to dislodge filter cake into the drawer. Figure 2: Detail Zoom 1 — Precision Polishing Spindle, Bearing Housing, Flange Clamping, and Reverse-Thread Locking Nut Figure 3: Detail Zoom 2 — Single-Port Aerodynamic Extraction Hood, Dual-Vortex Airflow, and Particle Capture Dynamics Figure 4: Detail Zoom 3 — Multi-Pocket Fabric Filter Matrix, Mechanical Shaker Agitation Grid, and Slide-Out Recovery Drawer Figure 5: Detail Zoom 4 — Industrial Operator Control Console, Electrical Switches, VFD Speed Regulator, and Emergency Stop Interface 3. Essential Safety Regulations & Hazard Controls DANGER — severe mechanical entanglement hazard: NO GLOVES. STRICT PROHIBITION OF GLOVES: NEVER wear gloves (cotton, leather, rubber, or nitrile), loose clothing, neckties, rings, or wrist jewelry during polishing spindle operation. The high-speed rotating spindle and cotton buff will instantly grab textile fibers and drag the operator’s hands into the arbor within milliseconds. Long hair MUST be securely bound in a protective cap. 3.1 Mandatory Personal Protective Equipment (PPE) Eye & Face Protection: ANSI Z87.1 / EN 166 Grade B certified safety goggles or face shield. Respiratory Protection: NIOSH N95 or EN 149 FFP2 particulate respirator for fine dust. Hearing Protection: Industrial earplugs or earmuffs (NRR ≥ 22 dB) during extended shifts. Apparel & Footwear: Snug workwear with elastic cuffs; steel-toe anti-slip safety shoes. 3.2 Combustible Dust & Static Grounding Protocols Grounding: Cellulose acetate, acrylic, and polishing wax generate combustible fine dust. Ensure chassis grounding resistance is strictly < 4.0 Ω to dissipate static charge buildup. Spark Control: NEVER polish spark-producing ferrous metals (steel/iron) without prior complete cleanout of the filtration chamber and dust drawer. 4. Installation & Pre-Commissioning 1. Leveling. Place machine on a level concrete floor. Adjust 4 leveling footpads until the tabletop is level in all axes, then lock jam nuts. 2. Electrical. Connect to dedicated branch circuit (16A breaker for 220V 1-Phase; 10A breaker for 380V 3-Phase). Secure PE ground wire (<4Ω). 3. Rotation. Buffing wheel MUST rotate clockwise downward toward operator. If rotation is reversed on 3-phase units, swap incoming lines L1 and L2. 4. Wheel Mounting. Slide inner flange onto shaft → Mount wheel → Slide outer flange → Hand-thread M16 reverse nut → Tighten firmly with spanner (45–50 N·m). 5. Standard Operating Procedures (SOP) & Finishing Follow this streamlined 4-stage workflow to guarantee repeatable, mirror-grade finishing and ensure maximum operator safety. Figure 6: Standard Operating Procedure (SOP) 4-Stage Operational Workflow & Recommended 4:00 – 6:00 Safe Wheel Contact Arc 5.1 Daily Startup Sequence 1. Power. Turn ON Main Power isolator switch (green indicator illuminates). 2. Suction. Press DUST SUCTION button and verify strong negative air draw at the hood throat. 3. Lighting. Turn ON LED Work Light switch to illuminate the contact plane. 4. Spindle. Press SPINDLE START and dial VFD speed potentiometer to target RPM (2,000–2,400 RPM for acetate; 3,000 RPM for metal). 5.2 Workpiece Contact Arc & Kickback Prevention WARNING — kickback danger & safe contact zone. MANDATORY CONTACT ZONE (4:00 TO 6:00 ARC): Always present the workpiece against the LOWER QUADRANT of the wheel (between 4:00 and 6:00). NEVER polish above the centerline (12:00 to 2:00 zone) — the wheel will violently snatch and throw the workpiece forward (kickback hazard). Maintain light, steady, tangential pressure. 5.3 Eyewear & Precision Hardware 3-Stage Finishing Protocol Process Stage Recommended Wheel Compound Speed Surface Objective Stage 1 (Coarse Cut & Deburr) Spiral cotton / sisal wheel Brown Tripoli compound 2,200–2,400 RPM Removes CNC milling tool marks and burrs. Stage 2 (Smooth & Level) Yellow treated cotton wheel Green Chromium Oxide compound 2,000–2,200 RPM Buffs frame bevels and bridge into a smooth satin finish. Stage 3 (Mirror Finish) Soft unstitched muslin wheel Blue Luster or White Diamond wax 1,800–2,000 RPM Polish with light touch for optical mirror gloss. Compound tip — dedicated wheels per stage. Always use a dedicated buffing wheel per compound grade. A wheel contaminated with coarse Tripoli will transfer swirl marks into the final mirror stage. Rake wheels clean between batches. 5.4 End-of-Shift Shutdown Routine Stop spindle → Run suction for 30s to purge ductwork → Turn OFF suction, light, and power → Pump dust shaker lever 6–8 times into drawer. 6. Dust Filtration, Shaker Operation & Recovery 1. Recovery Drawer — empty daily. Turn OFF machine. Release dual quick-latches, slide 15L drawer out, empty swarf into waste/recycling bin, wipe EPDM gasket clean, and clamp latches airtight. 2. Shaker Agitation — every 4 hours. With suction fan completely OFF, grasp external side shaker lever and pump vigorously 6–10 times. Internal grid shakes caked dust down into the drawer. 3. Swarf Recovery — precious metal reclamation. The sealed collection drawer enables 100% dry reclamation of gold, silver, brass, and titanium polishing swarf without slurry contamination. 7. Preventive Maintenance & Troubleshooting 7.1 Preventive Maintenance Schedule Maintenance Frequency Mandatory Inspection & Service Procedures Daily (Every Shift) Empty 15L recovery drawer; clean PC visor; pump filter shaker 6–8 times; check wheel wear. Weekly (40 Hours) Inspect spindle arbor runout; check drive belt tension; inspect EPDM drawer gasket seal. Monthly (160 Hours) Inspect filter bags for tears or caking; verify ground bond (<4.0 Ω); check electrical terminals. Semi-Annually (1,000 Hours) Lubricate spindle bearings with 3–5g high-speed grease (Mobil Polyrex EM); check VFD. Annually (2,000 Hours) Replace complete set of multi-pocket filter bags (SPM-FLT-1004); inspect motor dynamic balance. 7.2 Comprehensive Troubleshooting Matrix Fault Symptom Probable Root Causes Corrective Action & Resolution Machine will not power ON Main breaker tripped; E-Stop locked down; blown fuse. Reset breaker; rotate E-Stop clockwise to release; check fuse. Motor hums but will not spin Phase loss on power line; VFD fault; arbor jam. Verify incoming line voltages; check VFD code; clear arbor. Excessive machine vibration Unbalanced buffing wheel; loose M16 lock nut. Dress or replace buffing wheel; tighten M16 nut to 45 N·m. Weak suction airflow at hood Filter bags caked; drawer unlatched; duct clog. Pump shaker lever 10 times; clamp drawer tight; clear duct. Workpiece burning (Acetate) RPM too high; excessive pressure; dry buffing wheel. Reduce speed to 2,000–2,400 RPM; use light touch; apply wax. Swirl marks / haze on surface Wheel contaminated with coarse compound/grit. Rake wheel clean; use dedicated buffing wheel per compound. Acoustic squeal / grinding noise Dry spindle bearings; loose drive belt rubbing frame. Grease bearings with Mobil Polyrex EM; adjust belt tension. 8. Spare Parts & Factory Service Contact 8.1 Genuine Factory Spare Parts Catalog Part Description & Specifications Factory Part No. Application & Replacement Notes Multi-Pocket Polyester Filter Bag Set (4 Pockets, 5–10µm) SPM-FLT-1004 Replace every 12–18 months depending on duty cycle Polycarbonate Safety Visor Shield (3mm High-Impact PC) SPM-SHD-PC01 Pre-drilled mounting holes with hinge hardware NSK High-Speed Spindle Deep Groove Ball Bearings (Pair) BRG-6205-2RS Pre-greased, double rubber sealed (25×52×15 mm) Over-Center Toggle Clamps with Rubber Spindle Pad CLP-TGL-GH403 Heavy-duty zinc-plated steel for recovery drawer M16 Left-Hand Reverse Thread Hex Nut & Clamping Flanges NUT-M16-LH02 Precision balanced alloy steel hardware set Mushroom Head Twist-to-Reset Emergency Stop Pushbutton SW-ESTOP-XB2 Standard 22mm panel mount, 1NC contact block 24W Industrial Shadowless Daylight LED Tube Luminaire LED-T8-24W-6.5K 6500K Color Temperature, IP54 dust resistant EPDM Foam Airtight Recovery Drawer Sealing Gasket GSK-EPDM-1505 Self-adhesive oil and wax resistant sponge rubber 8.2 Manufacturer Warranty & Official Contact The SPM-ECO-1000 is backed by a 12-Month Manufacturer Warranty covering motor, blower, VFD, and structural frame under normal industrial operation. For technical assistance, custom buffing process development, replacement wheels, or spare parts inquiries, contact our engineering support team. We also offer OEM/ODM customization and consumables supply for the full single-station polishing machine range — browse our finishing compounds and consumables categories for stage-matched waxes, compounds, and buffing wheels. Need a dust-controlled buffing workstation for your parts? Send your part material, size, current surface condition, and target finish. Our finishing team can recommend the right machine, wheels, compound, and test process. Contact Our Finishing Team JINTAIJIN POLISH MACHINERY CO., LTD. • Official website: www.surface-polish.com  |  Support email: info@surface-polish.com  |  ISO 9001:2015 & CE Certified
  • Double-Deck Bamboo Tumbling Machine: Standard Operating Procedure, Control Guide & Finishing Recipes
    Double-Deck Bamboo Tumbling Machine: Standard Operating Procedure, Control Guide & Finishing Recipes Aug 19 , 2026
    Double-Deck Bamboo Tumbling Machine: Standard Operating Procedure, Control Guide & Finishing Recipes Model Series: SP-TB4 / SP-TB8 • Precision Dry Tumbling System • Official operation manual The SP-TB Series double-deck bamboo tumbling machine is a precision dry tumbling system designed for high-gloss finishing of premium eyewear frames (acetate, propionate), fine hardware, jewelry, and luxury plastic or wood components. Its octagonal, seasoned bamboo barrels provide natural thermal buffering, gentle wax absorption, and a soft cascading action that delivers mirror-like surfaces without edge distortion. This manual covers machine structure, control panel operation, the full 6-step standard operating procedure (SOP), proven dry tumbling recipes, preventive maintenance, and quick troubleshooting. If you are comparing equipment options first, review our rotary barrel tumbling machines range or the wider finishing machine collection. Equipment overview & capability. The two-tier vertical architecture saves floor space while doubling batch output. Each barrel is built from aged natural bamboo staves with stainless steel ventilation screens, and the drive system is protected by a full-height yellow wire mesh guard. The machine is suited to acetate/propionate eyewear frames, fine hardware, jewelry, and luxury plastic/wood components. 1. Technical Parameters & Configuration The table below lists the standard engineering configuration of the SP-TB4 (4-barrel) and SP-TB8 (8-barrel) models. Technical Parameter Engineering Specification / Configuration Structure / Barrels Double-Deck (2 Tiers), 4 or 8 Octagonal Bamboo Barrels Barrel Material Aged Natural Bamboo Staves with SS Ventilation Filter Screens Main Motor / Power 2.2 kW / 3.0 HP High-Torque Heavy-Duty Motor (380V 3-Phase / 220V 1-Phase) Tumbling Speed 28 – 35 RPM (Optimized Gravity Cascade Angle: 45°–50°) Control System Digital Microprocessor Timer (0–99.9 h/m), Start, Stop, JOG Inching, Reset Safety Enclosure Full-Height Industrial Yellow Wire Mesh Guard Enclosure Discharge System Heavy-Duty Middle Galvanized Pull-Out Receiving Hopper Tray Official Support Website: www.surface-polish.com | Email: info@surface-polish.com 2. Machine Structure & Component Nomenclature The machine layout features a space-saving two-tier vertical architecture. The diagram and table below identify all primary structural components and their exact English technical terms. Figure 1: Machine Structural Layout & Subsystem Nomenclature # Component Functional Description & Operational Role 1 Bamboo Tumblers Dual-deck octagonal barrels (#3, #4 upper; #7, #8 lower) for gentle cascading dry polishing. 2 Clamping Bars & Latches Heavy-duty steel compression bars with quick-acting toggle clamps to secure hatch doors. 3 Ventilation Mesh Screens Perforated stainless steel screens to dissipate internal frictional heat and vent micro-dust. 4 Receiving Hopper Drawer Middle heavy-gauge galvanized collection tray for clean, rapid workpiece/media discharge. 5 Structural Steel Chassis Rigid, vibration-damped welded steel frame supporting dual-tier drive loads. 6 Yellow Safety Mesh Enclosure Full-height yellow wire mesh cage isolating transmission belts, pulleys, and drive chains. 7 Electric Control Cabinet Dust-proof electrical enclosure housing the pushbutton station, safety locks, and LED timer. 3. Control Panel & Operator Interface The front-mounted control station allows precise cycle management, automated timed shutoff, and micro-positioning (JOG) for loading and unloading. The digital timer automatically stops the machine when the programmed cycle is complete. Figure 2: Electrical Control Cabinet Interface & Button Layout Control Element Hardware Type / Color Operating Logic & Standard Action Power Lamp Red Pilot Lamp (Top) Illuminates continuously when the 3-phase/single-phase main power supply is energized. Start Button Green Pushbutton Latches the main magnetic contactor to start continuous automatic tumbling cycle. Stop Button Red Pushbutton Immediately de-energizes the drive motor and halts all barrel rotation. JOG / Inching Yellow Pushbutton Momentary run: rotates barrels only while pressed. Used to align doors for loading/unloading. Timer Reset Blue Pushbutton Resets the digital timer accumulator back to zero (00:00) for a new cycle run. Digital LED Timer Microprocessor Controller Digital display with +/- setting buttons. Automatically shuts down the machine upon cycle completion. CAUTION — JOG (inching) safety rule. Always use the yellow JOG button to rotate barrel doors into position. NEVER attempt to rotate barrels by hand when the motor is stopped or energized, as residual torque may cause pinch hazards. 4. Standard Operating Procedure (6-Step SOP) Follow this streamlined 6-step workflow to guarantee repeatable, mirror-grade polishing and ensure maximum operator safety. Figure 3: Standard Operating Procedure (6-Step Dry Tumbling Workflow) Step 1: Pre-Start Inspection & JOG Positioning. Verify the yellow safety cage is secured. Turn on the main isolator. Press the yellow JOG button intermittently until the target barrel door faces vertically upward (12 o’clock position). Step 2: Load Polishing Media & Workpieces. Release the red toggle latches, remove clamping bars, and open the hatch. Fill the barrel to 50%–60% total volume with walnut shells or corncobs. Add workpieces at a strict 3:1 to 4:1 media-to-workpiece ratio. Step 3: Apply Polishing Wax / Rolling Cream. Distribute specialized polishing wax or rolling oil evenly across the media (15–30 g per batch). Ensure the ventilation screens are clean and unclogged. Step 4: Secure Clamping Bars & Latches. Reinstall the barrel hatch door. Position the steel clamping bars and engage the red toggle clamps until firmly locked. Verify zero clearance around the door gasket. Step 5: Program Digital Timer & Press START. Press the blue TIMER RESET button. Set the desired cycle duration on the digital timer (e.g. 12.0 hours). Press the green START button. The machine runs continuously and auto-stops upon completion. Step 6: Discharge & Workpiece Separation. Slide the galvanized receiving hopper drawer directly under the target barrel. Use the JOG button to rotate the barrel door downward (6 o’clock position). Release the latches, open the hatch, and discharge the contents into the hopper for screening. 5. Dry Tumbling Process Recipes & Media Matrix Dry tumbling relies on progressive multi-stage micro-cutting and buffing. Use the proven recipe chart below for acetate eyewear, luxury plastics, and precision metals. Cycle times are typical starting ranges and should be confirmed with sample parts. Process Stage Recommended Media Polishing Compound Cycle Time Surface Objective 1. Rough Cutting Coarse Walnut Shell (16#–20#) Rough Cut Wax / Gray Paste 8 – 14 Hours Removes CNC milling marks, burrs, and parting lines. 2. Medium Smoothing Medium Walnut Shell (24#–36#) Medium Polish Cream / Brown Wax 10 – 16 Hours Smooths micro-scratches, creates uniform satin finish. 3. Fine Glossing Fine Corncob (20#–40#) / Bamboo Pegs Fine Buffing Oil / White Wax 12 – 18 Hours Enhances surface depth, semi-bright luster, prepares for mirror finish. 4. High Mirror Luster Micro Corncob (40#–60#) / Hard Pegs Mirror Finish Glaze / Blue-Green Wax 14 – 24 Hours Produces flawless, ultra-deep optical clarity & mirror reflection. Pro tip — tumbling volume & density control. Optimal tumbling efficiency occurs at 50%–60% total barrel fill. Never underfill (below 40%, risks severe impact damage) or overfill (above 70%, prevents cascading action and causes matte dead spots). Media and compound selection is the largest variable in dry tumbling results. Browse our dry finishing media range for walnut shell and corncob grades, or review finishing compounds for stage-matched waxes and glazes. 6. Preventive Maintenance & Quick Troubleshooting 6.1 Routine Maintenance Schedule Daily check: inspect door toggle clamps and rubber gaskets for wear. Clear accumulated dust from ventilation mesh screens using a soft brush or shop vacuum. Weekly check: check drive belt tension inside the yellow mesh cage (approx. 10–12 mm deflection under firm thumb pressure). Inspect chain lubrication. Monthly service: apply NLGI #2 lithium grease to all pillow block bearings via grease nipples. Inspect bamboo staves for tightness; tighten mounting bolts if loose. 6.2 Quick Troubleshooting Matrix Fault Symptom Probable Root Cause Corrective Action / Solution Machine fails to start when pressing START Main power off / emergency halt engaged / timer not set / fuse blown Check red power lamp, release stop button, reset timer, check supply breaker. JOG button works but START does not latch Timer timed out / contactor auxiliary contact fault Press blue Timer Reset button; inspect contactor wiring inside control box. Excessive noise or vibration during run Worn pillow block bearing / loose drive chain / unbalanced load Lubricate or replace bearings, adjust chain tensioner, ensure even media filling. Media dust leaking during operation Worn hatch sealing gasket / toggle clamps not fully locked Inspect and replace silicone gasket; adjust clamping bar latch tension. Workpieces have uneven or poor luster Improper media ratio / insufficient wax / clogged mesh screens Adjust media-to-part ratio toward 4:1; clean ventilation screens to prevent overheating. 7. Technical Support & Custom Process Development For technical assistance, custom tumbling process development, replacement barrels, or spare parts inquiries, contact our engineering support team. We also offer OEM/ODM customization, polishing compounds and media supply, and wear parts for the full SP-TB series. Need a custom dry tumbling process for your parts? Send your part material, size, current surface condition, and target finish. Our finishing team can recommend the right machine, media, compound, and test process. Contact Our Finishing Team Official website: www.surface-polish.com  |  Support email: info@surface-polish.com
  • How to Choose Media Size for Small Holes, Slots and Internal Cavities
    How to Choose Media Size for Small Holes, Slots and Internal Cavities Jul 27 , 2026
    How to Choose Media Size for Small Holes, Slots and Internal Cavities How to Choose Media Size for Small Holes, Slots and Internal Cavities Short answer: choose the smallest media that reaches the required feature and can still be separated reliably. A smaller chip may improve access, but it can also lodge in a hole, pass through a slot, slow separation or change the contact intensity. The correct size is therefore a geometry, defect, machine and inspection decision—not a simple “smaller is better” rule. Important: confirm media access and separation on representative parts. A catalog size is not proof that a particular shape will pass through your feature without becoming trapped. 1. Map the feature before selecting media Record the smallest opening, slot width, cavity depth and passage length. Also mark threads, sealing faces, cosmetic surfaces and edges that must not be over-rounded. The critical dimension is often not the nominal hole diameter: an angled entry, burr, cross-hole or blind cavity can reduce the usable passage. Through holes: check entry and exit burrs, cross-sections and the chance of a chip passing through and becoming trapped elsewhere.Slots: compare the shortest slot dimension with the media's smallest cross-section and orientation.Blind cavities: check whether media can enter, circulate and leave without packing at the bottom.Internal channels: confirm that the process objective is reachable; surface contact inside a channel may be uneven. 2. Use a fit-and-function screen, not only a size label QuestionWhy it mattersTrial check Can the media enter?A large or poorly oriented shape may never reach the burr.Mark entry and exit; inspect after a short cycle. Can the media leave?Trapped chips create rework, contamination and customer risk.Count retained pieces after separation and washing. Can it protect the edge?Too small or too sharp a contact can increase edge rounding.Measure edge radius and critical dimensions. Media shape changes the effective cross-section. Cylinders, triangles, angle-cut shapes and plastic forms do not enter the same feature in the same way. Select a shape and size together, then check the machine's circulation and separation method. 3. Balance access with lodging and separation Reducing media size may improve access but can make separation slower, especially when the workpiece has many small openings or when the media approaches the feature size. Review the machine's screen, magnetic, flow or vibration separation method before approving a fine media grade. The ceramic versus plastic media guide explains why media family and shape must be considered with geometry. Do not rely on visual shake-out alone. Use a defined retention check, such as a counted sample, flushing step or controlled inspection of cavities. The acceptance method should match the part's risk and customer requirements. 4. Match size to the incoming defect and target finish A small media chip may reach a cavity but lack the mass or cutting action needed to remove a heavy burr. Conversely, a large aggressive media can remove material quickly on an exposed edge while missing the internal feature. Separate the objectives: internal burr removal, surface smoothing, edge radiusing and final polishing may require different stages or machine concepts. For delicate or high-value parts, compare loose bulk finishing with a process that holds the workpiece, such as drag or stream finishing. The machine choice should follow the geometry and damage risk, not the media label alone. 5. A repeatable media-size trial Measure and record the smallest opening, depth and passage length.Select two candidate shapes and two sizes that can be separated by the available equipment.Run a short access trial, then inspect every critical cavity for retained media.Measure burr removal, edge radius, roughness or visual finish as specified.Run the best candidate again with a fresh sample to confirm repeatability.Document the media, machine, load, compound/water, cycle time and separation method. Use the mass-finishing sample trial record to document the size decision and release criteria. For broader machine capacity choices, see the bowl and tub selection guide. Buyer checklistSmallest opening, slot width, cavity depth and passage lengthIncoming burr height and target edge radiusMaterial, hardness, critical dimensions and cosmetic facesCandidate media shape, size and separation methodMachine type, load ratio, compound/water and cycle timeRetention acceptance method and documented release criteria Need help selecting media for internal features?Send the part drawing or photos, smallest passage, incoming burr and target finish. We can help define an access, separation and inspection trial before equipment or media are finalized.Contact SurfacePolish for a process review This guide is a process-selection framework. Final media size, shape and cycle must be confirmed on representative parts.
  • How to Choose Media Size for Small Holes, Slots and Internal Cavities
    How to Choose Media Size for Small Holes, Slots and Internal Cavities Jul 27 , 2026
    How to Choose Media Size for Small Holes, Slots and Internal Cavities How to Choose Media Size for Small Holes, Slots and Internal Cavities Short answer: choose the smallest media that reaches the required feature and can still be separated reliably. A smaller chip may improve access, but it can also lodge in a hole, pass through a slot, slow separation or change the contact intensity. The correct size is therefore a geometry, defect, machine and inspection decision—not a simple “smaller is better” rule. Important: confirm media access and separation on representative parts. A catalog size is not proof that a particular shape will pass through your feature without becoming trapped. 1. Map the feature before selecting media Record the smallest opening, slot width, cavity depth and passage length. Also mark threads, sealing faces, cosmetic surfaces and edges that must not be over-rounded. The critical dimension is often not the nominal hole diameter: an angled entry, burr, cross-hole or blind cavity can reduce the usable passage. Through holes: check entry and exit burrs, cross-sections and the chance of a chip passing through and becoming trapped elsewhere.Slots: compare the shortest slot dimension with the media's smallest cross-section and orientation.Blind cavities: check whether media can enter, circulate and leave without packing at the bottom.Internal channels: confirm that the process objective is reachable; surface contact inside a channel may be uneven. 2. Use a fit-and-function screen, not only a size label QuestionWhy it mattersTrial check Can the media enter?A large or poorly oriented shape may never reach the burr.Mark entry and exit; inspect after a short cycle. Can the media leave?Trapped chips create rework, contamination and customer risk.Count retained pieces after separation and washing. Can it protect the edge?Too small or too sharp a contact can increase edge rounding.Measure edge radius and critical dimensions. Media shape changes the effective cross-section. Cylinders, triangles, angle-cut shapes and plastic forms do not enter the same feature in the same way. Select a shape and size together, then check the machine's circulation and separation method. 3. Balance access with lodging and separation Reducing media size may improve access but can make separation slower, especially when the workpiece has many small openings or when the media approaches the feature size. Review the machine's screen, magnetic, flow or vibration separation method before approving a fine media grade. The ceramic versus plastic media guide explains why media family and shape must be considered with geometry. Do not rely on visual shake-out alone. Use a defined retention check, such as a counted sample, flushing step or controlled inspection of cavities. The acceptance method should match the part's risk and customer requirements. 4. Match size to the incoming defect and target finish A small media chip may reach a cavity but lack the mass or cutting action needed to remove a heavy burr. Conversely, a large aggressive media can remove material quickly on an exposed edge while missing the internal feature. Separate the objectives: internal burr removal, surface smoothing, edge radiusing and final polishing may require different stages or machine concepts. For delicate or high-value parts, compare loose bulk finishing with a process that holds the workpiece, such as drag or stream finishing. The machine choice should follow the geometry and damage risk, not the media label alone. 5. A repeatable media-size trial Measure and record the smallest opening, depth and passage length.Select two candidate shapes and two sizes that can be separated by the available equipment.Run a short access trial, then inspect every critical cavity for retained media.Measure burr removal, edge radius, roughness or visual finish as specified.Run the best candidate again with a fresh sample to confirm repeatability.Document the media, machine, load, compound/water, cycle time and separation method. Use the mass-finishing sample trial record to document the size decision and release criteria. For broader machine capacity choices, see the bowl and tub selection guide. Buyer checklistSmallest opening, slot width, cavity depth and passage lengthIncoming burr height and target edge radiusMaterial, hardness, critical dimensions and cosmetic facesCandidate media shape, size and separation methodMachine type, load ratio, compound/water and cycle timeRetention acceptance method and documented release criteria Need help selecting media for internal features?Send the part drawing or photos, smallest passage, incoming burr and target finish. We can help define an access, separation and inspection trial before equipment or media are finalized.Contact SurfacePolish for a process review This guide is a process-selection framework. Final media size, shape and cycle must be confirmed on representative parts.
  • How to Choose Media Size for Small Holes, Slots and Internal Cavities
    How to Choose Media Size for Small Holes, Slots and Internal Cavities Jul 27 , 2026
    How to Choose Media Size for Small Holes, Slots and Internal Cavities How to Choose Media Size for Small Holes, Slots and Internal Cavities Short answer: choose the smallest media that reaches the required feature and can still be separated reliably. A smaller chip may improve access, but it can also lodge in a hole, pass through a slot, slow separation or change the contact intensity. The correct size is therefore a geometry, defect, machine and inspection decision—not a simple “smaller is better” rule. Important: confirm media access and separation on representative parts. A catalog size is not proof that a particular shape will pass through your feature without becoming trapped. 1. Map the feature before selecting media Record the smallest opening, slot width, cavity depth and passage length. Also mark threads, sealing faces, cosmetic surfaces and edges that must not be over-rounded. The critical dimension is often not the nominal hole diameter: an angled entry, burr, cross-hole or blind cavity can reduce the usable passage. Through holes: check entry and exit burrs, cross-sections and the chance of a chip passing through and becoming trapped elsewhere.Slots: compare the shortest slot dimension with the media's smallest cross-section and orientation.Blind cavities: check whether media can enter, circulate and leave without packing at the bottom.Internal channels: confirm that the process objective is reachable; surface contact inside a channel may be uneven. 2. Use a fit-and-function screen, not only a size label QuestionWhy it mattersTrial check Can the media enter?A large or poorly oriented shape may never reach the burr.Mark entry and exit; inspect after a short cycle. Can the media leave?Trapped chips create rework, contamination and customer risk.Count retained pieces after separation and washing. Can it protect the edge?Too small or too sharp a contact can increase edge rounding.Measure edge radius and critical dimensions. Media shape changes the effective cross-section. Cylinders, triangles, angle-cut shapes and plastic forms do not enter the same feature in the same way. Select a shape and size together, then check the machine's circulation and separation method. 3. Balance access with lodging and separation Reducing media size may improve access but can make separation slower, especially when the workpiece has many small openings or when the media approaches the feature size. Review the machine's screen, magnetic, flow or vibration separation method before approving a fine media grade. The ceramic versus plastic media guide explains why media family and shape must be considered with geometry. Do not rely on visual shake-out alone. Use a defined retention check, such as a counted sample, flushing step or controlled inspection of cavities. The acceptance method should match the part's risk and customer requirements. 4. Match size to the incoming defect and target finish A small media chip may reach a cavity but lack the mass or cutting action needed to remove a heavy burr. Conversely, a large aggressive media can remove material quickly on an exposed edge while missing the internal feature. Separate the objectives: internal burr removal, surface smoothing, edge radiusing and final polishing may require different stages or machine concepts. For delicate or high-value parts, compare loose bulk finishing with a process that holds the workpiece, such as drag or stream finishing. The machine choice should follow the geometry and damage risk, not the media label alone. 5. A repeatable media-size trial Measure and record the smallest opening, depth and passage length.Select two candidate shapes and two sizes that can be separated by the available equipment.Run a short access trial, then inspect every critical cavity for retained media.Measure burr removal, edge radius, roughness or visual finish as specified.Run the best candidate again with a fresh sample to confirm repeatability.Document the media, machine, load, compound/water, cycle time and separation method. Use the mass-finishing sample trial record to document the size decision and release criteria. For broader machine capacity choices, see the bowl and tub selection guide. Buyer checklistSmallest opening, slot width, cavity depth and passage lengthIncoming burr height and target edge radiusMaterial, hardness, critical dimensions and cosmetic facesCandidate media shape, size and separation methodMachine type, load ratio, compound/water and cycle timeRetention acceptance method and documented release criteria Need help selecting media for internal features?Send the part drawing or photos, smallest passage, incoming burr and target finish. We can help define an access, separation and inspection trial before equipment or media are finalized.Contact SurfacePolish for a process review This guide is a process-selection framework. Final media size, shape and cycle must be confirmed on representative parts.
  • How to Choose Media Size for Small Holes, Slots and Internal Cavities
    How to Choose Media Size for Small Holes, Slots and Internal Cavities Jul 27 , 2026
    How to Choose Media Size for Small Holes, Slots and Internal Cavities How to Choose Media Size for Small Holes, Slots and Internal Cavities Short answer: choose the smallest media that reaches the required feature and can still be separated reliably. A smaller chip may improve access, but it can also lodge in a hole, pass through a slot, slow separation or change the contact intensity. The correct size is therefore a geometry, defect, machine and inspection decision—not a simple “smaller is better” rule. Important: confirm media access and separation on representative parts. A catalog size is not proof that a particular shape will pass through your feature without becoming trapped. 1. Map the feature before selecting media Record the smallest opening, slot width, cavity depth and passage length. Also mark threads, sealing faces, cosmetic surfaces and edges that must not be over-rounded. The critical dimension is often not the nominal hole diameter: an angled entry, burr, cross-hole or blind cavity can reduce the usable passage. Through holes: check entry and exit burrs, cross-sections and the chance of a chip passing through and becoming trapped elsewhere.Slots: compare the shortest slot dimension with the media's smallest cross-section and orientation.Blind cavities: check whether media can enter, circulate and leave without packing at the bottom.Internal channels: confirm that the process objective is reachable; surface contact inside a channel may be uneven. 2. Use a fit-and-function screen, not only a size label QuestionWhy it mattersTrial check Can the media enter?A large or poorly oriented shape may never reach the burr.Mark entry and exit; inspect after a short cycle. Can the media leave?Trapped chips create rework, contamination and customer risk.Count retained pieces after separation and washing. Can it protect the edge?Too small or too sharp a contact can increase edge rounding.Measure edge radius and critical dimensions. Media shape changes the effective cross-section. Cylinders, triangles, angle-cut shapes and plastic forms do not enter the same feature in the same way. Select a shape and size together, then check the machine's circulation and separation method. 3. Balance access with lodging and separation Reducing media size may improve access but can make separation slower, especially when the workpiece has many small openings or when the media approaches the feature size. Review the machine's screen, magnetic, flow or vibration separation method before approving a fine media grade. The ceramic versus plastic media guide explains why media family and shape must be considered with geometry. Do not rely on visual shake-out alone. Use a defined retention check, such as a counted sample, flushing step or controlled inspection of cavities. The acceptance method should match the part's risk and customer requirements. 4. Match size to the incoming defect and target finish A small media chip may reach a cavity but lack the mass or cutting action needed to remove a heavy burr. Conversely, a large aggressive media can remove material quickly on an exposed edge while missing the internal feature. Separate the objectives: internal burr removal, surface smoothing, edge radiusing and final polishing may require different stages or machine concepts. For delicate or high-value parts, compare loose bulk finishing with a process that holds the workpiece, such as drag or stream finishing. The machine choice should follow the geometry and damage risk, not the media label alone. 5. A repeatable media-size trial Measure and record the smallest opening, depth and passage length.Select two candidate shapes and two sizes that can be separated by the available equipment.Run a short access trial, then inspect every critical cavity for retained media.Measure burr removal, edge radius, roughness or visual finish as specified.Run the best candidate again with a fresh sample to confirm repeatability.Document the media, machine, load, compound/water, cycle time and separation method. Use the mass-finishing sample trial record to document the size decision and release criteria. For broader machine capacity choices, see the bowl and tub selection guide. Buyer checklistSmallest opening, slot width, cavity depth and passage lengthIncoming burr height and target edge radiusMaterial, hardness, critical dimensions and cosmetic facesCandidate media shape, size and separation methodMachine type, load ratio, compound/water and cycle timeRetention acceptance method and documented release criteria Need help selecting media for internal features?Send the part drawing or photos, smallest passage, incoming burr and target finish. We can help define an access, separation and inspection trial before equipment or media are finalized.Contact SurfacePolish for a process review This guide is a process-selection framework. Final media size, shape and cycle must be confirmed on representative parts.
  • How to Prevent Part-on-Part Damage in Vibratory Finishing
    How to Prevent Part-on-Part Damage in Vibratory Finishing Jul 24 , 2026
    How to Prevent Part-on-Part Damage in Vibratory Finishing How to Prevent Part-on-Part Damage in Vibratory Finishing Short answer: part-on-part damage is usually a contact-control problem. Protect the workpieces with enough media coverage, a suitable media size and shape, a stable load ratio and a machine motion that keeps parts separated. Confirm the change with before-and-after inspection instead of assuming that a softer media or shorter cycle will solve every defect. Important: the same scratch or dent can have different causes, including direct workpiece contact, media lodging, contamination or an aggressive process. Use a controlled trial to isolate one variable at a time. 1. Identify the damage before changing the process Record where the defect appears and when it is introduced. Map cosmetic faces, thin walls, threads, sealing surfaces and sharp edges. A repeated mark on a mating face suggests a different control problem from random dents on an exposed corner. Scratches: check trapped chips, broken media, contamination and sliding contact.Dents or impact marks: check direct part contact, drop height, fill level and excessive machine intensity.Edge damage: check media shape, unsupported features and over-processing.Uneven damage: check loading pattern, circulation and whether parts are segregating in the bowl or tub. 2. Keep workpieces separated with media coverage Media should surround the parts so that workpieces are not repeatedly striking each other. A low media-to-part ratio can expose the parts; an overloaded machine can restrict circulation and create local contact. Start from the machine supplier's recommended fill range, then confirm actual movement with a representative load. Small openings and recessed features need special attention. Media that is too large may not protect an internal surface, while media that is too small can lodge in holes or become difficult to separate. For a broader machine and capacity decision, see the bowl and tub selection guide. 3. Match media shape and hardness to the risk Observed riskTrial directionWhat to measure Impact on cosmetic facesLower-impact media, more coverage, lower intensityDent count, visual grade, cycle time Scratches from contaminationClean media, screen fines, separate material familiesScratch length, residue, media condition Thin features contacting each otherChange loading, reduce drop/contact intensity, consider fixturingBend, dent depth, dimensional change Media selection should remain tied to the finishing objective. A more aggressive cutting media may remove a burr faster but can also increase edge rounding or impact risk. Review the ceramic versus plastic media guide before changing media family. 4. Control machine motion, load and cycle time Machine type changes how parts circulate, slide and separate. Bowl vibrators, tubs, rotary barrels and centrifugal systems do not create the same contact pattern. Check amplitude or speed, load ratio, media fill, water and compound condition, and actual cycle time. If damage increases late in the cycle, the process may be stable initially but over-processing the surface. Do not solve a contact problem only by reducing time if the incoming burr or contamination remains. Instead, compare a small process matrix and retain the best result in a trial record. 5. A repeatable trial for separating part-on-part causes Photograph and label ten representative parts before processing.Mark critical faces and record incoming burrs, scratches and dimensions.Run a baseline load, then change only one variable: media coverage, media shape, machine intensity or cycle time.Inspect after a short interval and at the final interval; do not inspect only the final batch.Record dents, scratches, edge radius, residue and media separation results.Repeat the best setting with a second sample to confirm that the result is stable. The mass-finishing sample trial record provides a practical structure for recording the variables and release decision. 6. When to consider fixturing or another finishing process Some geometries cannot be protected reliably by loose media alone. Thin blades, delicate cosmetic faces, deep cavities and parts with strict edge-radius limits may need fixturing, a different machine family or a dedicated finishing stage. Treat this as an engineering decision, not a failure of the operator to find the right cycle. Buyer checklistWhere does the damage appear and what does it look like?What are the part material, hardness, weight and critical surfaces?What is the smallest hole, slot or recess that media must access?What are the current media size, shape, fill and condition?What machine, speed/frequency, load and cycle time are being used?Which dimensions, edge radius or cosmetic standard must be released? Need help reducing contact damage?Share the part drawing or photos, incoming defect, target finish, current machine and media details. We can help define a controlled sample trial and identify the variables that need confirmation.Contact SurfacePolish for a process review This guide is an engineering selection framework. Final media, machine and cycle decisions should be confirmed on representative parts and documented with inspection results.
  • How to Choose Ceramic vs Plastic Media for Aluminum, Brass and Steel Parts
    How to Choose Ceramic vs Plastic Media for Aluminum, Brass and Steel Parts Jul 23 , 2026
    Ceramic vs Plastic Tumbling Media for Aluminum, Brass and Steel Parts How to Choose Ceramic vs Plastic Media for Aluminum, Brass and Steel Parts Short answer: choose ceramic media when controlled cutting, burr removal or edge radiusing is the priority; choose plastic media when a lower-impact, lighter-contact process is needed for softer metals, cosmetic surfaces or a finer finishing stage. The correct choice still depends on part geometry, incoming defects, target finish, machine motion and trial results. Important: media selection is a process decision, not a universal material rule. Supplier pages describe product capabilities; research papers describe mechanisms under specific conditions. Confirm the result on representative parts before approving a production recipe. 1. Start with the finishing objective Separate the objective into one primary target and any secondary targets: Deburring: remove a defined burr without damaging threads, holes or sealing faces. Edge radiusing: create a controlled edge radius rather than simply making the edge “smooth.” Smoothing: reduce peaks and blend machining or casting marks. Polishing: improve brightness or reduce roughness after a suitable pre-finish. Cleaning: remove oil, scale or loose residue without over-processing the part. Open research links material removal and surface topography to particle contacts, process parameters and initial surface condition. That is why the same media can behave differently on two parts that look similar but have different burr height, hardness or geometry. 2. Ceramic vs plastic: a practical comparison Decision factorCeramic mediaPlastic media Typical roleCutting, deburring, edge radiusing, surface grindingLower-impact smoothing, polishing and separation-sensitive work Contact behaviorHigher density can increase contact pressure and cutting actionLighter contact can reduce impact on softer or cosmetic surfaces Common fitSteel, iron, aluminum, brass and difficult burrsAluminum, brass, plastics and parts where impact marks are a concern Main risksExcess edge rounding, media lodging or cosmetic impact if over-aggressiveLonger cycle, media wear, foam/chemistry sensitivity and insufficient burr removal Best next stepControl shape, size, load and time with edge-radius checksCheck separation, surface appearance, wear and cycle-time stability This comparison is a selection framework synthesized from official media guidance and open finishing research; it is not a promise that every ceramic or plastic formulation will behave identically. 3. Match media to material and geometry Aluminum Aluminum often needs enough cutting action to remove burrs, but excessive impact or unsuitable chemistry can create cosmetic damage or residue. Begin with a less aggressive trial when the part has thin walls, visible faces or sealing surfaces. Use a small enough media size to reach the required features, while checking that it cannot lodge in holes or slots. Brass Brass valves and fittings require protection of threads, seats and sealing faces. Ceramic may be appropriate for controlled burr removal, while plastic may be preferable for a lighter finishing stage. Keep the objective explicit: thread-safe deburring is different from bright cosmetic polishing. See the existing brass valves and fittings guide for part-specific risks. Steel and stainless steel Steel parts can tolerate stronger cutting action than many soft alloys, but the required result may still be a controlled edge break rather than maximum stock removal. For small fasteners, compare burr removal, thread condition and media separation in the same trial record. Use the small fastener deburring guide as the application context. 4. Shape, size and the three failure modes to check Media shape and access Cylinders, triangles, angle-cut shapes and other geometries behave differently in slots, holes and recessed areas. A smaller media size can improve access, but it can also increase separation difficulty or lodging risk. Choose the smallest media that can be separated reliably after the process, not simply the smallest media available. Part-on-part impact Mixed loading, insufficient media coverage or an unsuitable machine motion can allow parts to strike each other. Inspect cosmetic faces, thin walls and sharp features after each trial stage. If contact damage is unacceptable, investigate fixturing, a different machine family or a lower-impact media/process combination. Excess edge rounding Deburring and edge radiusing are not the same as removing as much material as possible. Record burr height before processing and edge radius after processing. If the edge radius grows beyond the drawing or assembly requirement, reduce cutting intensity, cycle time or media aggressiveness before changing the entire machine concept. 5. Machine and compound choices Media cannot be selected independently of the machine. A bowl, tub, rotary barrel, centrifugal unit, drag finisher or magnetic polisher creates a different contact pattern. For a broader bowl-versus-tub and capacity decision, use the existing vibratory machine selection guide. For small precision components and magnetic pins, compare the magnetic polishing machine page. Wet processes also depend on water and compound condition. Track concentration, foam, contamination, pH or conductivity where relevant to the process. Dry finishing uses a different control logic: the medium, paste or powder, dust extraction and housekeeping must be evaluated together. Do not transfer a wet-process cycle directly to dry media. 6. A sample-trial method buyers can repeat Define the incoming condition: material, hardness if known, burr height, surface defects and critical dimensions. Mark critical zones: threads, holes, sealing faces, cosmetic faces and edges requiring a defined radius. Run a small matrix: ceramic vs plastic, two media sizes, and two cycle times. Change one variable at a time where possible. Record machine type, load ratio, media fill, compound/water condition, speed or frequency and actual cycle time. Measure burr height, edge radius, Ra/Sa where specified, visual defects and media separation performance. Keep samples and photographs with the trial record. Approve a recipe only after repeat runs show stable results. Use the printable mass-finishing sample trial record to keep the comparison auditable. 7. Buyer checklist before requesting a quotation Part material, hardness and surface condition Part dimensions, weight, batch size and production target Smallest hole/slot and any media-lodging risk Critical edges, threads, sealing faces and cosmetic surfaces Target burr height, edge radius, roughness or visual standard Wet or dry process preference, water handling and separation requirements Photos or drawings that can be shared for a sample trial Need help selecting media? Send the part material, geometry, incoming defect, target finish and a few representative samples. We can help define a trial matrix and identify the machine, media and compound variables that need confirmation. Request a process discussion Source basis and evidence boundary This article synthesizes public technical information from Rösler, OTEC and Walther Trowal with open research on material removal, contact conditions, roughness measurement and additive-manufacturing post-processing. Manufacturer pages describe their own systems and consumables; research results apply to their stated test conditions. Production parameters, finish guarantees and compliance claims require a representative sample trial.

#+86-592-2381506

Email : info@surface-polish.com

Headquarters address : No. 31, Xinchang Road, Xinyang Industrial Zone, Haicang District, Xiamen

click here to leave a message

Leave A Message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.

Home

Products

whatsapp

contact